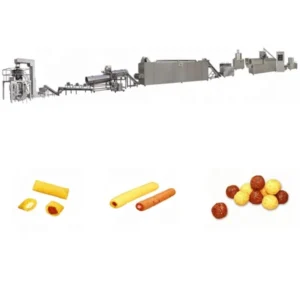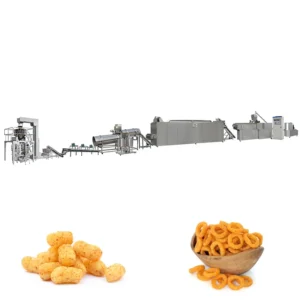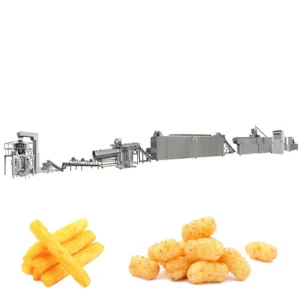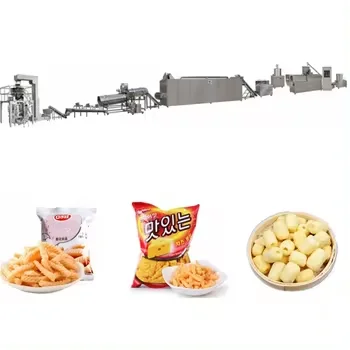
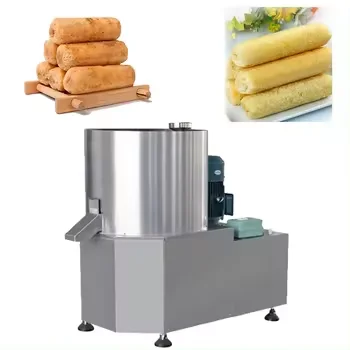
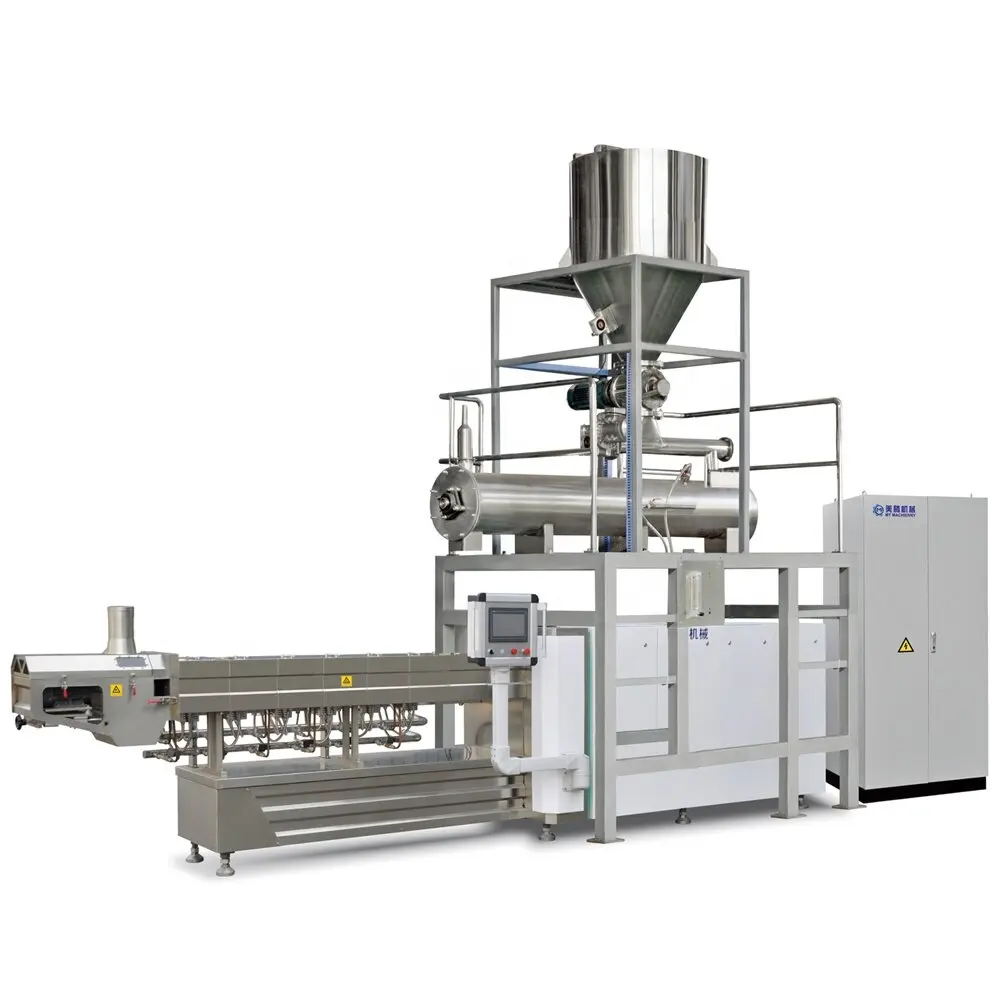
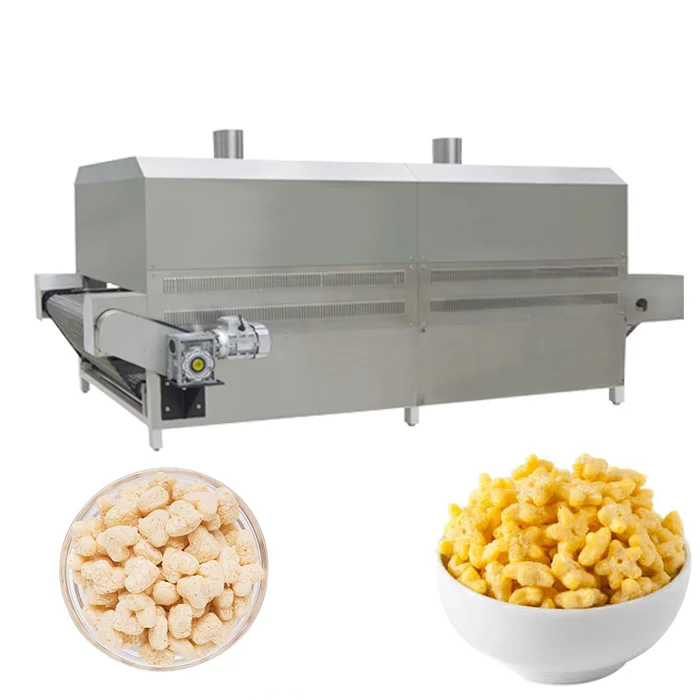
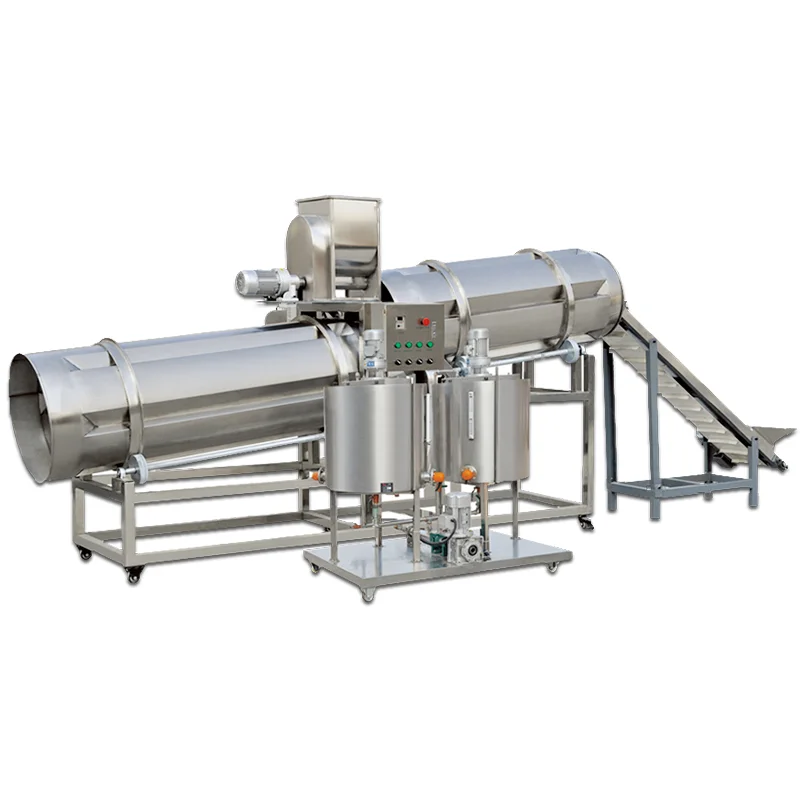
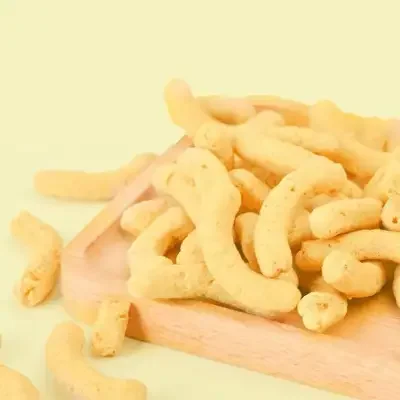
MT65/MT70/MT85/MT100 Twin Screw Puffed Snacks Extrusion Line, Frequency Speed Control, CE Certified — complete turnkey solution from batching through extrusion, drying, flavoring to packing.
- Throughput matched across every station so extruder output aligns with dryer and coating drum capacity, preventing bottlenecks on your actual flour blend.
Screw configuration and die design are specified to your raw material and target shape, with in-house trial runs documented before shipment.
Description
Matched Throughput Across Every Station — we balance extruder output with dryer, flavoring, and packing capacity so the puffed snacks extrusion production line runs without bottlenecks from raw material batching to final stacking.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Puffed Snacks Extrusion Line |
| Models Available | MT65, MT70, MT85, MT100 |
| Screw Type | Twin Screw |
| Installed Power | MT65: 130 kW / MT70: 180 kW / MT85: 220 kW / MT100: 240 kW |
| Real Power Consumption | MT65: 95 kW / MT70: 120 kW / MT85: 130 kW / MT100: 160 kW |
| Output Capacity | MT65: 120–150 kg/h (basis to be confirmed); MT70: 200–300 kg/h (basis to be confirmed); MT85: 300–500 kg/h (basis to be confirmed); MT100: 600–800 kg/h (basis to be confirmed) |
| Control System | Frequency speed controlling system |
| Line Stations | Mixing / Batching → Extruding → Drying → Coating / Flavoring → Cooling → Packing → Stacking |
| Drying Heat Source Options | Electric, Steam, or Gas |
| Flavoring System | Double drum flavoring line with sugar melting and spraying nozzle |
| Shape Customization | Interchangeable dies (cheese ball, tube, stick, ring, fruit loop, star, wheel, flower, heart, etc.) |
| Core Filling Option | Available with additional core filling machine and cutting machine |
| Voltage & Frequency | Configurable per destination market (to be confirmed before order) |
| Warranty | 1 year |
| Assembly State | Complete turnkey line with all auxiliary equipment integrated |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Directly expanded corn puffs and cheese balls | Corn flour, corn grits, rice flour |
| Ring, star, and tube-shaped puffed snacks | Wheat flour, oat flour, barley flour blends |
| Core-filled snacks with cream or chocolate center | Cereal-based dough with fat-based or sugar-based fillings |
| Multi-grain extruded breakfast cereal pieces | Mixed grain flour blends requiring controlled expansion |
| Fortified snack pellets for nutrition programs | Blended cereal and protein-supplemented raw materials |
Why Your Actual Flour Blend Matters More Than the Brochure Number
A capacity figure means nothing until it is proven on the exact raw material you will run.
I have watched lines get shipped across borders only to stall at half the promised output because the buyer’s flour had a different starch profile than the factory test sample. One Southeast Asian customer sent us a formula mixing cassava starch into standard corn flour after we had already configured the screw combination for pure corn. The gelatinization temperature shifted, the expansion ratio dropped, and it took four days of on-site screw reconfiguration before the product met spec. [NEED_CITE: starch gelatinization behavior in twin screw extrusion]
That is why every puffed snacks extrusion production line we build goes through a trial run in our testing workshop using the buyer’s own raw material before the machine leaves the factory. The actual throughput, expansion behavior, and texture get documented — not assumed from a generic test.
Matching Extruder Output to Downstream Capacity
The extruder is only one station on the line. If the dryer cannot remove moisture fast enough, product backs up and loses crunch. If the flavoring drums cannot coat at the rate the extruder produces, you get uneven seasoning or forced slowdowns. We calculate throughput at every station — mixing, extruding, drying, coating, cooling, and packing — and size each component so the entire turnkey corn puff making line runs at a consistent rate without any single station choking the others.
Screw Configuration Dictated by Your Formula, Not a Catalog Default
Twin screw extrusion gives us the flexibility to adjust screw element sequencing, pitch, and kneading block arrangement based on the specific starch, protein, and fat content of the buyer’s raw material. A high-fat formula needs a different shear profile than a lean corn grits mix. We record the screw and die configuration for each project so that when replacement wear parts are needed, the exact setup ships without guesswork. [NEED_CITE: twin screw element configuration for cereal extrusion]
Reading the Spec Sheet Against Your Production Target
Installed power and real power consumption tell different stories. The MT65 draws 130 kW at peak but typically runs at 95 kW during steady-state extrusion. That gap matters for electrical planning and transformer sizing at the installation site. The frequency speed controlling system lets operators fine-tune screw RPM to match raw material behavior batch by batch, maintaining consistent puff density even when ambient humidity or flour moisture varies between deliveries. The interchangeable die system means a single extruder platform can produce cheese balls, rings, sticks, and stars — shape changes require only a die swap and minor parameter adjustment rather than a full line reconfiguration. Drying heat source selection between electric, steam, or gas depends on local utility costs and availability, a decision that should happen during the layout phase, not after the dryer arrives.
What Happens When Line Stations Are Mismatched
An extruder running at full output while the coating drum operates at half capacity creates a cascade of problems. Product sits unseasoned on the conveyor, absorbing ambient moisture and losing surface crispness. Operators throttle the extruder down to match the coater, which means running below the designed throughput and changing the residence time inside the barrel. That shift alters the expansion ratio, producing a denser puff that does not match the market sample the buyer approved. [NEED_CITE: effect of line imbalance on extruded snack quality]
Why Project Buyers Specify This Line
Every station from batching to stacking comes from one supplier, which means throughput calculations are coordinated across the entire turnkey corn puff making line rather than stitched together from separate vendors. The in-house testing workshop runs trial production on the buyer’s actual flour blend before shipment, producing a documented report with real output data. Screw and die configurations are engineered for the specific raw material and target product shape, not copied from a generic reference build. The core filling option integrates inline with the existing cutting and conveying system, so adding filled snacks later does not require tearing out and replacing downstream equipment. Frequency speed control at the extruder gives operators a practical way to adjust for raw material variation without stopping production.
Documentation & Verification
- Line layout drawing showing station spacing and throughput balance calculations
- Screw and die configuration record specific to your flour blend and target shape
- Trial run report on your raw material documenting expansion ratio and output
- Electrical schematic with confirmed voltage, frequency, and control language
- CE declaration of conformity and ISO certificate for customs clearance
- Operation and maintenance manual with wear parts replacement schedule
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line footprint from mixer to stacker
- Dedicated electrical circuit sized to the confirmed real power consumption of your model
- Modular station delivery with sequenced unloading matching the installation order
- On-site screw and die verification against the trial run configuration before first production
- Operator training covering frequency speed adjustment, die changes, and daily cleaning routines
- Wear parts list with lead times for screws, dies, and flavoring nozzles
Before You Send the Inquiry
Tell us the exact flour blend or raw material formula you plan to run, including any starch or protein additives, along with your target product shapes and whether core filling is part of the plan. Share your workshop dimensions and ceiling height so we can draft a line layout that fits, and confirm the local voltage and frequency standard plus the preferred control panel language. If you can send a sample of your raw material, we will run it in the testing workshop and include the trial results with the proposal.
Frequently Asked Questions
Q: How do you verify line capacity on my specific raw material before shipment?
A: We run your actual flour blend through the extruder in our testing workshop, adjusting screw configuration and barrel temperature until the product meets your target expansion and texture. The trial run report documents real output, moisture loss through the dryer, and flavoring coverage — so the capacity figure you receive is based on your material, not a generic test.
Q: What is the phased installation and commissioning schedule for a full turnkey line?
A: Stations arrive in installation sequence, starting with the mixing and batching system and ending with the packing and stacking section. Our engineers supervise unloading, mechanical assembly, electrical connection, and then run each station individually before linking them. Full-line commissioning typically follows a structured checklist covering every parameter from screw speed to dryer temperature.
Q: How do you ensure extruder output is matched to dryer and flavoring drum capacity?
A: During the layout phase, we calculate the mass flow rate at each station based on your target output and raw material moisture content. The dryer belt length, airflow, and heat source are sized to handle the extruder’s actual throughput, and the double drum flavoring system is selected to coat at the same rate without product backlog.
Q: Can the line produce both directly expanded and core-filled snacks on the same platform?
A: Yes. The core filling machine and cutting unit integrate inline with the existing extruder and conveyor system. Switching between directly expanded shapes and core-filled products involves changing the die, adding the filling station into the product flow, and adjusting cutting parameters — no major mechanical overhaul is required.
Q: What operator training and ongoing maintenance support is included after commissioning?
A: Our on-site team trains your operators on frequency speed adjustment, die changeover procedures, dryer temperature management, and daily cleaning protocols. You receive a documented wear parts list with recommended replacement intervals for screws, dies, and spray nozzles, plus access to remote technical support for parameter troubleshooting after our engineers depart.
Related products
-

Automatic Puffed Food Snack Machine Electric Corn Puffs Snacks Making Machinery New Condition Flavorful Puff Snack Production
¥7,550.00 Select options This product has multiple variants. The options may be chosen on the product page -

Crunchy Puffed Snack Breakfast Cereal Corn Flakes Making Machine
¥1,000.00 Select options This product has multiple variants. The options may be chosen on the product page -

New Stainless Steel Automatic Snack Food Machinery Extruder Puffed Corn Maize Puff Processing Line for Food Industry High
¥12,350.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Rice Crispies Extruder Machine/Chocolate Corn Flakes Extrusion Plant/wheat Flaking Snacks Production Line
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page