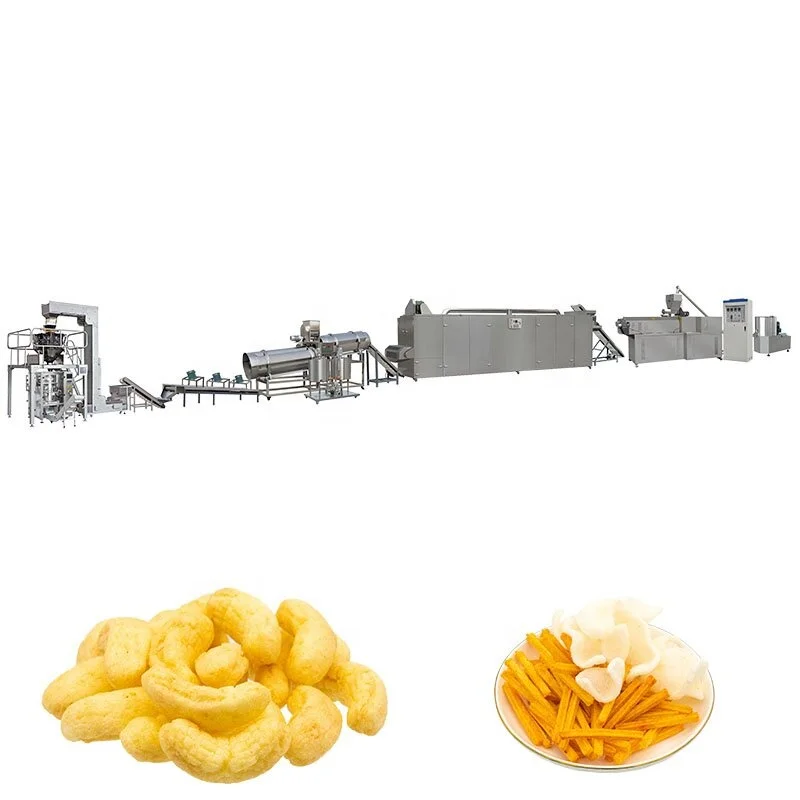
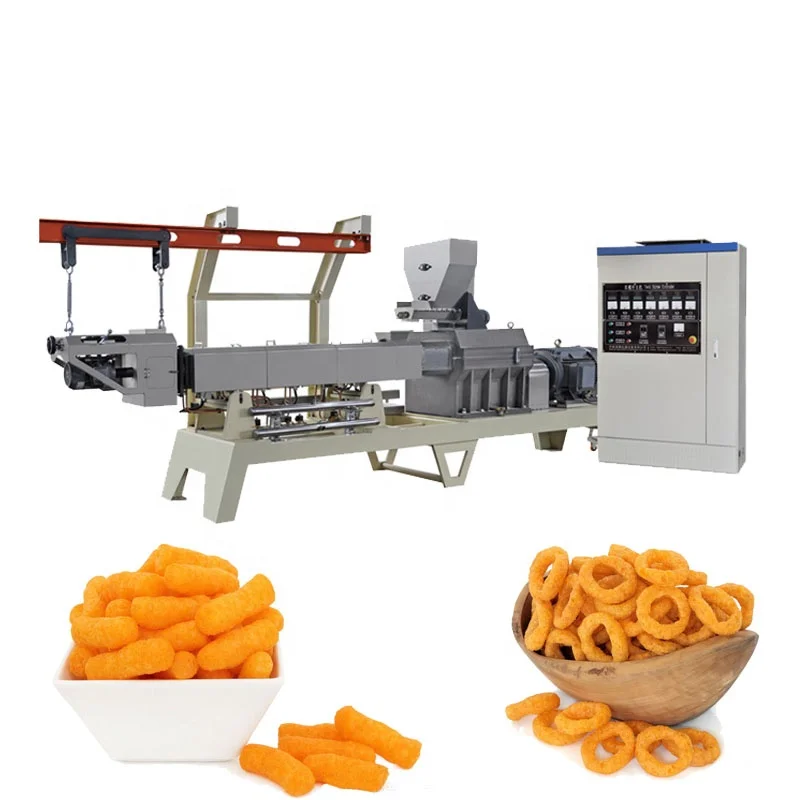
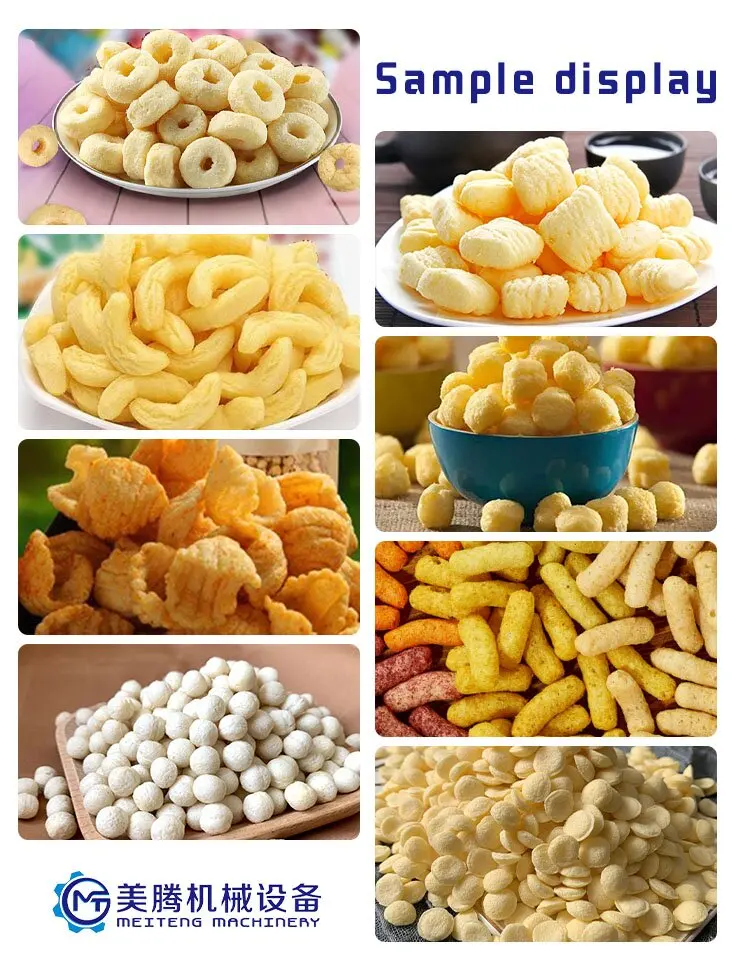
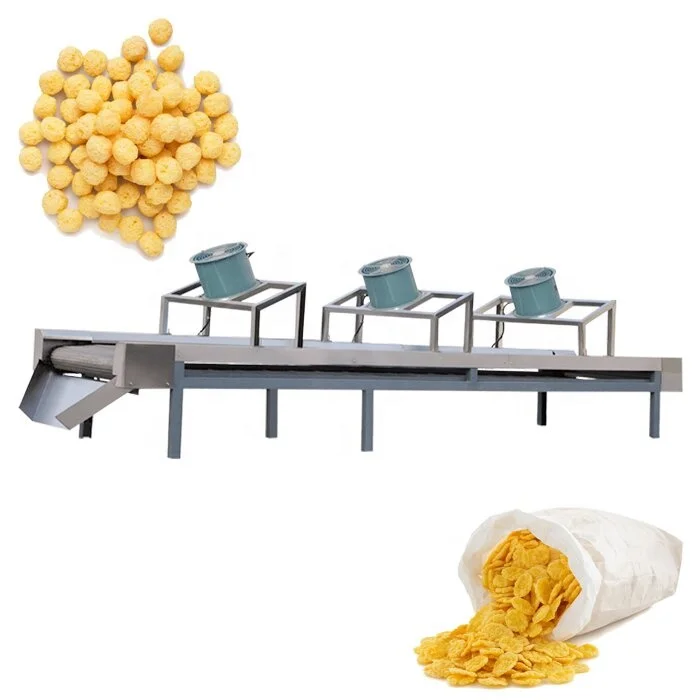
MT65 Fully Automatic Puff Snack Processing Line, Twin-Screw Extruder, 84kW Installed Power — engineered as a complete turnkey project from batching through extrusion to seasoning and packing. Every station is throughput-matched under a single layout, with screw configuration and die design specified to your raw material and target product density. In-house trial runs on your recipe verify output before shipment, supported by full line documentation and on-site commissioning.
- Models: MT65 / MT70 / MT85 / MT75 / MT95
- Twin-screw extrusion with food-grade stainless steel contact parts
- Line stations: mixer, extruder, shaping machine, oven, seasoning drum, cooler
Description
Throughput-Matched Engineering — Every station on the MT65 puff snack processing line is calculated against the same production target so that mixer, extruder, roaster, and seasoning drum perform as one coordinated system instead of a patchwork of mismatched capacities.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 |
| Product Type | Fully Automatic Puff Snack Processing Line |
| Model Options | MT65 / MT70 / MT85 / MT75 / MT95 |
| Screw Type | Twin-screw |
| Installed Power (MT65) | 84 kW |
| Power Consumption (MT65) | 59 kW |
| Output Capacity (MT65) | 120–150 kg/h (basis not stated in source — confirm raw material type, moisture content, product format) |
| Overall Dimensions (MT65) | 21000 × 1200 × 2200 mm |
| Extruder Main Motor Power | 30 kW |
| Extruder Actual Power | 30–35 kW |
| Extruder Installed Power | 45.87 kW |
| Extruder Dimensions | 2800 × 830 × 1875 mm |
| Powder Mixer Tank Volume | 150 kg |
| Powder Mixer Power | 4 kW |
| Powder Mixer Rotary Speed | 385 rpm |
| Powder Mixer Mixing Time | 10 min per batch |
| Powder Mixer Dimensions | 1000 × 630 × 1100 mm |
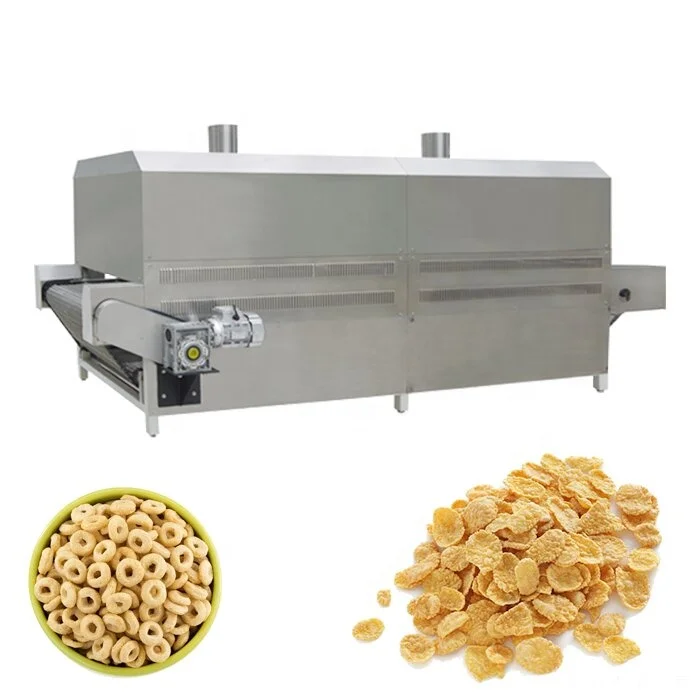
| High-Temperature Roaster Effective Belt Length | 3.5 m |
| Roaster Far Infrared Heater Power | 3.9 kW × 24 |
| Roaster Belt Motor Power | 0.55 kW |
| Roaster Dimensions | 4500 × 1500 × 1600 mm |
| Screw Conveyor Power | 0.75 kW |
| Screw Conveyor Dimensions | 2500 × 500 × 2000 mm |
| Line Stations | Powder mixer, screw conveyor, twin-screw extruder, sandwich machine, shaping machine, elevator, high-temperature roaster, seasoning machine, cooler |
| Construction Material | Stainless steel (food-grade contact parts) |
| Automation Level | Fully automatic (batching through seasoning to finished product) |
| Warranty | 1 year complete warranty, lifetime maintenance service |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Puffed and extruded snack production | Corn grits, rice flour, wheat flour blends at controlled moisture |
| Core-filled / sandwich snack production | Grain-based outer shell with cream, chocolate, or fruit paste filling |
| Puffed rice cracker production | Rice flour with starch modifiers for controlled expansion |
| Wheat roast snack production | Whole or cracked wheat processed through high-temperature roasting |
| Nutritious breakfast cereal products | Multi-grain formulations with vitamin or mineral fortification |
Why "Nominal Capacity" Can Derail a Puff Snack Processing Line Turnkey Project
A capacity number without raw material context is a guess, not a guarantee.
I remember an early project where a puff snack line was specified to a Southeast Asian buyer at a nominal hourly output. The screw configuration followed a generic build. When the customer ran their own recipe — higher oil content in the flour blend — the extrudate came out sticky, failed to hold shape, and the entire batch was scrapped. The extruder was not at fault; the configuration was. That failure started with a capacity quote that never referenced the buyer’s actual material [NEED_CITE: importance of raw material validation in extrusion line specification]. A puff snack processing line turnkey project only delivers when throughput is verified against your specific recipe, moisture content, and target density.
Screw Configuration and Die Design Set the Texture
In twin-screw extrusion, the screw element arrangement and die geometry determine shear intensity, residence time, and expansion ratio. A generic screw build may handle standard corn grits but fail on high-fat or high-fiber formulations. The MT65 line specifies screw configuration and die design to the buyer’s raw material and target product, so expansion and density match what the market expects. This is why a puff snack processing line turnkey project must begin with recipe analysis, not a catalogue selection.
Every Station Must Keep Pace with the Extruder
A common failure in assembled lines is the extruder producing faster than the downstream roaster can dry or the seasoning drum can coat. On this line, the powder mixer cycles 150 kg batches in roughly 10 minutes, the high-temperature roaster provides a 3.5-meter effective belt for adequate drying residence, and the seasoning drum volume is calculated against the same hourly target. If any station is undersized, the extruder must be throttled back — and the quoted output becomes theoretical [NEED_CITE: throughput matching across extrusion line stations].
Reading the Specs That Actually Matter
The 30 kW main motor on the MT65 twin-screw extruder provides the torque needed for viscous snack doughs, while actual running power of 30–35 kW reflects real energy draw under load. The roaster uses 24 far-infrared heating elements at 3.9 kW each — that thermal capacity determines how quickly surface moisture is driven off without over-drying the product core. The 385 rpm mixer speed with a 10-minute batch cycle ensures uniform hydration before material enters the extruder, which is critical because uneven moisture distribution causes inconsistent expansion at the die. Food-grade stainless steel contact surfaces meet hygiene standards required for snack production and simplify washdown between recipe changeovers.
The Cost of Skipping a Trial Run
When a line ships without a trial run on the buyer’s actual raw material, product development starts after installation — on the factory floor, with production deadlines pressing. Screw combinations are swapped, die plates are re-ordered, and drying curves are adjusted through trial and error. Each iteration burns raw material and delays revenue [NEED_CITE: cost of post-installation commissioning delays in food extrusion projects]. The hidden cost is not the wasted material; it is the lost market window while the line sits idle during recipe tuning.
Why Source This Line from a Single Supplier
Complete lines from batching to packing under one supplier mean throughput is matched across every station rather than assembled from separate vendors who each guarantee only their own machine. Screw configuration and die design are specified to the buyer’s raw material and target product rather than copied from a generic template. An in-house testing workshop allows trial runs on your actual material before the line ships, so product development begins before installation. Twin-screw expertise across puffed snacks, core-filled products, and breakfast cereals means the process knowledge is built into the line from the start. Pre-sales consultation through on-site installation, commissioning, and ongoing maintenance keeps one team accountable from inquiry through production.
Documentation & Verification
- Line layout and capacity calculation confirming throughput matching across every station
- Screw and die configuration record matched to your specific recipe and target product density
- Trial run report on your raw material generated in the testing workshop before dispatch
- Electrical schematic with voltage, frequency, and control language confirmed before production
- Factory test record documenting actual run conditions and output measurements
- Operation and maintenance manual with wear parts list specific to your configuration
Installation, Commissioning & Support
- Foundation and floor space planning based on the 21000 × 1200 × 2200 mm MT65 line footprint
- Dedicated electrical circuit sized for 84 kW installed power with confirmed local voltage and frequency
- On-site assembly with station-by-station alignment verification across the full line length
- First-run commissioning with parameter adjustment for your raw material and target snack format
- Operator training covering screw element changes, die swaps, and roaster temperature profiling
- Wear parts list including screws and dies with recommended replacement intervals
What We Need to Start Your Line Configuration
To move from inquiry to a validated line layout, share your raw material type and typical moisture content, your target snack format and density, and the hourly output you need to meet market commitments. We also need your local voltage, frequency, and preferred control language so the electrical package is confirmed before production begins. If you have existing upstream or downstream equipment that must integrate, include those specifications as well.
Frequently Asked Questions
Q: How is the output capacity verified, and what conditions does it depend on?
A: Output capacity depends on raw material type, moisture content, and the specific die configuration used. We verify throughput by running your actual material in our in-house testing workshop before shipment. The trial produces a documented report showing real output under your recipe conditions, so the number you receive is not a generic catalogue figure but a measured result tied to your product.
Q: How do you ensure the dryer and seasoning stations match extruder throughput?
A: Every station is calculated against the same production target during the layout phase. The roaster belt length, heater capacity, and seasoning drum volume are all sized so that none becomes a bottleneck when the twin-screw extruder runs at full output. The line layout document shows the throughput calculation for each station, giving you visibility into how capacity is balanced.
Q: Can I send my raw material for a trial run before the line ships?
A: Yes. Our testing workshop runs your actual raw material through the extruder with the specified screw and die configuration before the line leaves the factory. You receive a trial run report showing product texture, density, and expansion results. This means product development happens before installation, not on your factory floor under production pressure.
Q: What voltage, frequency, and control language options are confirmed before production?
A: We confirm your local voltage, frequency, and preferred control language during the specification stage, before production begins. The electrical schematic is prepared with these parameters and included in your documentation package. This avoids commissioning delays caused by mismatched electrical supply or operators unable to read the control interface.
Q: What does on-site installation and operator training include?
A: Our team handles station-by-station assembly, mechanical alignment, electrical connection, and first-run commissioning with your raw material. Operator training covers daily operation, screw and die changes, roaster temperature adjustment, and routine maintenance. A wear parts list with replacement intervals is provided so you can plan your first spare parts order before the initial components reach end of life.
Related products
-

Puffed Snack Food Machine Snack Food Machine Puffed Snack Machine
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Hot Sale Corn Snack Extruder Puffed Snacks Production Machine Corn Puffs Making Machine
¥20,000.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puffed Snacks Seasoning Flavor Machine Twin Screw Corn Puffing Food Making Extruder Equipment
¥8,355.00 Select options This product has multiple variants. The options may be chosen on the product page -

Corn Puff Processing Line with Mixer Fryer Baking Oven Automatic High Productivity Grain Products Snack Making Machine
¥8,300.00 Select options This product has multiple variants. The options may be chosen on the product page