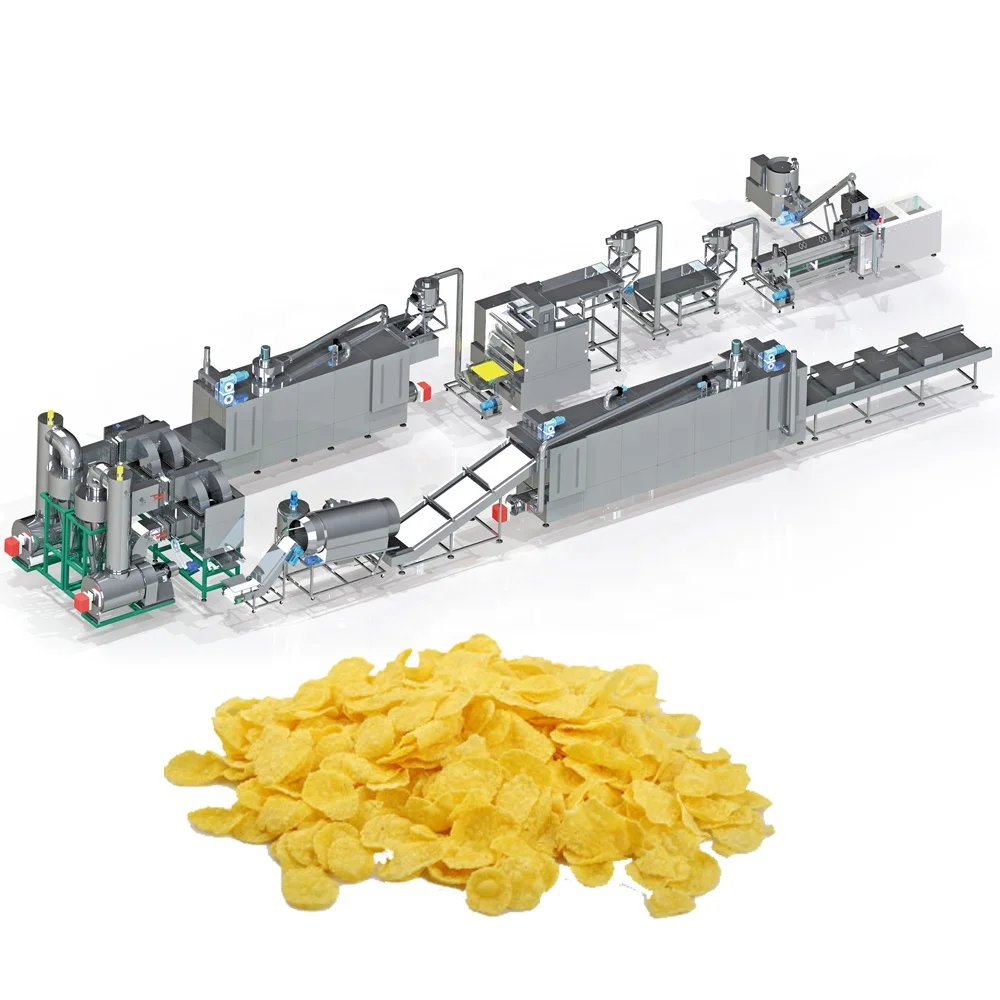
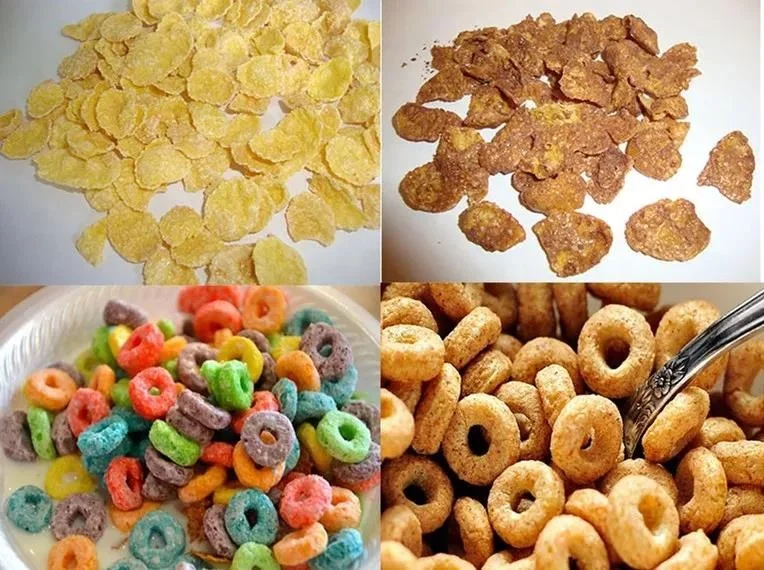
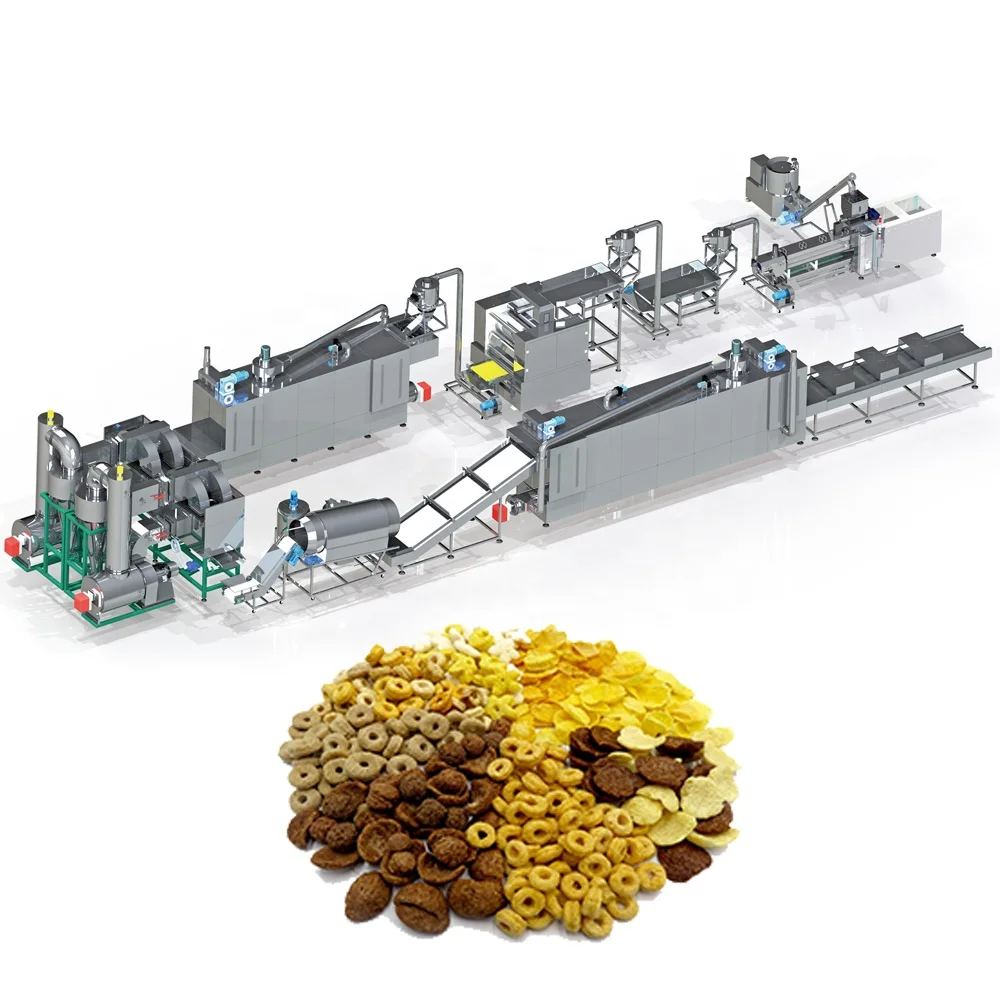
Breakfast Cereal Production Line, Twin-Screw Extruder, PLC & MCC Control — complete turnkey layout from batching through extrusion, drying, roasting and packing for corn flake and multi-grain cereal manufacturing.
- Screw configuration and die design matched to raw material and target flake density, with multi-station throughput calculated to eliminate bottlenecks across mixer, extruder, cooler and dryer
- Energy options include electric, gas, diesel or steam heating, configurable to local utility infrastructure
- Trial run on your actual corn, rice or multi-grain formulation performed in our in-house testing workshop before shipment
Description
Throughput-Matched Line Design — every station from mixer to packing is calculated against your target cereal output, so no single extruder or dryer dictates the line’s rhythm.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Breakfast Cereal and Corn Flake Extrusion Processing Line |
| Extruder Type | Double screw (twin-screw) extruder |
| Construction Material | Food grade stainless steel 201/304 |
| Voltage & Frequency | Three phases 380V/50Hz, Single phase 220V/50Hz (customizable to local voltage) |
| Control System | PLC and MCC control with Delixi or Delta inverter |
| Motor | Siemens (made in China) or China top brand |
| Power Consumption | Approx. 100 kW (electric heating); approx. 50–60 kW (gas or diesel heating) (basis not stated in source — confirm line configuration and capacity) |
| Energy Options | Electricity, gas, diesel, or steam |
| Line Stations | Mixer → Extruder → Vibrate cooler machine → Roasting machine → Packing machine |
| Raw Material Form | Powder (flour) or grits |
| Compatible Raw Materials | Corn, rice, millets, wheat, oat, barley, buckwheat, brown rice |
| Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (via die/mould adjustment) |
| Output Capacity | Confirmed per raw material and target product (basis to be confirmed) |
| Dryer Type | Multi-layer dryer (length and layer configurable to product) |
| Flavoring System | Semi-automatic or automatic; supports sugar, oil, and powder seasoning |
| Assembly State | Complete line (turnkey) |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn flake and coco pops breakfast cereal production | Corn flour, corn grits, rice flour |
| Multi-grain flake and extruded cereal manufacturing | Wheat, oat, barley, buckwheat, brown rice, millet blends |
| Fortified breakfast cereal with added nutrients | Vitamin, protein, and mineral-enriched cereal bases |
| Artificial and fortified rice production | Rice flour, broken rice, starch blends |
| Puffed and extruded snack food manufacturing | Corn, rice, and multi-grain formulations in varied shapes |
What "Nominal Capacity" Leaves Out of a Breakfast Cereal Production Line Turnkey Quote
A line rated on paper often stalls on your actual corn or multi-grain recipe — verification must happen before the machines are crated.
I once watched a corn flake project in Germany where the extruder ran at spec but the downstream dryer could not keep pace. Three days of idle throughput sat on the factory floor because nobody matched station capacities before loading the containers. When buyers evaluate a breakfast cereal production line turnkey proposal, the extruder capacity figure is only meaningful if the mixer feed rate, cooler throughput, multi-layer dryer residence time, and roasting oven output are all calculated to the same target. [NEED_CITE: throughput balancing across extrusion line stations]
Matching Every Station to the Extruder’s Rhythm
A twin-screw extruder can push product faster than a dryer can remove moisture if the two are specified in isolation. This breakfast cereal production line turnkey configuration pairs each station — from batching mixer through vibrating cooler to multi-layer dryer and roasting machine — against a single output target calculated for the buyer’s raw material and flake density requirement.
Trial Runs Before the Machines Leave the Factory
Rather than starting product development after installation, raw material trials run in the in-house testing workshop on the buyer’s exact corn grits, rice flour, or multi-grain blend. The trial confirms screw configuration, die selection, moisture profile, and expansion behavior before the line is finalized for shipment. [NEED_CITE: pre-shipment extrusion trial methodology]
Reading the Specifications That Actually Matter
Twin-screw extrusion offers wider material tolerance than single-screw designs, handling everything from fine corn flour to coarse oat and buckwheat grits without surging. The PLC and MCC control system with Delta or Delixi inverters maintains consistent screw speed and barrel temperature across production runs, which directly governs starch gelatinisation and flake density. Multi-layer dryer length and layer count are configurable — a longer dryer with more layers increases residence time for denser multi-grain flakes that need extended moisture removal. Die and mould adjustment across ball, ring, stick, star, and fruit loop shapes lets a single extruder serve multiple product formats without changing the upstream mixer or downstream cooler.
The Hidden Cost of Mismatched Line Components
When an extruder is supplied without matching dryer or coating capacity, the bottleneck surfaces during the first production week. Buyers end up running the extruder at reduced output to match the slowest downstream station, leaving paid capacity unused on the floor. Voltage, frequency, and control language confirmed late in the process delay commissioning by weeks, while generic screw and die configurations copied from unrelated builds produce flakes with the wrong crunch or density for the target market. [NEED_CITE: commissioning delays from unconfirmed electrical specifications]
Why Source This Line Here
Screw configuration and die design are specified to the buyer’s raw material and target flake shape rather than copied from a generic build, ensuring correct expansion and density from the first run. Every station — mixer, extruder, vibrating cooler, dryer, roaster, flavouring system, and packing — is throughput-matched under one supplier, eliminating the integration gaps that appear when stations come from separate vendors. An in-house testing workshop runs trials on the buyer’s actual corn, rice, or multi-grain formulation before shipment. Pre-sales consultation covers line layout and utility planning, followed by on-site installation, commissioning, and operator training. Documentation includes the electrical schematic with voltage and control language confirmed for the destination country before production starts.
Documentation & Verification
- Line layout and capacity calculation showing throughput matched at every station
- Trial run report on buyer’s raw material performed before shipment
- Screw and die configuration record specific to target flake shape and density
- Electrical schematic with voltage, frequency, and control language confirmed for destination
- CE declaration of conformity and ISO certificate included with shipment
- Operation and maintenance manual with wear parts list for ongoing production
Installation, Commissioning & Support
- Foundation and floor space planned to the confirmed line layout and station footprint
- Power supply sized to the approx. 100 kW electric or 50–60 kW gas heating configuration
- PLC and MCC control panels wired and tested before dispatch, with language set to local requirements
- First-run commissioning includes screw speed, barrel temperature, and dryer residence time tuning on buyer’s recipe
- Operator training covers die changes across product shapes and daily cleaning of food-grade stainless steel contact surfaces
- Wear parts list with screw and die replacement schedule provided at handover
Preparing Your Line Inquiry
To configure a breakfast cereal production line turnkey proposal that fits your factory, share your raw material type and recipe formulation, target output per hour, and the specific flake or cereal shape you intend to produce. Confirm your local voltage, frequency, and preferred control panel language. If you have existing upstream batching or downstream packing equipment, note the interface requirements so the new line integrates without gaps.
Frequently Asked Questions
Q: How is line capacity verified on my specific raw material before the line is built?
A: Your exact corn, rice, or multi-grain formulation runs in the in-house testing workshop before any machine ships. The trial confirms screw speed, barrel temperature profile, and die selection against your target flake density and shape. A trial run report documents the results and forms part of the final line specification.
Q: How are extruder, dryer, and roaster capacities matched across the line?
A: Each station is calculated against a single throughput target based on your raw material moisture content and target product density. The multi-layer dryer length and layer count are configured so residence time matches extruder output, and the roasting oven is sized to the same rate, preventing bottlenecks.
Q: What voltage and control language options are confirmed before production?
A: The electrical schematic is confirmed with your local voltage and frequency — three-phase 380V/50Hz, single-phase 220V/50Hz, or a custom configuration — before production begins. PLC and MCC control panel language is set to match your operators’ requirements, and the documentation package reflects all confirmed specifications.
Q: How are screw and die configurations selected for different cereal shapes?
A: The twin-screw configuration and die design are chosen based on your raw material behavior and target product shape — whether ball, ring, stick, or fruit loop. The testing workshop trial validates expansion, texture, and density on your recipe before the screw and die set is finalized for the production line.
Related products
-

Puffed Snack Food Machine Snack Food Machine Puffed Snack Machine
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Corn Crisps Extruder Production Machine for Maize Chips and Corn Sticks New Condition
¥8,000.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puff Corn Snacks Food Line Puffed Rice Ball Production Making Equipment Machines
¥10,565.00 Select options This product has multiple variants. The options may be chosen on the product page -

Corn Puff Processing Line with Mixer Fryer Baking Oven Automatic High Productivity Grain Products Snack Making Machine
¥8,300.00 Select options This product has multiple variants. The options may be chosen on the product page