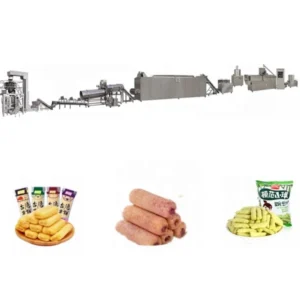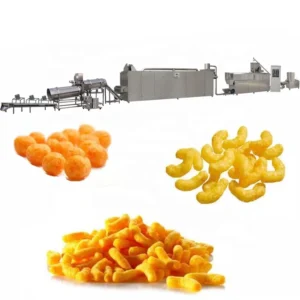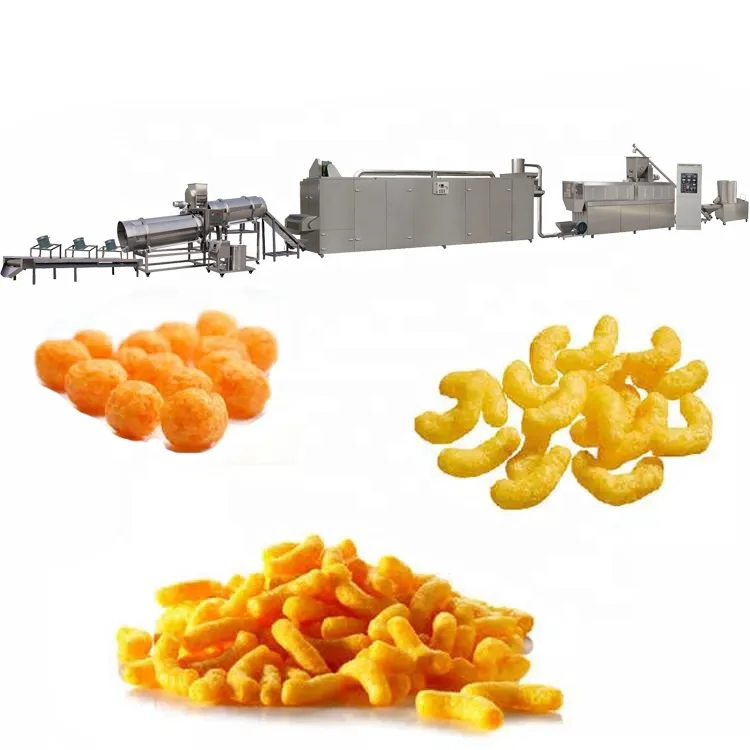
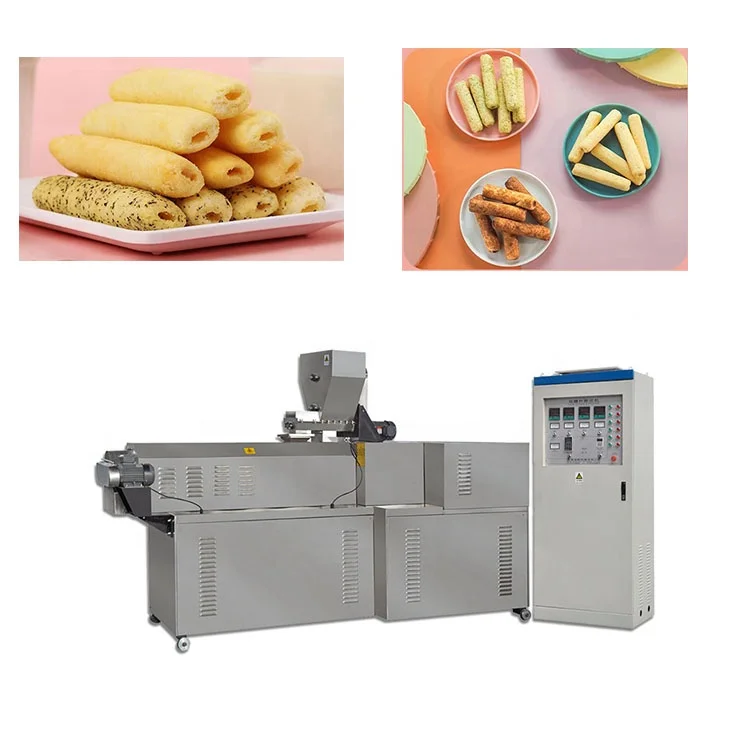
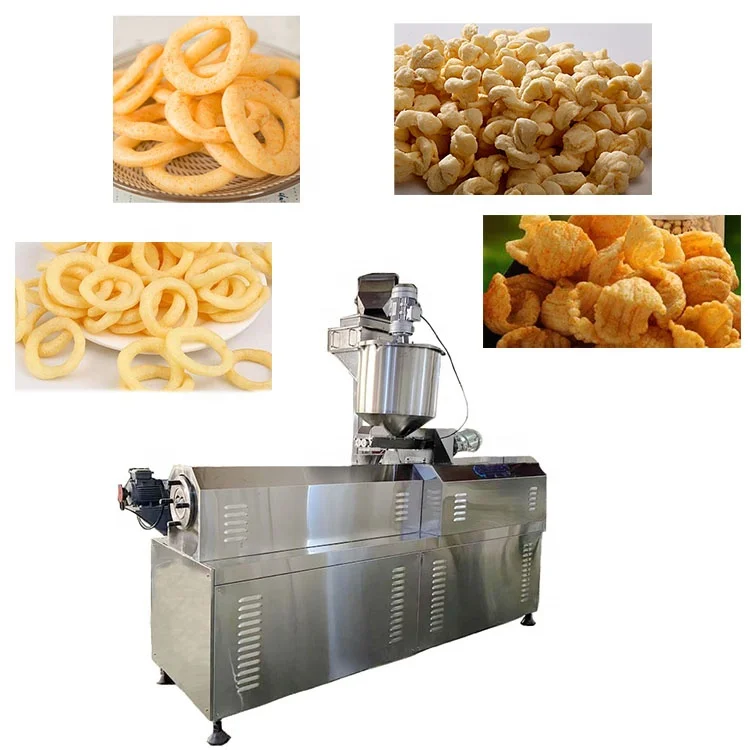
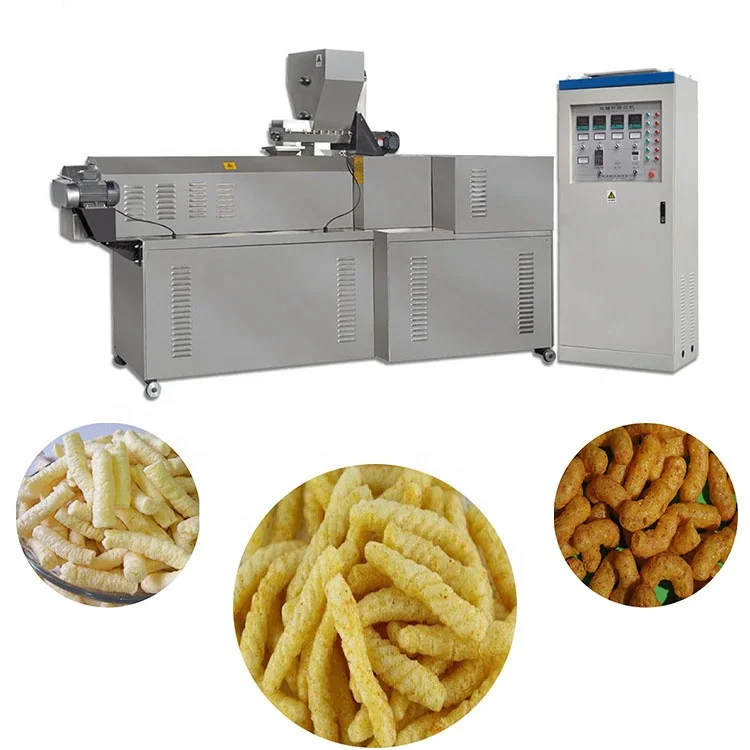
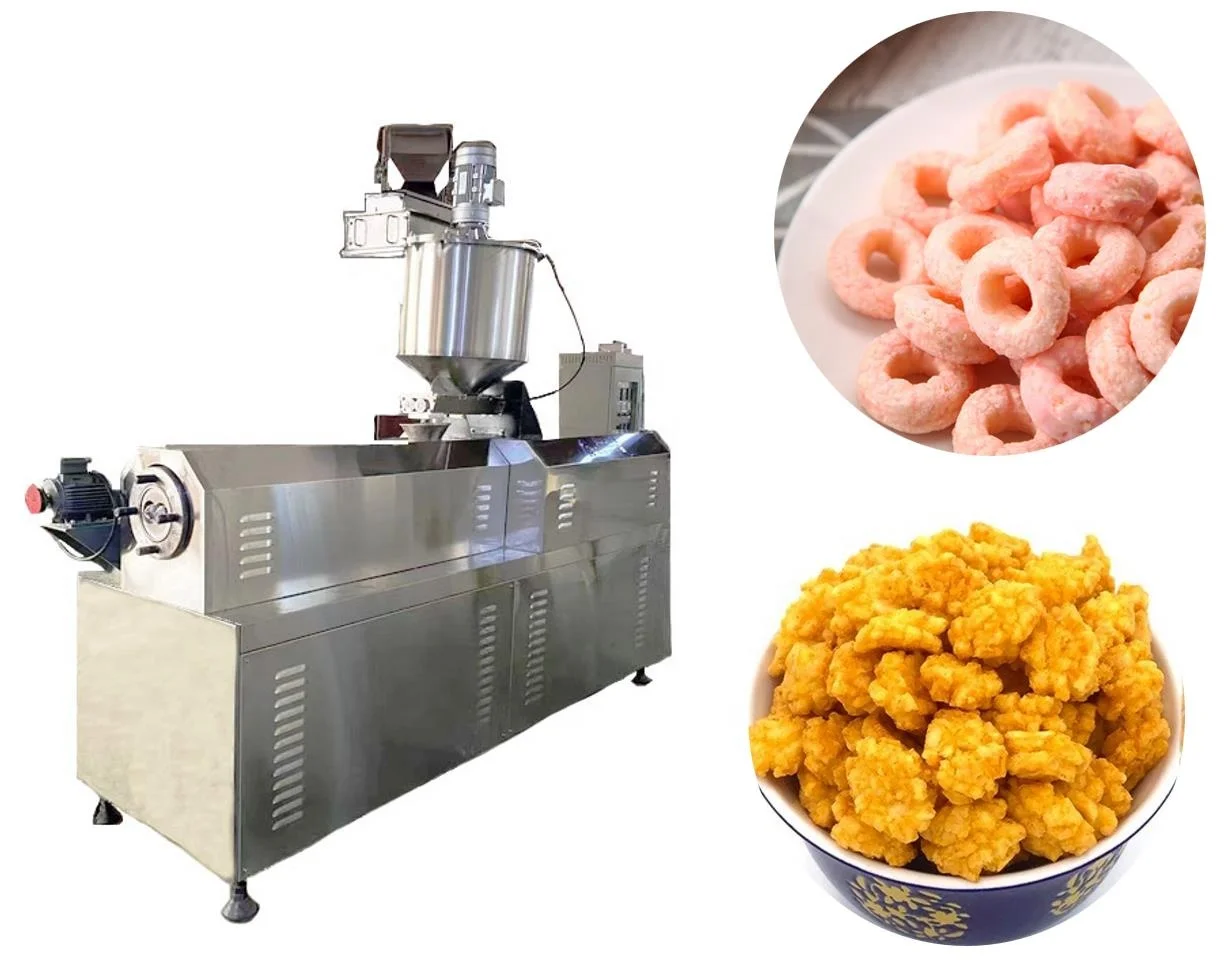
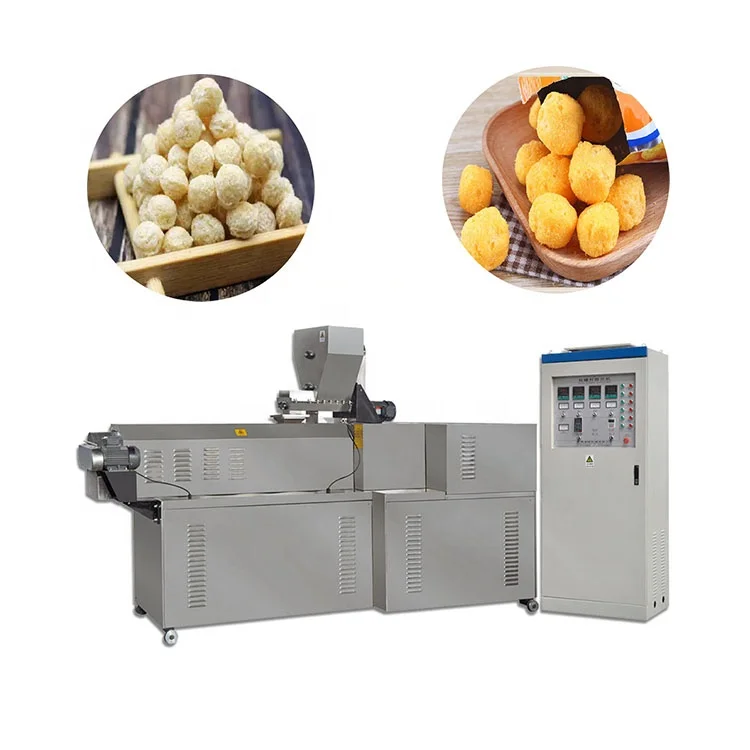
Puffed Snack Extrusion Production Line, Twin Screw, 380V/50Hz, Food-Grade SS 201/304 — engineered as a turnkey project from batching through extrusion to packing. Every station is throughput-matched, with screw and die configuration specified to your cereal formulation and target snack density. Flexible energy options (electric/gas/diesel/steam) align with your factory utilities. Backed by in-house trial runs on your raw material, matched throughput across all nodes, and single-supplier accountability for layout through commissioning.
- Line sequence: Mixer → Extruder → Vibrate Cooler → Roasting → Packing
- Product formats: corn puffs, cheese balls, core-filled bars, cereal bars, sheet snacks
- CE & ISO certified, semi-automatic and automatic options available
Description
Station-by-station throughput matching — Every node from batching through packing is calculated against your cereal formulation, so no single machine bottlenecks the puffed snack extrusion production line turnkey project.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Puffed Snack Extrusion Production Line |
| Screw Type | Twin Screw (double screw extruder) |
| Raw Materials | Rice, millet, brown rice, buckwheat, corn, cereals |
| Line Stations | Mixer → Extruder → Vibrate Cooler Machine → Roasting Machine → Packing Machine |
| Product Formats | Core-filling snacks, chocolate filled bar, cream filled pillow, rice cake, cereal bar, sheet snacks, cheese balls, corn puffs |
| Energy Options | Electricity / Gas / Diesel / Steam |
| Voltage & Frequency | Three phases 380V/50Hz; Single phase 220V/50Hz (customizable to local voltage) |
| Power (Electricity) | About 100 kW (basis to be confirmed) |
| Power (Gas/Diesel) | About 50–60 kW (basis to be confirmed) |
| Material | Food grade stainless steel 201/304 |
| Automation Level | Semi-automatic and automatic options available |
| Control System | PLC/MCC (basis to be confirmed) |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Direct-expanded corn puffs and cheese balls | Corn grits, rice flour, corn starch blends |
| Core-filled snack bars and cream pillows | Cereal dough with chocolate, cream, or fruit paste filling |
| Sheet snacks and cereal bars | Millet, brown rice, buckwheat, multigrain formulations |
| Nutritional cereal and artificial rice | Fortified cereal blends, grain-based nutritional powders |
| Puffed rice cakes | Rice, brown rice, mixed grain formulations |
Why "Rated Capacity" Fails on Real Cereal Formulations
A puffed snack extrusion production line turnkey quotation that only lists extruder output misses the throughput reality across every downstream station.
I have seen lines arrive on site and stall because the roasting oven could not keep pace with the extruder when the buyer switched to a higher-moisture corn blend. The mixer batch cycle, extruder screw speed, cooler residence time, and packing speed all have to move at the same rate for the puffed snack extrusion production line turnkey project to run continuously. [NEED_CITE: throughput balancing principles in continuous food extrusion lines] When one station is undersized relative to the next, you end up with product backing up on conveyors, moisture levels drifting out of spec, and operators manually throttling the extruder to match a slower dryer — defeating the purpose of buying a complete line.
Mapping the Full Station Sequence Before the First Bolt Is Set
A puffed snack extrusion production line turnkey project begins with a layout that accounts for utility drop points, material flow direction, and operator access at every station. The mixer feeds the twin-screw extruder at a controlled rate, then product moves through the vibrate cooler to stabilize moisture before entering the roasting machine. Each transition point — conveyor length, transfer chute angle, buffer bin volume — is sized so that the line runs as one continuous system rather than a collection of standalone machines waiting on each other.
Matching Utility Planning to What Your Factory Actually Has
Energy source selection is one of the earliest decisions on a turnkey project, and it has to be resolved before production drawings begin. This line supports electricity, gas, diesel, and steam, which means the roasting and drying stages can be configured around whatever utility infrastructure your facility already provides. Voltage and frequency must be confirmed for the destination country — a 380V/50Hz machine dropped into a 440V/60Hz plant without transformer planning will delay commissioning by weeks. [NEED_CITE: voltage and frequency standards by export market] The control system language is locked in at the same stage so operators are not deciphering unfamiliar interface text on day one.
Reading the Specs That Matter for Extrusion Behavior
The twin-screw configuration gives this line a wider processing window than single-screw alternatives when working with varied cereal inputs like buckwheat, millet, or brown rice blends. Screw configuration and die design are specified together — the screw profile controls shear and residence time inside the barrel, while the die geometry determines product shape, expansion ratio, and final density. Moisture content in the raw material directly affects expansion at the die face: higher moisture generally lowers expansion and increases density, which is why a trial run on the buyer’s actual cereal blend is necessary before locking in the screw combination. The food-grade stainless steel 201/304 contact surfaces meet hygiene requirements for direct food contact and withstand the repeated washdown cycles that snack production demands. Barrel temperature profiling across multiple heating zones lets operators fine-tune gelatinisation and expansion independently, giving consistent product texture across long production runs.
What Happens When Throughput Matching Is Skipped
A line assembled from separate vendors often arrives with an extruder rated for a certain output but a cooler or roaster that was never checked against that figure. Product piles up between stations, moisture content drifts outside the range the roaster can handle, and the packing station sits idle waiting for upstream bottlenecks to clear. [NEED_CITE: consequences of unmatched throughput in multi-station food processing lines] On one project I supported, the drying section was sized for a different product density than what the extruder actually produced, and it took four days of on-site screw and die reconfiguration to bring the line back to a stable running state.
Why Sourcing the Complete Line from One Supplier Changes the Project
Every station from batching to packing comes from a single source, so throughput calculations are cross-checked across the entire sequence rather than left to individual machine vendors. Screw configuration and die design are matched to your specific cereal formulation and target snack format before the line ships, not guessed from a generic build. The in-house testing workshop runs your actual raw material through the extruder and downstream equipment, producing a trial report that documents product density, expansion, and throughput before you take delivery. Pre-sales engineering covers layout design, utility planning, and phased installation scheduling, then the same team handles on-site commissioning and operator training. CE and ISO documentation is provided as part of the project package, meeting import requirements for markets that enforce machinery directives. [NEED_CITE: CE machinery directive requirements for industrial food processing equipment]
Documentation & Verification
- Line layout and capacity calculation showing throughput at every station for your cereal blend
- Trial run report on your actual raw material conducted in the testing workshop before shipment
- Screw and die configuration record matched to your target snack density and format
- Electrical schematic with confirmed voltage, frequency, and control language for your country
- CE declaration of conformity and ISO certificate included with customs documentation
Installation, Commissioning & Support
- Foundation and floor space plan based on the full station sequence from mixer through packing machine
- Dedicated electrical circuit sized for the confirmed power draw at your local voltage and frequency
- Phased assembly schedule coordinating extruder, cooler, roaster, and packing station installation
- First-run commissioning with screw and die adjustment on your cereal formulation to reach target density
- Operator training covering control system interface, product changeover, and daily washdown procedures
- Wear parts list for screws, dies, and barrel liners with recommended replacement intervals
What to Prepare Before Requesting a Quotation
To build a line configuration that holds capacity on your specific product, we need your target snack format, the cereal or grain blend you plan to run, and the moisture range of your incoming raw material. Share your available utility specs — voltage, frequency, and whether you want electric, gas, diesel, or steam heating — along with the control language your operators require. If you have existing upstream or downstream equipment that this line must integrate with, include those machine specs and conveyor heights.
Frequently Asked Questions
Q: How is line capacity verified across every station, not just at the extruder?
A: Throughput is calculated for the mixer batch cycle, extruder output, cooler residence time, roaster pass-through rate, and packing speed based on your cereal formulation. The in-house trial run validates these figures on your actual raw material before the line ships, so the capacity you see in the proposal reflects real running conditions.
Q: What voltage, frequency, and control language are confirmed before production begins?
A: Your facility’s electrical supply — voltage, phase, and frequency — is confirmed at the quotation stage so motors, heaters, and control panels are built to match. The PLC or MCC interface language is set at the same time, ensuring operators can navigate the system from commissioning day forward.
Q: How is screw and die configuration determined for my cereal blend and target snack?
A: The screw profile and die geometry are selected based on your raw material composition, moisture content, and the expansion ratio your target product requires. A trial run in the testing workshop validates the configuration, and adjustments are made before shipment if the output density or texture does not match your specification.
Q: What does the in-house trial run cover before shipment?
A: The trial run processes your supplied raw material through the extruder and relevant downstream stations, measuring product density, expansion, moisture, and throughput. A written report with these results is provided before dispatch, and buyers can witness the test or review findings remotely.
Q: What is the installation and operator training process on site?
A: Engineers follow a phased installation schedule, assembling each station in sequence and connecting utilities according to the pre-confirmed layout. Commissioning includes running your cereal formulation through the full line, adjusting screw and die settings, and training operators on the control system, product changeover, and maintenance routines.
Related products
-

Máquina Automática de Snacks de Comida Inflada Máquina Eléctrica para Hacer Snacks de Maíz Puff Nueva Condición Producción de Snacks Puff Sabrosos
¥7,550.00 Select options This product has multiple variants. The options may be chosen on the product page -

Máquina Extrusora de Snacks de Maíz Pequeña de Puffs de Maíz de Doble Tornillo
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page -

Línea de producción de equipos industriales para el procesamiento de cereales de desayuno Crispy Maize Chocos Corn Flakes totalmente automática
¥1,000.00 Select options This product has multiple variants. The options may be chosen on the product page -

Máquina para hacer copos de maíz de cereal de desayuno crujiente y inflado.
¥1,000.00 Select options This product has multiple variants. The options may be chosen on the product page