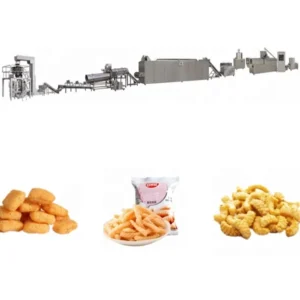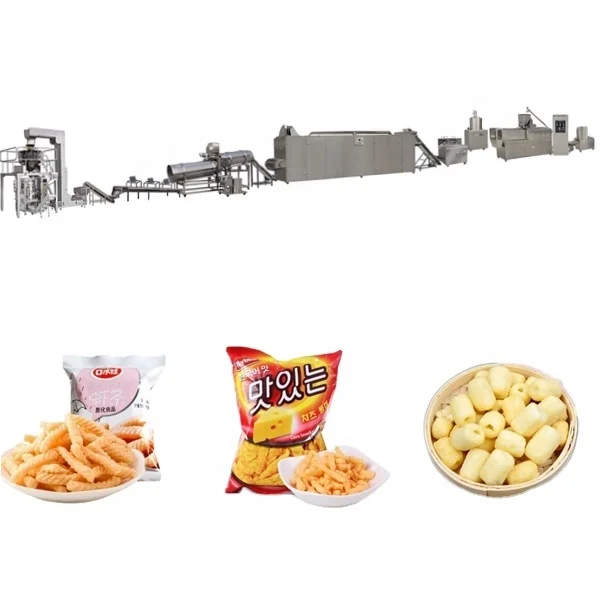
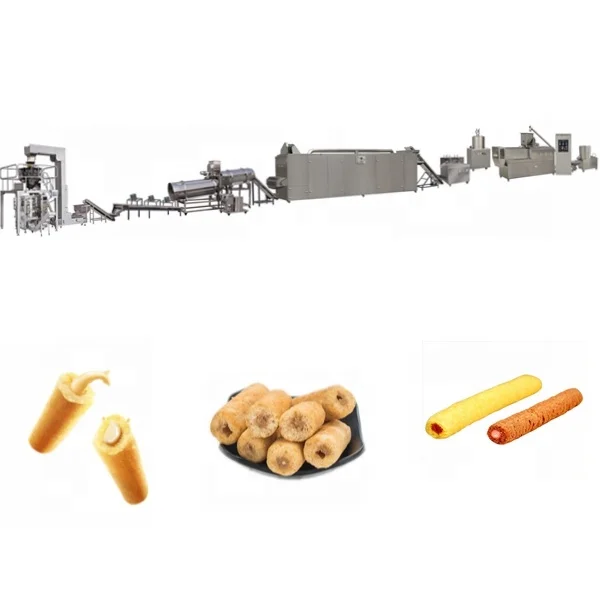
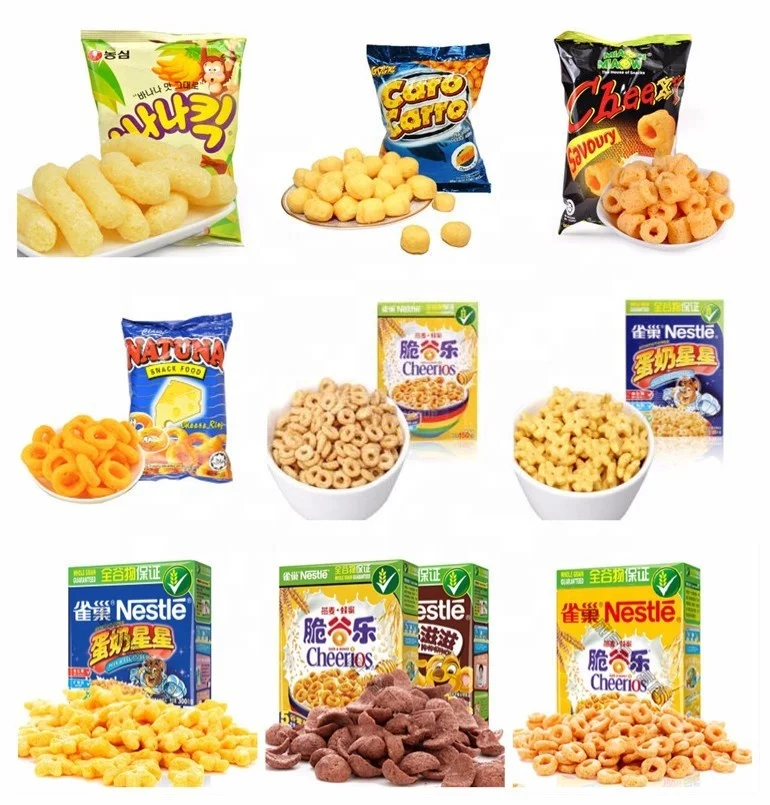
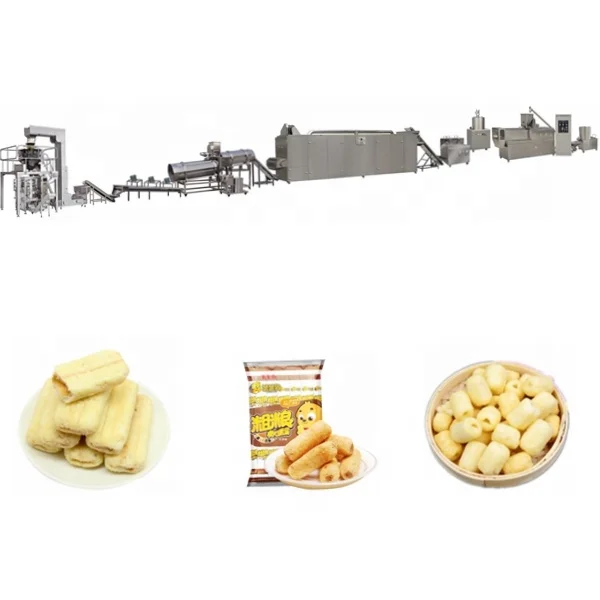
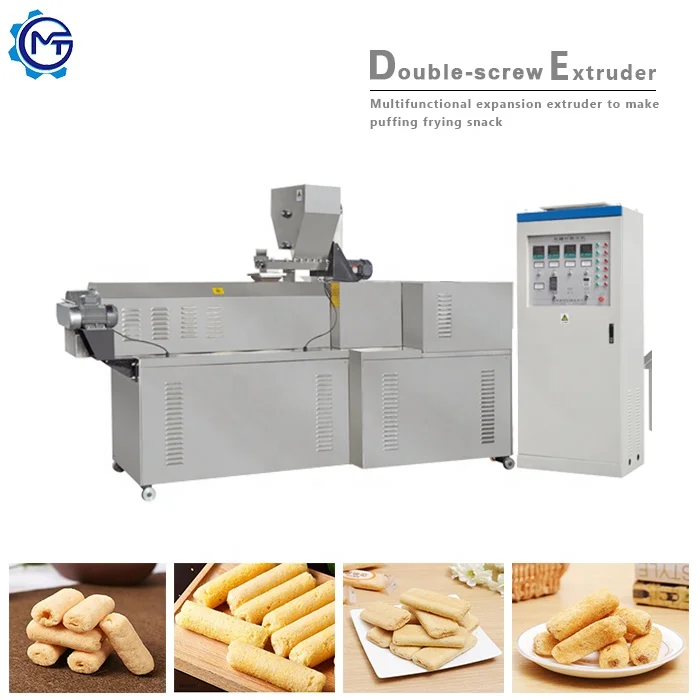
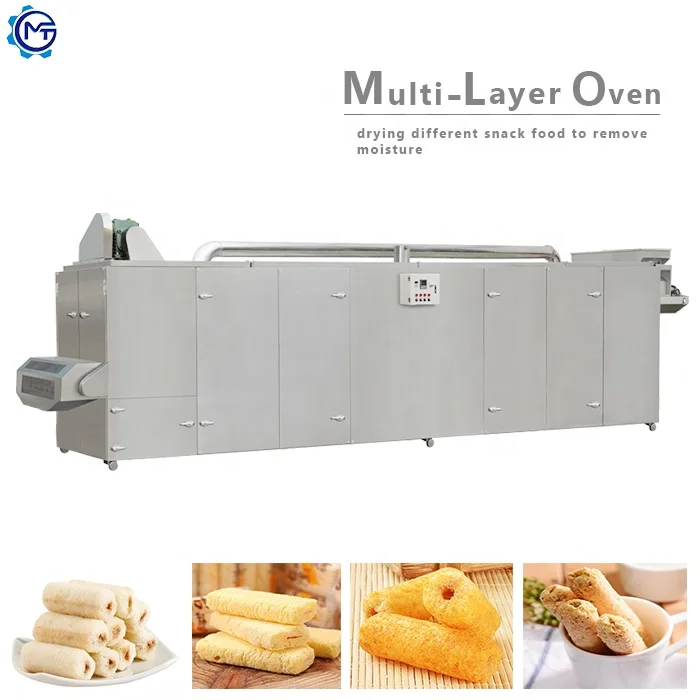
MT70 / MT85 / MT75 Twin Screw Extrusion Corn Puffs Snack Production Line, 100-500 kg/h Output, Gas/Electric Dryer — configured for cereal-based puffed snacks including cheese balls, fruit loops, and shaped corn puffs from corn, rice, wheat, or oat flour.
- Screw configuration and die design specified to your raw material formula and target puff density, with shapes changed via die swaps on one extruder platform
- Dryer and coating drum throughput matched to extruder output so no bottleneck forms between stations, verified in line layout before build
Trial runs on your actual raw material are conducted in our in-house testing workshop, with a full report provided before shipment.
Description
Line Throughput Matched End-to-End — every station from the batching hopper to the packing conveyor is sized against your target output so the extruder never waits on the dryer.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extrusion Corn Puffs Snack Production Line |
| Models Available | MT70, MT85, MT75 |
| Screw Type | Twin-screw with automatic lubrication and cooling |
| Raw Materials | Corn flour, rice flour, wheat flour, oat flour, barley flour |
| Final Product Shapes | Cheese ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (via die change) |
| Installed Power (MT70) | 130 kW |
| Power Consumption (MT70) | 95 kW |
| Output Capacity (MT70) | 100–120 kg/h (basis not stated in source — confirm raw material type and moisture content) |
| Overall Dimensions (MT70) | 21 × 1.5 × 2.2 m |
| Installed Power (MT85) | 180 kW |
| Power Consumption (MT85) | 120 kW |
| Output Capacity (MT85) | 200–300 kg/h (basis not stated in source — confirm raw material type and moisture content) |
| Overall Dimensions (MT85) | 25 × 1.5 × 2.2 m |
| Installed Power (MT75) | 220 kW |
| Power Consumption (MT75) | 130 kW |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material type and moisture content) |
| Overall Dimensions (MT75) | 28 × 1.5 × 2.2 m |
| Dryer Heating Source | Gas or electric |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Production Procedure | Mixing → Extruding → Roasting/Drying → Sugar-coating/Flavoring → Cooling → Packing |
| Voltage & Frequency | Configurable to local supply requirements |
| Assembly State | Complete line, shipped as integrated stations |
| Standards | CE certified, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn puffs and maize chips | Corn flour, corn grits at controlled moisture |
| Cheese balls and extruded snack balls | Corn and rice flour blends with cheese coating |
| Fruit loops and ring-shaped cereal snacks | Multi-grain flour mixes with sugar glaze |
| Stick and tube format puffed snacks | Wheat, oat, or barley flour with savory seasoning |
| Star, flower, and novelty shapes | Cereal-based dough via interchangeable die plates |
Why Extruder Output Alone Tells You Nothing About Line Speed
A corn puffs extrusion production line turnkey is only as fast as its slowest downstream station.
When a buyer sees a capacity number quoted for the extruder, it rarely accounts for what happens after the die. I once worked on a maize snack project where the extruder could push product at a steady rate, but the dryer was sized for a lower throughput. The high-moisture puffs piled up at the dryer infeed, and the operator had to throttle the extruder back to prevent spoilage. The whole corn puffs extrusion production line turnkey ended up running well below its nameplate figure [NEED_CITE: throughput bottleneck between extruder and dryer in snack lines]. The real question is never how much the extruder can produce in isolation — it is whether the dryer, coating drum, cooler, and packing station can all keep pace with that same volume on your specific raw material.
How Throughput Is Balanced Across Every Station
Every station on this corn puffs extrusion production line turnkey is calculated against the extruder output before any machine enters production. The dryer length and belt speed are matched to the moisture removal load coming off the extruder, and the coating drum diameter is sized so that tumbling time does not create a queue. If the extruder model is changed during project scoping, the downstream equipment is recalculated rather than carried over from a standard template. This is the difference between a line that runs at its design rate and one that constantly stalls at the transition points.
Raw Material Variables That Shift the Real Output
The capacity range listed for each model assumes a reference material, but actual throughput shifts with flour type, particle size, and incoming moisture content. Rice flour behaves differently from corn grits inside the barrel — it gelatinizes at a lower temperature and can change expansion rate, which in turn affects drying time. Before we quote a final line speed, we run your actual raw material through the extruder in our testing workshop and measure the real exit moisture, puff density, and drying curve. That data becomes the basis for sizing the dryer and coating stations [NEED_CITE: effect of cereal flour type on extrusion expansion and drying load].
What the Screw Configuration and Die Choice Mean for Your Product
The twin-screw design allows the screw elements to be rearranged along the shaft to control shear intensity, residence time, and pressure profile inside the barrel. A higher-shear configuration works well for dense cheese balls that need a tight internal structure, while a gentler profile suits hollow tube shapes where wall thickness must stay uniform. The die plate determines the cross-section of the extrudate, and each shape — ring, star, flower, fruit loop — requires its own die and cutting setup. Because the screw elements are modular, the same MT-series extruder can be reconfigured for a different snack format if your product range expands, without replacing the entire barrel assembly.
Reading the Power and Dimension Figures
Installed power on the MT75 reaches 220 kW, which covers the main drive motor, barrel heating zones, and cutter assembly. Actual power consumption sits lower — 130 kW for the MT75 — because heating elements cycle on and off once thermal equilibrium is reached. The overall line length of 28 m for the MT75 configuration includes the extruder, dryer, coating section, and cooler in sequence. When planning your factory floor, add clearance at both ends for raw material staging and finished product palletizing. Gas-heated dryers reduce electrical load substantially but require a dedicated gas supply line and exhaust ducting, while electric dryers simplify utility planning at the cost of higher amperage demand [NEED_CITE: gas versus electric dryer utility requirements in food extrusion plants].
The Cost of Skipping a Line-Level Throughput Check
When stations are sourced from separate vendors, each supplier quotes equipment rated for a nominal capacity — but those ratings are rarely based on the same material assumptions. The extruder vendor tests on corn, the dryer vendor tests on a generic load, and nobody is responsible for the handoff. The result is a line where material accumulates between stations, product quality drifts as residence time in the dryer varies, and operators spend their shifts adjusting speeds manually. Correcting this after installation means replacing or reconfiguring equipment that was never wrong on its own — it was just never matched to the rest of the line [NEED_CITE: consequences of unmatched station capacity in multi-vendor snack lines].
Why Sourcing the Entire Line from One Supplier Changes the Equation
Every station on this corn puffs extrusion production line turnkey is designed, built, and tested under one project scope, so throughput matching is an engineering calculation rather than a negotiation between vendors. The screw configuration and die design are specified to your raw material formula and target puff density before production begins. Our in-house testing workshop runs your actual flour blend and documents the expansion ratio, exit moisture, and drying profile before the line ships. Electrical schematics are drawn to your factory voltage and frequency, and control panel labels match your operator language. The line layout includes utility drop points and floor clearance so your contractor can prepare the site before the equipment arrives.
Documentation & Verification
- Line layout drawing showing station spacing, throughput balance, and utility drop locations for your factory
- Screw element arrangement and die plate drawing matched to your target snack shape and density
- Trial run report on your raw material with measured expansion, moisture, and drying data
- Electrical schematic reflecting your confirmed voltage, frequency, and control language
- CE declaration of conformity and ISO certificate included with shipping documents
- Wear parts list identifying screw sections, die plates, and cutter blades with replacement intervals
Installation, Commissioning & Support
- Foundation load plan based on the 28 m line length and MT75 weight distribution across stations
- Dedicated electrical circuit sized to the 220 kW installed power with voltage confirmed before wiring
- Stations shipped in labeled modules for sequential assembly matching the floor layout drawing
- First-run parameter setting covering barrel temperature zones, screw speed, and dryer belt speed
- Operator training on die changeover, screw element inspection, and coating drum adjustment
- Spare screw segments and die plates shipped with initial order to cover first replacement cycle
Preparing Your Inquiry
To scope the right configuration, share your primary flour type and any secondary ingredients, your target daily output in kilograms, and the snack shapes you plan to run. Include your factory voltage and frequency, the available floor space with ceiling height, and whether gas or electric drying is preferred. If you have existing upstream or downstream equipment that the new line must connect to, send the interface details so the layout can account for those tie-in points.
Frequently Asked Questions
Q: How is line throughput verified against my raw material?
A: We run your actual flour blend in our testing workshop before shipment. The trial measures extrudate expansion, exit moisture, and drying curve. Those results are used to confirm or adjust the dryer length and coating drum size so every station matches the real output, not just the extruder nameplate figure.
Q: Can the line layout fit my existing factory footprint?
A: The layout is drawn around your floor dimensions and ceiling height after we receive a site plan. Utility drop points for power, water, gas, and exhaust are positioned to match your building infrastructure. If space is tight, we can adjust station spacing or suggest an L-shaped configuration.
Q: How are the dryer and coating drum sized to avoid bottlenecks?
A: Dryer belt length and speed are calculated from the moisture removal load leaving the extruder. The coating drum diameter and tumbling time are set so that coated product exits at the same rate the cooler receives it. If the extruder model changes during scoping, downstream equipment is resized accordingly.
Q: What does on-site installation and commissioning include?
A: Our technician oversees station assembly in sequence per the layout drawing, connects utilities to pre-confirmed voltage and frequency, sets initial barrel temperatures and screw speeds, and runs the line through a full production cycle. Operator training covers die changeover, routine screw inspection, and daily cleaning procedures.
Related products
-

Línea de procesamiento de puff de maíz con mezclador, freidora, horno de horneado, máquina automática de alta productividad para la fabricación de productos de grano y snacks.
¥8,300.00 Select options This product has multiple variants. The options may be chosen on the product page -
Línea de Procesamiento Automático de Copos de Maíz Maquinaria para Fabricación de Cereales para el Desayuno y Snacks de Coco Pops
¥7,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Línea de procesamiento de bocadillos inflados completamente automática
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Máquina Extrusora de Snacks de Maíz Pequeña de Puffs de Maíz de Doble Tornillo
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page