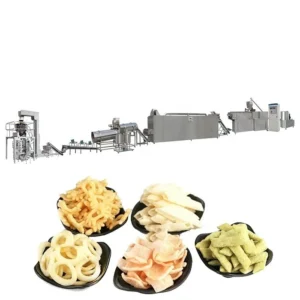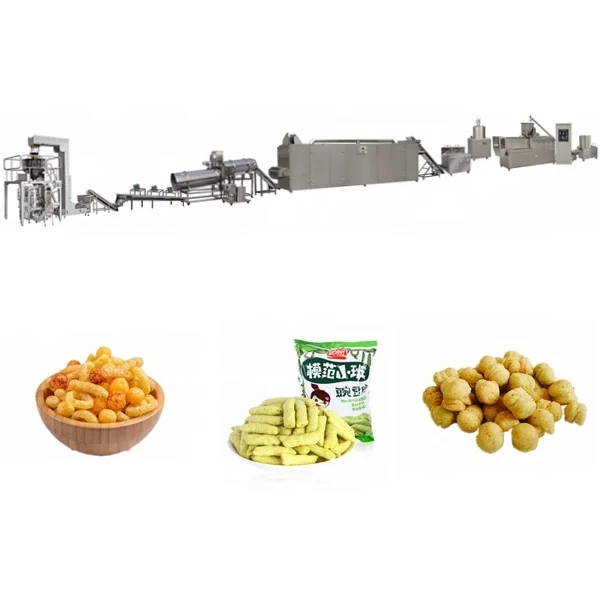
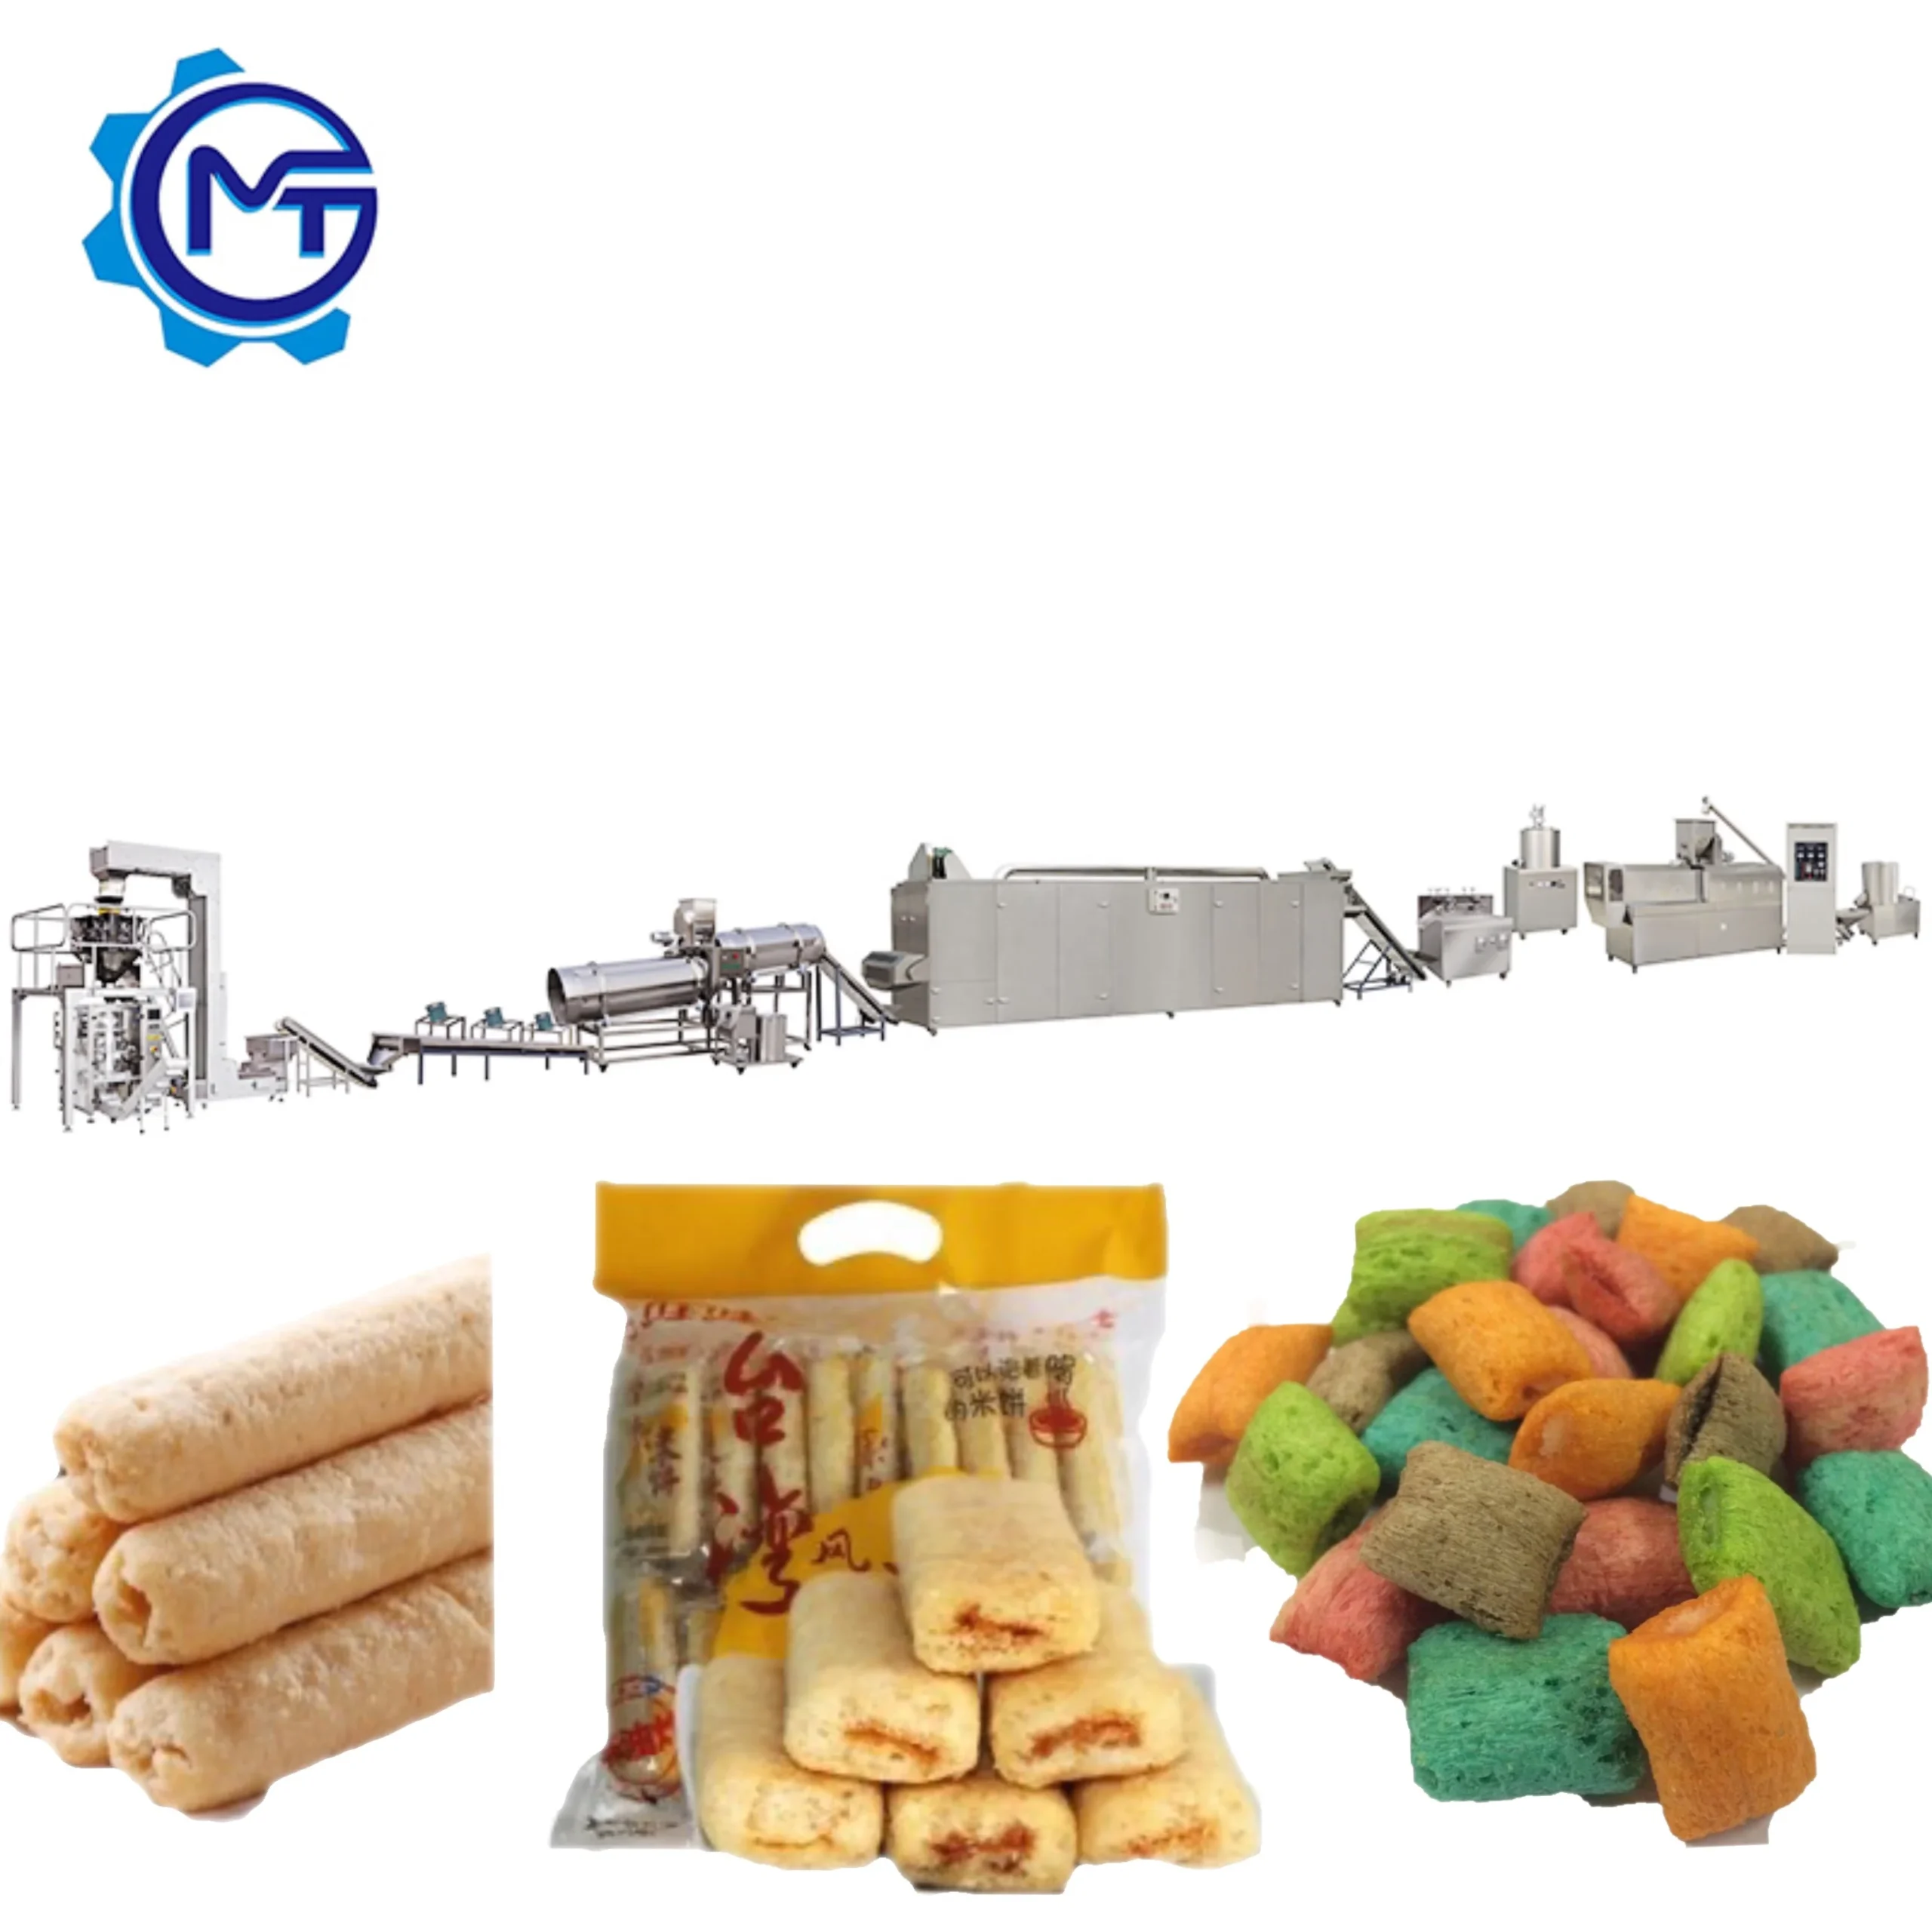
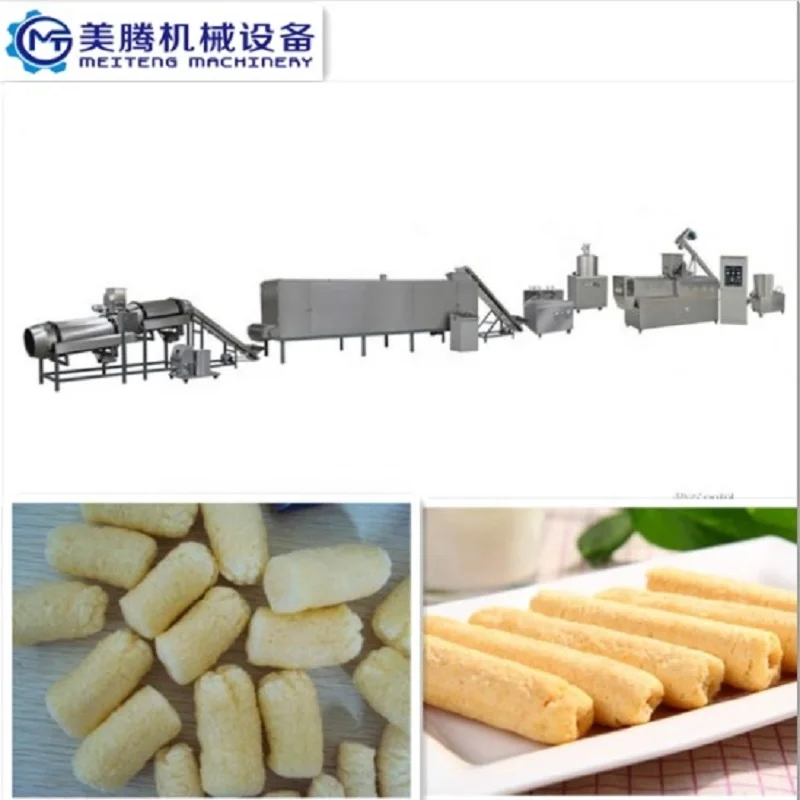
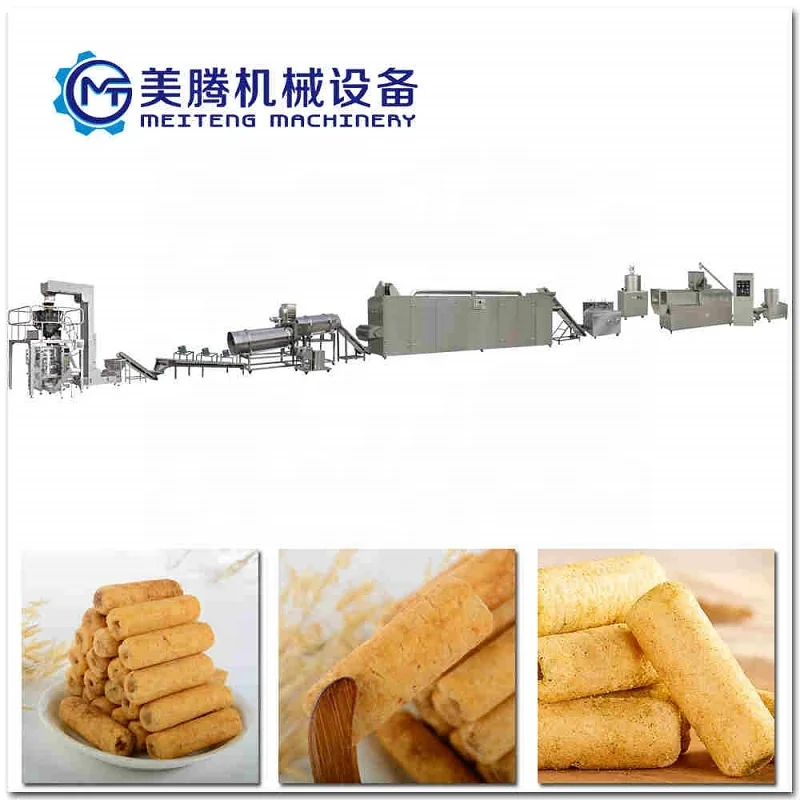
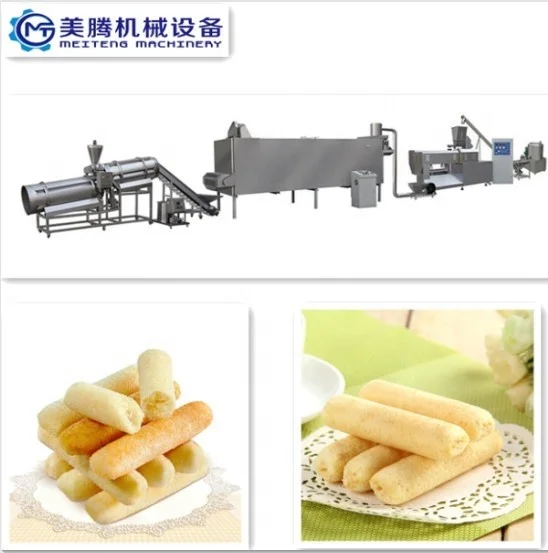
MT70 / MT85 / MT75 Twin Screw Extruder Plant, 130-220 kW, Gas/Electric Dryer — engineered as a complete turnkey line from batching through extrusion, drying, coating, cooling and packing for puffed snack production.
- Screw configuration and die design matched to your raw material and target puff shape, controlling expansion and density from corn, rice, wheat or oat flour
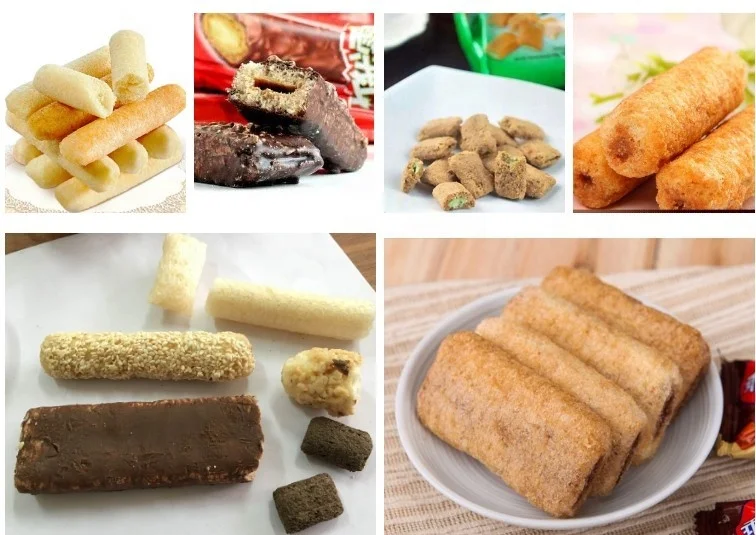
- Multiple die options produce cheese balls, tubes, sticks, rings, fruit loops and more on one line
- Automatic lubricating and cooling system supports continuous running
Layout, throughput matching and trial runs on your actual recipe are completed in-house before shipment, with voltage and control language confirmed to your local supply.
Description
Integrated Throughput Engineering — every station from batching to packing is sized against the extruder output so no single drum or dryer chokes the line during continuous runs.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Twin Screw Extruder Plant for Puffed Snacks |
| Screw Type | Twin-screw |
| Installed Power | MT70: 130 kW; MT85: 180 kW; MT75: 220 kW |
| Power Consumption | MT70: 95 kW; MT85: 120 kW; MT75: 130 kW |
| Output Capacity | MT70: 100–120 kg/hr (basis not stated in source); MT85: 200–300 kg/hr (basis not stated in source); MT75: 300–500 kg/hr (basis not stated in source) |
| Overall Dimensions (L×W×H) | MT70: 21 × 1.5 × 2.2 m; MT85: 25 × 1.5 × 2.2 m; MT75: 28 × 1.5 × 2.2 m |
| Raw Materials | Corn, rice, wheat, oat, barley flour |
| Final Product Shapes | Cheese ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (die-dependent) |
| Dryer Heating Source | Gas or Electric |
| Coating System | Double tumble drum with sugar melting, elevator, spraying nozzle |
| Screw Construction | Wear-resistant alloy, special technology |
| Lubrication | Automatic lubricating and cooling function |
| Assembly State | Complete turnkey line |
| Voltage & Frequency | Customized to local supply |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn puff and cheese ball production | Corn flour, rice flour with fat and sugar coating |
| Extruded tube and stick snacks | Wheat, oat, and barley flour blends |
| Fruit loop and ring cereal snacks | Multi-grain flour mixtures with sugar glazing |
| Star, wheel, and heart novelty shapes | Corn and rice flour with die changes |
| Snack plant capacity expansion | Scaling from pilot to mid-volume output on existing recipes |
What "Rated Capacity" Leaves Out About Snack Extrusion Lines
A capacity number without a raw material basis is a guess, not a guarantee.
I have stood on factory floors in Southeast Asia watching a brand-new extrusion line stall because the supplier quoted output on standard corn grits while the buyer was running a high-fat recipe. The screw torque alarm tripped within minutes, and the die output broke into uneven pulses [NEED_CITE: twin screw extrusion behavior on high-fat raw material blends]. The entire line sat idle while a new screw configuration was assembled and shipped. Every twin screw extruder turnkey production line we ship runs a trial on the buyer’s actual flour blend before crating, so throughput figures are tied to real material behavior, not catalog assumptions.
Matching Extrusion Parameters to Snack Recipes
The screw profile, barrel temperature zones, and die geometry together determine whether corn flour expands into a light cheese ball or a dense tube. A twin screw extruder turnkey production line configured for one shape may not transition cleanly to another without documented screw element changes. We specify the screw combination and die bore against the buyer’s target product density and shape before production begins.
Throughput Balance Across Every Station
An extruder pushing product at full rate means little if the downstream dryer cannot remove moisture fast enough or the coating drum cannot tumble the full volume. Each station on this line is sized so the drying residence time, coating drum volume, and cooling conveyor length all track the extruder output without creating a bottleneck [NEED_CITE: extrusion line throughput matching between dryer and coating stations]. The result is a continuous flow from mixer to pack-off rather than a series of surge hoppers and idle conveyors.
Reading the Power and Dimension Data
Installed power on the MT75 reaches 220 kW while running consumption sits at 130 kW — the gap reflects startup surge and peak torque events when cold dough first enters the barrel. Buyers planning electrical infrastructure should size transformers and cable runs around installed power, not average draw. The line footprint stretches to 28 meters for the MT75 configuration; factory planners need clear linear space plus service access on both sides of the extruder barrel for screw pull-back during die changes. Automatic lubrication and cooling keep the screw shaft bearings stable through long shifts, reducing the chance of thermal seizure that would otherwise force an unplanned stop.
The Cost of Skipping Pre-Shipment Validation
When a line arrives at the buyer’s site and fails to hold output on the local flour, the corrective path involves flying in a process engineer, machining new screw elements, and running trial batches while the factory waits. Downtime during commissioning often costs more in lost production than the trial run itself [NEED_CITE: commissioning delays in food extrusion projects due to untested raw material compatibility]. A factory test on the buyer’s recipe before dispatch compresses on-site commissioning to mechanical alignment and operator familiarization rather than process troubleshooting.
Why Source This Line From a Single Project Supplier
Supplying the mixer, extruder, dryer, coating system, cooler, and packing conveyor under one scope means throughput calculations are cross-checked at every hand-off point. Screw and die configurations are recorded against the buyer’s raw material certificate, not pulled from a generic build sheet. Our in-house testing workshop runs the buyer’s flour before the line ships, producing a documented trial report. Electrical schematics confirm voltage, frequency, and control language before the panel is wired, preventing the rewiring delays that stall commissioning on arrival. The line carries CE and ISO certification, meeting import requirements across regulated markets.
Documentation & Verification
- Line layout drawing matched to buyer factory footprint and utility tie-in points
- Screw and die configuration record tied to buyer raw material certificate
- Trial run report on buyer flour blend documenting output and product density
- Electrical schematic with voltage, frequency, and control language confirmed pre-build
- Operation and maintenance manual with wear parts list for screws and dies
Installation, Commissioning & Support
- Foundation plan accounts for MT75 line length of 28 m and extruder vibration isolation points
- Electrical supply sized to installed power of up to 220 kW with dedicated circuit breaker
- Extruder barrel and screws ship assembled; dryer sections bolt on site
- Commissioning includes first-run parameter logging on buyer raw material
- Operator training covers die changeover, screw pull-back, and lubrication system checks
- Spare screw elements and die plates listed with part numbers for reorder
What to Include in Your Inquiry
Share your flour blend composition, target snack shape, and daily output goal so we can match the extruder model and downstream sizing. Confirm your local voltage and frequency along with the control panel language your operators read. If you have existing upstream mixers or downstream packing machines, note their throughput so the line integrates without over- or under-sizing any station.
Frequently Asked Questions
Q: How is line capacity verified on my actual raw material before shipment?
A: We run your flour blend through the extruder in our testing workshop, logging output rate, product density, and screw torque. The trial report ships with the line so you can compare commissioning results against the pre-dispatch baseline.
Q: How do you match throughput between extruder, dryer, and coating drum?
A: Each station is sized during layout engineering so dryer residence time and coating drum volume track the extruder output rate, preventing material backlog or idle time at any single point.
Q: What voltage and control language options are confirmed before production?
A: We collect your site voltage, frequency, and preferred control language during the specification stage and reflect them on the electrical schematic before the panel is wired, avoiding rewiring on arrival.
Q: What does the turnkey scope cover from design through startup?
A: Scope includes factory layout drawing, equipment supply from mixer to pack-off, pre-shipment trial, on-site installation supervision, commissioning with parameter logging, and operator training on die changes and maintenance routines.
Q: How are screw and die configurations chosen for different snack shapes?
A: Screw element arrangement and die bore are selected based on your flour composition and target shape density. Changing from a cheese ball to a tube, for example, involves a documented swap of die plate and screw profile section.
Related products
-

Crunchy Puffed Snack Breakfast Cereal Corn Flakes Making Machine
¥1,000.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic High Productivity Puffed Corn Snacks Extruder Production Equipment New Condition Puff Snack Food Making Machine
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Hot Sale Corn Snack Extruder Puffed Snacks Production Machine Corn Puffs Making Machine
¥20,000.00 Select options This product has multiple variants. The options may be chosen on the product page -

New Stainless Steel Automatic Snack Food Machinery Extruder Puffed Corn Maize Puff Processing Line for Food Industry High
¥12,350.00 Select options This product has multiple variants. The options may be chosen on the product page