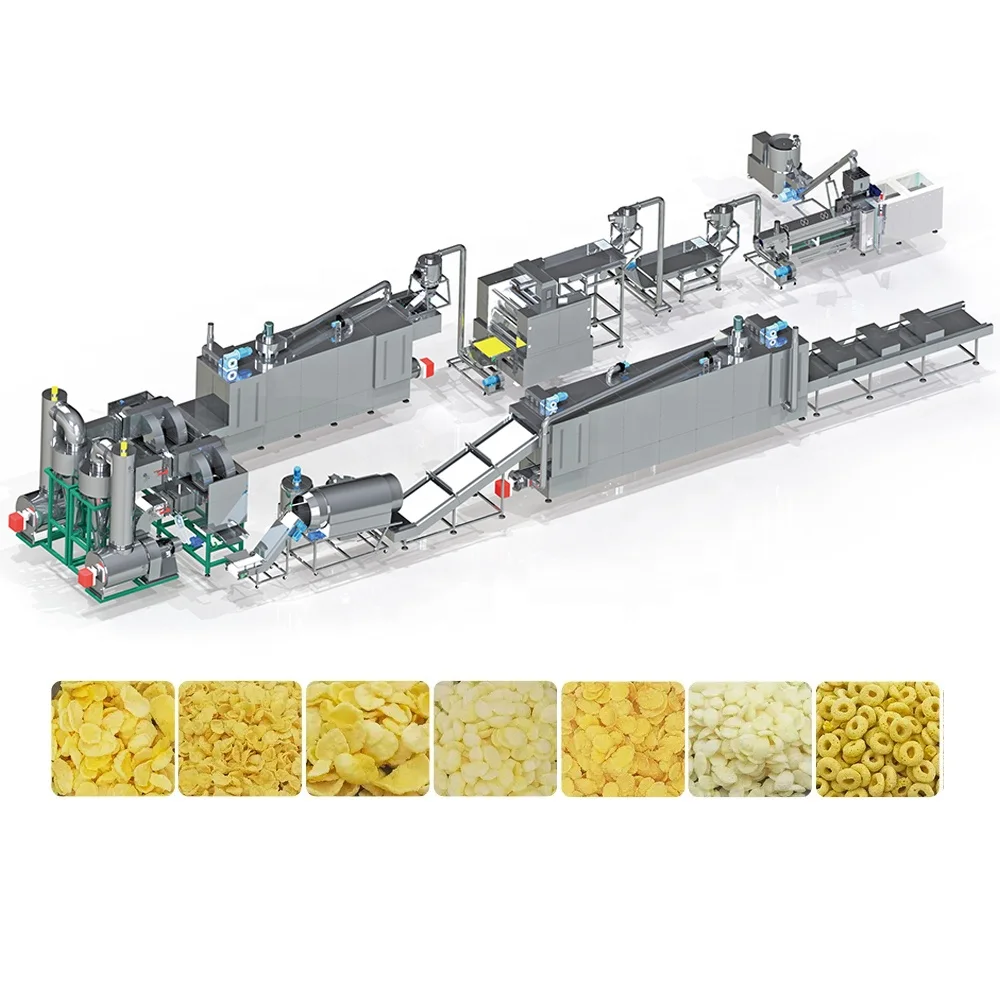
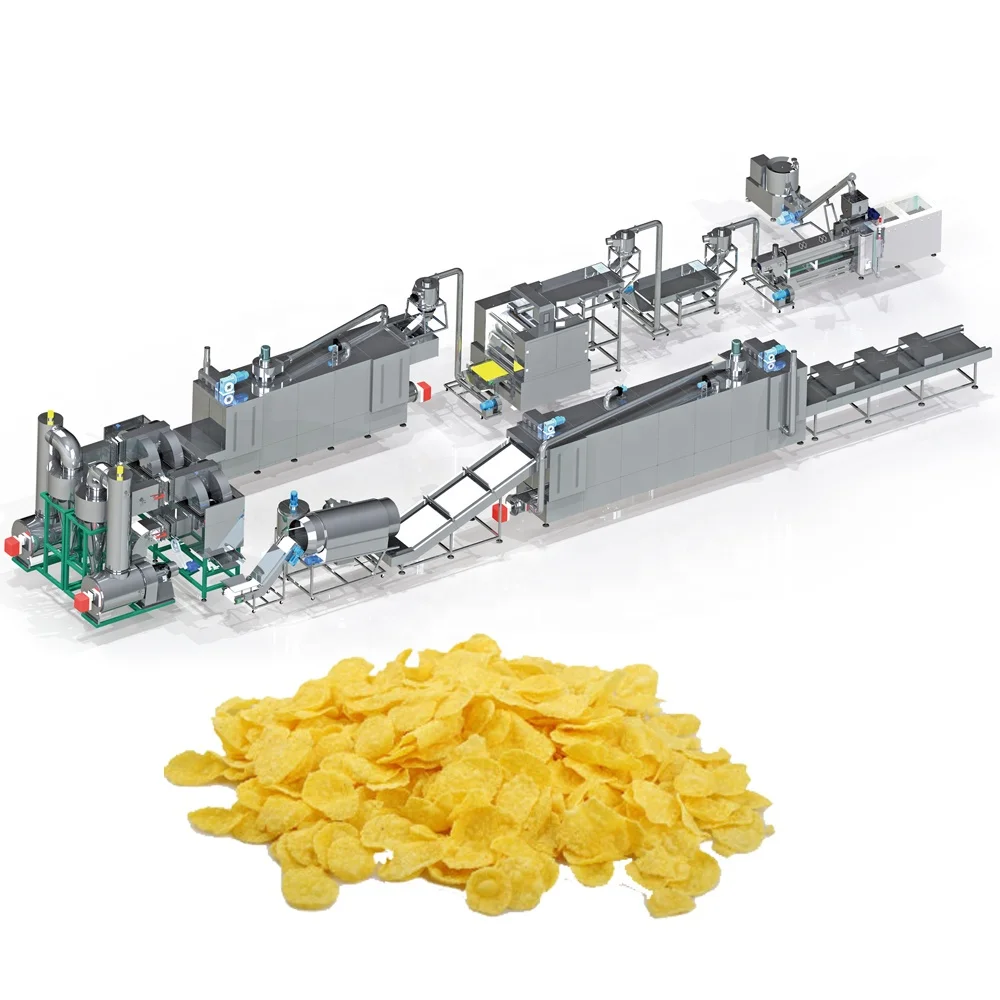
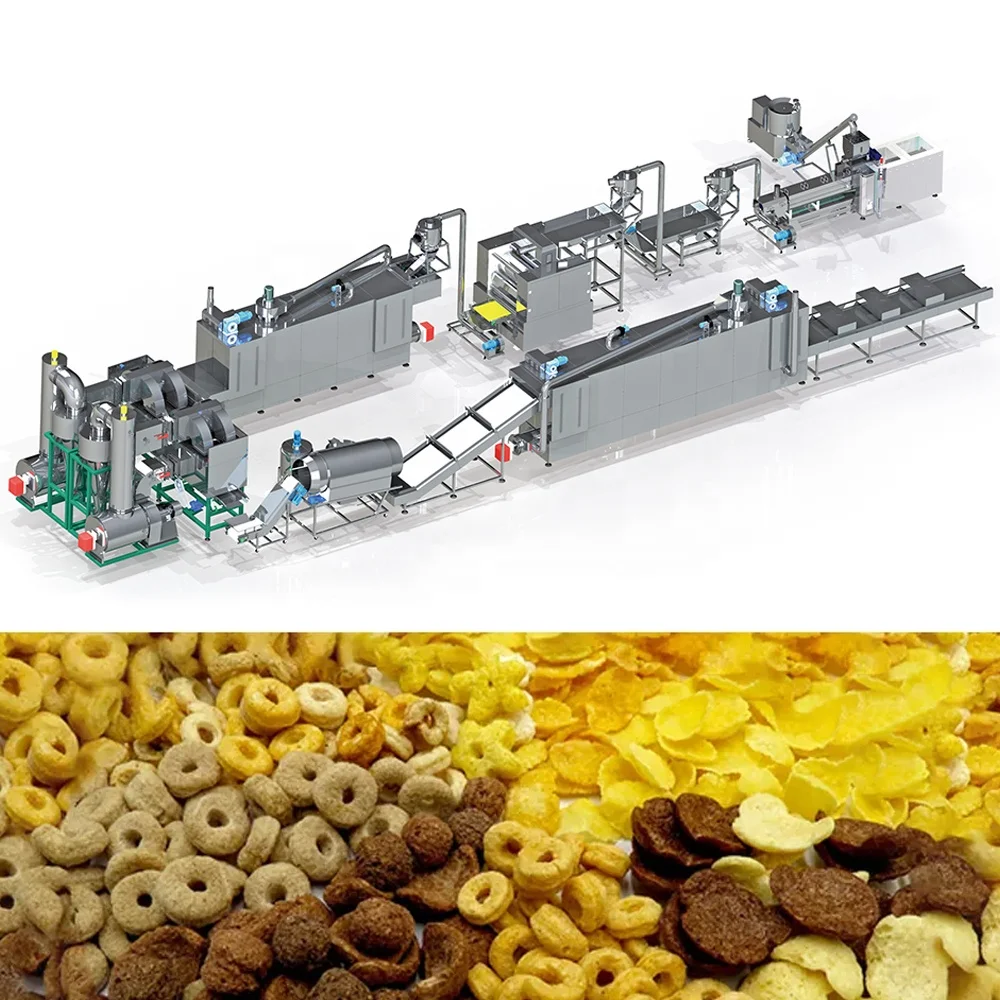
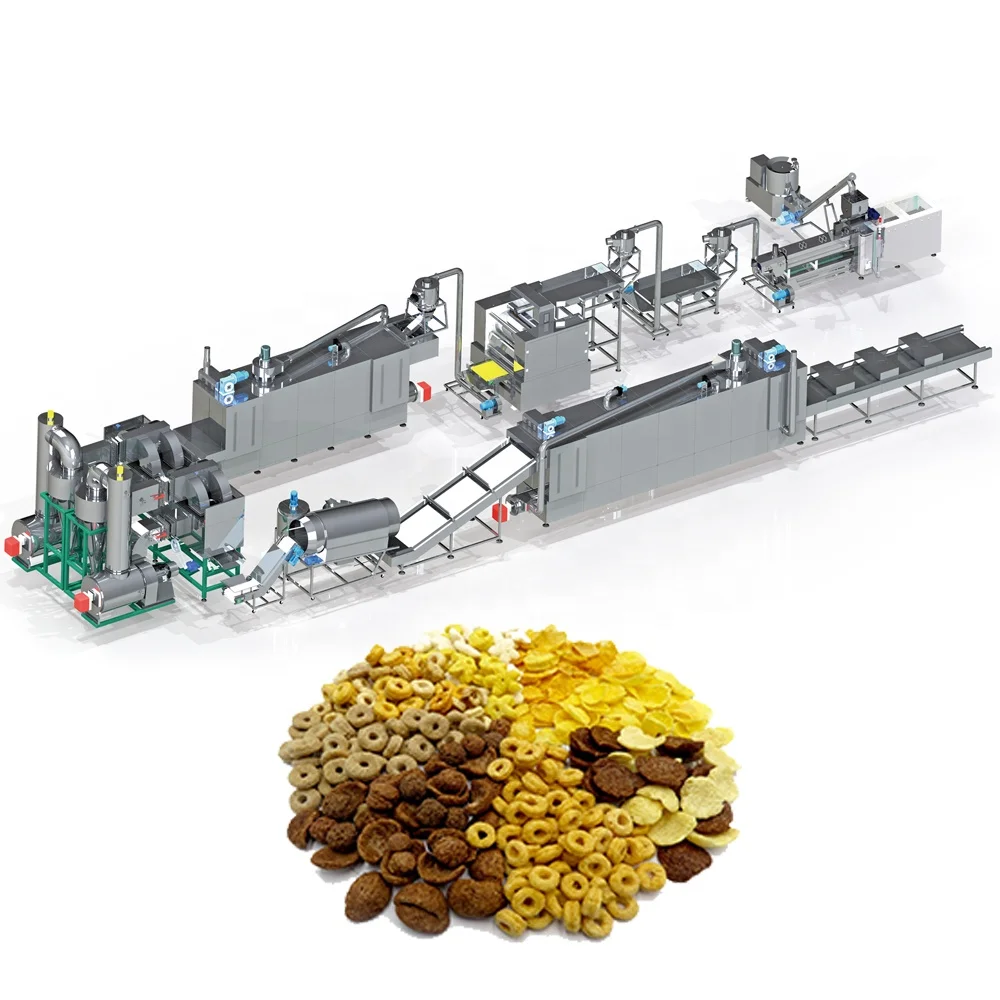
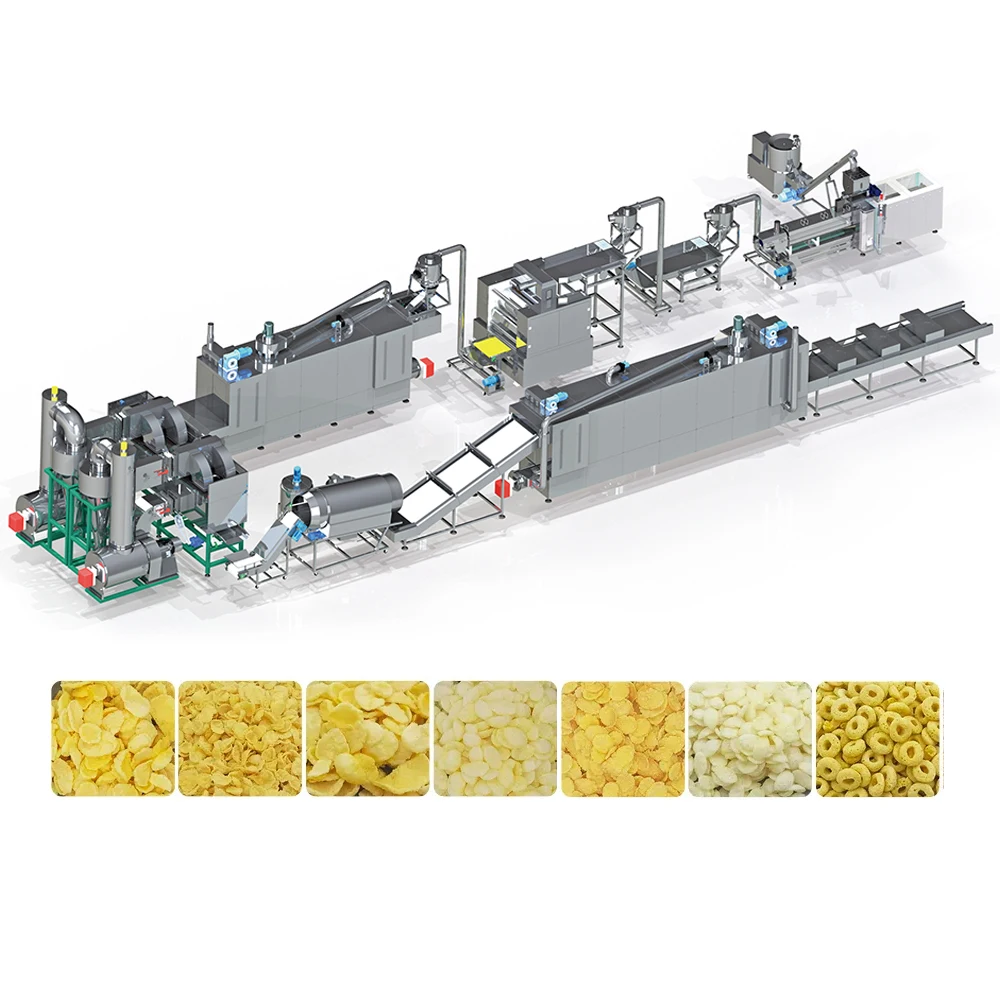
MT75 Corn Flakes Production Line, Twin Screw, 300-500KG/HR Output — a complete turnkey food extrusion processing line from batching through flaking, hot air roasting, sugar coating and packing. Hydraulic double-roller flaking with infrared temperature control delivers uniform flake thickness, while dual-fan roasting ensures precise toasting. PLC and MCC automation keeps every station throughput-matched to eliminate bottlenecks. Backed by in-house trial runs on your raw material before shipment, with screw and die configuration documented to your target product format.
Description
Turnkey Line Engineering — Every station from batching to packing sized to actual throughput, eliminating the bottlenecks that occur when extruders, flakers and dryers are sourced from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model | MT75 |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/h (basis to be confirmed) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC with MCC |
| Dryer Heating Source | Gas or Electric |
| Flaking Drive | Double motors, hydraulic roller system |
| Flaking Temperature Control | Infrared sensor |
| Roasting Oven | Hot air, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spray nozzle |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits, maize flour |
| Sugar-coated corn flakes | Corn base with sugar syrup coating |
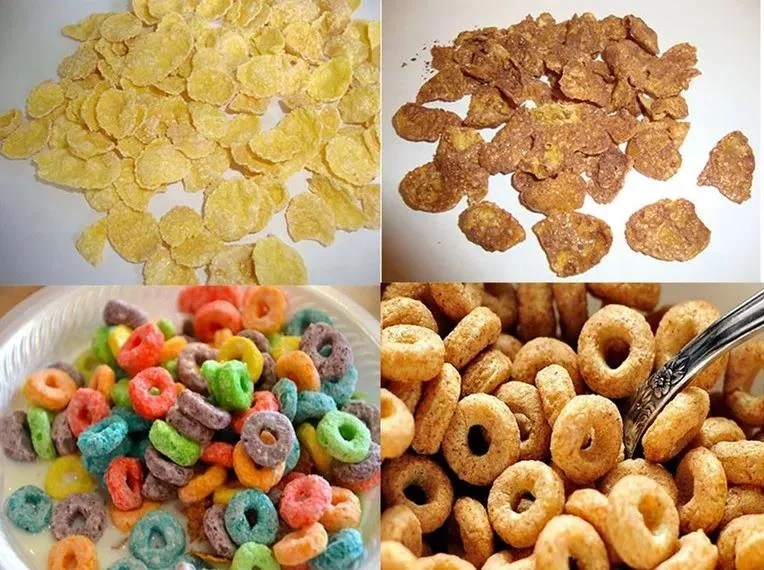
| Shaped breakfast cereals | Rice, wheat, oat, barley powder — ball, tube, ring, star, fruit loop formats |
| Fortified cereal production | Grain blends with added vitamin and mineral premix |
| Extruded snack cereals | Multi-grain formulations in wheel, flower and heart shapes |
Why "500 kg/h" Means Nothing Without Line Integration
A corn flakes production line turnkey only delivers its rated output when every downstream station matches the extruder’s actual throughput.
I’ve watched contractors quote an extruder based on a nameplate figure, then bolt on a dryer half the size and a coating drum that can’t keep pace. The result is product backing up at the flaker discharge, operators shoveling material by hand, and the whole corn flakes production line turnkey running at a fraction of what was promised. The bottleneck is rarely the extruder itself [NEED_CITE: throughput matching principles in continuous food processing lines]. It is almost always the station that was treated as an afterthought.
Station-by-Station Throughput Matching
A corn flakes production line turnkey must be engineered as a single system, not a collection of standalone machines. The MT75 line sequences mixing, extruding, flaking, drying, hot air roasting, sugar spraying, sugar coating, a second drying stage, cooling and packing in a continuous flow. Each station is sized so that material moves forward without queuing or starving the next unit. The hydraulic flaking system uses double motors for independent roller drive, maintaining uniform flake thickness even as feed rate varies across the run.
Roasting and Coating Without the Bottleneck
The hot air roasting oven runs two separate circulating fans with a cyclone dust removal device, keeping temperature distribution even across the bed depth. After roasting, the coating stage uses a double tumble system for sugar melting paired with a dedicated elevator and spray nozzle array. This prevents the common failure mode where coated product clumps because the drum was undersized for the upstream volume [NEED_CITE: sugar coating adhesion and tumble drum sizing in cereal manufacture]. Every connection between these stations is specified before the line ships.
Reading the Specs That Actually Matter
The twin-screw configuration handles the shear and moisture range that corn, rice, wheat and oat blends demand, where a single-screw would struggle with inconsistent gelatinisation. Installed power of 210 kW and running consumption of 150 kW indicate a motor and barrel sizing that allows sustained output without thermal overload during long production shifts. The PLC with MCC control gives operators recipe storage and repeatable parameter sets, which matters when switching between natural flakes and sugar-coated variants on the same line. Infrared temperature sensing at the flaker means roller surface heat is monitored in real time, preventing the thin spots and scorching that ruin flake integrity. The overall footprint of 45 × 1.5 × 3.5 m reflects a linear layout that fits standard industrial bays without requiring mezzanine structures.
What Happens When Stations Are Mismatched
A contractor I worked with sourced an extruder from one supplier and a dryer from another for a breakfast cereal project. The dryer could not handle the moisture load coming off the flaker, so flakes entered the roasting oven too wet. The roasting cycle had to be extended, which dropped the line output well below the figure everyone had planned around. Operators were manually diverting product to keep the roaster from flooding [NEED_CITE: moisture load calculation errors in multi-vendor cereal line integration]. That project took months of rework to bring online.
Why Procurement From One Supplier Changes the Outcome
Throughput across every station is calculated against your raw material and target flake format before the layout is drawn, not adjusted after machines arrive. The screw and die configuration is specified to your formulation — corn grits behave differently from oat or barley blends, and the extruder internals reflect that. A trial run on your actual raw material takes place in the testing workshop, producing a report you can review before the line ships. Electrical schematics and voltage are confirmed against your facility’s supply, so the PLC and MCC panels arrive wired for your market. The entire line — mixing through packing — carries CE certification under a single supplier’s responsibility.
Documentation & Verification
- Line layout and capacity calculation matched to your corn or multi-grain formulation
- Screw and die configuration record specific to your target flake shape and density
- Trial run report on your raw material produced in the testing workshop before dispatch
- Electrical schematic with voltage and frequency confirmed for your facility
- Factory test record covering all stations from extruder through packing conveyor
Installation, Commissioning & Support
- Foundation plan based on the 45 m linear footprint and station load points
- Dedicated power circuit sized for 210 kW installed capacity with MCC protection
- Station-by-station commissioning sequence from mixer through cooler and packer
- PLC recipe programming for natural and sugar-coated variants during on-site setup
- Operator training on hydraulic flaker adjustment and infrared sensor calibration
- Wear parts list covering screws, dies, roller surfaces and spray nozzles
Preparing Your Inquiry
Share the specific grain formulation you plan to run, whether corn, rice, wheat, oat or a blend, along with the flake format and coating type you need. Confirm your facility voltage, frequency and available floor length so the layout can be drafted to fit. If you have existing upstream milling or downstream packing equipment, note the interface points so the line integrates without gaps.
Frequently Asked Questions
Q: How is throughput matched between the extruder and every downstream station?
A: Each station — flaker, dryer, roaster, coater, cooler — is sized based on the extruder’s actual output on your specific raw material, not on a generic nameplate figure. The layout is calculated so product flows continuously without queuing or starving any unit.
Q: What electrical details are confirmed before the line is built?
A: Voltage, frequency and control language are verified against your facility’s supply and operator requirements. The PLC and MCC panels are wired and labelled accordingly, and the electrical schematic is provided for your local electrician before shipment.
Q: Can the line layout fit an existing building with fixed column spacing?
A: The 45 m linear footprint is a reference, not a constraint. The layout is redrawn around your column positions, utility drop points and ceiling height, with station spacing adjusted to maintain material flow without compromising access for maintenance.
Q: Is a trial run performed on our raw material before the line ships?
A: Yes. Your formulation is run in the testing workshop, and the resulting trial report covers extrusion behaviour, flake quality and coating adhesion so you can evaluate product output before the equipment leaves the factory.
Q: What does the commissioning schedule look like for the full line?
A: Commissioning follows a station sequence starting with the mixer and extruder, then progressing through flaking, drying, roasting and coating. Each stage is tested independently before the next is brought online, with operator training integrated throughout the process.
Related products
-

Puff Corn Snacks Food Line Puffed Rice Ball Production Making Equipment Machines
¥10,565.00 Select options This product has multiple variants. The options may be chosen on the product page -
New Stainless Steel Automatic Puffed Rice Flour Snacks Making Machine High Productivity Multi-function
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Stainless Steel Corn Puff Cake Making Machine Corn Snack Food Machines Top Selling Snacks Machine
¥8,560.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Rice Crispies Extruder Machine/Chocolate Corn Flakes Extrusion Plant/wheat Flaking Snacks Production Line
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page