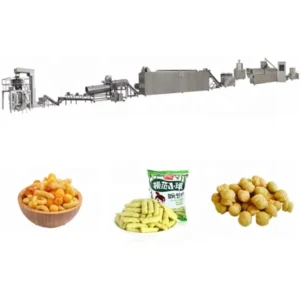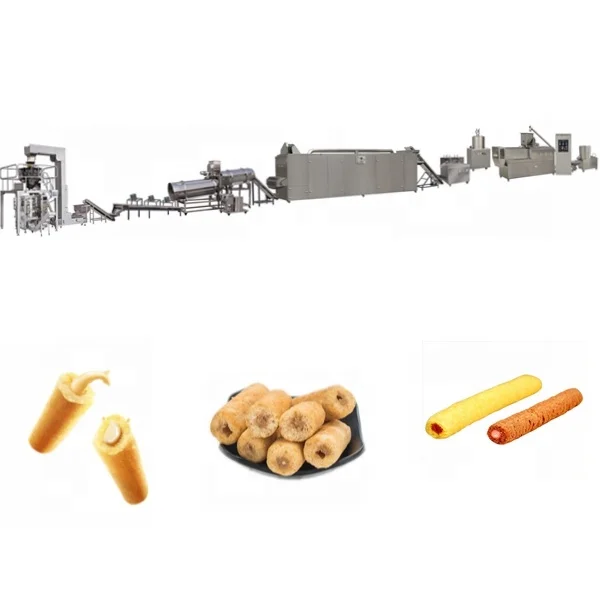
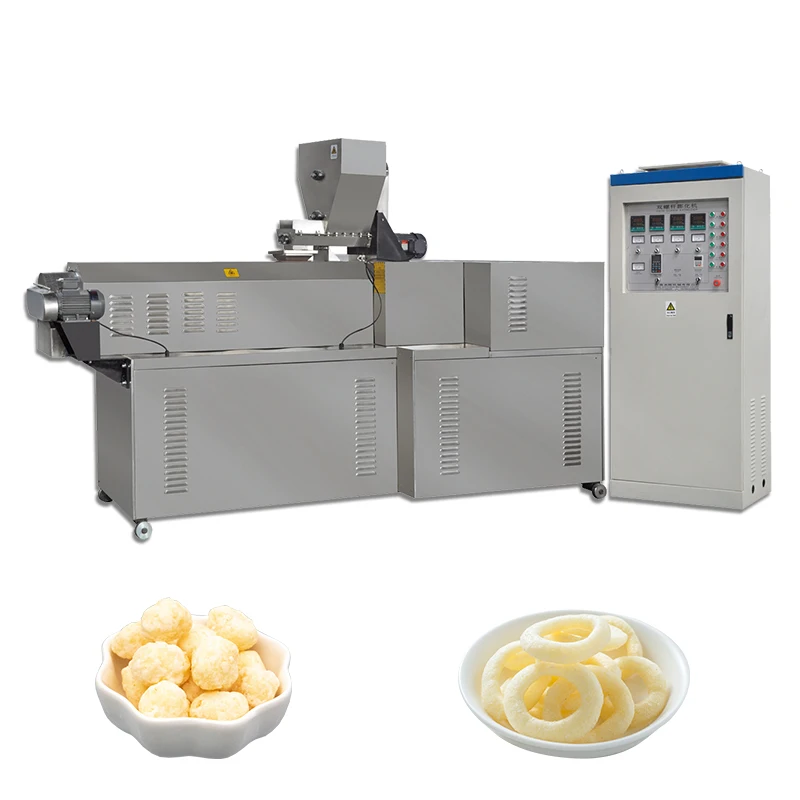
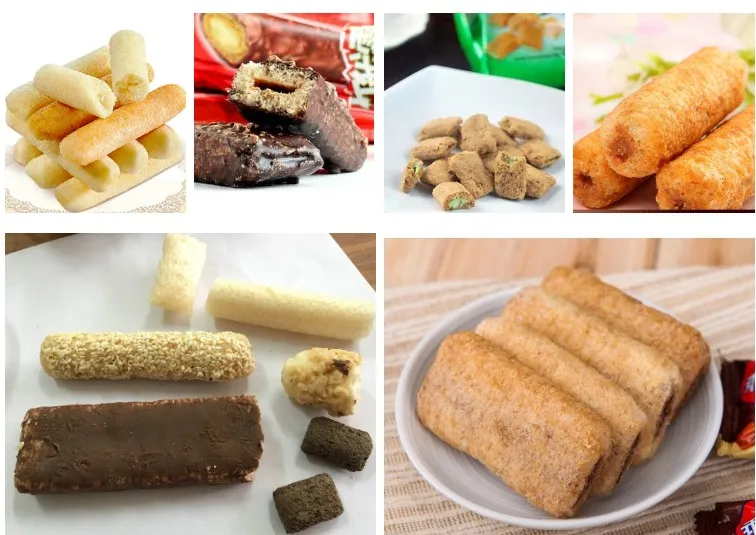

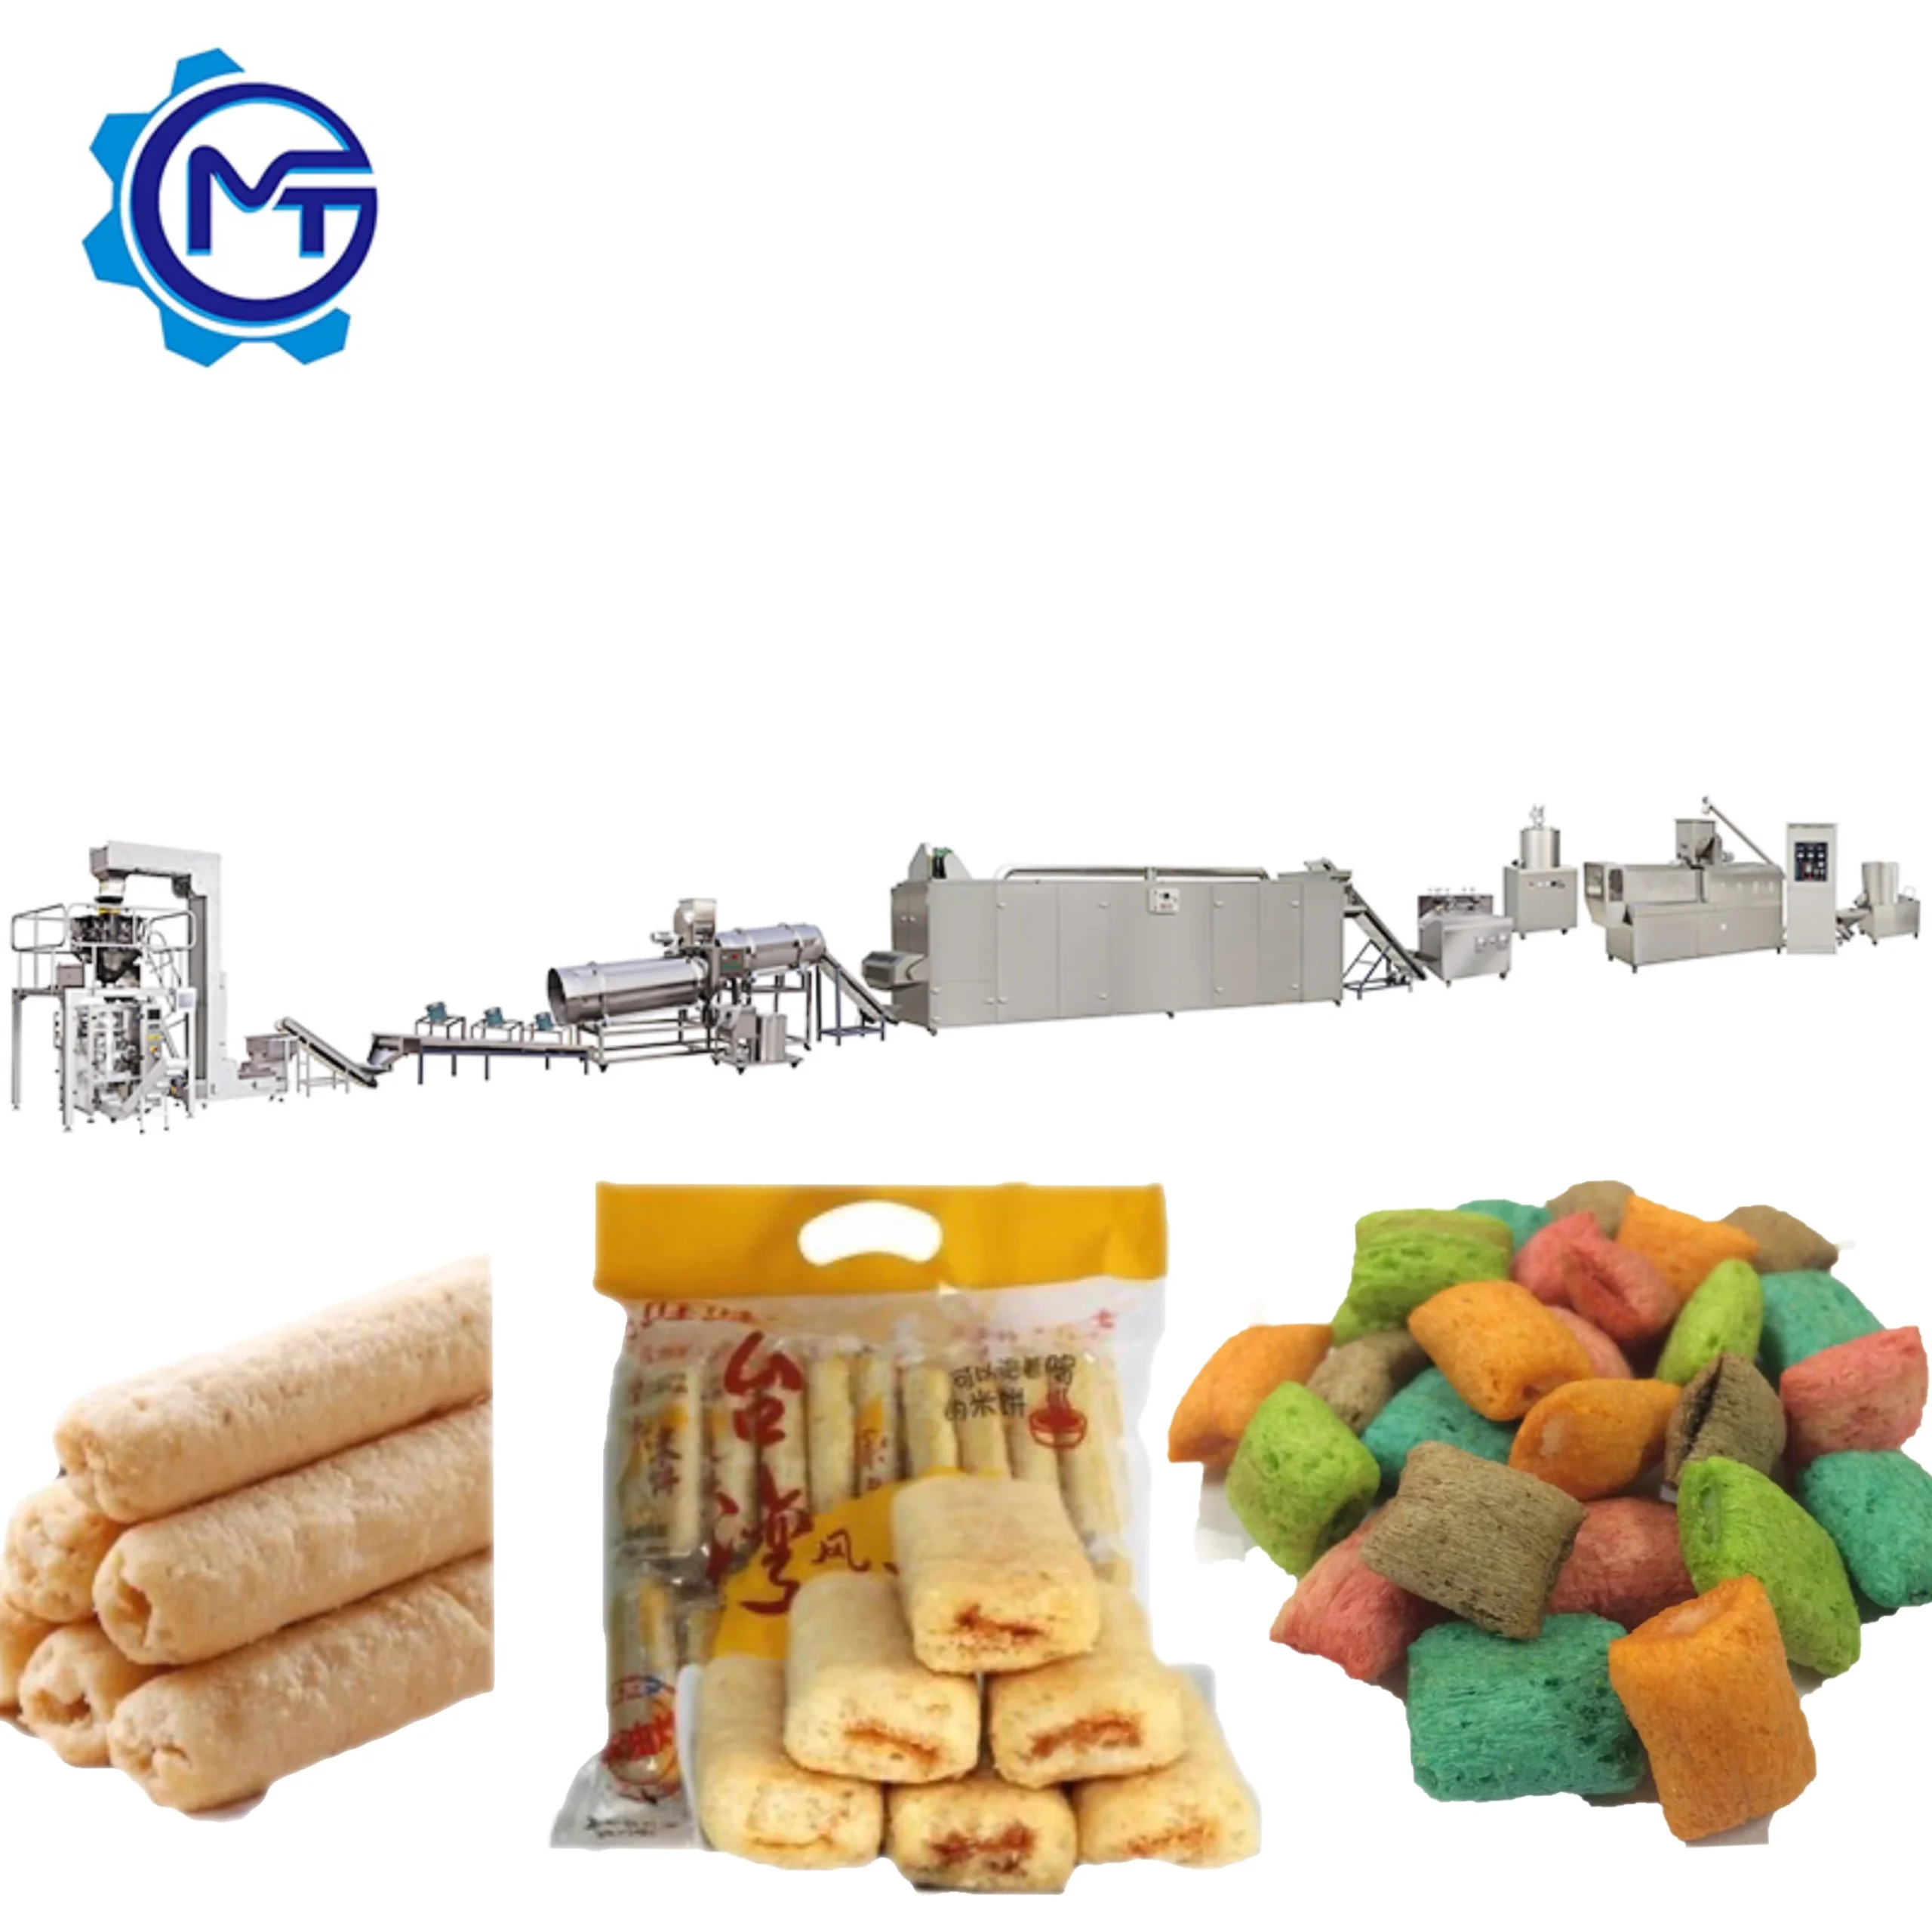
MT70 / MT85 / MT75 Twin Screw Extrusion Corn Flakes & Puffed Snack Production Line — complete turnkey line from batching through extrusion, drying, coating and packing.
- Twin screw configuration and die geometry specified to your cereal flour blend, controlling expansion, density and final flake texture
- Every station throughput-matched to eliminate downstream bottlenecks across the full production layout
Line layout, screw configuration record and in-house trial run report on your raw material provided before shipment.
Description
Screw Geometry Tuned to Your Flour — every MT twin-screw extruder is configured for the buyer’s actual corn, rice, or oat blend rather than shipped with a generic screw profile, so the dough achieves the exact gelatinisation and expansion the downstream dryer expects.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extrusion Corn Flakes & Puffed Snack Production Line |
| Available Models | MT70 / MT85 / MT75 |
| Screw Type | Twin Screw |
| Installed Power (MT70 / MT85 / MT75) | 130 kW / 180 kW / 220 kW |
| Power Consumption (MT70 / MT85 / MT75) | 95 kW / 120 kW / 130 kW |
| Output Capacity (MT70) | 100–120 kg/h (basis not stated in source — confirm raw material / moisture / product shape) |
| Output Capacity (MT85) | 200–300 kg/h (basis not stated in source — confirm raw material / moisture / product shape) |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material / moisture / product shape) |
| Overall Dimensions (MT70 / MT85 / MT75) | 21 × 1.5 × 2.2 m / 25 × 1.5 × 2.2 m / 28 × 1.5 × 2.2 m |
| Raw Materials | Corn, rice, wheat, oat, barley flour |
| Die Configuration | Interchangeable dies for ball, tube, stick, ring, fruit loop, star, wheel, flower, heart shapes |
| Heating Source (Dryer) | Gas or Electric |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Screw Feature | Automatic lubricating, cooling function; wear-resistant screw material |
| Voltage & Frequency | Customizable to local supply |
| Assembly State | Complete turnkey line from mixing to packing |
| Standards | CE certified; ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Breakfast corn flake production | Corn grits and corn flour blends |
| Fortified breakfast cereal lines | Multi-grain mixes with vitamin premix |
| Cheese ball and puffed snack manufacturing | Corn, rice, or wheat flour bases |
| Fruit loop and ring cereal formats | Oat and barley flour with sugar coating |
| 2D and 3D extruded snack shapes | Cereal flour blends with interchangeable dies |
Why "Rated Capacity" Means Nothing Without a Trial Run
A corn flakes extruder production line turnkey package quoted at a nominal output figure is only a starting guess until the dough actually runs through the barrel on the buyer’s flour blend.
I remember a buyer who sourced an extruder based purely on a brochure number. The machine arrived, his corn grits formula had slightly higher fibre content than the vendor tested with, and the dough viscosity spiked inside the barrel. Expansion dropped, flakes came out dense, and the downstream dryer — sized for a lighter product — over-dried the batch. Two weeks of line downtime followed while new screw elements were flown in [NEED_CITE: material variability effects on twin-screw extrusion output]. That is the gap a trial run closes before the machines ever leave the factory.
When a corn flakes extruder production line turnkey proposal lands on your desk, the first question is not the price — it is whether anyone has actually extruded your flour on that screw configuration.
Matching Extruder Output to Dryer and Coating Drum Throughput
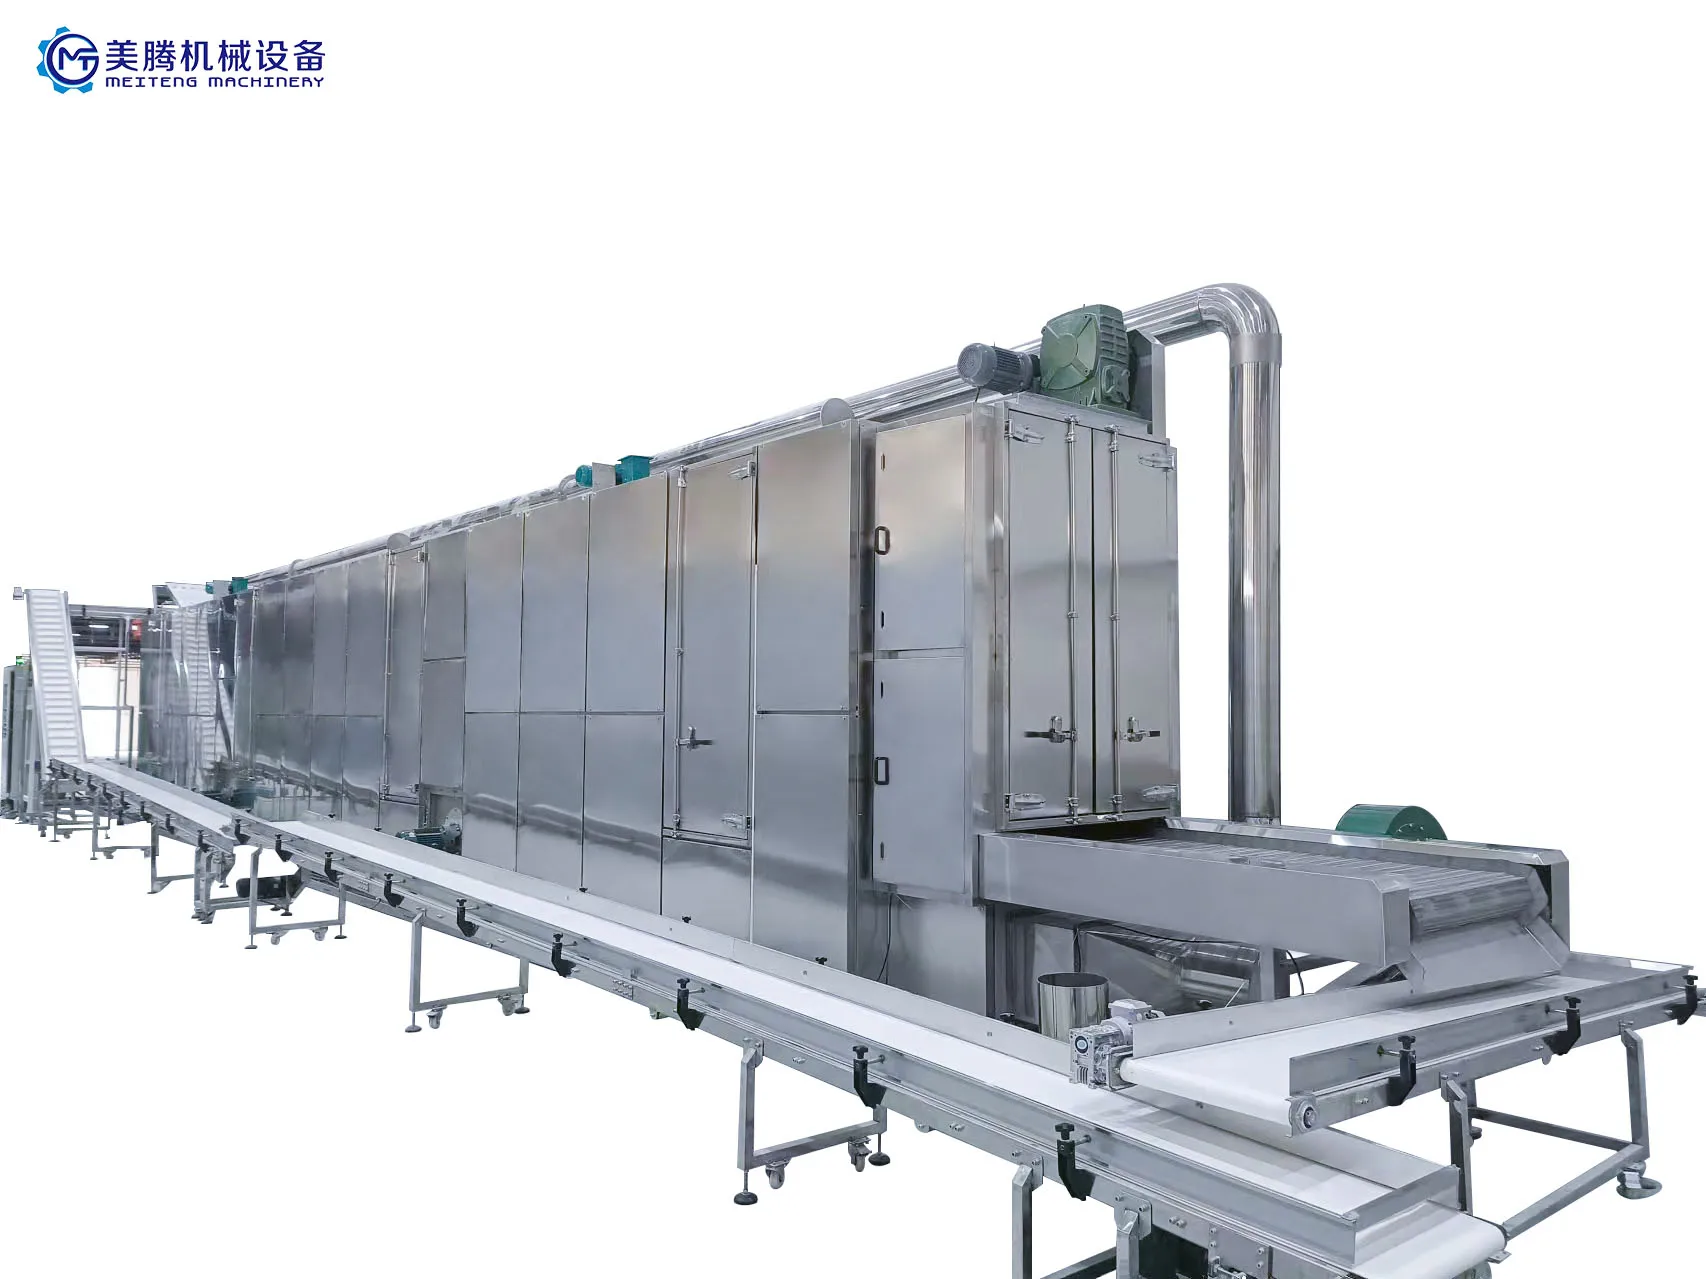
The most common failure in a cereal extrusion line is not the extruder itself but the mismatch between stations. An MT75 extruder pushing dough at its upper range will overwhelm a dryer that was spec’d for a smaller model, leaving flakes sitting on the belt too long or passing through too wet. Every MT line layout calculates the mass balance from mixer through extruder, dryer, coating drum, cooler, and packer so each station handles the same throughput without buffering or starving. This is why a single-supplier turnkey approach matters: one engineering team owns the entire flow, and no station gets overlooked.
Screw Profile and Die Geometry Specified to Your Raw Material
Corn flour, oat flour, and rice flour each behave differently under shear and heat inside a twin-screw barrel. The screw elements — kneading blocks, conveying sections, reverse-flight zones — are arranged to control residence time and mechanical energy input for each specific blend [NEED_CITE: screw element configuration principles for food extrusion]. The die orifice diameter and land length then determine the pressure drop at exit, which directly controls expansion ratio and final flake density. A generic screw build might run corn adequately but produce flat, unexpanded pieces when the recipe shifts to a high-oat fortified cereal. MT documents the screw configuration and die selection for each buyer’s recipe, so the same extruder platform can be reconfigured later when new product formats are added.
Reading the Specs That Actually Matter
The installed power and power consumption figures across the MT70, MT85, and MT75 models reveal the thermal and mechanical energy available for gelatinisation. Higher installed power on the MT75 (220 kW) supports the longer barrel and greater screw volume needed for 300–500 kg/h class runs, while the MT70’s 130 kW suits smaller batch operations. The twin-screw design is essential here: unlike single-screw extruders, twin screws provide positive conveying and self-wiping action, which prevents starch build-up and allows processing of higher-moisture doughs without surging [NEED_CITE: twin screw versus single screw extrusion for cereal applications]. The automatic lubricating and cooling function on the screw shaft maintains barrel temperature uniformity across long production runs, preventing the hot spots that cause inconsistent expansion. Die interchangeability across ball, tube, ring, fruit loop, and star shapes means a single extruder covers multiple SKU formats without requiring a second capital machine.
The Hidden Cost of Skipping Voltage Confirmation
One detail that routinely delays commissioning is electrical mismatch. The destination market may run on a different voltage or frequency than the factory where the machine was tested, and motor speeds, heater outputs, and control logic all shift when the supply is wrong. A corn flakes extruder production line turnkey project that skips formal voltage and frequency confirmation before production can face weeks of rewiring on site [NEED_CITE: voltage and frequency standards by export market]. The control language on the HMI is another easily missed item — operators staring at alarm messages in an unfamiliar language makes troubleshooting slow and error-prone.
Why Procure This Line Here
Throughput matching across every station means the mixer, extruder, dryer, coating drum, cooler, and packer are calculated as one system, not assembled from separate catalogues. The in-house testing workshop allows trial runs on the buyer’s actual corn or cereal flour before shipment, generating a trial run report that validates expansion, density, and texture against product specifications. Screw configuration and die design are documented specifically for each buyer’s raw material and target format, so reconfiguration for future products is a known procedure rather than guesswork. Pre-sales line layout and capacity calculation cover factory footprint, utility planning, and phased installation scheduling. Ongoing maintenance support includes wear parts supply — screws, dies, and barrel liners — so the first replacement does not become a sourcing emergency.
Documentation & Verification
- Line layout drawing with throughput calculation matched to your corn or cereal flour recipe
- Screw and die configuration record documenting element arrangement for your target flake density
- Trial run report on your raw material produced in the testing workshop before dispatch
- Electrical schematic with voltage, frequency, and control language confirmed to your market
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation and utility plan based on the MT model’s overall dimensions and power consumption rating
- Dedicated electrical circuit sized to the installed power of your selected extruder model
- Modular station delivery with phased assembly sequence to match site readiness
- First-run parameter setting covering barrel temperature zones, screw speed, and die pressure
- Operator training on HMI controls, die changeover, and screw cleaning procedures
- Wear parts inventory covering screws, dies, and barrel liners for the first replacement cycle
Preparing Your Inquiry
Share your target product format — corn flakes, cheese balls, fruit loops, or a mix — along with the raw material blend and any fortification additives you plan to use. Specify your local voltage, frequency, and preferred control language so the electrical design matches your facility from day one. If you have an existing dryer or packing system that must integrate with the new extrusion line, provide its throughput rating so the layout can be matched accordingly.
Frequently Asked Questions
Q: How is the line capacity verified on my actual corn or cereal flour blend before I commit?
A: Before shipment, the extruder runs a trial in the in-house testing workshop using your exact flour blend. The output is measured for expansion ratio, flake density, and texture. A trial run report is generated and shared with you, so the capacity figure is based on real data from your material rather than a generic benchmark.
Q: How do you match dryer and coating drum throughput to the extruder so no station bottlenecks the line?
A: Each line layout begins with a mass balance calculation across every station. The dryer belt length and heating capacity, coating drum volume, and cooler airflow are all sized to handle the extruder’s actual output on your recipe. This prevents wet flakes piling up before the dryer or the coating drum running half-empty.
Q: Can the screw configuration and die be changed later if I add a new snack format to the same line?
A: Yes. The twin-screw barrel accepts different element arrangements, and the die plate is interchangeable across ball, tube, ring, fruit loop, star, and other shapes. The original screw and die configuration is documented, so reconfiguring for a new product is a defined procedure with known screw profiles and die geometries.
Q: What voltage, frequency, and control language will be confirmed before the machines are built?
A: Voltage, frequency, and HMI language are confirmed during the specification stage before production starts. The electrical schematic reflects your local supply standard, and motor ratings, heater elements, and control logic are all matched accordingly. This avoids on-site rewiring and commissioning delays.
Q: How is the phased installation and commissioning schedule planned for a complete turnkey project?
A: The installation sequence follows the line flow — extruder first, then dryer, coating, cooler, and packing. Each phase has defined utility prerequisites and floor readiness checks. Commissioning covers parameter tuning on your raw material, operator training, and a production validation run before the line is handed over.
Related products
-

Puff Corn Snacks Food Line Puffed Rice Ball Production Making Equipment Machines
¥10,565.00 Select options This product has multiple variants. The options may be chosen on the product page -
New Condition Automatic Corn Puff Snacks Food Extruder Cheese Ball Making Machine Plant
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Puffed Food Snack Machine Electric Corn Puffs Snacks Making Machinery New Condition Flavorful Puff Snack Production
¥7,550.00 Select options This product has multiple variants. The options may be chosen on the product page -

Corn Puff Processing Line with Mixer Fryer Baking Oven Automatic High Productivity Grain Products Snack Making Machine
¥8,300.00 Select options This product has multiple variants. The options may be chosen on the product page