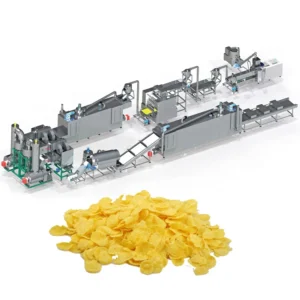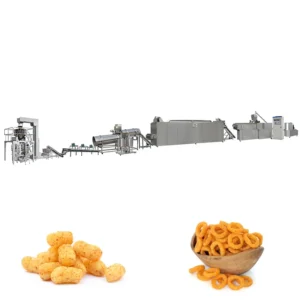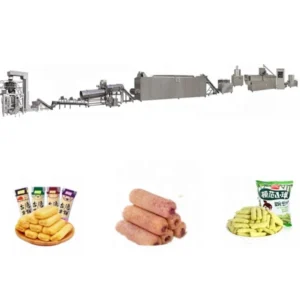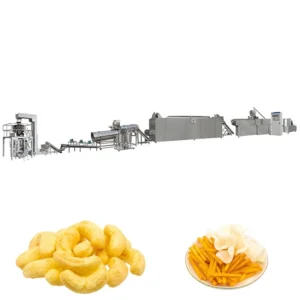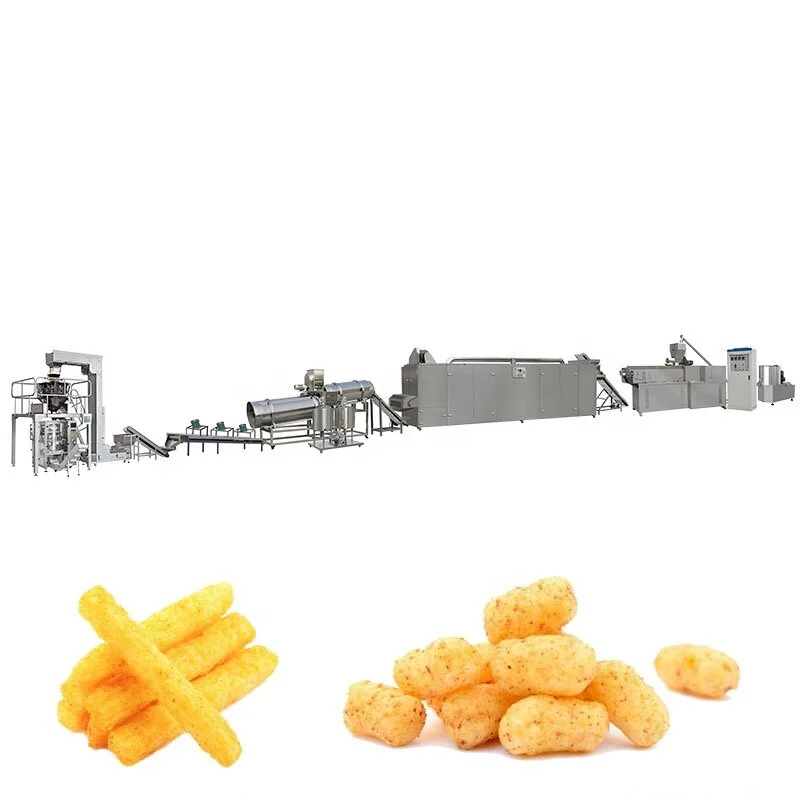
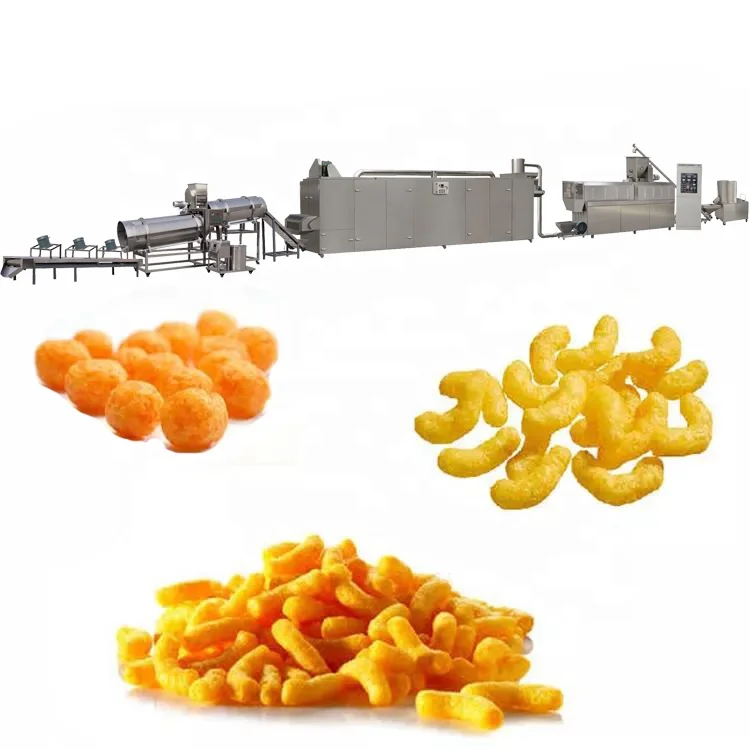
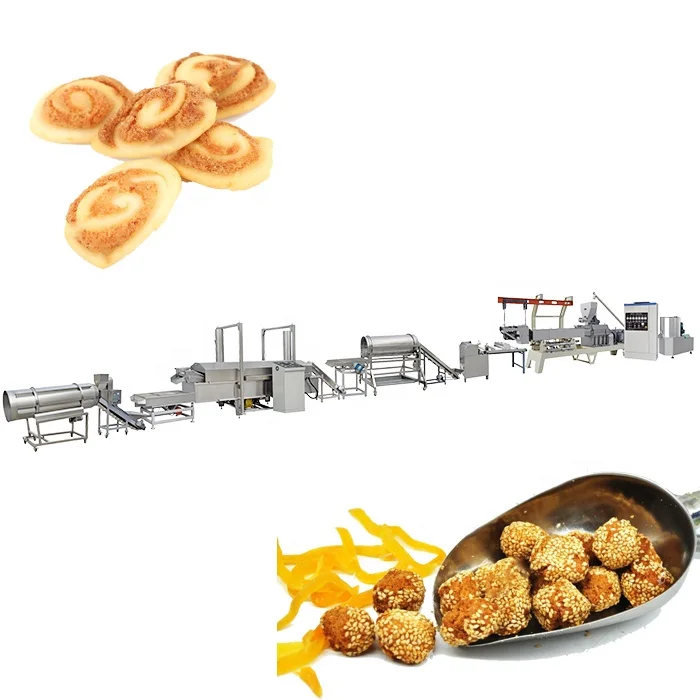
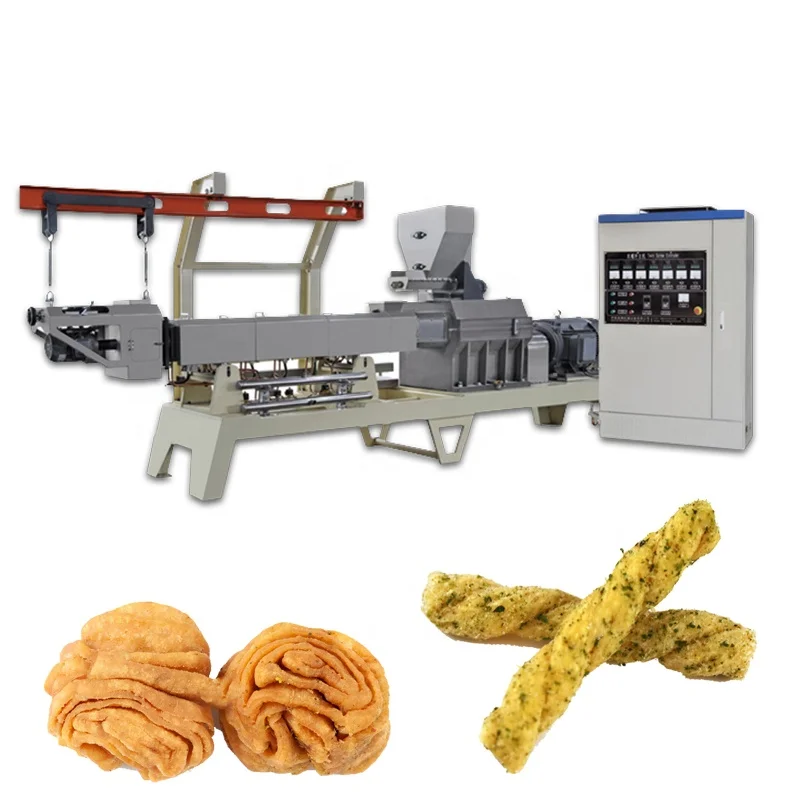
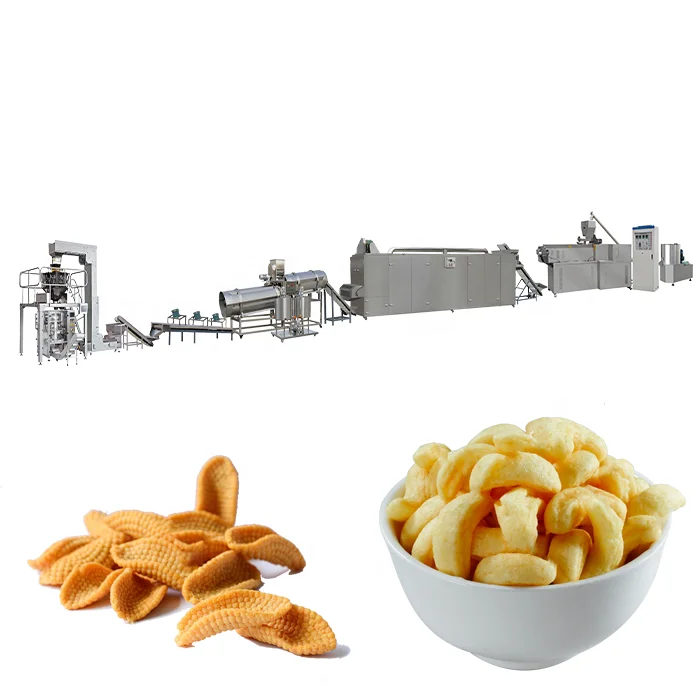
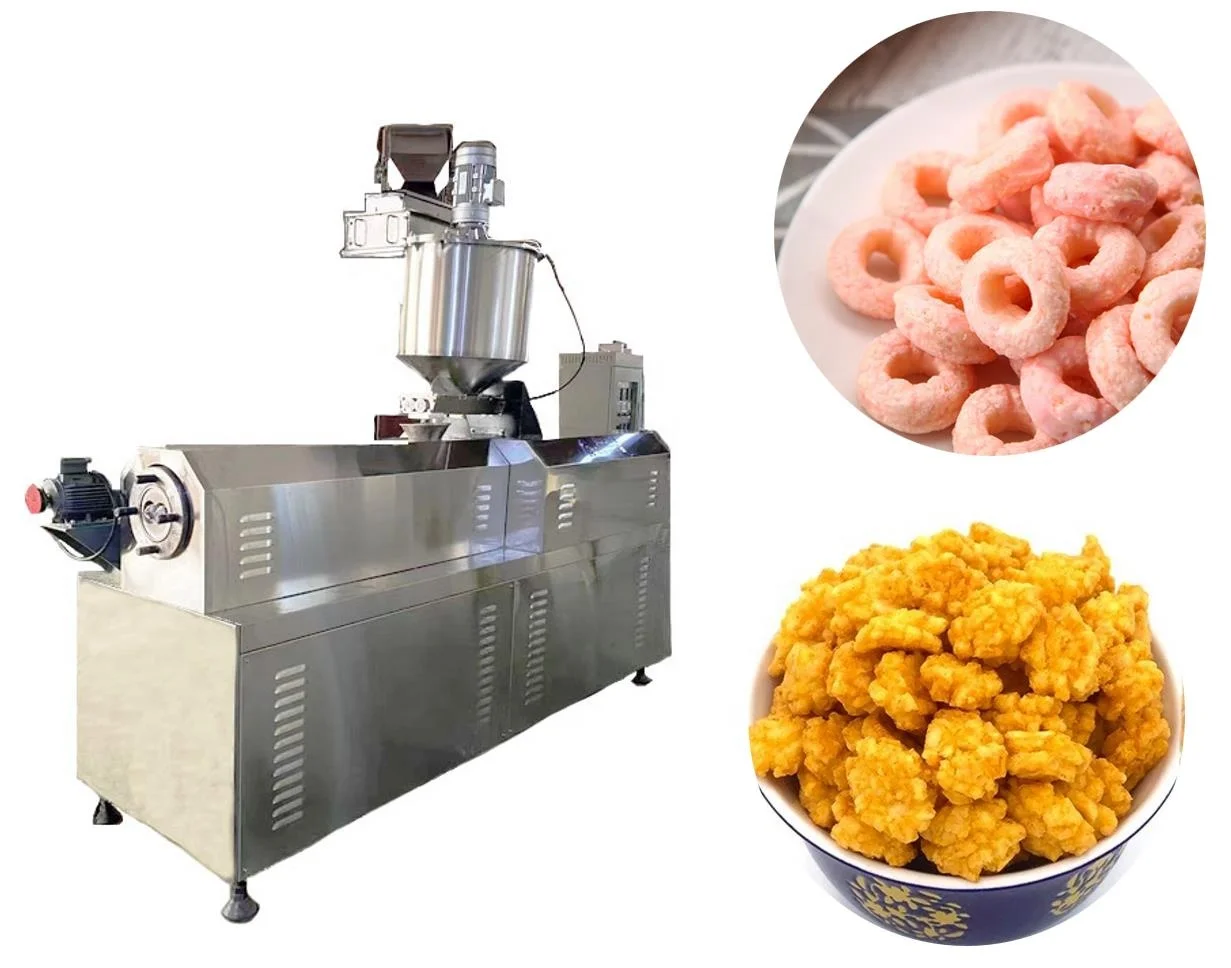
Twin Screw Corn Crisps Extrusion Line, 380V/50Hz, Food-Grade SS304 Contact, Multi-Shape Die Options — complete turnkey system from batching through extrusion to packing. Screw configuration and die geometry are specified to your cereal blend, controlling expansion, density and texture across every product format. All stations are throughput-matched under one supplier to eliminate bottlenecks between extruder, dryer and flavouring.
Description
Throughput-Matched Line Design — every station from mixer to packing is sized to the extruder’s actual output on your cereal blend, eliminating the bottleneck that occurs when equipment is sourced separately.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Crisps / Maize Chips / Corn Sticks Extrusion Production Line |
| Extruder Type | Twin-screw (double screw) extruder |
| Raw Materials | Rice, millet, brown rice, buckwheat, corn/maize, and other cereals |
| Voltage & Frequency | Three-phase 380V/50Hz; Single-phase 220V/50Hz (configurable to buyer’s local supply) |
| Motor & Inverter | Siemens (China-made) or China top brand motor; Delixi or Delta inverter |
| Contact Material | Food-grade stainless steel 201/304 |
| Energy Source Options | Electricity, gas, diesel, or steam |
| Electrical Power (electricity-heated) | approx. 100 kW (basis to be confirmed) |
| Electrical Power (gas/diesel-heated) | approx. 50–60 kW (basis to be confirmed) |
| Line Stations | Mixer → Extruder → Vibrate Cooler → Roasting/Drying Machine → Packing Machine |
| Dryer Configuration | Multi-layer design, configurable length and layer count |
| Flavouring System | Semi-automatic or automatic; supports sugar, oil, and powder seasoning |
| Die Configuration | Interchangeable moulds for various shapes |
| Assembly State | Complete line, shipped as separate stations |
| Standards | CE (electronic edition available on request) |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn crisps and maize chips | Corn/maize flour with adjustable moisture and seasoning |
| Corn sticks and extruded cereal shapes | Cereal blends through interchangeable die plates |
| Core-filled and pillow snacks | Cream or paste centre injected through co-extrusion dies |
| Artificial and fortified rice | Rice, millet, brown rice, buckwheat, and mixed cereals |
| Puffed snack variants | Cheese balls, rice cakes, cereal bars, and sheet snacks |
Why "Rated Capacity" Means Nothing Without Your Raw Material
A corn crisps extrusion production line turnkey package quoted at a fixed output figure only holds if your flour blend, moisture level, and target density match the test conditions exactly.
I spent weeks on a site in central Mexico where the corn flour arriving from the local mill carried two percentage points more moisture than the sample used for the original quotation. The extruder ran, but expansion dropped and the line could not sustain its nameplate throughput. Parameters had to be rebuilt from scratch during commissioning. That delay cost the buyer far more than a factory trial ever would. [NEED_CITE: moisture variation in milled cereal feedstocks and extrusion stability]
Screw Geometry Dictates What Your Cereal Blend Can Become
The twin-screw extruder at the heart of this line allows the screw elements and barrel zones to be rearranged for the specific starch behaviour of your cereal blend. Corn flour gelatinises at a different shear and temperature threshold than buckwheat or brown rice, so the screw profile must be specified before steel is cut. A corn crisps extrusion production line turnkey project that ships with a generic screw build will produce inconsistent expansion across batches.
Die Selection Controls Density, Not Just Shape
The interchangeable die plates determine more than the visual format of each piece. Die opening diameter and land length govern the pressure drop at the barrel exit, which directly controls expansion ratio and final product density. A snack that must float in milk requires a different die specification than a corn stick destined for a seasoned bag. Matching die geometry to the target texture is part of the configuration work that happens before production begins. [NEED_CITE: die land length and expansion ratio in twin-screw extrusion]
Reading the Power and Energy Specs Against Your Site Reality
The listed electrical power values distinguish between electricity-heated and gas-or-diesel-heated configurations, but the basis for each figure must be confirmed against your chosen line capacity and dryer length. A multi-layer dryer running on steam will pull far less electrical load than an electrically heated unit, yet it demands a boiler and steam piping on site. Voltage and frequency must be locked in before the control panel is wired — a 380V/50Hz panel shipped to a 440V/60Hz region will not start without a costly transformer or rewinding. Siemens motors and Delixi or Delta inverters are specified, but the control language on the HMI must be confirmed so that local operators can read alarms without translation delays.
The Cost of Mismatched Stations Down the Line
When the extruder is sized correctly but the dryer or flavouring drum is not, product piles up between stations and moisture content drifts outside specification. I have walked into plants where a properly configured twin-screw extruder was feeding a dryer that could only handle two-thirds of the output, forcing the entire line to run below capacity. [NEED_CITE: throughput imbalance consequences in snack extrusion lines] The buyer had paid for a line that could never reach its quoted throughput because the stations were never balanced as a system.
Why Sourcing the Full Line From One Supplier Changes the Outcome
Every station on this corn crisps extrusion production line turnkey project — mixer, extruder, vibrate cooler, multi-layer dryer, and packing — is configured under one roof so that throughput calculations are reconciled before fabrication. Screw configuration and die design are specified against the buyer’s actual cereal blend and target product density, not copied from a standard build. An in-house testing workshop runs your raw material before the line ships, so expansion, texture, and moisture are validated before you see the equipment on site. Food-grade stainless steel 201 or 304 contact surfaces are used across all product zones. Energy source options — electricity, gas, diesel, or steam — let the dryer and roaster be matched to whatever utility infrastructure your facility already has.
Documentation & Verification
- Line layout showing throughput calculation at each station from mixer through packing
- Screw element arrangement and die plate record matched to your cereal blend
- Trial run report on your raw material conducted in the testing workshop
- Electrical schematic confirming voltage, frequency, and control language for your site
- CE declaration of conformity in electronic format for import clearance
- Operation and maintenance manual in English with wear parts list
Installation, Commissioning & Support
- Foundation and floor space plan reflecting the full station footprint and utility drops
- Dedicated circuit sizing for the extruder motor and chosen heating energy source
- Separate station assembly with belt and piping connections verified on site
- First-run parameter tuning using your cereal blend to confirm expansion and density
- Operator training covering screw changeover, die swap, and HMI alarm response
- Wear parts list for screws, dies, and seals with reorder part numbers
What to Include With Your Inquiry
Send the exact cereal blend composition and moisture range you plan to run, the target product format and bag weight, and your site voltage and frequency. Include the available energy source — electricity, gas, diesel, or steam — and the floor area and ceiling height of the production hall. If you have existing upstream or downstream equipment, note the interface points so the line layout accounts for them.
Frequently Asked Questions
Q: How is output capacity verified on my actual raw material?
A: Your cereal blend is run in our in-house testing workshop before shipment. We document expansion ratio, product density, and moisture at the extruder discharge, then adjust screw configuration and barrel temperature until the target specification is met. The trial run report ships with the line.
Q: How are screw configuration and die design selected for my product?
A: We match screw element arrangement and die geometry to your cereal blend’s starch gelatinisation behaviour and the target texture. A product that must be light and crisp requires a different screw profile and die land length than a dense corn stick, so each build is specified individually.
Q: How is throughput matched between stations to prevent bottlenecks?
A: Every station — mixer, extruder, cooler, dryer, flavouring, and packing — is sized against the extruder’s validated output on your raw material. Throughput at each point is documented in the line layout, so no single station restricts the rest.
Q: What voltage and control language options are confirmed before production?
A: Voltage, frequency, and HMI language are confirmed during the specification stage and recorded on the electrical schematic. This prevents commissioning delays caused by incompatible power supply or unreadable alarm messages at your site.
Q: What does on-site installation and operator training include?
A: Our engineers assemble each station, connect utilities, and run the first production batches with your operators. Training covers screw and die changeover, parameter adjustment on the control panel, and routine maintenance schedules for wear parts.
Related products
-

Twin Screw Corn Puffs Extruder Machine Small Corn Snack Food Extruder Machine
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page -
Twin Screw Extruder for Cheese Puffs Food Stainless Steel Simple Puffed Rice Snack Machine
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Rice Crispies Extruder Machine/Chocolate Corn Flakes Extrusion Plant/wheat Flaking Snacks Production Line
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puff Corn Snacks Food Line Puffed Rice Ball Production Making Equipment Machines
¥10,565.00 Select options This product has multiple variants. The options may be chosen on the product page