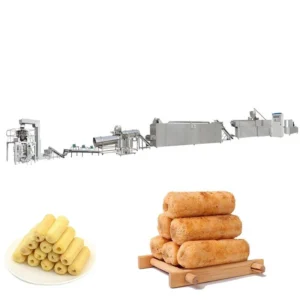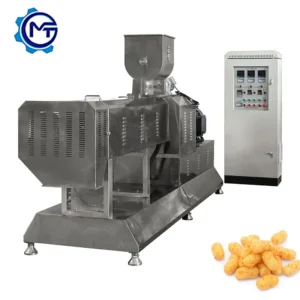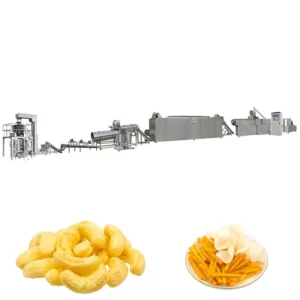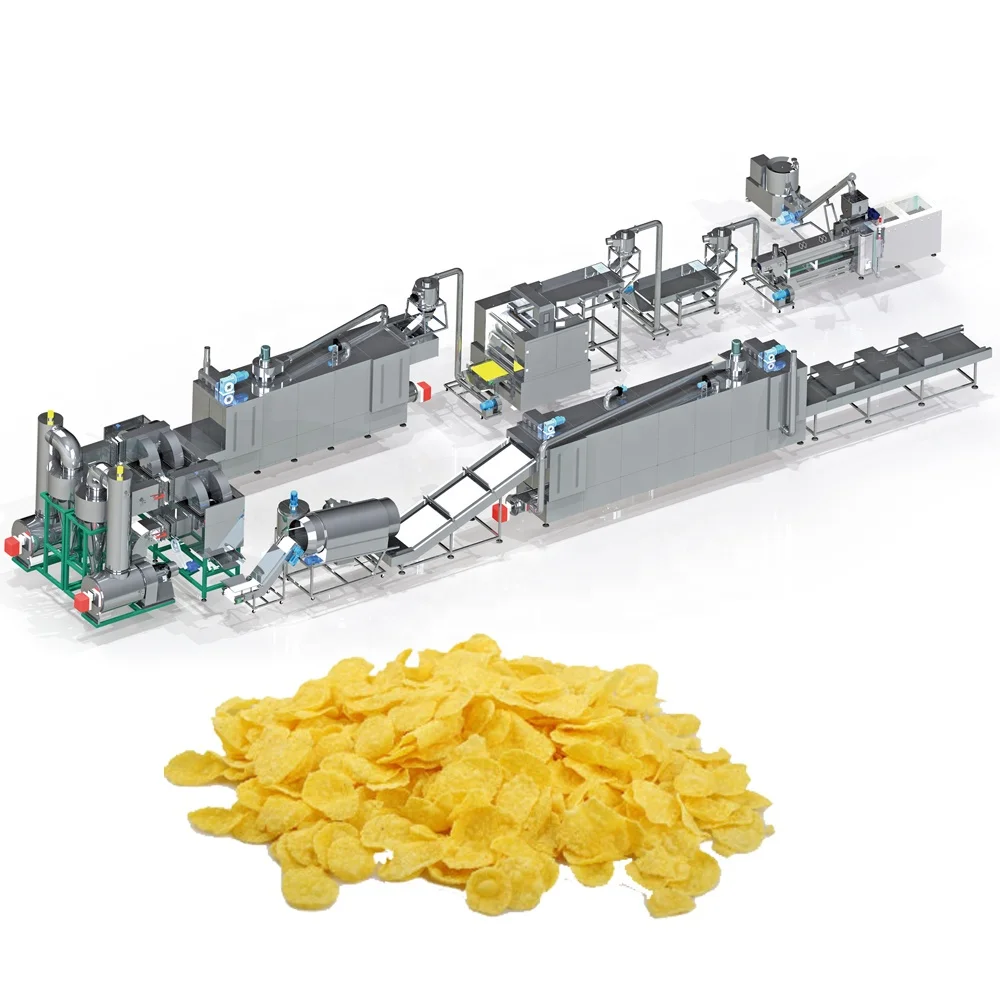
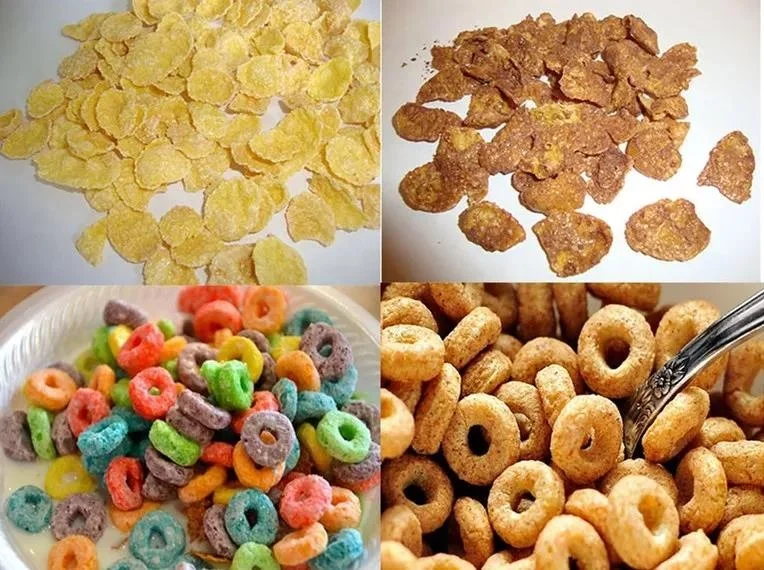
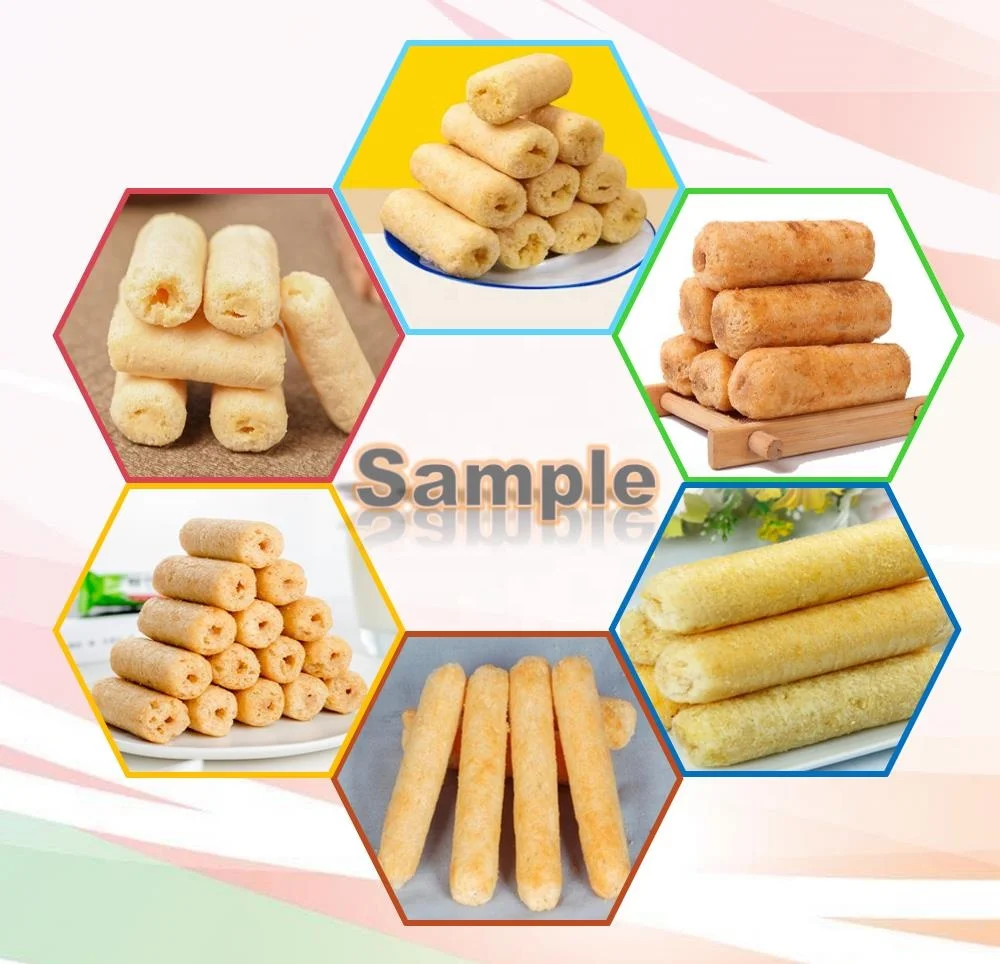
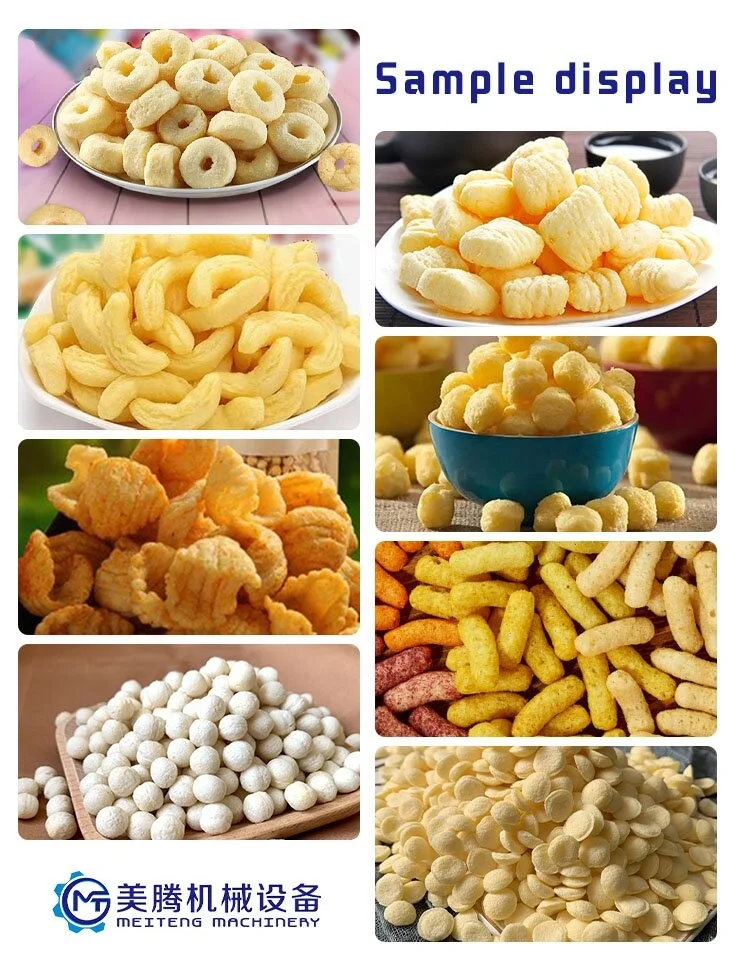
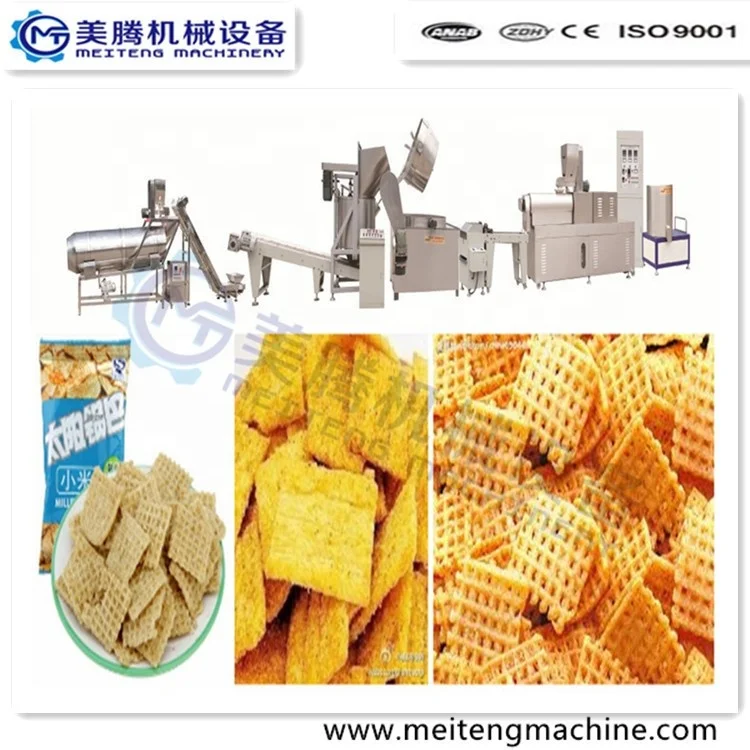
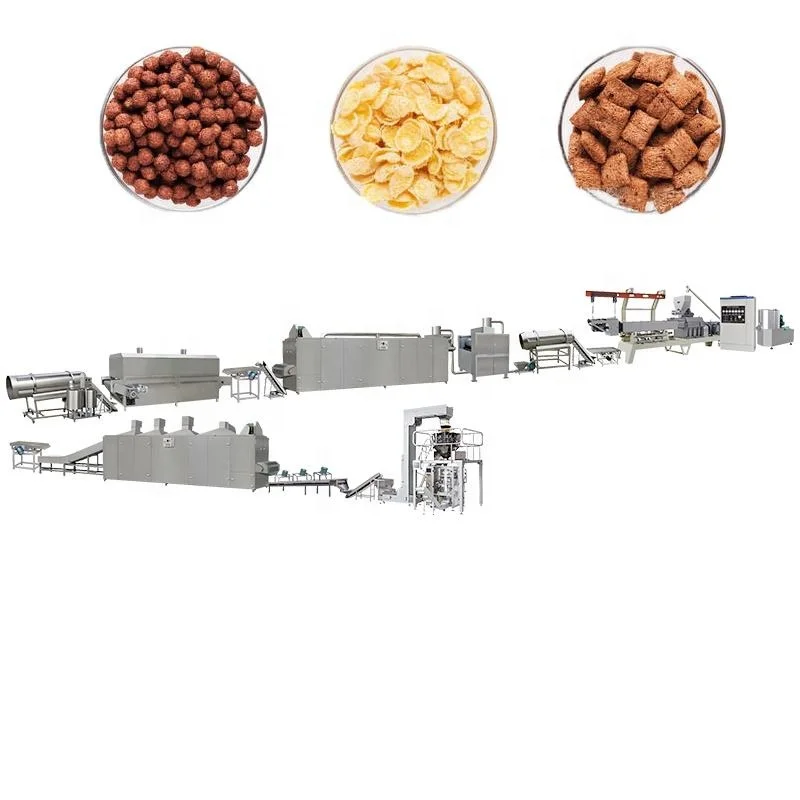
Breakfast Cereal & Corn Flakes Extrusion Line, Twin-Screw, 100–500 kg/h — engineered for corn flakes, granola, and puffed snack production from batching through packing.
Screw configuration and die design are matched to your specific raw material formulation, controlling expansion, density, and final product texture across shapes like rings, loops, balls, and flakes. Multi-energy dryer options (electricity, gas, diesel, steam) are sized to prevent downstream bottlenecks.
- In-house trial runs on your flour or grits before shipment verify actual throughput
- Electrical schematics confirmed to local voltage and frequency standards
Description
Turnkey Line Throughput Matching — Every station from batching to packing is sized against the extruder’s real output on your specific corn or grain formulation, so the line runs at the rate we quote, not a catalog maximum that disappears on your factory floor.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Breakfast Cereal & Puffed Snack Extrusion Line |
| Extruder Type | Twin-screw (double screw) extruder |
| Output Capacity | 100–500 kg/h (basis not stated in source — confirm raw material, moisture content, and product format) |
| Screw Configuration | Interchangeable screw elements matched to product profile |
| Raw Materials | Corn, rice, millets, wheat, oat, barley, buckwheat, brown rice |
| Raw Material Form | Powder (flour) or grits |
| Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (via die change) |
| Energy Source Options | Electricity / Gas / Diesel / Steam |
| Voltage & Frequency | 380 V / 50 Hz (three-phase); 220 V / 50 Hz (single-phase); configurable to local standard |
| Rated Power | ~100 kW (electric heating) / ~50–60 kW (gas or diesel heating) |
| Control System | Electricity control box with inverter (Delixi or Delta); motor: Siemens (China) or equivalent |
| Material of Construction | Food-grade stainless steel 201 / 304 |
| Dryer | Multi-layer belt dryer, length and layer count designed per product |
| Flavoring System | Semi-automatic or automatic; supports sugar, oil, and powder seasoning |
| Line Stations | Mixer → Extruder → Vibrate Cooler → Roasting Machine (Dryer) → Packing Machine |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn flake breakfast cereal | Corn grits or corn flour, toasted and flaked through extrusion and drying |
| Granola and multi-grain clusters | Oat, wheat, barley blends with nuts or dried fruit inclusions |
| Fortified breakfast cereal | Vitamin- and mineral-enriched grain flour blends for nutrition programmes |
| Puffed extruded snacks | Rice, corn, or millet flour shaped into balls, rings, loops, sticks, or stars |
| Artificial or fortified rice | Rice flour or broken rice reconstituted into uniform grain shapes |
| Infant and nutritional cereal powder | Pre-cooked grain blends ground after extrusion for instant porridge |
Why "500 kg per Hour" Means Nothing Without Your Raw Material
The only capacity number that matters is what the breakfast cereal corn flakes production line turnkey actually runs on the flour or grits you will feed it.
I spent two weeks in a Southeast Asian plant watching a corn flake line jam because the screw profile had been specified on standard yellow corn grits at 14 percent moisture, while the buyer was running local high-moisture broken corn that refused to gelatinize at the same barrel temperatures. The extruder was rated for the headline throughput, yet the real output on that material sat well below it, and every downstream station — the dryer, the cooler, the flaking rolls — had been sized to the catalog figure rather than the actual one. A breakfast cereal corn flakes production line turnkey must be validated on your formulation before the machines leave the factory, not after they arrive and the first batch fails to expand. [NEED_CITE: starch gelatinization temperature range for corn and rice grits in twin-screw extrusion]
Screw Profile and Die Geometry Define the Flake, Not the Motor
The twin-screw extruder at the heart of this line uses interchangeable screw elements that are rearranged for each product target. For corn flakes, the screw profile must generate enough shear to fully gelatinize the starch while keeping the dough plasticity high enough for downstream flaking. A die orifice sized too small produces thin strands that shatter under the flaking rolls; sized too large, the pellets stay soft and stick to the rolls. We record the exact screw element sequence and die bore diameter used during the trial run so you can reproduce the same flake texture on every production day.
Drying Is Where Capacity Actually Bottlenecks
The multi-layer belt dryer is the longest station on the line physically and the one most often undersized. Corn flakes entering the dryer carry significant surface moisture from the extrusion and flaking stages, and they need a specific residence time at controlled temperature to reach the target crunch without scorching. If the dryer belt length or layer count is calculated on a theoretical throughput rather than the real extruder output, you end up with either under-dried flakes that go limp in the bag or a dryer running at maximum belt speed that still cannot keep up. We match the dryer footprint to the confirmed extruder capacity so the breakfast cereal corn flakes production line turnkey holds its rate hour after hour. [NEED_CITE: moisture migration rates in multi-layer belt drying for extruded cereal products]
What the Voltage and Heating Choices Mean for Your Utility Bill
The line offers electric, gas, diesel, and steam heating options for the dryer and roasting stages. Electric heating draws close to 100 kW at the extruder alone, which demands a dedicated transformer and heavy-gauge cabling — viable where industrial electricity tariffs are low but costly where they are not. Gas or diesel cut the rated electrical draw to roughly 50–60 kW and shift the energy expense to fuel, which may be cheaper per unit of heat in your region. The control panel ships with either a Delixi or Delta inverter, and the HMI language, voltage, and frequency are configured to your local grid before dispatch so the first power-on is not a debugging session.
When the Wrong Configuration Costs You Weeks
A generic screw build copied from a different cereal application leaves you with flakes that either crumble in the packaging or refuse to crisp in milk. I have walked into plants where the flavoring drum was rated for a lower throughput than the extruder, forcing the entire line to idle while the drum caught up — a bottleneck that does not appear in any brochure. If the dryer layers are too few for the actual moisture load, operators crank the temperature, scorching the surface while the core stays damp, and the shelf-life complaint arrives weeks later. These are not equipment failures; they are configuration failures, and they are preventable with a proper trial run on your raw material before the line is crated for export. [NEED_CITE: impact of screw element arrangement on expansion index in cereal extrusion]
Why This Line Comes From One Supplier, Not Five
Every station — mixer, extruder, vibrate cooler, roasting dryer, flavoring system, packing — is sourced from the same facility, so throughput is balanced across the chain rather than guessed from separate vendor data sheets. The screw configuration and die design are specified to your raw material and target product shape, not pulled from a generic build library. An in-house testing workshop runs your actual flour or grits through the extruder before shipment, producing a trial report that confirms capacity, texture, and expansion on your formulation. Food-grade stainless steel 201 or 304 contact surfaces are used throughout, and the electrical schematic, voltage confirmation, and control language are documented before the control cabinet is closed. CE and ISO documentation ships with the line so your local import and safety inspection has the paperwork it requires.
Documentation & Verification
- Line layout drawing showing throughput matching between every station on the cereal line
- Screw element sequence and die bore record specific to your grain formulation
- Trial run report on your raw material produced in the in-house testing workshop
- Electrical schematic with voltage, frequency, and control language confirmed for your grid
- CE declaration of conformity and ISO certificate for customs and local safety audit
- Wear parts list with part numbers for screws, dies, and barrel liners
Installation, Commissioning & Support
- Foundation plan referencing the twin-screw extruder weight and vibration isolation points
- Dedicated power circuit sized to the confirmed 100 kW electric or 60 kW gas/diesel heating load
- Modular station delivery allowing the multi-layer dryer to be assembled inside standard ceiling heights
- First-run parameter log covering barrel temperatures, screw speed, and dryer belt speed on your material
- Operator training on die changeover between flake, ring, and ball shapes using the supplied die plates
- Scheduled wear parts shipment covering screw elements and die inserts for the first production cycle
What We Need to Size Your Line Accurately
Share the exact grain variety and moisture content you plan to run, whether that is yellow corn grits at a known percentage or a multi-grain flour blend. Tell us your target daily output and the shift pattern you intend to run, along with the available floor space and ceiling height in your production hall. Confirm your local voltage, frequency, and the control panel language your operators need. If you already have upstream batching or downstream packing equipment, send the model and capacity so we can match the interface points and avoid throughput gaps across the breakfast cereal corn flakes production line turnkey.
Frequently Asked Questions
Q: How is output capacity verified, and on which raw material is the 100–500 kg/h range based?
A: The capacity range depends on your specific grain type, moisture content, and target flake or puff shape. We run your actual raw material in our in-house testing workshop before shipment and issue a trial report that records the real throughput, expansion index, and texture achieved. That report becomes the capacity baseline for your line, not a generic catalog figure.
Q: Can voltage, frequency, and control panel language be configured for my country?
A: Yes. The control system is configured to your local voltage and frequency — whether 380 V / 50 Hz, 440 V / 60 Hz, or another standard — before the cabinet ships. The inverter brand (Delixi or Delta) and the HMI language are confirmed during the quotation stage so your operators see instructions in their working language on day one.
Q: How do I choose between electricity, gas, diesel, or steam heating for the dryer?
A: The decision comes down to your local energy costs and available infrastructure. Electric heating draws higher electrical load but simplifies installation. Gas or diesel lowers the electrical demand and may reduce per-unit energy cost where fuel is inexpensive. Steam is preferred when your plant already operates a boiler. We model the operating cost for each option against your confirmed extruder throughput.
Q: What spare wear parts should I order with the initial line?
A: Screw elements, die plates, and barrel liners are the primary wear items in a twin-screw cereal extruder. We provide a wear parts list with quantities calculated for your planned annual running hours, and replacement parts are manufactured to the same configuration record so they install without re-commissioning the line.
Q: How does the layout prevent the dryer or flavoring station from bottlenecking the extruder?
A: Every downstream station is sized against the confirmed extruder output from the trial run, not a theoretical maximum. The multi-layer dryer belt length, the vibrate cooler area, and the flavoring drum volume are all calculated to handle the actual throughput, so no single machine forces the line to idle or slow down during continuous production.
Related products
-

Corn Puff Processing Line with Mixer Fryer Baking Oven Automatic High Productivity Grain Products Snack Making Machine
¥8,300.00 Select options This product has multiple variants. The options may be chosen on the product page -

New Puffed Snack Food Machine Production Line Corn Flake Puff Corn Making Machine Twin Screw Extruder 100-500kg/h Capacity Food
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puff Corn Snacks Food Line Puffed Rice Ball Production Making Equipment Machines
¥10,565.00 Select options This product has multiple variants. The options may be chosen on the product page -
New Condition Automatic Corn Puff Snacks Food Extruder Cheese Ball Making Machine Plant
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page