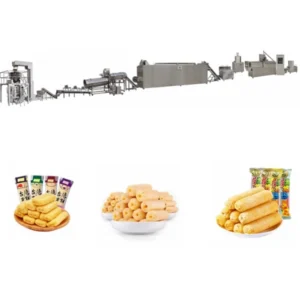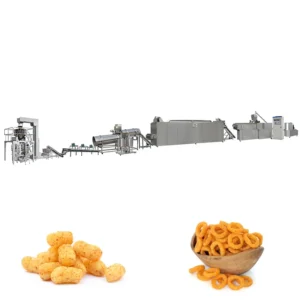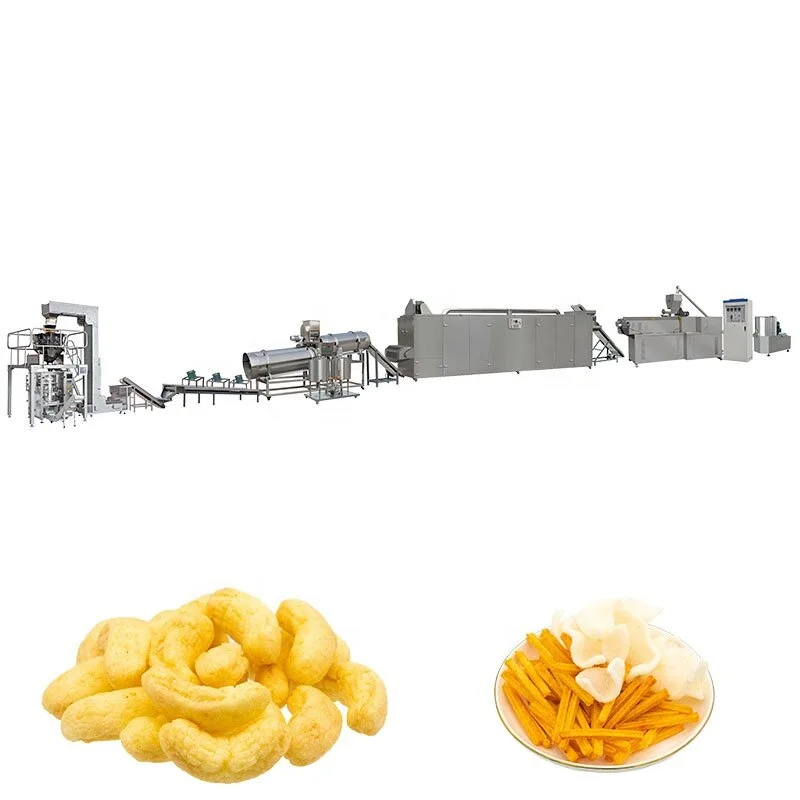
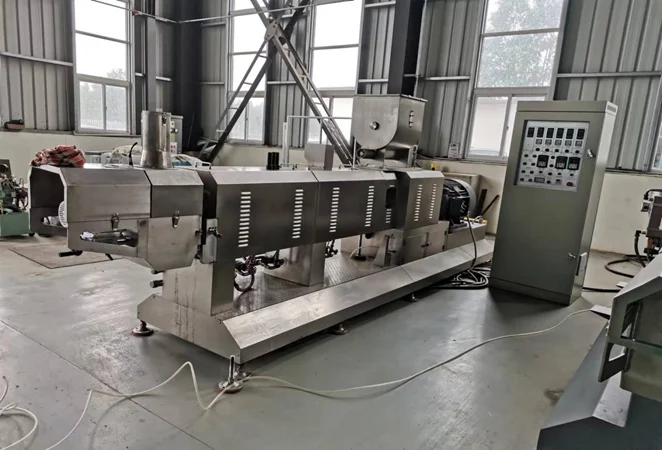
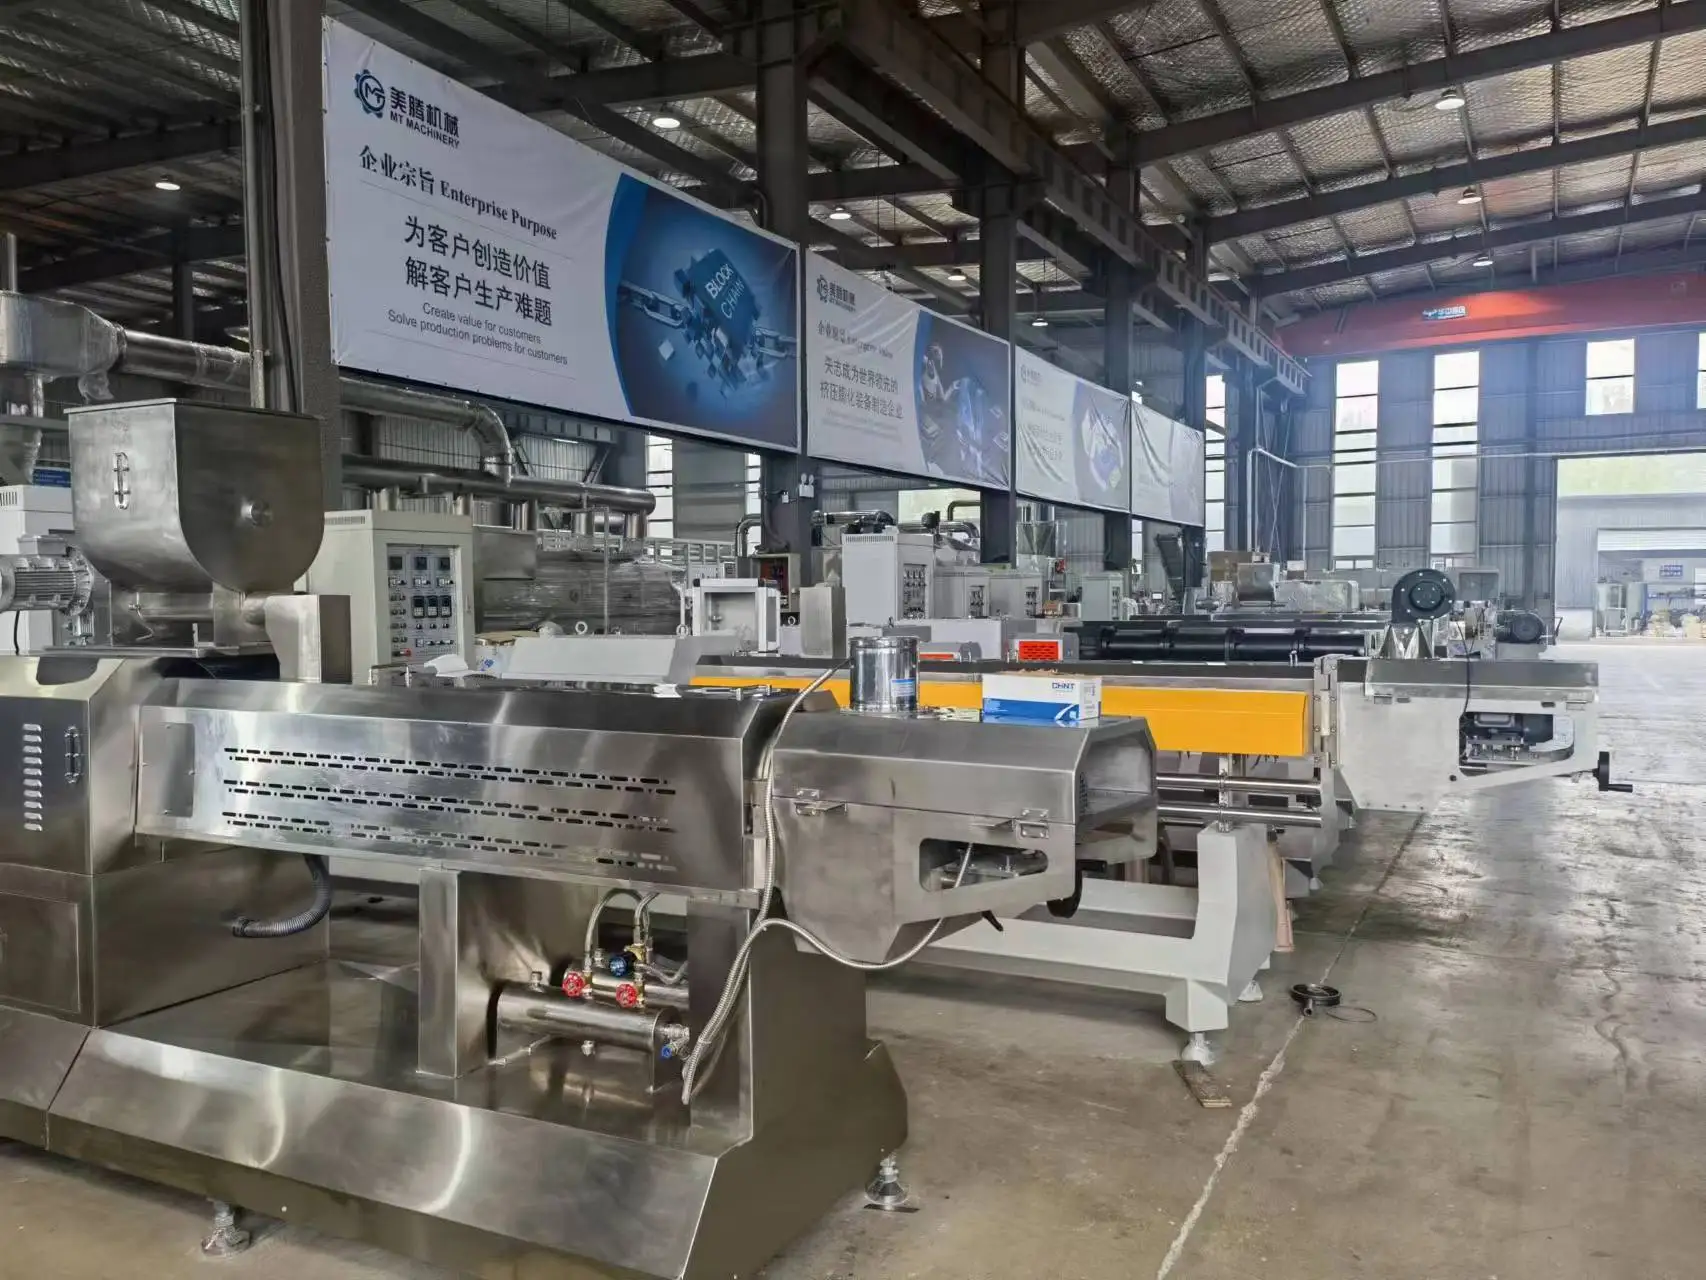
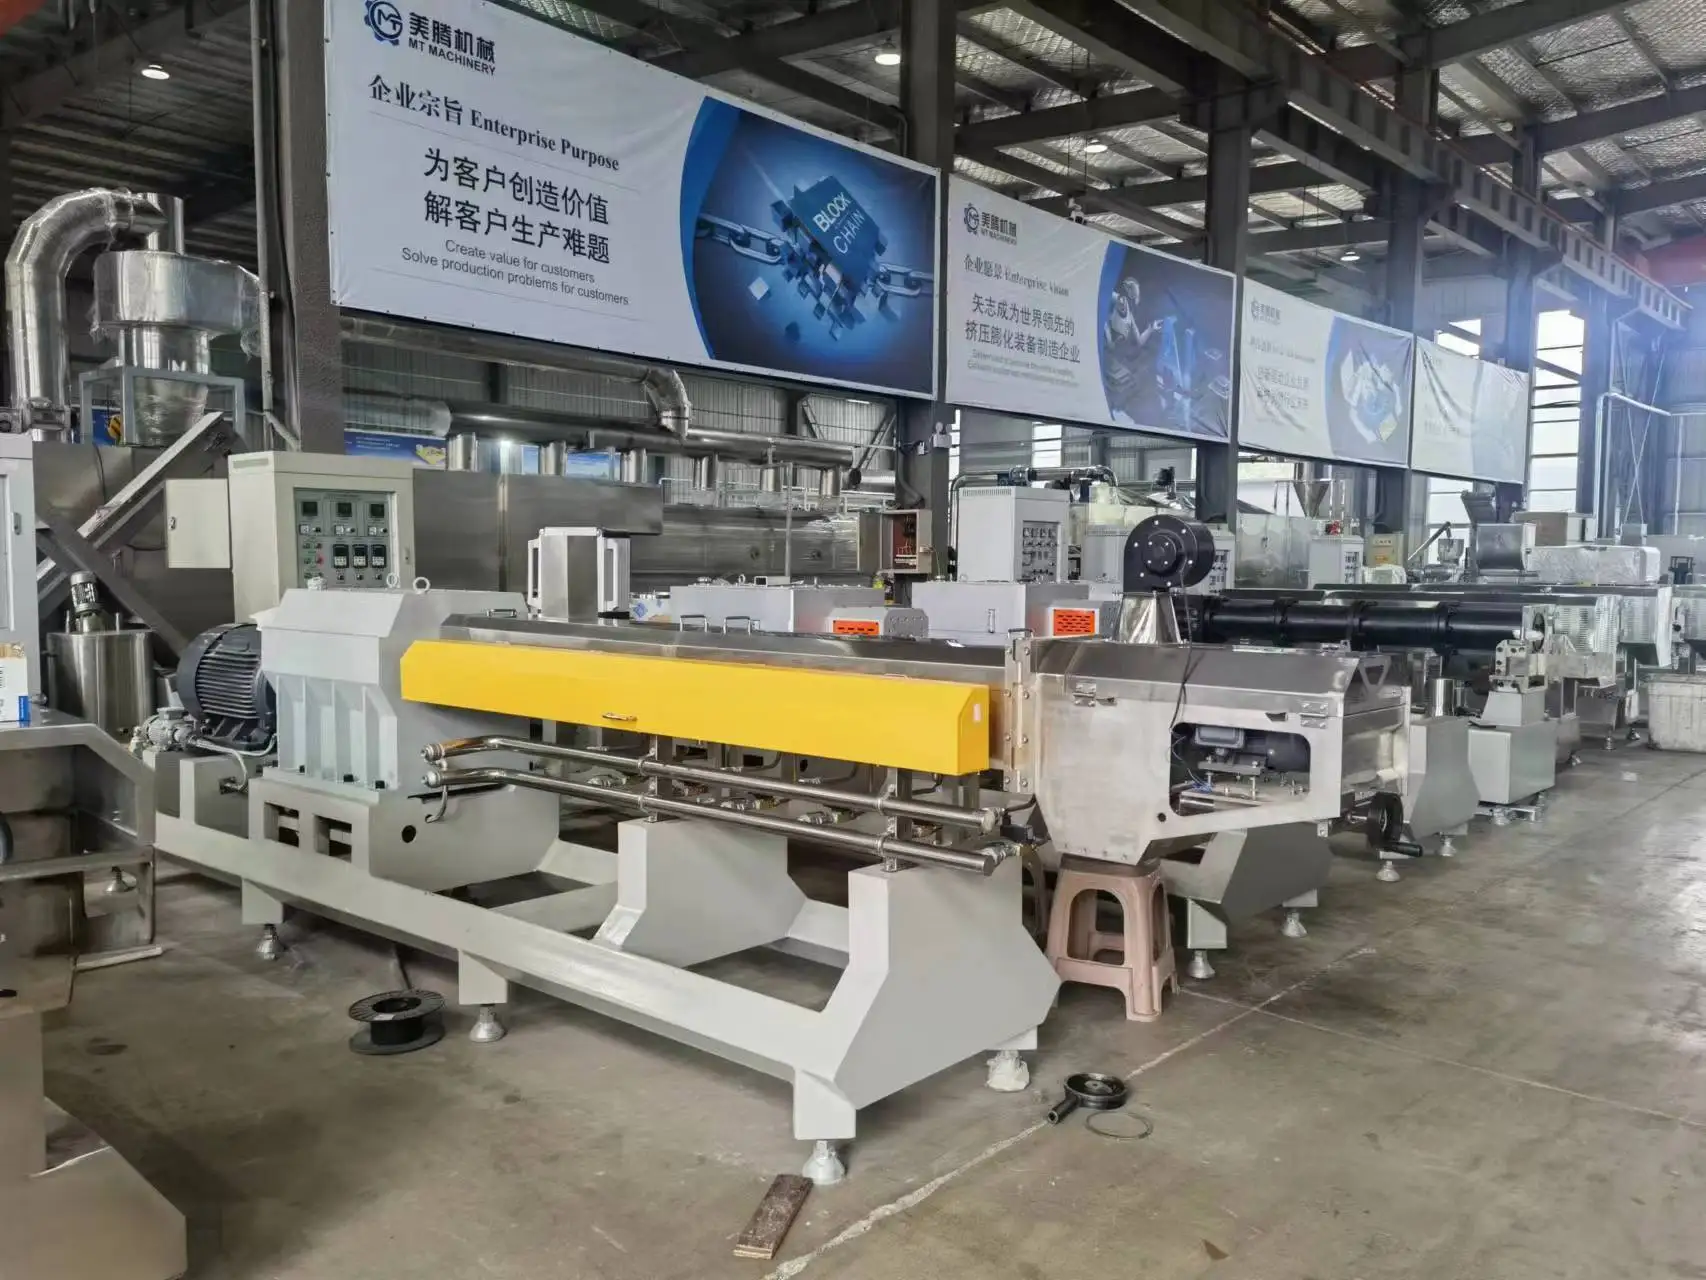
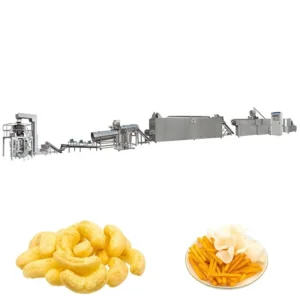
Puffed Snack Food Extrusion Line, Twin-Screw, Automatic PLC Control — configured for rice flour, corn, and maize-based extruded snacks with matched throughput from mixing through drying and flavoring.
Screw configuration and die design are specified to your raw material and target snack density, while the multi-layer dryer is sized in length and layer count to hold the required moisture profile and residence time.
- Complete line under one supplier with throughput verified across every station
- In-house trial run on your raw material before shipment
- On-site installation, commissioning, and operator training included
Description
Turnkey Line Accountability — every station from mixing to packing is sized and supplied by a single manufacturer, eliminating the throughput mismatches that occur when a snack line is assembled from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Puffed Snack Food Extrusion Line |
| Screw Type | Twin-screw (double screw) |
| Line Stations | Mixing, extruding, shaping, cutting, drying, flavoring |
| Control System | Automatic PLC controlled (PLC brand and language options to be confirmed) |
| Output Capacity | High productivity (basis not stated in source — confirm raw material, moisture, target product shape) |
| Dryer Type | Multi-layer (length and layer configurable based on product) |
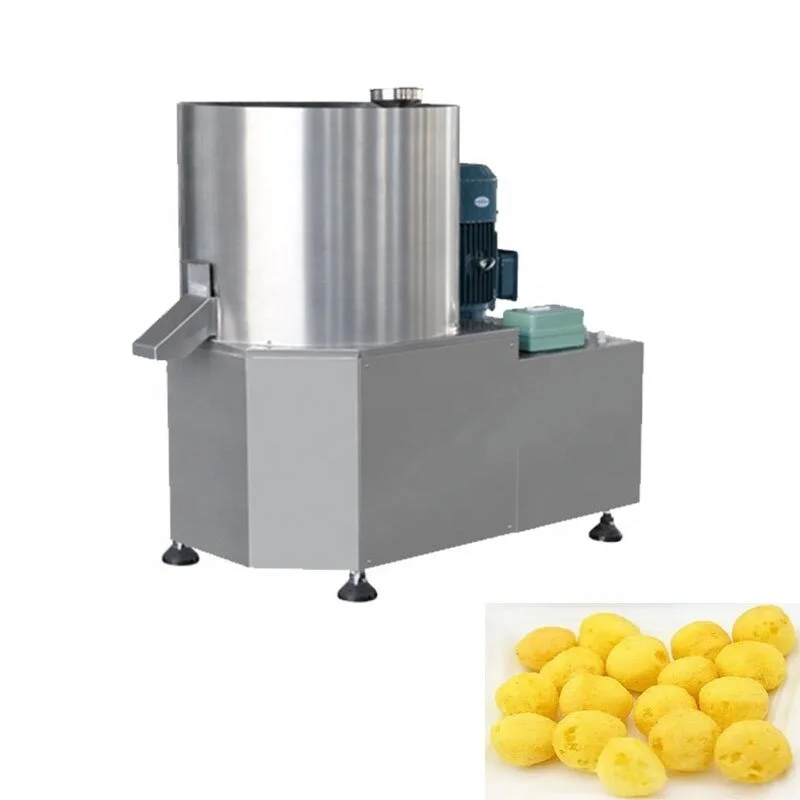
| Flavoring System | Semi-automatic or automatic options; handles sugar, oil, and powder seasoning |
| Extruder Capability | Puffed snacks, fried snacks, artificial rice, special products (via screw and die change) |
| Voltage & Frequency | Target market voltage and frequency to be confirmed |
| Certification | CE, ISO (certificate scope and validity to be confirmed) |
| Warranty | 24 months, lifetime service (verify against current manufacturer policy) |
Application Suitability
| Application | Material or Output |
|---|---|
| Puffed rice snacks | Rice flour, rice grits |
| Puffed corn snacks | Corn grits, maize flour |
| Maize-based extruded snacks | Maize, corn blends |
| Artificial rice | Rice flour, starch blends |
| Core-filled snacks | Flour blends, cream or chocolate filling |
| Fried snack pellets | Potato starch, wheat flour, corn starch |
Why Nominal Line Capacity Fails on Your Actual Recipe
A puffed snack extrusion production line turnkey is only as productive as its most constrained station, and nominal figures rarely reflect what happens when your specific raw material hits the barrel.
In my time commissioning lines across different climates and grain supplies, I have watched extruders that ran smoothly on standard corn grits completely stall or produce under-expanded product when a buyer switched to a local maize variety with different starch composition. The dryer then receives product at the wrong moisture level, the flavoring drum cannot coat evenly, and the packing station sits idle waiting for output. The whole line rhythm breaks down from a single upstream mismatch [NEED_CITE: starch gelatinisation behaviour across grain varieties]. This is why a line configuration must be built around the buyer’s confirmed recipe rather than a generic datasheet figure.
Matching Extruder Output to Downstream Stations
The twin-screw extruder at the heart of this puffed snack extrusion production line turnkey is configured with screw geometry and die design matched to the buyer’s raw material and target snack shape. Barrel sections are zoned for independent temperature control, so operators can manage shear and moisture profile through the barrel length. When the extruder produces a consistent output density, the downstream shaping and cutting stations receive uniform feed, which is the precondition for stable throughput across the entire line.
Dryer and Flavoring Throughput Alignment
A multi-layer dryer with configurable length and layer count allows the residence time to be set according to the moisture profile exiting the extruder. If the dryer is undersized relative to extruder output, product leaves with residual moisture that causes staling or uneven seasoning adhesion. The flavoring system — available in semi-automatic or fully automatic configuration — must then receive product at the correct surface moisture to hold sugar glaze, oil spray, or powder seasoning. When all three stations are throughput-matched by one supplier, the puffed snack extrusion production line turnkey avoids the bottleneck where one vendor blames another for lost output [NEED_CITE: industrial dryer residence time calculation for extruded snacks].
Reading the Specification Sheet Correctly
Twin-screw extrusion provides a wider processing window than single-screw designs, meaning the line can handle raw materials with varying fat, moisture, and particle size without frequent screw changes. The screw configuration itself — the arrangement of conveying, kneading, and reverse elements — determines shear intensity and residence time inside the barrel, which directly controls expansion ratio and final snack density. Die design governs the cross-section shape and the pressure drop at the exit, influencing whether the product expands uniformly or develops internal voids. Automatic PLC control maintains barrel temperature and screw speed within tight bands, reducing batch-to-batch variation that manual operation introduces over a long production run.
The Cost of Undersized Supporting Equipment
When a dryer is quoted based on extruder nominal output but the buyer’s raw material requires longer residence time, the line must slow down to dry properly — effectively running below the paid-for capacity every shift. I have seen operators forced to bypass the dryer’s final zone or increase line speed to meet targets, sending product to packing with moisture levels that invite mold growth in humid storage. Similarly, a flavoring drum that cannot keep pace creates a pile-up of unseasoned product that must be re-run or discarded. These losses compound quietly and are rarely traced back to the original line configuration decision [NEED_CITE: post-extrusion moisture targets for shelf-stable snack packaging].
Why Source the Full Line from One Supplier
Every station — mixing, extruding, shaping, cutting, drying, and flavoring — is designed to hold the same throughput, so no single piece of equipment constrains the others. Screw and die configuration is specified against the buyer’s confirmed raw material rather than copied from a generic build. An in-house testing workshop runs trial production on the buyer’s actual material before shipment, catching expansion or density issues before the line leaves the factory. Voltage, frequency, and PLC language are confirmed before production begins, so the control panel matches the local electrical grid and operator language on arrival. The same engineering team handles layout design, installation, commissioning, and ongoing wear parts supply, keeping accountability in one place.
Documentation & Verification
- Line layout showing throughput calculation for each station against your target output
- Trial run report on your specific rice or corn flour before factory dispatch
- Screw and die configuration record matched to your snack shape and density target
- Electrical schematic confirming voltage, frequency, and PLC language for your site
- CE and ISO certificate copies with scope covering food extrusion machinery
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Utility plan covering PLC power circuit and multi-layer dryer heating zones for your site voltage
- Foundation and floor loading layout matching the full line footprint including dryer length
- Barrel and screw assembly sequence with torque settings for the twin-screw extruder
- First-run parameter logging across all barrel zones and dryer temperatures with your material
- Operator training on die changes, screw swaps, and PLC fault diagnosis in your preferred language
- Wear parts inventory covering screws, dies, and dryer belt sections for the first production cycle
Before You Request a Quotation
To configure a line that holds capacity on your actual recipe, share your raw material specification including flour type, particle size, and fat content, along with the target snack shape, density, and required output per shift. Confirm your factory voltage and frequency, available floor space and ceiling height, and whether existing upstream or downstream equipment needs to integrate with the new line.
Frequently Asked Questions
Q: How is line capacity verified against my specific raw material and recipe before shipment?
A: Your raw material is shipped to the in-house testing workshop where the configured twin-screw extruder, dryer, and flavoring stations run a trial at line speed. A trial run report documents throughput, expansion ratio, moisture at each stage, and final snack density against your specification before the line is approved for dispatch.
Q: How do you ensure dryer and flavoring station throughput matches the extruder output?
A: The multi-layer dryer length and layer count are sized based on the moisture profile your material produces at the extruder exit. The flavoring drum capacity and seasoning application rate are then calculated against that confirmed extruder throughput, so every station is rated to hold the same output without creating a bottleneck.
Q: What screw and die configuration will be specified for my target snack shape and density?
A: The screw element arrangement — conveying, kneading, and reverse sections — is designed to deliver the shear and residence time your raw material requires. The die aperture and land length are then matched to produce the cross-section shape and expansion ratio your market expects, and both are documented in the configuration record.
Q: Can voltage, frequency, and PLC control language be confirmed to match my factory before production begins?
A: Yes. The electrical schematic, motor nameplate ratings, and PLC interface language are confirmed with you during the specification stage, before production starts. This avoids commissioning delays caused by mismatched voltage or control panels in a language your operators cannot read.
Q: What does the on-site installation, commissioning, and operator training process include?
A: Engineers supervise mechanical assembly, utility connection, and first-run parameter setting using your actual raw material. Operators are trained on die and screw changes, PLC operation, routine maintenance, and fault diagnosis. A wear parts list with replacement intervals is handed over for your maintenance planning.
Related products
-

Automatic Puffed Food Snack Machine Electric Corn Puffs Snacks Making Machinery New Condition Flavorful Puff Snack Production
¥7,550.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Corn Crisps Extruder Production Machine for Maize Chips and Corn Sticks New Condition
¥8,000.00 Select options This product has multiple variants. The options may be chosen on the product page -
New Stainless Steel Automatic Puffed Rice Flour Snacks Making Machine High Productivity Multi-function
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Rice Crispies Extruder Machine/Chocolate Corn Flakes Extrusion Plant/wheat Flaking Snacks Production Line
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page