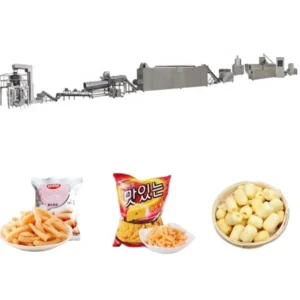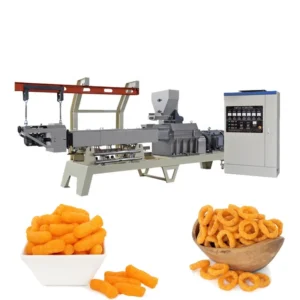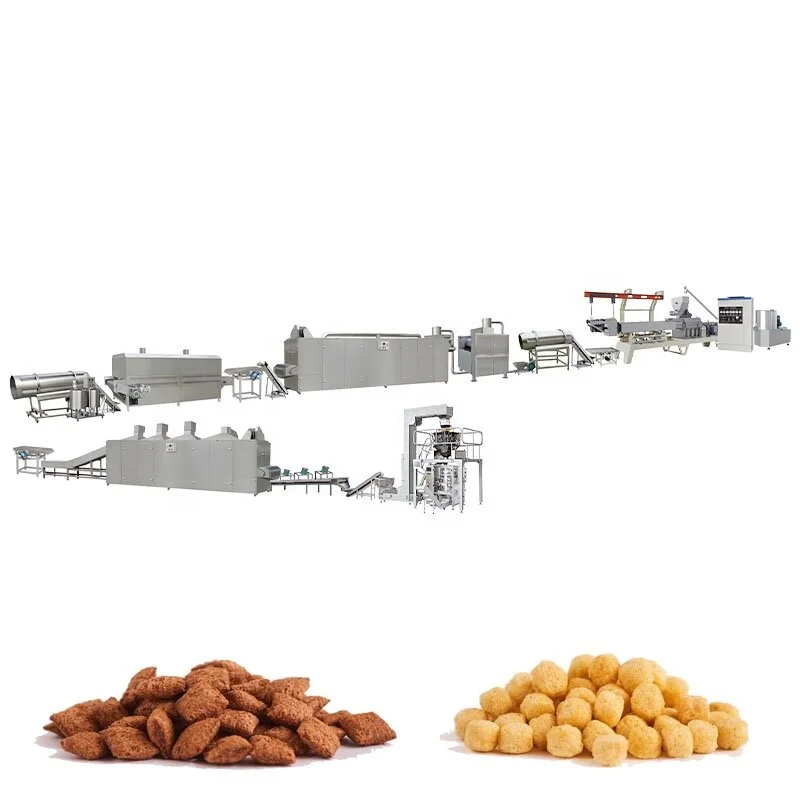
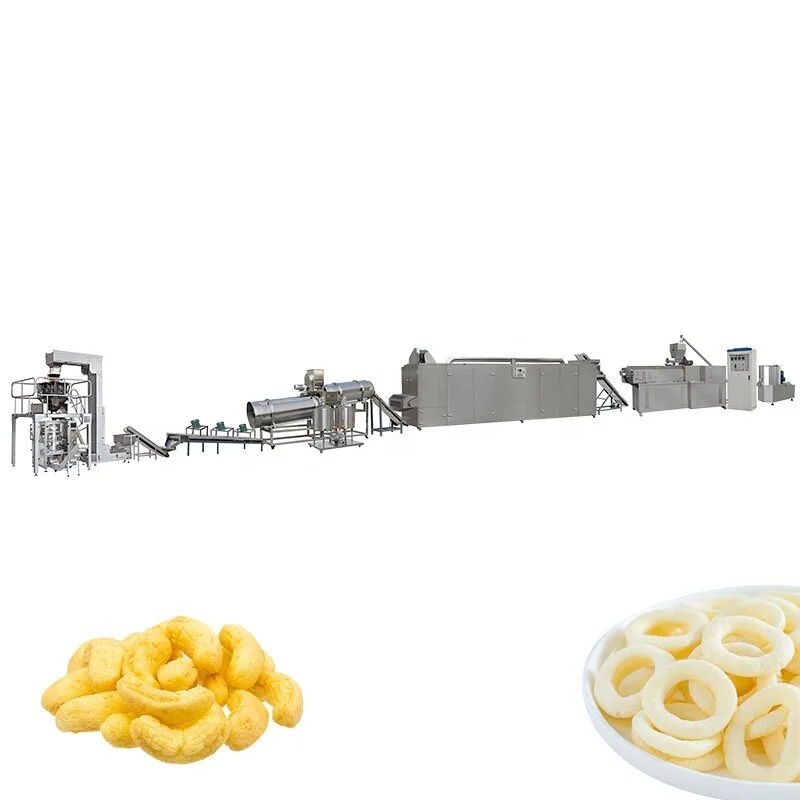
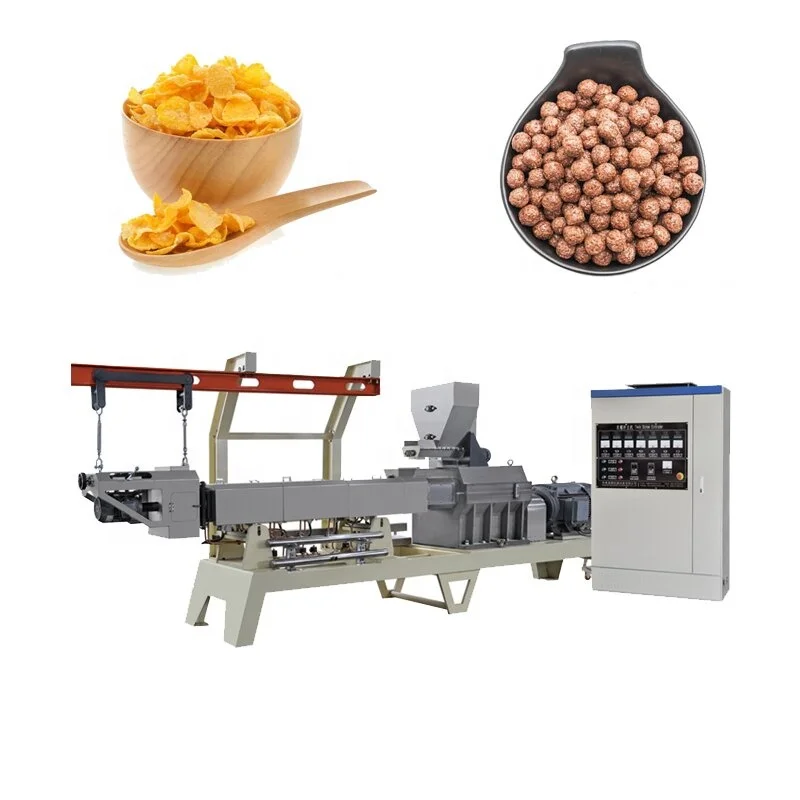
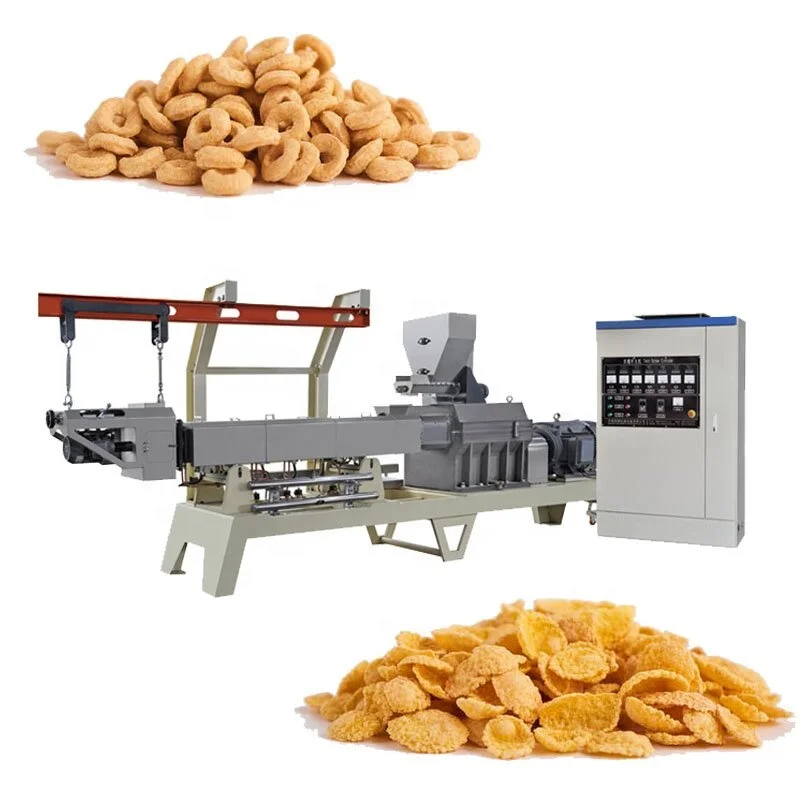
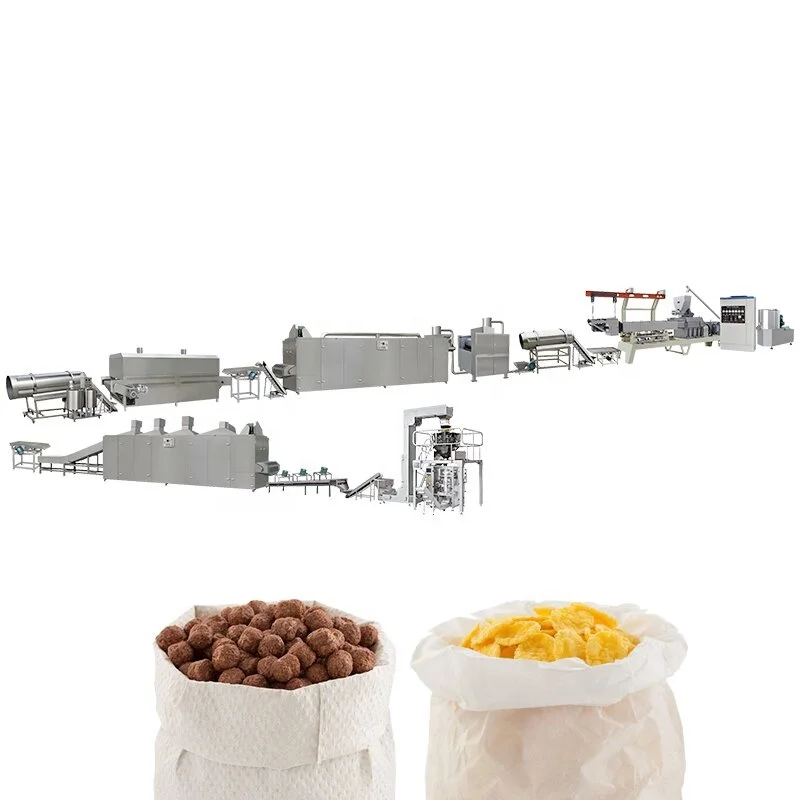
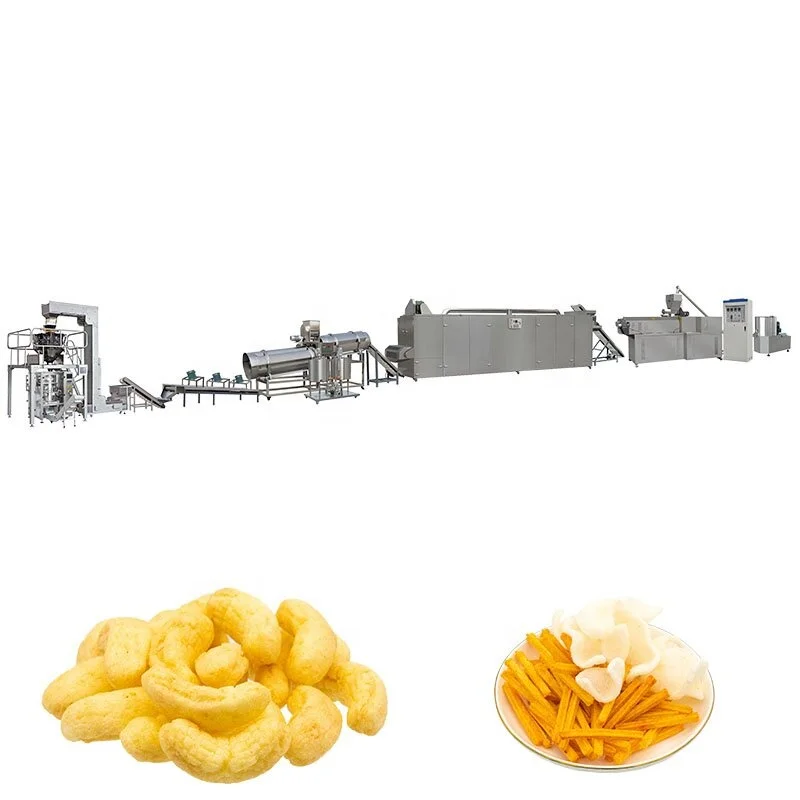
MT65 / MT70 / MT85 Twin Screw Puffed Snack Extrusion Line, 38CrMoAL Nitriding Screws, Delta Inverter Control — configured from batching through extrusion, drying, seasoning to cooling as one integrated project.
- Screw configuration and die design specified to your raw material and target puff density
- Five-layer mesh belt dryer with electric, gas or oil heating options, sealed structure for consistent moisture removal
- Interchangeable moulds for rings, stars, flowers, wheels and custom shapes
Trial runs on your actual raw material completed in our testing workshop before shipment, with full documentation and on-site commissioning included.
Description
Station-Throughput Matching — every mixer, extruder, dryer and seasoning drum in this twin screw puffed snack extrusion line is sized against the same hourly mass flow, so no single machine bottlenecks the next.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Puffed Snack Food Extrusion Line |
| Model | MT65 / MT70 / MT85 |
| Screw Type | Co-rotating twin screw, sectional modules |
| Screw Material | 38CrMoAL alloy, nitriding process |
| Main Motor | SIEMENS (China) |
| Inverter | Delta |
| Control System | Visible auto-temperature control; independent speed adjustment on feeding, extrusion and cutting |
| Feeding System | Food-grade stainless steel twin screw feeder |
| Gearbox | Automatic lubrication |
| Cutting System | Die-head-mounted rotary knife, V-belt drive |
| Barrel & Screw Cleaning | Self-cleaning design, no discharge required between material changes |
| Output Capacity (MT65) | 100–150 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Installed / Real Power (MT65) | 70 kW / 40 kW |
| Overall Dimensions (MT65) | 20,000 × 1,200 × 2,200 mm |
| Output Capacity (MT70) | 200–240 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Installed / Real Power (MT70) | 100 kW / 70 kW |
| Overall Dimensions (MT70) | 25,000 × 1,500 × 2,200 mm |
| Output Capacity (MT85) | 300–400 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Installed / Real Power (MT85) | 200 kW / 150 kW |
| Overall Dimensions (MT85) | 30,000 × 3,500 × 4,300 mm |
| Mixer Batch Capacity | 80–100 kg per batch |
| Mixer Mixing Time | 30 s – 3 min |
| Mixer Motor Power | 7.5 kW |
| Dryer Structure | Five-layer SUS mesh belt, side guards, sealed body |
| Dryer Max Temperature | 160 °C |
| Dryer Energy Options | Electric / gas / oil |
| Seasoning Drum | φ700 × 3,000 mm, 1.1 kW drive |
| Cooling Belt Width | 450 mm |
| Die Shapes Available | Round, triangle, square, star, flower, wheel, heart, smile, ring, strip, custom |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Direct-expanded ring and star snacks | Corn grits, rice flour, wheat flour blends |
| Heart- and flower-shaped children’s puffs | Corn and oat mixtures at controlled moisture |
| Fortified breakfast cereal pieces | Wheat, rye and multi-grain formulations |
| Wheel- and strip-format extruded snacks | Rice and corn starch bases with minor protein addition |
| Pilot runs for new snack concepts | Customer-supplied raw material tested before shipment |
Why "300 kg/h" Can Mislead Your Entire Layout
A line is only as fast as its slowest station, and extruder nameplate capacity rarely tells you which station that will be.
When I first started accompanying our senior engineers on overseas installations, the most common failure I witnessed was not the extruder itself — it was the dryer downstream choking because its belt width and residence time had been chosen from a catalogue page rather than from the actual output mass flow. The Twin Screw Puffed Snack Extrusion Line avoids this trap by calculating every conveyor, drying zone and coating drum against the same throughput basis [NEED_CITE: throughput matching principles in continuous food processing lines]. If the extruder pushes out a certain kilogram-per-hour figure on a specific grain at a defined moisture level, the five-layer mesh dryer must hold that volume at the required residence time, and the seasoning drum must tumble it without overflow. Skipping this calculation at the quotation stage is what turns a supposedly high-capacity line into a bottlenecked one.
Layout Planning Around the Full Machine Sequence
A turnkey twin screw puffed snack extrusion line starts at the mixer, where an 80–100 kg batch is blended within three minutes, then moves through the screw conveyor into the extruder feed hopper. From there the co-rotating twin screw pushes material through the die, the rotary cutter portions the expanded pieces, and the five-layer mesh belt dryer removes residual moisture before the seasoning drum applies oil and powder. Each hand-off point is designed so that the upstream station never overfeeds the downstream one.
What Happens When Throughput Is Miscalculated
We once supplied a line where the buyer insisted on a larger extruder without upgrading the dryer. During the factory trial on their corn-and-bone-meal formula, pieces left the die correctly but piled up on the dryer belt before moisture could be driven off, producing uneven color and texture [NEED_CITE: effect of insufficient drying residence time on extruded snack quality]. After that experience, our rule became simple: no configuration is finalized until the buyer’s actual raw material has run through the full station sequence in our testing workshop, and the trial report documents throughput at every hand-off.
Reading the Specs That Actually Matter on a Puffed Snack Line
The screw material — 38CrMoAL with nitriding — directly affects how long the modules resist abrasive grain particles before the flight profile degrades and expansion drops off. The Delta inverter covering feeding, extrusion and cutting means operators can fine-tune screw speed independently of cutter speed, which is essential when switching between a dense corn ring and a fragile rice star. Die interchangeability across ten standard shapes plus custom profiles lets one line serve multiple SKUs without buying a second extruder. Finally, the choice between electric, gas or oil heating on the dryer determines both the utility infrastructure the buyer must prepare and the ongoing energy cost per kilogram of finished snack [NEED_CITE: comparative energy costs of electric versus thermal-fluid drying in snack production].
The Hidden Cost of Ignoring Raw-Material Behavior
I still remember the call from a South Asian snack manufacturer: their twin screw extruder had been running corn flour smoothly during our factory test, but the moment they introduced a local rice-and-lentil blend with higher fiber content, the screws slipped and the barrel overloaded. The root cause was that the screw configuration had been set for one formula and never re-validated for the buyer’s actual grain mix. A line that cannot hold stable pressure across the buyer’s recipe range will produce inconsistent puff density, higher reject rates, and unplanned downtime for screw swaps [NEED_CITE: influence of fiber content on twin screw extrusion stability].
Why Sourcing the Complete Line from One Supplier Matters Here
Every station — mixer, conveyor, extruder, dryer, seasoning drum, cooling belt — is engineered under one roof, so throughput calculations use the same mass-flow basis instead of optimistic vendor claims stitched together. Screw configuration and die selection are matched to the buyer’s raw material and target shape before the machine is built, not after it arrives. The in-house testing workshop runs the buyer’s own formula prior to shipment, generating a trial report that documents actual output and product geometry. CE and ISO documentation accompanies every shipment, smoothing customs clearance and local safety audits. On-site installation includes operator training on the Delta inverter interface and self-cleaning procedures, reducing the ramp-up period.
Documentation & Verification
- Line layout drawing with station-by-station throughput calculation for your grain formulation
- Screw module arrangement and die configuration record matched to your target snack shape
- Electrical schematic confirming voltage, frequency and control-panel language before production
- Factory trial report on your raw material documenting output, expansion ratio and moisture
- CE declaration of conformity and ISO certificate for customs and local regulatory filing
- Operation and maintenance manual with wear-parts list specific to your screw and die set
Installation, Commissioning & Support
- Foundation plan accounts for the 20–30 m line length and dryer weight distribution
- Dedicated circuit sized for up to 200 kW installed power on the MT85 configuration
- Extruder arrives with barrel and screw pre-assembled; dryer panels bolt on site
- First-run parameter setting covers barrel temperature zones and Delta inverter speeds
- Operators trained on self-cleaning procedure to avoid material discharge between recipes
- Spare screw modules and die plates shipped with initial order to cover first replacement cycle
Preparing Your Inquiry
To move from general interest to a firm layout proposal, share the grain or flour types you plan to run, the moisture range you can control at the mixer, and the specific snack shapes you need. Include your workshop’s available length and ceiling height so the line can be arranged without re-routing utilities. Confirm the local voltage and frequency, as well as the preferred control-panel language, so the electrical cabinet is wired correctly before dispatch.
Frequently Asked Questions
Q: How do you confirm the actual output of the line before shipment?
A: We run the buyer’s own raw material through the full station sequence in our testing workshop. The trial report records throughput at each hand-off, final moisture after the dryer, and product dimensions. Only after the buyer reviews and approves the report do we proceed to final assembly and packing.
Q: Can the dryer energy source be changed after the order is placed?
A: The five-layer mesh dryer is designed for electric, gas or oil heating. Switching sources after the order requires modifying the heat-exchanger section and control wiring, so the decision should be confirmed before production starts to avoid lead-time extensions.
Q: What voltage and control-language options are available?
A: The electrical cabinet is built to the destination market’s voltage and frequency. The Delta inverter and temperature controller support multiple display languages. Both items must be confirmed in writing before wiring begins so that the correct breakers, transformers and HMI firmware are installed.
Q: How do you match screw configuration to different grain recipes?
A: Each screw is built from sectional modules. We select element geometry and sequence based on the buyer’s grain type, fat content and target expansion. The configuration record is documented and shipped with the machine so replacements can be ordered identically.
Q: What utility preparations does the factory need before installation?
A: The buyer must provide a leveled concrete floor capable of supporting the dryer’s loaded weight, a dedicated power circuit matching the confirmed voltage, and exhaust ducting for the dryer’s moisture-laden air. Detailed utility requirements are included in the line layout package issued at the quotation stage.
Related products
-

Equipo de producción de extrusión de bocadillos de maíz inflado de alta productividad automático en nueva condición Máquina para hacer alimentos de bocadillos inflados
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Máquina de Comida Snack Inflada Máquina de Comida Snack Máquina de Snack Inflado
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Línea de producción de palitos de bocadillo de maíz inflado automático Equipos en nueva condición
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page -

Línea de producción de equipos industriales para el procesamiento de cereales de desayuno Crispy Maize Chocos Corn Flakes totalmente automática
¥1,000.00 Select options This product has multiple variants. The options may be chosen on the product page