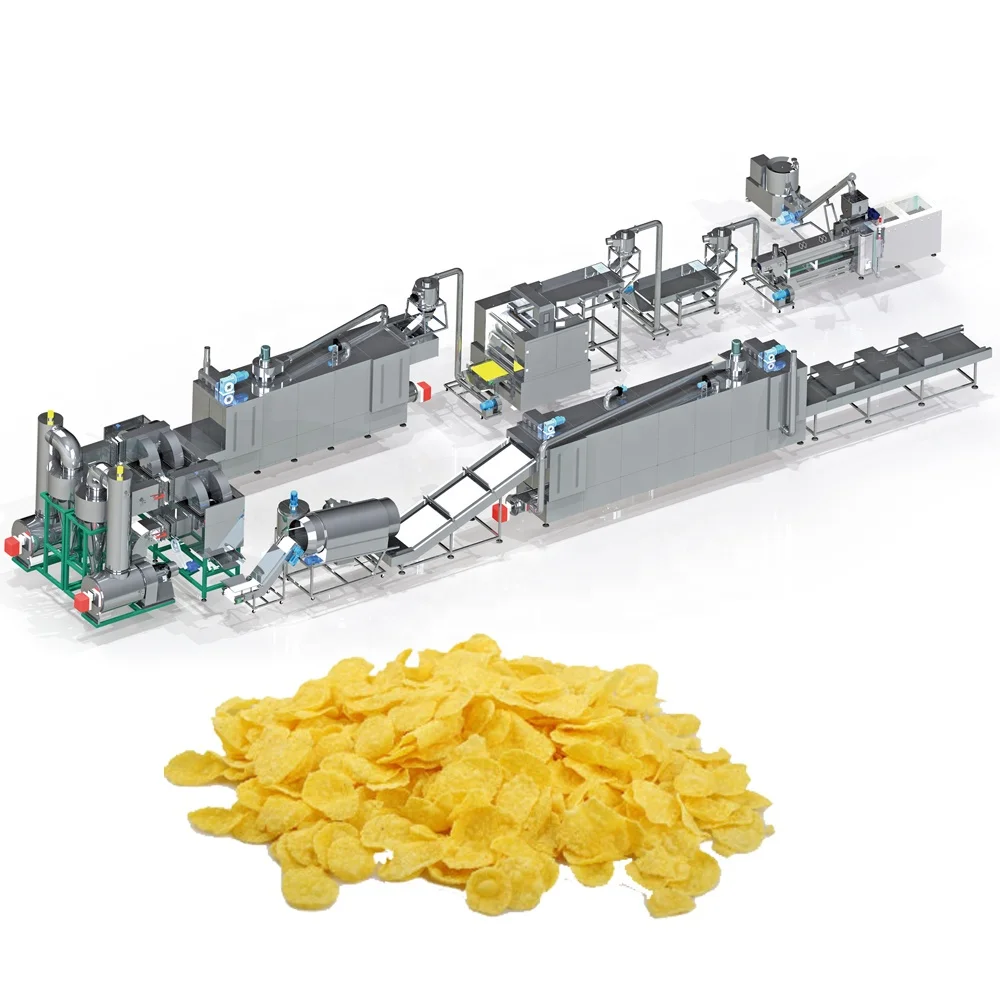
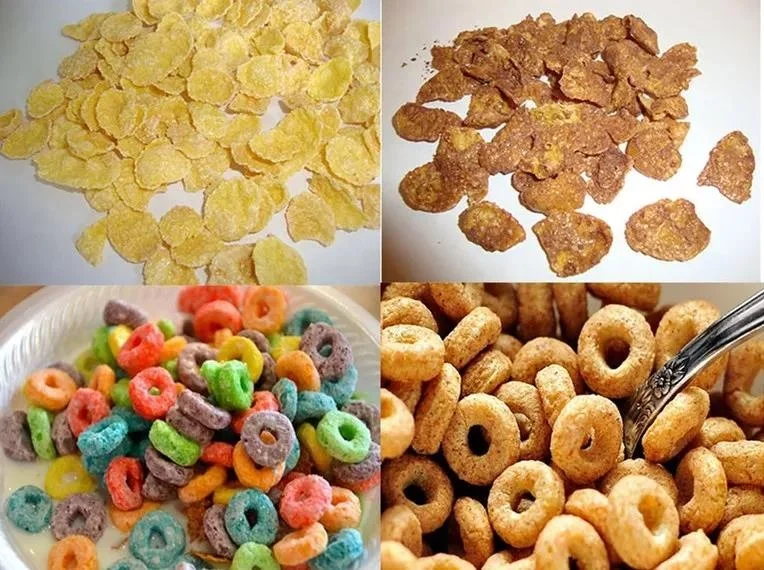
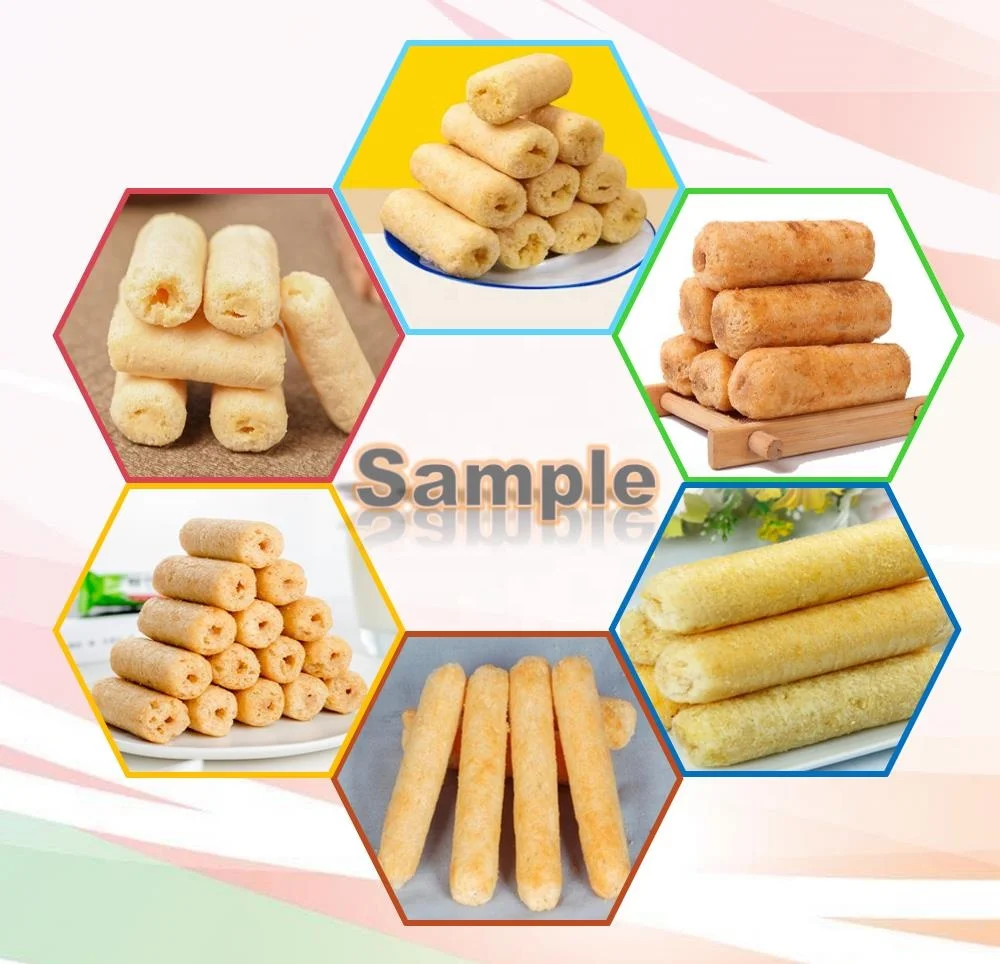
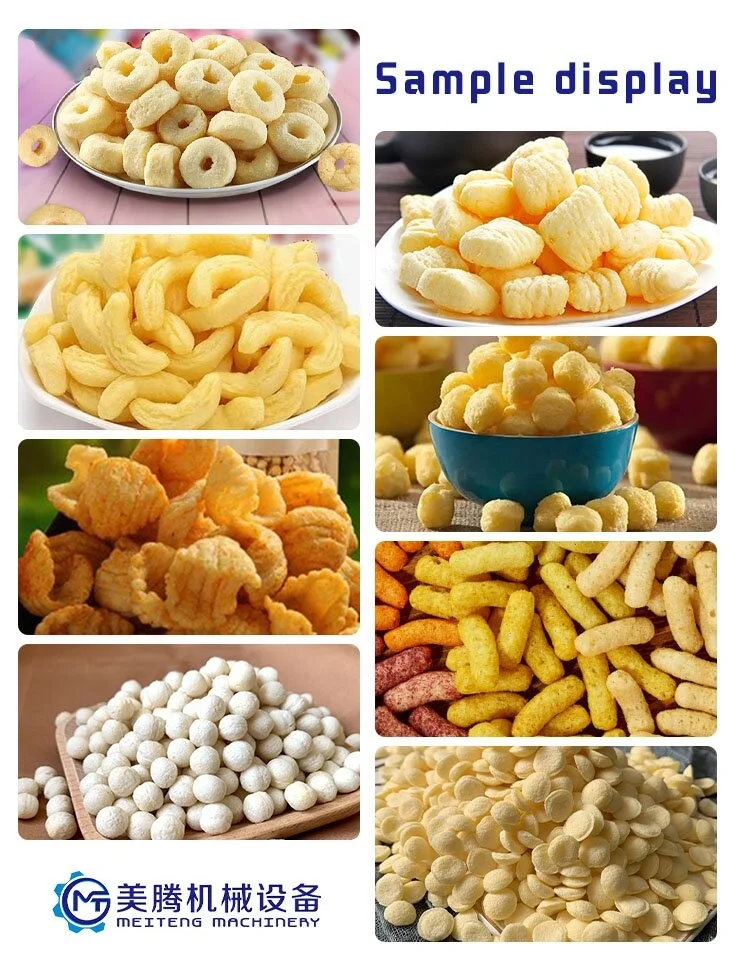
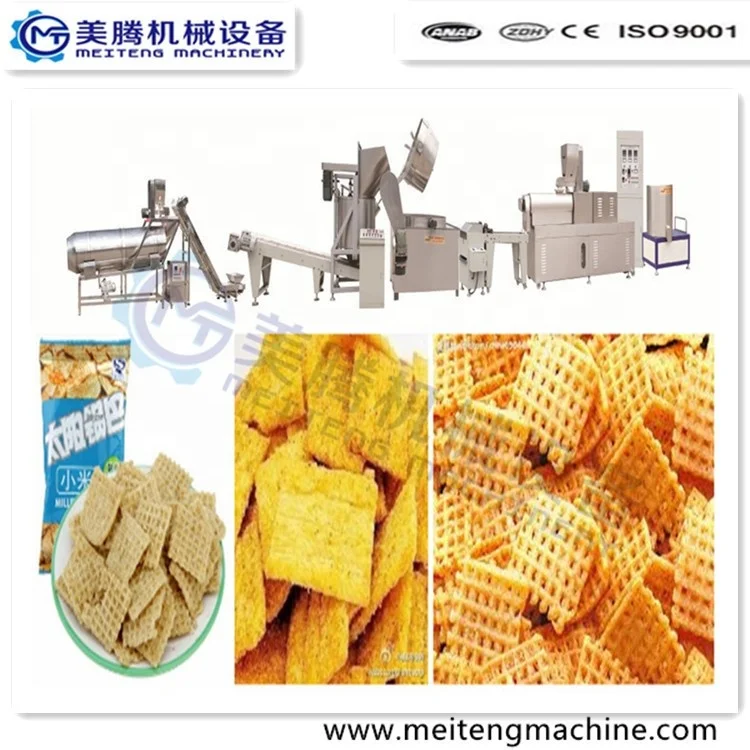
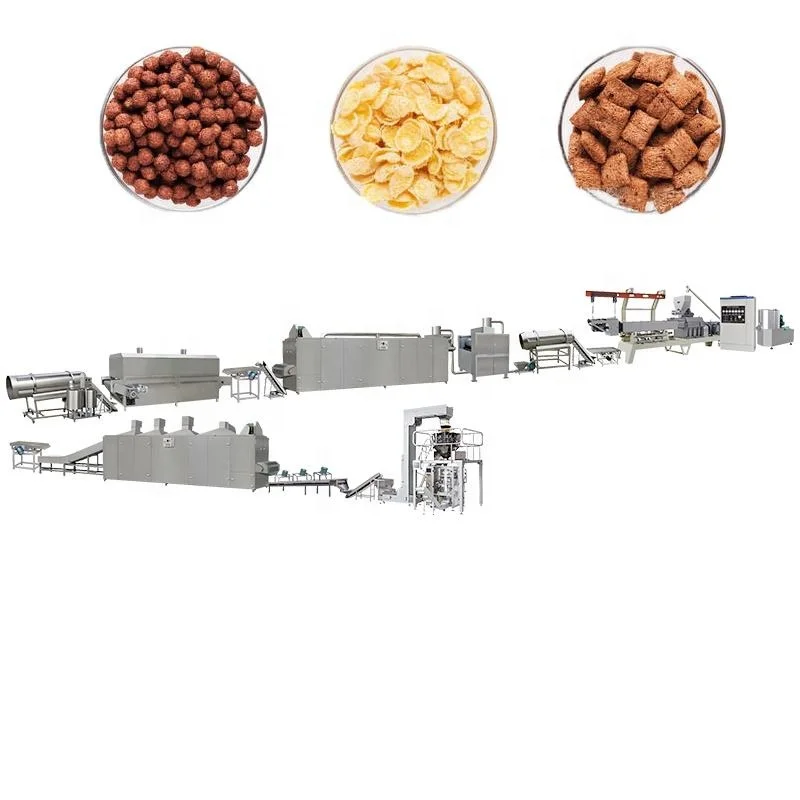
Food Extrusion Processing Line, Twin-Screw, 100-500 kg/h — configured for puffed snacks and corn flakes from corn, rice, wheat, oat and multi-grain blends. Complete turnkey layout from batching through extrusion, drying, flavouring and packing with throughput matched across every station. Screw and die profile set to your cereal formulation and target density.
- Multi-layer belt dryer sized to snack moisture curve
- PLC and MCC control with voltage confirmed pre-build
- Trial run on your raw material before shipment
Description
Throughput matched end-to-end — Every station from batching to packing is sized as a single system, so the twin-screw extruder, dryer and flavouring drum run at the same rate without one blocking the rest.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin-Screw Extrusion Production Line for Puffed Snacks and Corn Flakes |
| Extruder Type | Double (twin) screw extruder |
| Output Capacity | 100-500 kg/h (basis not stated in source — confirm raw material, moisture and target product format) |
| Raw Materials | Corn, rice, millets, wheat, oat, barley, buckwheat, brown rice (flour or grits) |
| Voltage & Frequency | Three phase 380V/50Hz; Single phase 220V/50Hz; customizable to local voltage per country |
| Rated Power | approx. 100 kW (electric heating) or 50-60 kW (gas/diesel heating) (source value — verify against manufacturer catalog) |
| Contact Material | Food grade stainless steel 201/304 |
| Energy Options | Electricity / gas / diesel / steam |
| Control Components | Siemens (China) or top Chinese brand motors; Delixi or Delta inverters |
| Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (by adjusting die/mould) |
| Line Stations | Mixer → Extruder → Vibrate Cooler → Roasting Machine (Dryer) → Packing Machine |
| Flavouring System | Semi-automatic or automatic; supports sugar, oil and powder seasoning |
| Dryer Type | Multi-layer belt dryer; length and layer configurable to product |
| Automation Level | High degree automation |
| Standards | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Puffed snack production | Cheese balls, corn puffs, extruded shapes from corn or rice grits |
| Breakfast cereal and corn flakes | Flaked cereal from corn flour or multi-grain blends |
| Fortified artificial rice | Vitamin-enriched rice kernels from mixed cereal blends |
| Multi-grain snack and cereal lines | Rice, millet, wheat, oat, barley, buckwheat formulations |
Why "Rated Capacity" Means Nothing Without the Full Line Context
A puffed snack and corn flakes extrusion production line turnkey is only as fast as its slowest station.
Quoting an extruder at a nominal output while the downstream dryer or flavouring drum runs slower is a common trap in snack and cereal projects. The result is a line that physically cannot hold its rated throughput on your actual raw material, forcing operators to throttle the extruder and lose saleable output every shift [NEED_CITE: throughput mismatch in multi-station extrusion lines]. When the drying curve for corn flakes demands a longer residence time than the belt dryer provides, moisture leaves the product above specification and shelf life collapses. This puffed snack and corn flakes extrusion production line turnkey is configured so that every station — mixer throughput, extruder screw speed, dryer belt length and layer count, flavouring drum dwell time — is calculated against the same target output before any steel is cut.
Layout and Station Sizing as One System
The line begins with a mixer sized to feed the extruder hopper continuously, avoiding the batch-starvation pauses that drop output on many snack lines. The twin-screw extruder pushes product through a vibrating cooler that sets the surface before the product enters the multi-layer belt dryer. Because the dryer length and layer count are configurable, the drying curve for a dense corn flake and a light puffed ball can both be accommodated without swapping hardware. This approach to the puffed snack and corn flakes extrusion production line turnkey keeps the overall footprint tight while matching throughput end-to-end.
Screw and Die Configuration Set to Your Formulation
A generic screw build copied from a catalogue extruder will produce the wrong texture when your flour blend has a different starch or protein ratio than the reference material. On this line, the screw elements and die geometry are specified after reviewing your raw material data sheet and target product density. The in-house testing workshop runs your actual flour blend before shipment, generating a trial report that locks in moisture, barrel temperature profile and screw speed. That record travels with the machine, so commissioning starts from a known baseline rather than weeks of trial and error on the factory floor [NEED_CITE: twin-screw extrusion screw configuration for cereal formulations].
What the Power and Heating Specs Mean for Your Utility Plan
The rated power sits around 100 kW when electric barrel heaters are specified, dropping to roughly 50-60 kW if gas or diesel heating is chosen for the dryer and extruder barrels. This difference shapes your transformer sizing and dedicated circuit planning. Sites with expensive industrial electricity often choose gas heating on the dryer to cut per-kilogram energy cost, while facilities with limited gas infrastructure stay fully electric. Voltage and frequency are confirmed against your local supply before production, and the control panel language is set to match your operators so that alarms and setpoints read correctly on day one.
The Hidden Cost of Undersized Downstream Stations
When a dryer is quoted on a generic moisture removal figure rather than your actual product’s drying curve, the line either runs wet product that sticks in the packing machine or operators slow the extruder to compensate. Flavouring drums that cannot keep up with extruder output leave seasoning uneven, and the packing station faces surges followed by starvation. These bottlenecks do not show up in a brochure, but they cost real output every shift [NEED_CITE: downstream bottleneck impact on extrusion line output].
Why Procure This Line Here
Every station is sourced from a single supplier, so throughput calculations and mechanical interfaces are reconciled before the first drawing is released. The testing workshop runs your flour blend and generates a trial report tied to your product specification, not a generic build. Screw and die configuration records, electrical schematics and voltage confirmation documents are delivered as a package, so your electrical contractor knows exactly what to prepare. On-site installation covers phased assembly, utility hook-up verification and operator training on the actual control interface. Wear parts lists specify screw elements, dies and dryer belt sections so your first replacement order is placed before the original parts wear through.
Documentation & Verification
- Line layout drawing with capacity calculation per station showing end-to-end throughput match
- Trial run report on your cereal flour blend conducted in the testing workshop before shipment
- Screw and die configuration record tied to your product density and shape specification
- Electrical schematic with voltage, frequency and PLC/HMI language confirmed before production
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Operation and maintenance manual with wear parts list and recommended replacement intervals
Installation, Commissioning & Support
- Foundation plan reflecting the full line footprint and multi-layer dryer weight distribution
- Dedicated circuit sizing based on confirmed 380V/50Hz or local voltage and the 100 kW electric heating load
- Phased assembly sequence from mixer through packing station with utility hook-up checkpoints
- First-run parameter setting using the trial report baseline for barrel temperature and screw speed
- Operator training on the confirmed control language covering alarms, setpoints and daily start-up
- Wear parts supply for screw elements, dies and dryer belt sections with lead time aligned to your first replacement window
What to Include in Your Inquiry
Share your target product format — whether puffed shapes, corn flakes or fortified rice — along with the flour blend composition and any moisture or density specification your market requires. Confirm your local voltage, frequency and preferred control panel language so the electrical design matches your site. If you have an existing upstream batching system or downstream packing line, provide the interface details so the new stations integrate without rework.
Frequently Asked Questions
Q: How is the line capacity verified, and on which raw material formulation and moisture level is it based?
A: Capacity is calculated per station using your specific flour blend composition, target moisture and product density. The in-house testing workshop runs your raw material before shipment, producing a trial report that documents actual throughput, barrel temperature profile and screw speed. This report becomes the baseline for on-site commissioning.
Q: How are the extruder, dryer and flavouring stations sized relative to each other to avoid bottlenecks?
A: Each station is sized from the same target output figure. The dryer belt length and layer count are matched to your product’s drying curve, and the flavouring drum volume is calculated to provide sufficient dwell time at the extruder’s actual discharge rate, so no single station limits the line.
Q: What trial run is performed on my raw material before the line ships, and what report will I receive?
A: Your flour blend is run through the twin-screw extruder in the testing workshop using the specified screw and die configuration. You receive a trial report documenting throughput, moisture, product density, barrel temperature settings and screw speed, which is used to set initial parameters during on-site commissioning.
Q: How are voltage, frequency and PLC/HMI language confirmed for my country before production starts?
A: Your local voltage and frequency are confirmed during the specification stage, and the electrical schematic is drawn to match. The PLC and HMI language is set to your operators’ requirement before the control panel is wired, so alarms and setpoints display correctly when the line powers on at your site.
Q: What does phased on-site installation, commissioning and operator training look like for a complete line?
A: Installation follows a phased sequence from mixer through packing, with utility hook-up verified at each station. Commissioning uses the trial report baseline to set parameters, and operators are trained on the confirmed control language covering daily start-up, alarms and wear part inspection before the team departs.
Related products
-

Hot Sale Corn Snack Extruder Puffed Snacks Production Machine Corn Puffs Making Machine
¥20,000.00 Select options This product has multiple variants. The options may be chosen on the product page -
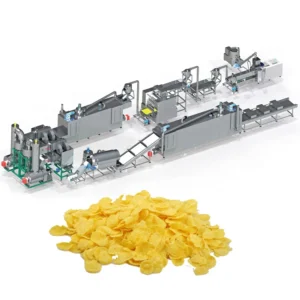
Automatic Corn Flake Processing Line Corn Coco Pops Breakfast Cereals Snacks Making Machinery
¥7,500.00 Select options This product has multiple variants. The options may be chosen on the product page -
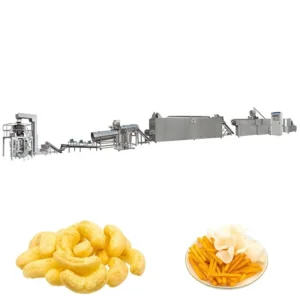
New Stainless Steel Automatic Puffed Rice Flour Snacks Making Machine High Productivity Multi-function
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

New Stainless Steel Automatic Snack Food Machinery Extruder Puffed Corn Maize Puff Processing Line for Food Industry High
¥12,350.00 Select options This product has multiple variants. The options may be chosen on the product page