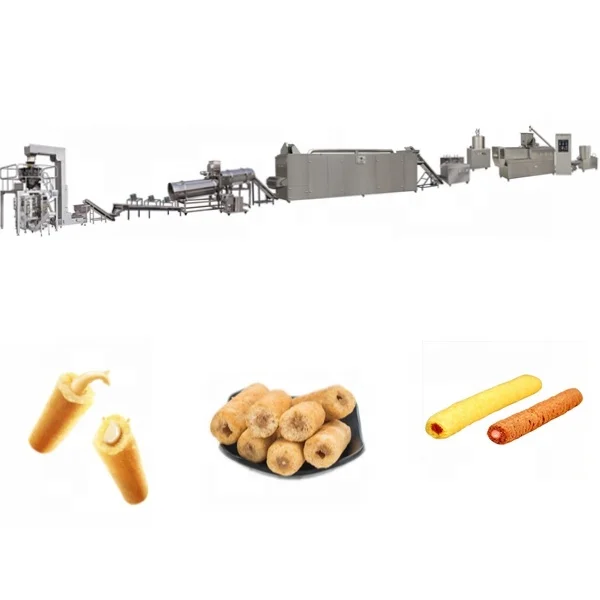
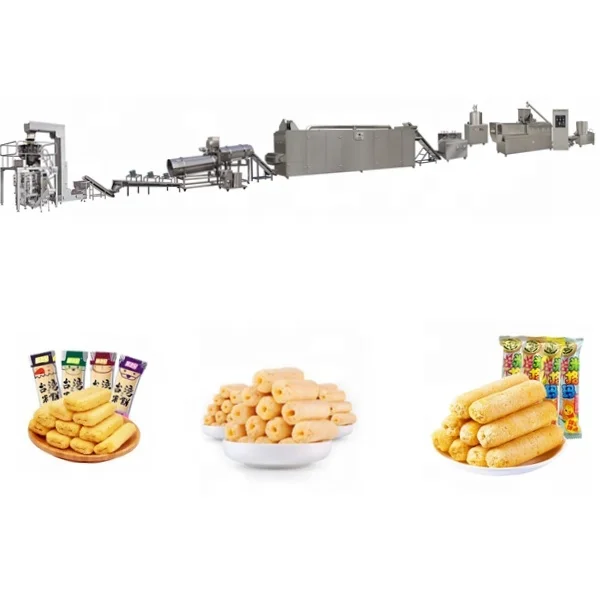
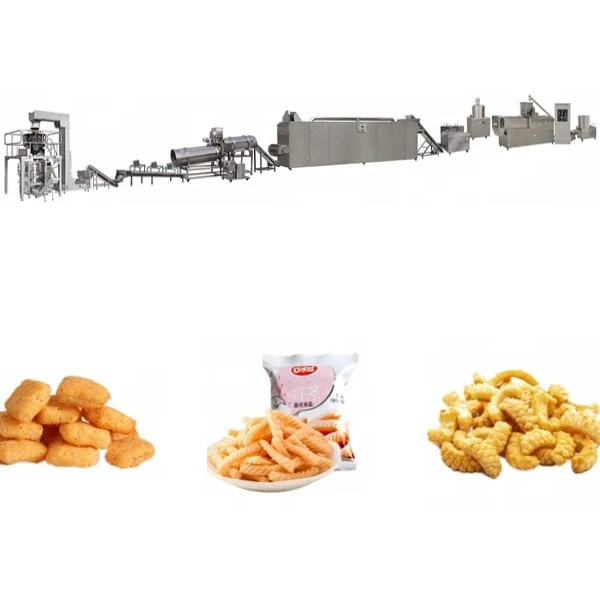
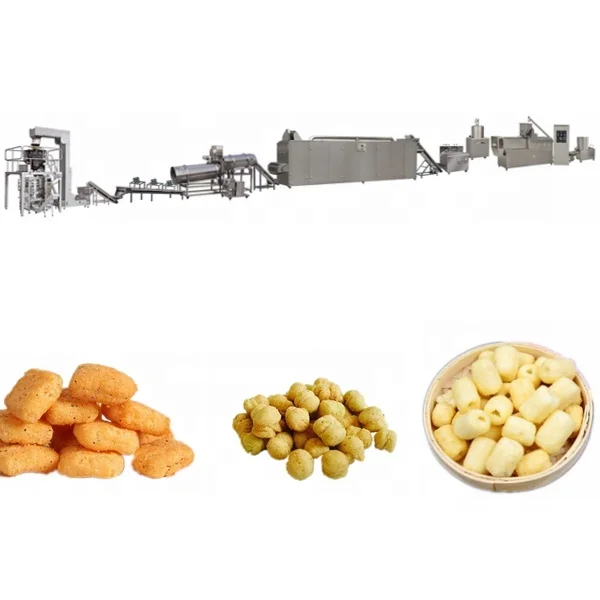
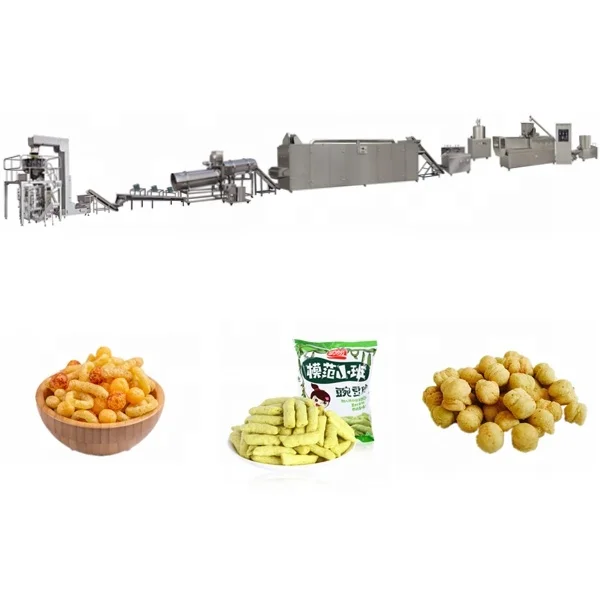
Puff Corn Snack Stick Production Line, Twin-Screw Extruder, PLC & MCC Control — engineered as a complete turnkey food extrusion processing line from batching through packing.
- Screw configuration and die design are matched to your raw material and target product density, controlling expansion and texture across rice, millet, buckwheat, and other cereals.
- Every station — mixer, extruder, vibrate cooler, roasting machine, packing — is throughput-matched under one supplier to eliminate inter-vendor bottlenecks.
- Multiple energy source options (electricity, gas, diesel, steam) and voltage confirmed to your local standard before production.
- CE certified with food-grade stainless steel construction throughout.
Trial runs on your actual raw material are completed in our in-house testing workshop before shipment, so product development starts before installation — not after.
Description
Matched Throughput — Every station from the mixer through the roasting oven to packing is sized against the extruder’s real output, so a puff corn snack stick production line turnkey build never bottlenecks at the slowest link.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Puff Corn Snack Stick Production Line |
| Extruder Configuration | Double screw extruder machine (screw diameter, L:D ratio, and barrel zones basis not stated in source) |
| Raw Material Compatibility | Rice, millet, brown rice, buckwheat, and other cereals |
| Line Sequence | Mixer → Extruder → Vibrate Cooler Machine → Roasting Machine → Packing Machine |
| Control System | PLC and MCC (Delixi or Delta inverter) |
| Motor | Siemens (made in China) or equivalent China top brand |
| Rated Power | Approx. 100 kW (electric heating); approx. 50–60 kW (gas or diesel heating) |
| Energy Source Options | Electricity, gas, diesel, or steam |
| Voltage & Frequency | Three-phase 380 V / 50 Hz, single-phase 220 V / 50 Hz (customizable to buyer’s local supply) |
| Machine Material | Food-grade stainless steel 201 or 304 |
| Product Format Flexibility | Core-filling snacks, chocolate-filled bars, cream-filled pillows, rice cakes, cereal bars, sheet snacks (by changing moulds and process) |
| Output Capacity | Basis not stated in source — confirm raw material, moisture content, and product size/density |
| Assembly State | Complete turnkey production line |
| Standard | CE (electronic edition available on request) |
Application Suitability
| Application | Material or Output |
|---|---|
| Puff corn snack sticks | Corn grits, rice flour, millet blends at controlled moisture |
| Core-filled snack bars | Cereal-based outer shell with cream, chocolate, or peanut butter filling |
| Breakfast cereal pieces | Brown rice, buckwheat, or multi-grain formulations |
| Sheet snacks and rice cakes | Rice or buckwheat batter pressed and cut post-extrusion |
| Artificial fortified rice | Rice flour blended with vitamin and mineral premix |
Why the Dryer Question Matters More Than the Extruder Price
A puff corn snack stick production line turnkey only performs when every downstream station can absorb what the extruder pushes out.
I once watched a snack line in Shandong sit idle for four hours because the roasting oven could not keep pace with the extruder. The operator kept throttling the screw speed just to avoid a pile-up on the conveyor. Nobody had calculated the moisture removal load against the oven’s belt length and dwell time. That mismatch does not show up on a quotation until the machines are bolted to the floor and the first run starts backing up [NEED_CITE: typical causes of throughput mismatch in snack extrusion lines].
Matching Screw Geometry to Your Cereal Blend
A puff corn snack stick production line turnkey depends on the relationship between screw element arrangement and the starch behaviour of your specific raw material. Corn grits gelatinise at a different moisture window than brown rice or buckwheat, and the shear profile inside the barrel must match that window. When the screw configuration is pulled from a generic build rather than specified to your blend, the extrudate can exit the die either under-expanded or scorched. Our in-house testing workshop runs your actual raw material before the line ships, so the die geometry and barrel temperature zones are locked in to your recipe, not a catalogue default.
Full-Line Station Sizing Under One Roof
Sourcing the extruder from one vendor and the roaster from another is where hidden capacity gaps appear. The puff corn snack stick production line turnkey approach we follow keeps mixer batch size, extruder throughput, cooler belt speed, roasting dwell time, and packing rate under a single capacity calculation. Each station is documented in the line layout so you can see the design throughput before production begins [NEED_CITE: importance of single-supplier throughput matching in food processing lines]. If your market later demands a higher output or a new product format, the layout gives a clear starting point for identifying which station to expand first.
Reading the Specification Sheet for What It Actually Controls
The rated power figure — roughly 100 kW on electric heating, dropping to about 50–60 kW on gas or diesel — tells you more than your utility bill. Electric barrel zones respond faster to PID loops, giving tighter temperature control when you switch between a high-moisture cream-filled bar and a low-moisture cereal stick. Gas or diesel heating lowers the electrical draw, which matters in regions where three-phase supply is limited or metered. The choice between stainless steel 201 and 304 hinges on your wash-down chemistry; 304 holds up longer against chlorinated cleaners used in dairy-containing snack facilities. PLC control with a Delta inverter lets you store multiple screw-speed and temperature recipes, reducing changeover guesswork when you rotate between puff sticks, sheet snacks, and core-filled formats.
The Cost of Skipping the Trial Run
Buyers who skip a pre-shipment trial run often spend the first week on-site adjusting screw combinations that should have been resolved in the factory. On one project, a buyer’s corn flour was noticeably coarser than the sample we tested with, and the die pressure climbed until the product density went outside specification. Four days of line stops and restarts followed before we found the right element spacing. Running your material in our testing workshop before dispatch removes that variable entirely [NEED_CITE: risks of commissioning extrusion lines without pre-shipment trials].
Why Source This Line Here
We build every station in-house or through audited partners, so throughput calculations are not handed off between unrelated factories. Screw and die configurations are recorded per order, meaning your replacement parts match the original setup without reverse engineering. Voltage and control language are confirmed to your country standard before production starts, preventing the delays that happen when a 60 Hz motor arrives in a 50 Hz market. Our machine testing workshop is equipped for full-line dry runs, not just single-machine bench tests. After installation, our technicians stay on-site through operator training, ensuring your crew can handle product changeovers independently.
Documentation & Verification
- Line layout and capacity calculation showing matched throughput at each station
- Screw and die configuration record tied to your cereal blend and target density
- Trial run report produced on your raw material before the line leaves the factory
- Electrical schematic with confirmed voltage, frequency, and control language
- CE declaration of conformity in electronic format
- Operation and maintenance manual with illustrated wear parts list
Installation, Commissioning & Support
- Foundation plan accounts for the roasting machine length and the vibrate cooler’s dynamic load
- Dedicated three-phase circuit sized to the confirmed heating source, electric or gas-assisted
- Line arrives in sectional modules for assembly aligned to your facility’s column spacing
- First-run parameter setting covers barrel zone temperatures, screw speed, and die gap for your initial product
- Operator training includes recipe storage in the PLC for repeatable changeovers between snack formats
- Wear parts list covers screws, dies, and barrel liners with recommended first-year replacement quantities
What to Include in Your Inquiry
Share your cereal blend composition, target moisture content after roasting, and the product formats you plan to run — whether puff sticks, core-filled bars, or sheet snacks. Confirm your facility’s available voltage and frequency, the language your operators need on the HMI, and whether an existing mixer or packing machine will be integrated. If you can send a raw material sample, we will schedule a trial run in the testing workshop before finalising the line configuration.
Frequently Asked Questions
Q: How is the line’s output capacity verified on my actual raw material and product size?
A: We run your cereal blend through the extruder in our in-house testing workshop, measuring expansion ratio, density, and moisture at each station. The trial run report documents the achieved throughput under those specific conditions, so the capacity figure in your quotation reflects your recipe rather than a generic benchmark.
Q: How are voltage, frequency, and control language confirmed before production?
A: During the specification review stage, we request your local supply standard and preferred HMI language. The electrical schematic is then drawn to match, and the motor, inverter, and heating elements are sourced accordingly. A written voltage confirmation document is signed off before any steel is cut.
Q: How do you match dryer and packing station capacity to the extruder output?
A: Each station is sized from the extruder’s verified throughput on your material. The roasting machine belt length and dwell time are calculated against the moisture removal load, and the packing machine cycle rate is set to absorb the cooled product flow. The line layout document shows every station’s design capacity side by side.
Q: Can I do a trial run on my raw material before the line ships?
A: Yes. Our machine testing workshop is set up for full-line dry runs. You can send a representative batch of your cereal blend, and we will extrude, cool, and roast it under production conditions. Any screw or die adjustments needed are made and recorded before packing.
Q: What spare wear parts are recommended for first-year operation?
A: We supply a wear parts list specific to your screw and die configuration, typically including replacement screw elements, die plates, barrel liners, and seals. The list notes expected service intervals based on the abrasiveness of your cereal blend, so you can plan your first-year inventory before installation.
Related products
-

Puffed Snack Food Machine Snack Food Machine Puffed Snack Machine
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puff Corn Extruder Machine Puffed Core Filled Snack Food Production Line Machine
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Puffed Food Snack Machine Electric Corn Puffs Snacks Making Machinery New Condition Flavorful Puff Snack Production
¥7,550.00 Select options This product has multiple variants. The options may be chosen on the product page -

Full Automatic Crispy Maize Chocos Corn Flakes Breakfast Cereals Processing Production Line Industrial Equipment
¥1,000.00 Select options This product has multiple variants. The options may be chosen on the product page