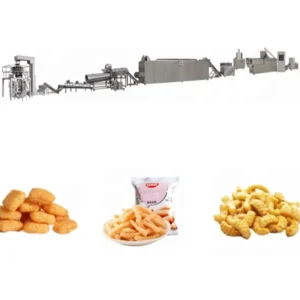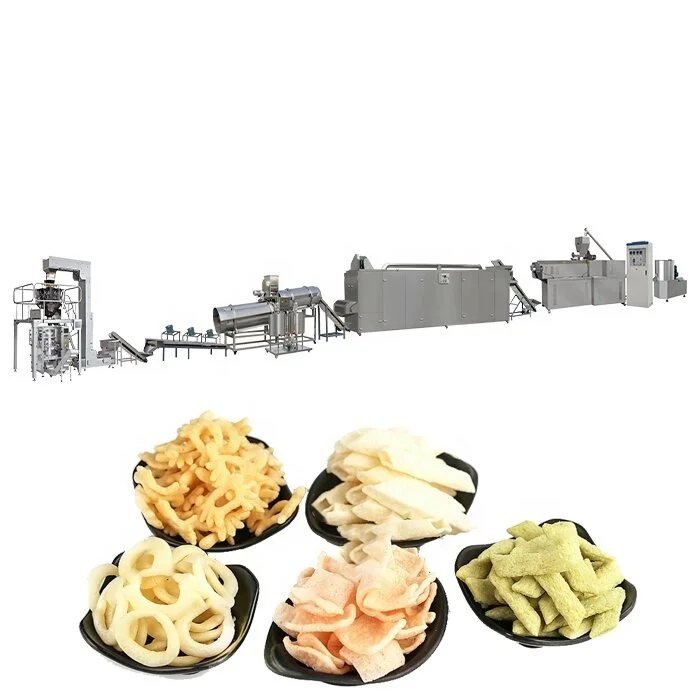
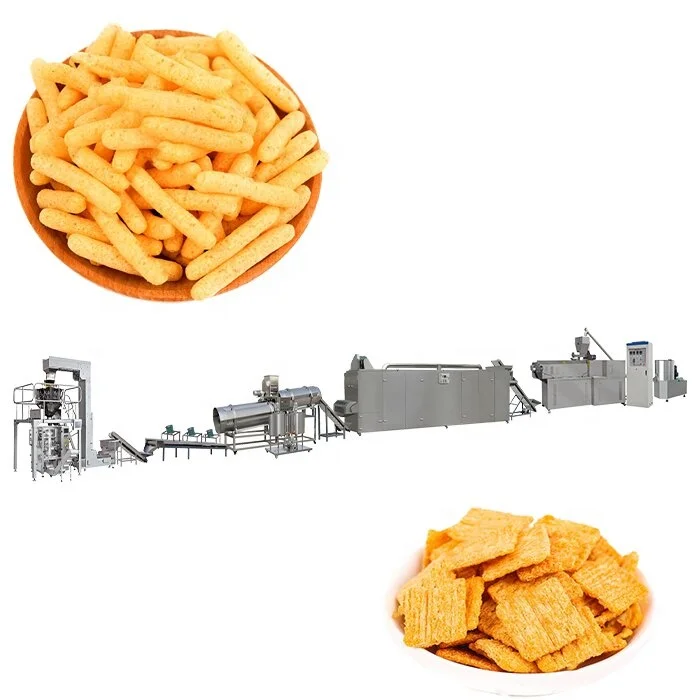
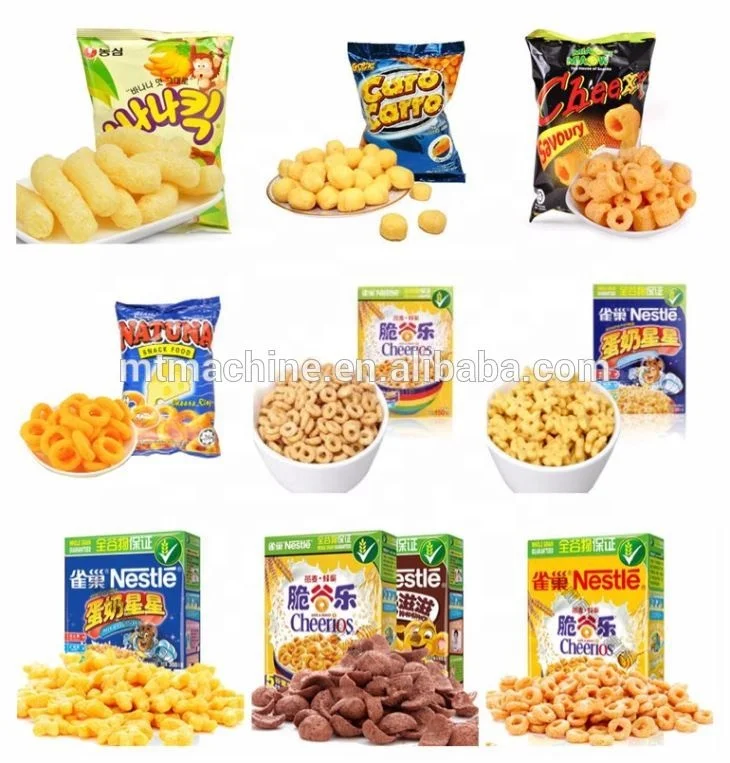
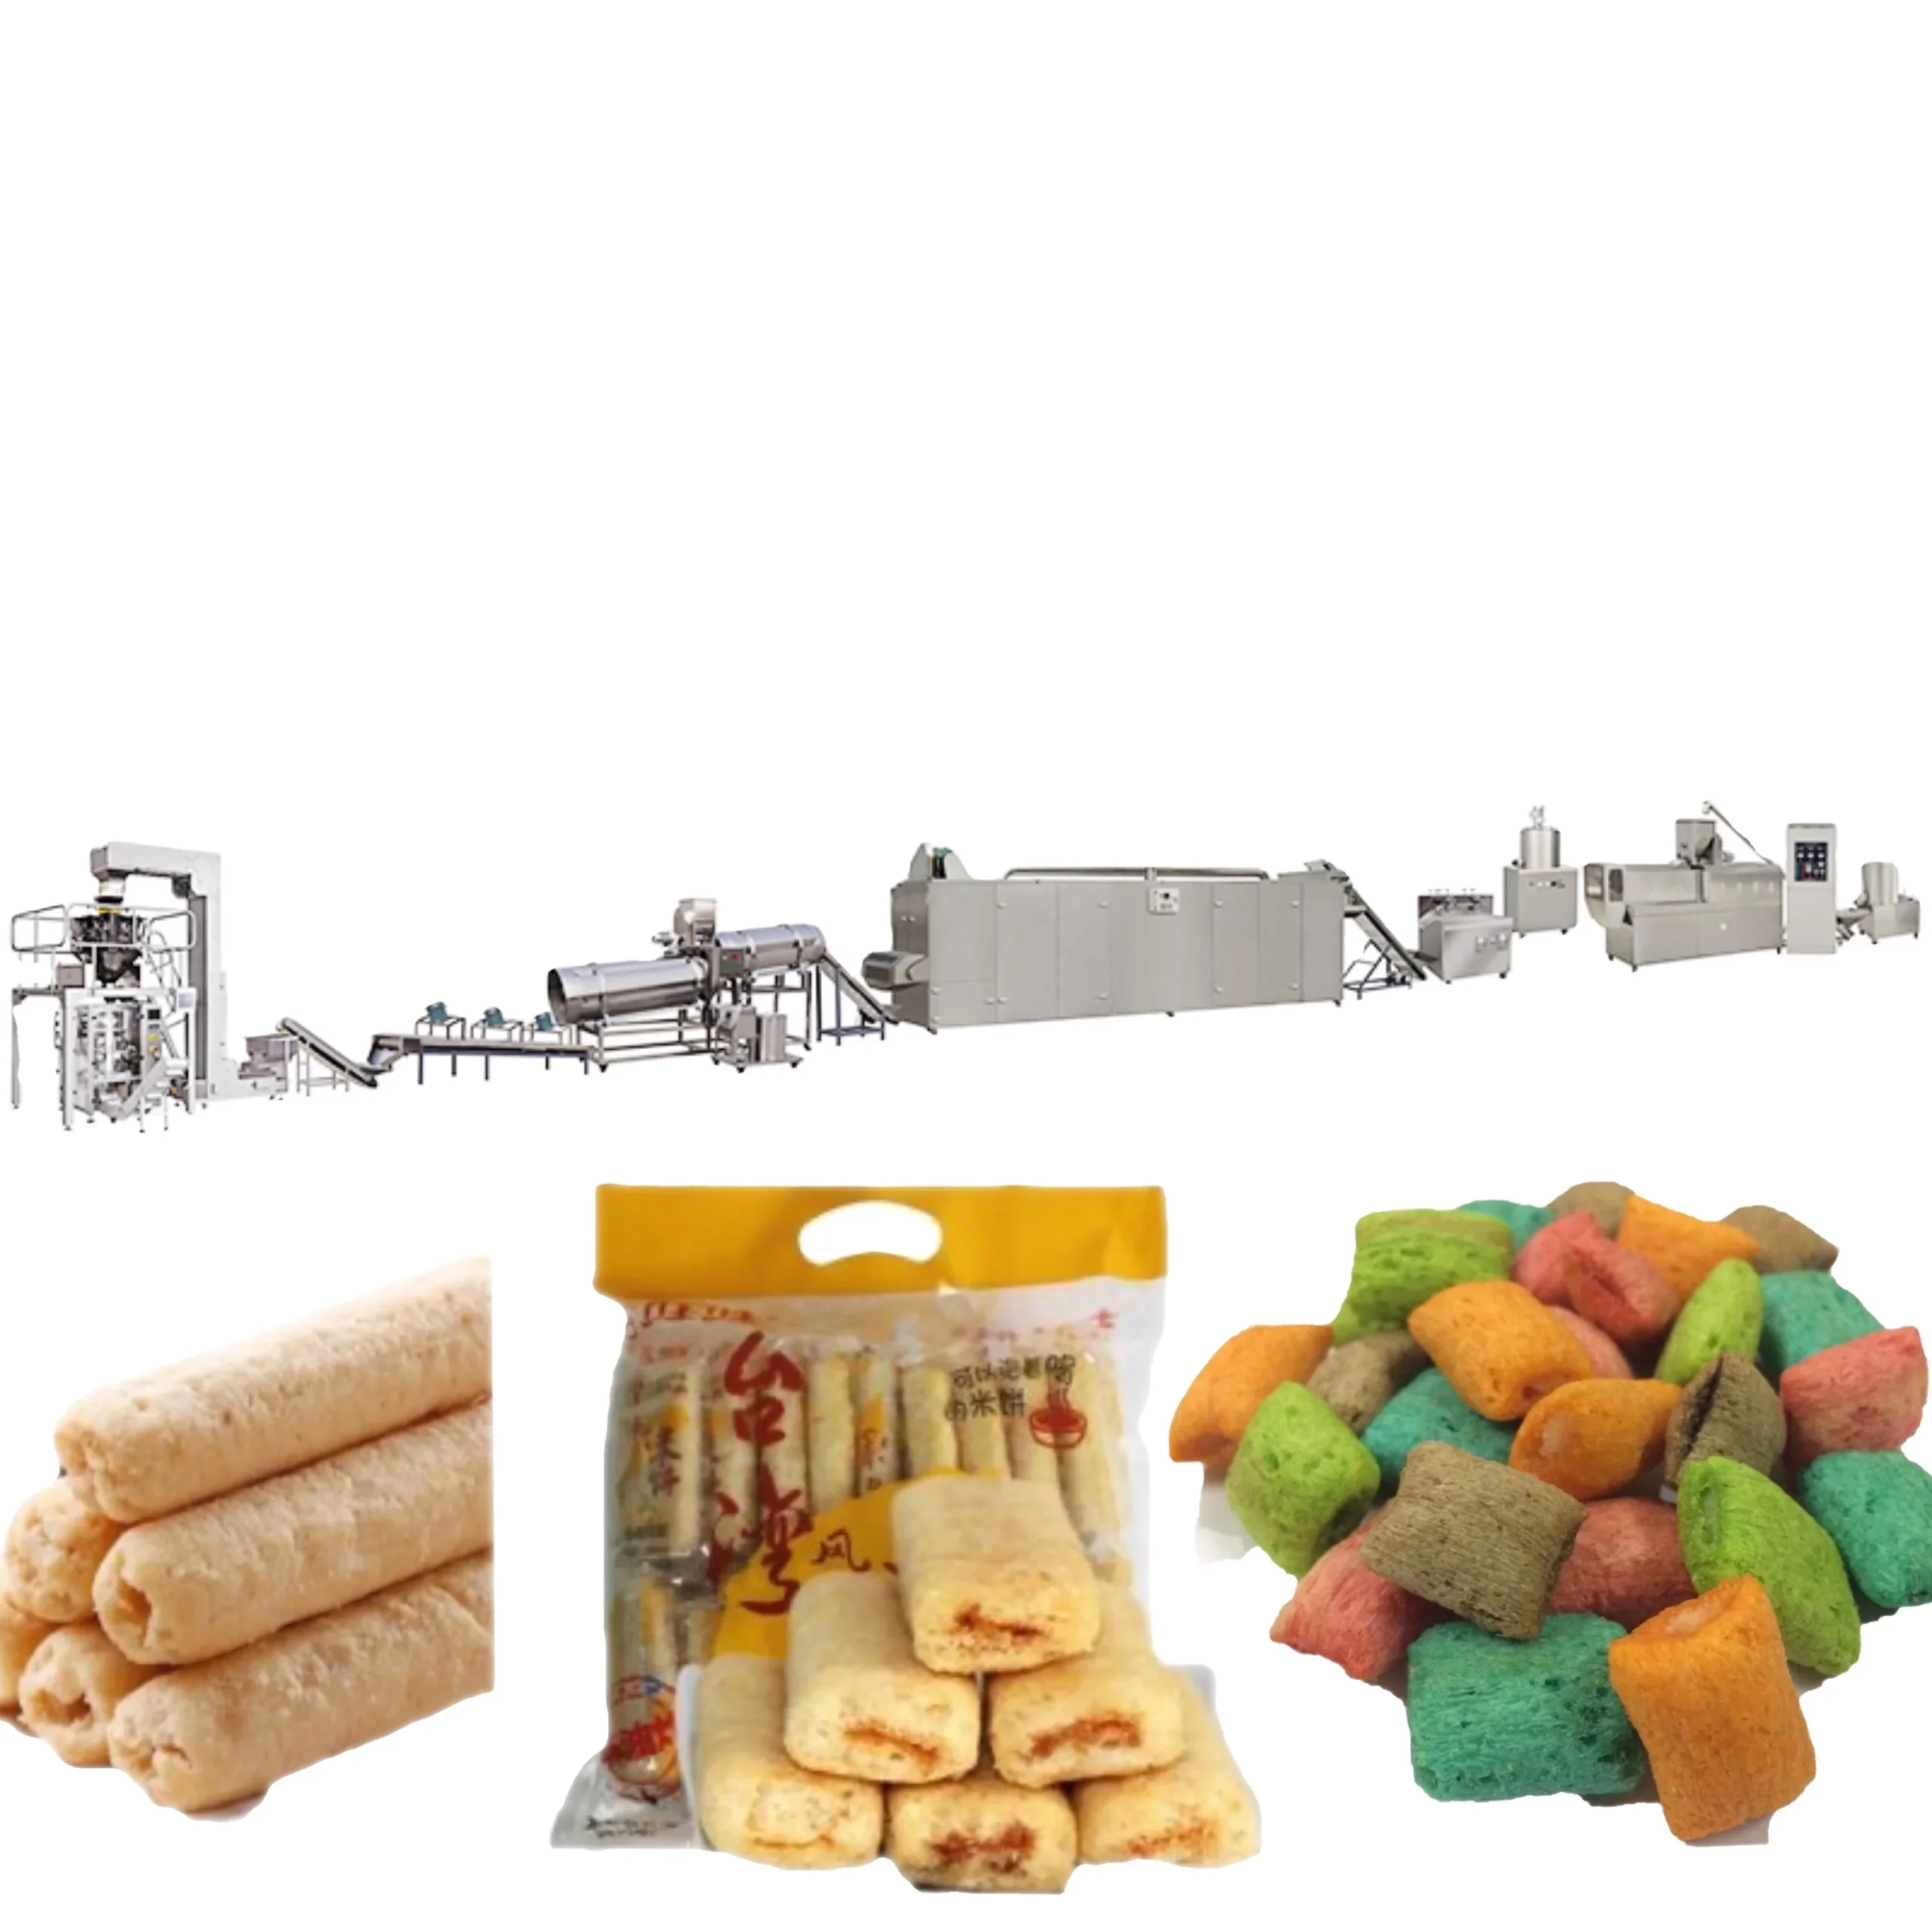
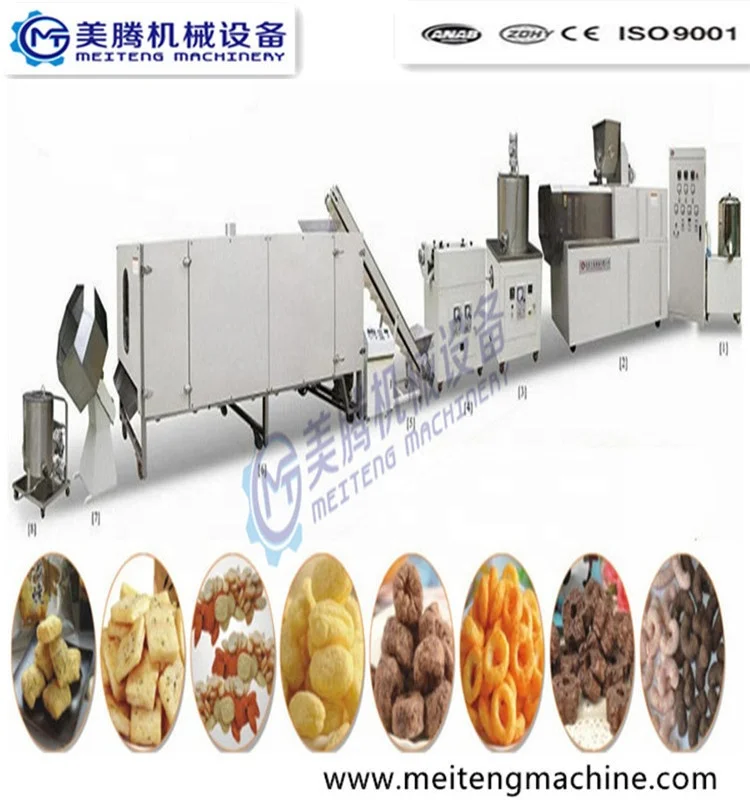
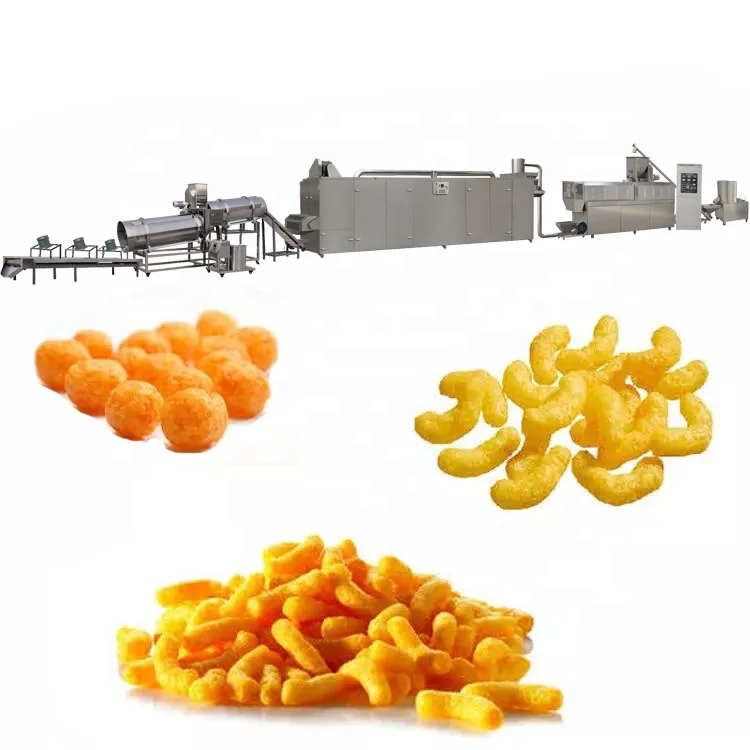
MT65 Twin Screw Snack Food Extrusion Line, 70 kW Installed Power, Siemens Motor — designed for puffed corn snacks, Nik Naks curls and extruded ring or star shapes. The five-layer mesh belt dryer with auto temperature control pairs with nitriding-treated self-cleaning screws to match throughput from mixing through flavoring and packing. In-house trial runs validate screw and die configuration against your raw material before shipment.
- Capacity-matched stations eliminate bottlenecks across the complete turnkey layout
- Converter-driven feeding, extrusion and cutting ensure precise speed coordination
- CE and ISO certified with full electrical schematic and voltage confirmation provided
Description
Capacity-Matched Turnkey Design — Every station from the mixer through the flavoring drum is throughput-balanced to the extruder output, eliminating the mid-line bottlenecks that commonly stall snack production floors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Snack Food Extrusion Line |
| Model | MT65 / MT70 / MT85 |
| Screw Type | Twin Screw |
| Installed Power | MT65: 70 kW / MT70: 100 kW / MT85: 200 kW |
| Real Power Consumption | MT65: 40 kW / MT70: 70 kW / MT85: 150 kW |
| Output Capacity | MT65: 100–150 kg/h (basis to be confirmed) / MT70: 200–240 kg/h (basis to be confirmed) / MT85: 300–400 kg/h (basis to be confirmed) |
| Overall Dimensions | MT65: 20000×1200×2200 mm / MT70: 25000×1500×2200 mm / MT85: 30000×3500×4300 mm |
| Main Motor | Siemens |
| Control System | Converter-driven speed adjustment on feeding, extrusion, and cutting |
| Feeding System | Food-grade stainless steel twin screw feeder |
| Gearbox | Automatic lubrication function |
| Cooling | Increased radiator on driving part for forced cooling |
| Cutting System | Knife fixed in die head seat, rotary cutting by V-belt drive |
| Barrel & Screw Material | Nitriding process, high strength and wear-resistance, self-cleaning |
| Dryer | Five-layer mesh belt, SUS construction, auto temperature control (MAX 160°C), electric / gas / oil heating options |
| Screw Conveyor | 1.1 kW, 2.5×0.5×2.0 m, stainless steel sealed roller |
| Cooling Conveyor | Stainless steel belt, 450 mm width, 6000×600×800 mm, fan-assisted |
| Line Stations | Mixer → Extruder → Vibrating Cooler → Dryer / Roaster → Flavoring System → Cooling Conveyor → Packing Machine |
| Warranty | 24 months, lifetime service |
| Assembly State | Complete turnkey line |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Puffed corn curls (Nik Naks style) | De-germed corn grits, corn flour blends with spice pre-mix |
| Core-filled snack pillows | Rice flour, corn starch, wheat flour with cream or chocolate filling |
| Die-cut extruded shapes (rings, stars, wheels, hearts, strips) | Corn, rice, wheat, and multigrain formulations |
| Coated and seasoned snack pellets | Potato starch blends, cereal-based doughs |
What "Rated Capacity" Really Means on a Snack Extrusion Floor
Nominal throughput means nothing until it is validated against your exact formulation and moisture content.
The most common failure I encounter on snack extrusion projects is a twin screw snack food extrusion production line turnkey quoted at a capacity number that simply cannot hold once real raw material hits the barrel. Standard corn grits behave very differently from de-germed corn flour with higher fat content — I have watched expansion collapse within minutes when that mismatch was not caught early. [NEED_CITE: raw material moisture and fat content effects on extrusion expansion]. The only way to prevent this is running the buyer’s actual sample through a testing workshop before the line is finalized.
Screw Profile and Die Geometry Determine Your Snack Texture
The twin screw configuration on this line is not a generic build copied across every snack format. Screw element arrangement — kneading blocks, reverse elements, and conveying sections — is specified to match the starch gelatinisation behaviour of the buyer’s grain blend. Die aperture and land length then control expansion ratio and surface density, which directly define the crunch and mouthfeel the end market expects. Changing from a corn curl to a core-filled pillow requires a different screw profile and die insert, and this line supports that changeover through modular screw segments and interchangeable die plates.
Drying and Flavoring Must Keep Pace with Extrusion Output
A twin screw snack food extrusion production line turnkey is only as productive as its slowest downstream station. The five-layer mesh belt dryer on this line is sized so that residence time at the target moisture removal rate matches the extruder discharge rate, preventing product backlog or under-dried snacks reaching the flavoring drum. [NEED_CITE: moisture content targets for shelf-stable puffed snacks]. Multiple heating options — electric, gas, or oil — allow the dryer to align with whatever energy infrastructure the buyer’s facility supports, which matters especially in regions where industrial gas is significantly cheaper per thermal unit than electricity.
Reading the Specs That Matter for Snack Consistency
The Siemens main motor paired with an automatic-lubrication gearbox provides the stable torque delivery that twin screw extrusion demands when processing viscous, high-starch doughs under continuous operation. The forced-cooling radiator on the driving section prevents thermal drift during long production runs, which would otherwise alter barrel temperature profiles and shift product density batch to batch. Converter-driven speed control across feeding, extrusion, and cutting ensures that the feed rate, screw RPM, and knife speed stay synchronized — a mismatch here produces uneven piece lengths and inconsistent expansion. The nitriding-treated barrel and screws offer wear resistance that extends service intervals while maintaining the self-cleaning action that reduces recipe changeover downtime on the production floor.
The Cost of Skipping Configuration Alignment
When screw configuration is copied from a generic build rather than matched to the buyer’s raw material, the result is a snack that either expands too much and becomes fragile during packing, or too little and feels dense against consumer expectations. [NEED_CITE: effect of screw configuration on extrudate density and expansion]. A dryer that is undersized relative to extruder output leaves residual moisture in the product, shortening shelf life and inviting mould complaints from distributors. These are not theoretical risks — they are the exact failures that shut down production lines within the first month of operation.
Why Sourcing the Full Line from One Supplier Matters
Every station on this twin screw snack food extrusion production line turnkey — from the batching mixer through the packing machine — is selected and sized by the same engineering team, which means throughput calculations account for real-world transfer losses between stations rather than quoting each machine at its isolated maximum. The in-house testing workshop runs the buyer’s actual raw material before shipment, so screw profile and die clearance are adjusted based on observed expansion rather than assumed behaviour. Pre-sales layout engineering covers utility routing, floor load, and maintenance access for the complete line footprint. Commissioning includes operator training with English-language manuals covering daily maintenance intervals specific to the nitriding-treated barrel and screw set. The 24-month warranty and lifetime service commitment back the entire line, not just individual machines sourced from separate vendors.
Documentation & Verification
- Line layout drawing with station-by-station throughput calculation for your snack format
- Trial run report on your specific corn or grain formulation conducted before dispatch
- Screw and die configuration record matched to your target shape, density, and expansion ratio
- Electrical schematic with voltage and frequency confirmed for your local grid standard
- CE declaration of conformity and ISO certificate for the complete assembled line
- Factory test record documenting continuous run performance on your raw material
Installation, Commissioning & Support
- Floor plan and foundation requirements mapped to the MT65 / MT70 / MT85 overall dimensions and station spacing
- Electrical supply specification covering Siemens motor power draw and converter-driven control circuits
- Delivery as complete turnkey line with station-by-station assembly sequence and rigging guidance
- On-site commissioning including screw profile fine-tuning and dryer temperature ramp calibration
- Operator training covering self-cleaning barrel procedures and nitriding surface care routines
- Wear parts list for screws, dies, and cutting knives with recommended replacement intervals
Before You Request a Quotation
To size the right line configuration, we need your target snack shape and the exact grain formulation you intend to run, including moisture content and any fat or fibre additions. Share your local voltage and frequency standard, the control language your operators require, and your available floor space with ceiling height clearance. If you have existing upstream or downstream equipment you plan to integrate, specify the interface points so we can match conveyor heights and transfer speeds.
Frequently Asked Questions
Q: How is the actual output capacity of this line determined?
A: Output figures listed for each model are reference ranges that must be validated against your specific raw material formulation, moisture level, and target snack density through a trial run. We test your actual sample in our workshop and document the achievable throughput before finalizing the line configuration and quotation.
Q: Can the screw and die setup handle multiple snack shapes on one line?
A: Yes. The twin screw elements are modular and reconfigurable, and the die head accepts interchangeable die plates for shapes like rings, stars, curls, and strips. Changeover requires swapping the die insert and adjusting screw profile segments to match the expansion behaviour of each new format.
Q: How do you ensure the dryer does not bottleneck the extruder?
A: The five-layer mesh belt dryer is sized so its effective drying capacity at the required moisture removal rate equals or exceeds the extruder discharge rate. Residence time, belt speed, and temperature zones are calculated based on the specific snack geometry and target final moisture for your product.
Q: What happens if my raw material behaves differently than expected during production?
A: That is exactly why we insist on running your sample material in our testing workshop before the line ships. We have seen formulations with higher fat content collapse during expansion, requiring on-site screw profile and die clearance adjustments. Catching this before crating avoids costly field rework.
Q: What documentation comes with the line for customs and installation?
A: You receive a complete documentation package including the line layout, electrical schematic with confirmed voltage, trial run report, screw and die configuration record, CE declaration, ISO certificate, operation manual, and packing photographs. We also provide customs documentation support for smooth clearance at your destination port.
Related products
-

Puffed Snack Food Machine Snack Food Machine Puffed Snack Machine
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

New Stainless Steel Automatic Snack Food Machinery Extruder Puffed Corn Maize Puff Processing Line for Food Industry High
¥12,350.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puff Corn Extruder Machine Puffed Core Filled Snack Food Production Line Machine
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Corn Puff Processing Line with Mixer Fryer Baking Oven Automatic High Productivity Grain Products Snack Making Machine
¥8,300.00 Select options This product has multiple variants. The options may be chosen on the product page