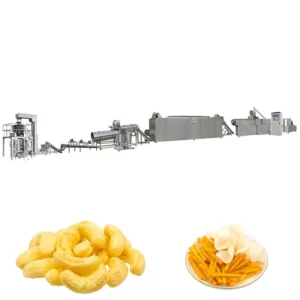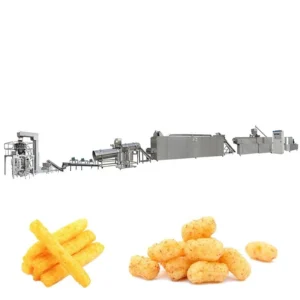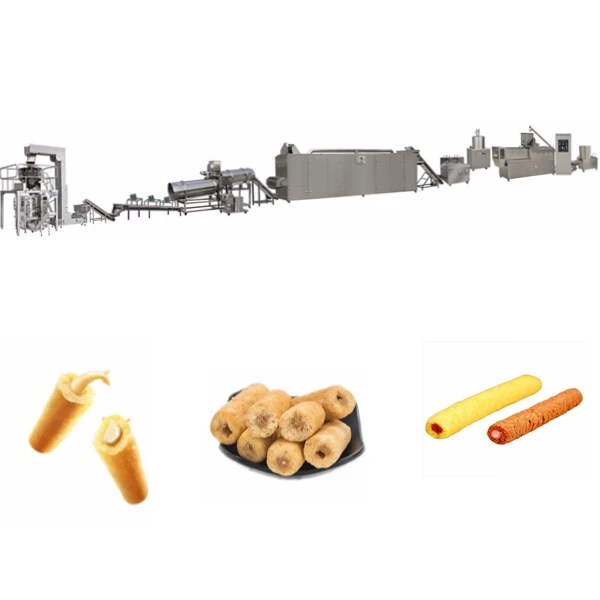
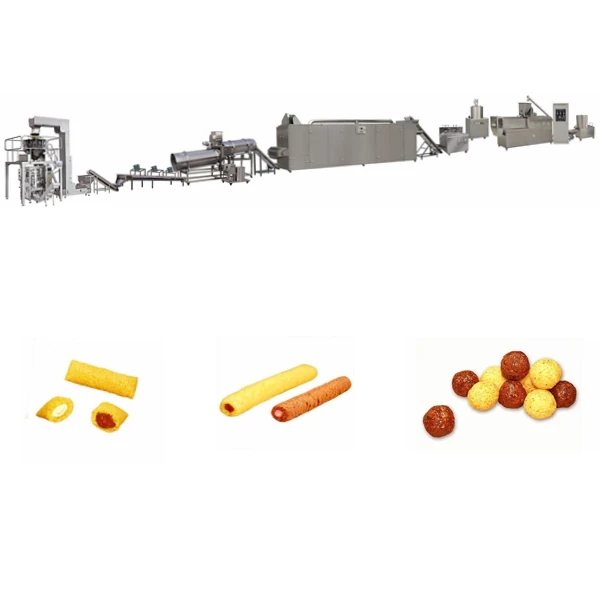
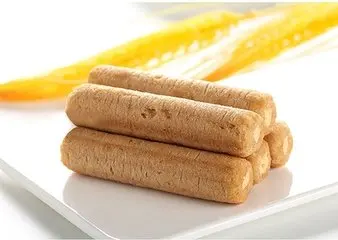
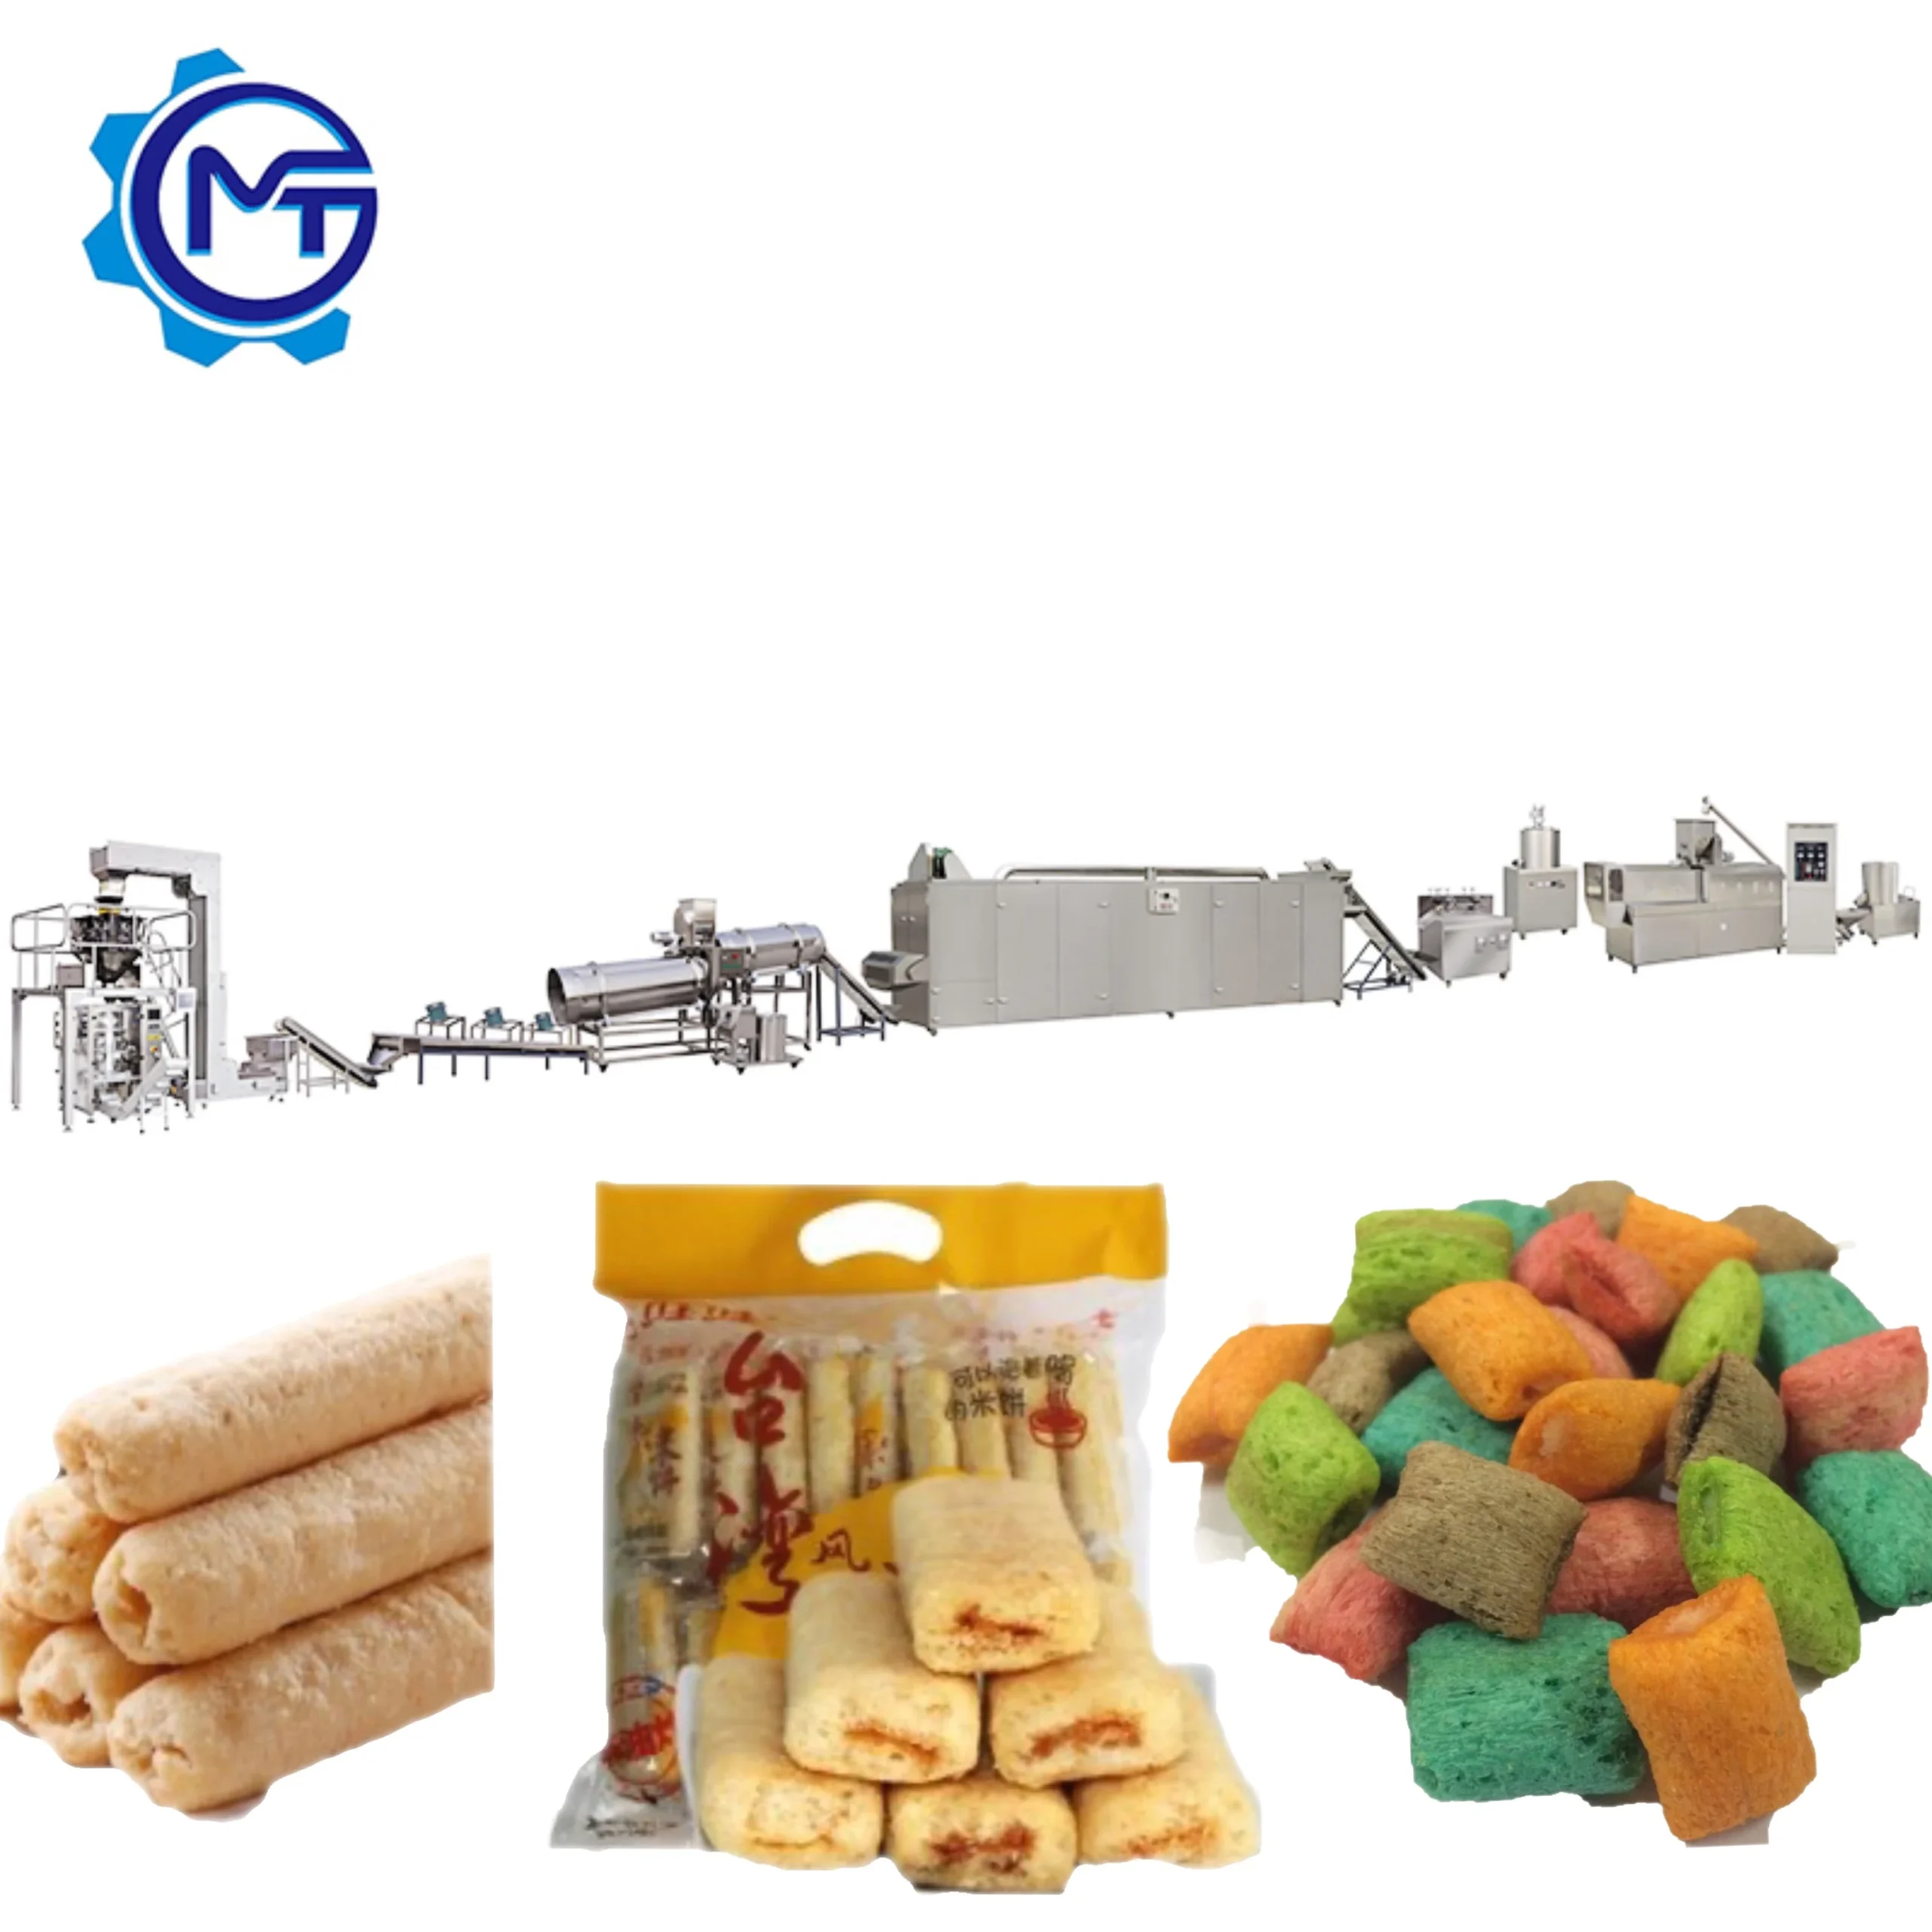
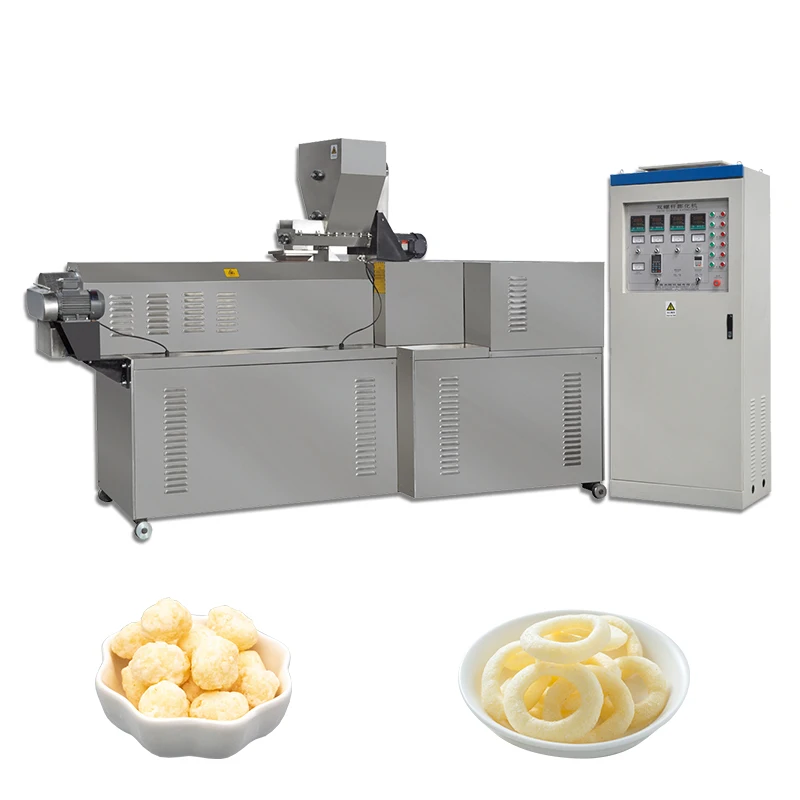
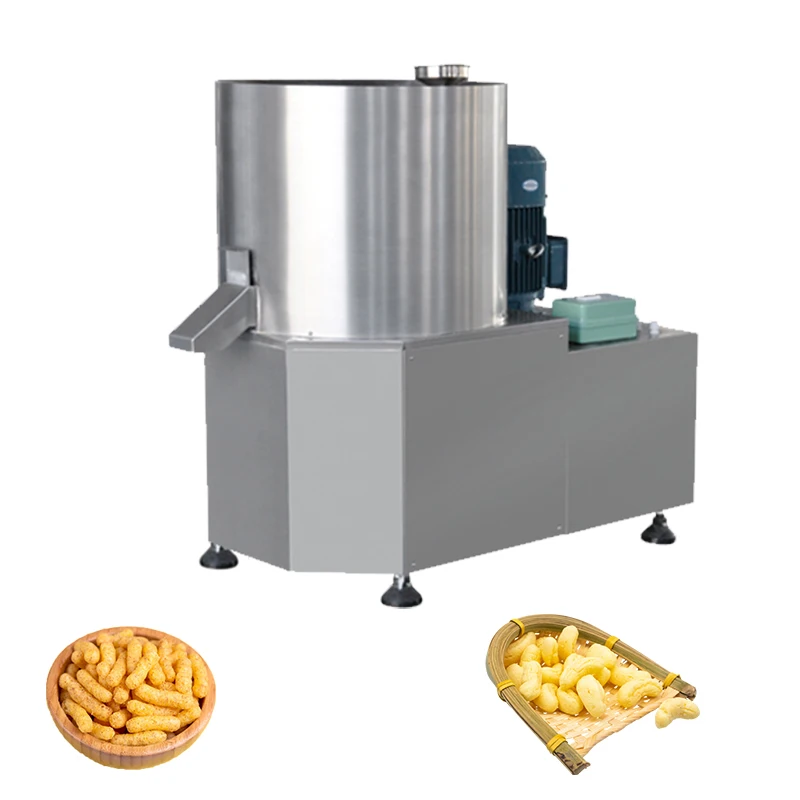
MT70 / MT85 / MT75 Twin Screw Extrusion Puffed Snack Production Line, 130–220 kW, PLC & MCC Control — engineered as a complete turnkey system from mixing through packing, with throughput balanced across every station to prevent bottlenecks. Screw configuration and interchangeable die geometry are matched to your specific flour blend and target snack shape, controlling expansion, density and texture. In-house trial runs on your raw material validate output before shipment.
Description
Throughput-Matched Integration — every station from the twin-screw extruder through the dryer, coating drum and packer is balanced to your raw material and target snack geometry so no single unit chokes the line.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extrusion Puffed Snack Production Line |
| Models Available | MT70 / MT85 / MT75 |
| Extruder Type | Twin Screw |
| Installed Power | 130 kW (MT70) / 180 kW (MT85) / 220 kW (MT75) |
| Power Consumption | 95 kW (MT70) / 120 kW (MT85) / 130 kW (MT75) |
| Output Capacity | 100–120 kg/h (MT70, basis to be confirmed) / 200–300 kg/h (MT85, basis to be confirmed) / 300–500 kg/h (MT75, basis to be confirmed) |
| Overall Dimensions (L×W×H) | 21 × 1.5 × 2.2 m (MT70) / 25 × 1.5 × 2.2 m (MT85) / 28 × 1.5 × 2.2 m (MT75) |
| Control System | PLC and MCC |
| Screw Material | Special alloy steel, wear-resistant |
| Lubrication | Automatic lubricating system |
| Cooling | Integrated cooling function |
| Dryer Heating Source | Gas / Electric |
| Coating System | Double tumble with sugar melting, elevator, coating drum, spraying nozzle |
| Line Stations | Mixing → Extruding → Drying → Coating / Flavouring → Cooling → Packing |
| Die Configuration | Interchangeable dies for multiple shapes (ball, tube, stick, ring, fruit loop, star, wheel, flower, heart) |
| Raw Materials | Corn, rice, wheat, oat, barley flour |
| Assembly State | Complete line |
| Voltage & Frequency | Customized to local supply |
| Factory Layout | Customized to buyer’s factory size |
| Standards | CE (since 2014), ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn puffs and cheese balls for retail snack packs | Corn flour, rice flour with cheese or seasoning coating |
| Cereal rings and fruit loops for breakfast cereal lines | Wheat, oat and mixed grain flour blends |
| Extruded sticks and tubes for foodservice and vending | Corn and barley flour with savoury flavouring |
| Star, wheel and heart-shaped snacks for children’s ranges | Rice and wheat composite flour |
| Pilot-scale new format development | Any supported flour blend at MT70 capacity tier |
What "Rated Capacity" Leaves Out on a Puffed Snack Production Line
Output figures only matter when tied to your exact flour blend, moisture content and target expansion ratio.
I remember standing on a workshop floor in the Pearl River Delta watching a puffed snack line stall on its third hour. The supplier had rated the line on pure corn grits at a fixed moisture level, but the buyer was running a mixed grain blend with higher fibre and different starch behaviour. The extruder barrel temperature profile was wrong for that material, the die orifice was too restrictive, and the downstream dryer could not keep up with the moisture load. Two weeks of re-tuning followed [NEED_CITE: raw material variability in extrusion processing]. A puffed snack production line turnkey is only as reliable as the trial that validated it.
Matching the Screw Profile to Your Flour Blend
The twin-screw extruder sits at the centre of this puffed snack production line turnkey. Screw configuration — the sequence of conveying, kneading and reverse elements inside the barrel — determines how much shear and residence time the material receives. Corn flour with high starch content gelatinises readily and needs a moderate shear profile, while an oat-heavy blend with more fibre and fat requires a more aggressive kneading block arrangement to achieve consistent expansion. The screw combination is specified to the buyer’s raw material rather than copied from a generic build.
Balancing Every Station Against the Extruder Output
A common failure on snack lines is a mismatch between extruder throughput and downstream capacity. If the dryer cannot remove moisture fast enough, the coating drum receives product that is still too warm and the seasoning clumps. On this line, the dryer, double-tumble coating system, cooler and packing station are all sized to the extruder’s verified output on the buyer’s formulation. The PLC and MCC control system coordinates start-up and shut-down sequences across stations so material does not accumulate or starve at any transfer point [NEED_CITE: throughput balancing in continuous food processing lines].
Reading the Spec Sheet: What Matters for Snack Extrusion
Three parameters deserve close attention when comparing extruder models for puffed snack production. Installed power — ranging from 130 kW on the MT70 to 220 kW on the MT75 — dictates the mechanical energy available for shear and cooking inside the barrel. The length-to-diameter ratio of the screws, implicit in the overall machine dimensions, controls residence time: longer barrels give more dwell for thorough starch gelatinisation but require more precise temperature zoning. Interchangeable dies allow a single extruder platform to produce balls, tubes, rings, stars and other geometries simply by swapping the die plate and adjusting the cutter speed, avoiding the need for dedicated machines per shape. The automatic lubricating system and integrated barrel cooling maintain stable operating conditions during continuous shifts, reducing the drift in product density that typically appears after several hours of run time.
The Cost of Skipping the Trial Run
Buying an extruder on paper capacity without a pre-shipment trial on your actual flour blend is one of the most expensive shortcuts in snack manufacturing. The screw combination, die selection, barrel temperature zones and dryer settings all interact with the specific starch-protein-fat balance of your raw material. When these are guessed at the factory and corrected on site, commissioning stretches from days into weeks. Operators lose confidence, raw material is wasted, and the first production batches fall outside the texture and density your market expects [NEED_CITE: extrusion commissioning delays due to untested material profiles]. Every hour spent re-tuning on site is an hour of lost saleable output.
Why Source This Line Here
Complete lines from mixing through packing come under a single supplier, so throughput is matched across every station rather than assembled from separate vendors who each guarantee only their own unit. Screw configuration and die design are specified to the buyer’s raw material and target product shape, not pulled from a catalogue default. An in-house testing workshop allows trial runs on the buyer’s actual flour blend before the line ships, producing a documented trial report that confirms expansion ratio, texture and achievable output. Twin-screw expertise spans pet food, aquatic feed, snacks, cereals, starch and protein applications, meaning the engineering team has encountered a wide range of material behaviours. Pre-sales consultation extends through layout design, on-site installation, commissioning and ongoing maintenance, so the same engineering group that configured the line supports it after start-up.
Documentation & Verification
- Line layout drawing matched to your factory floor dimensions and utility connections
- Screw and die configuration record documenting element sequence for your flour blend
- Trial run report on your raw material confirming expansion ratio and output before dispatch
- Electrical schematic with voltage, frequency and PLC language confirmed to your site
- Operation and maintenance manual covering all stations from mixer to packer
- Wear parts list identifying screw elements, die plates and seals for first replacement cycle
Installation, Commissioning & Support
- Foundation and floor space planned to the line’s 21–28 m length depending on model tier
- Dedicated power circuit sized to the MT75 peak draw of 220 kW installed capacity
- Modular station delivery allowing phased assembly in workshops with limited door clearance
- First-run parameter setting covering barrel temperature zones, screw speed and die selection
- Operator training on PLC interface, die changeover and coating drum adjustment
- Scheduled spare parts supply for wear-prone screw elements and die plates
Preparing Your Inquiry
To configure the right puffed snack production line turnkey for your facility, share your target snack format and the flour blend you intend to run, including moisture range and any additives. Confirm your local voltage and frequency, the control language your operators need, and the available floor space with ceiling height. If you have existing upstream mixers or downstream packing equipment, provide their throughput ratings so the new line can integrate without bottlenecks.
Frequently Asked Questions
Q: How is output capacity verified, and on which raw material formulation?
A: Output figures are validated through an in-house trial run using your specific flour blend at your stated moisture content. The trial report documents the actual throughput, expansion ratio and product density achieved, so the capacity you see is tied to your material rather than a generic test grain.
Q: How are screw configuration and die design matched to my flour blend and snack shape?
A: The screw element sequence — conveying, kneading and reverse blocks — is selected based on your raw material’s starch, protein and fibre profile. The die plate orifice and cutter speed are then paired to produce your target geometry, whether rings, balls, sticks or stars.
Q: What voltage, frequency and PLC language options are confirmed before production?
A: Before the line enters production, the electrical schematic is finalised to your site’s voltage and frequency. The PLC interface language is set to match your operators, preventing commissioning delays caused by untranslated alarms or parameter screens.
Q: Can I run a trial on my own raw material before the line ships?
A: Yes. The in-house testing workshop runs your flour blend through the configured extruder and downstream stations. You receive a trial report covering output rate, product texture and expansion data before the equipment leaves the factory.
Q: How is throughput balanced between the extruder, dryer, coating drum and packing station?
A: Each station is sized to the extruder’s verified output on your formulation. The dryer capacity matches the moisture load, the coating drum handles the product volume per batch, and the packing station speed aligns with the cooler discharge rate, preventing material backlog at any transfer point.
Related products
-

New Stainless Steel Automatic Snack Food Machinery Extruder Puffed Corn Maize Puff Processing Line for Food Industry High
¥12,350.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Puffed Food Snack Machine Electric Corn Puffs Snacks Making Machinery New Condition Flavorful Puff Snack Production
¥7,550.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puffed Snacks Seasoning Flavor Machine Twin Screw Corn Puffing Food Making Extruder Equipment
¥8,355.00 Select options This product has multiple variants. The options may be chosen on the product page -

Hot Sale Corn Snack Extruder Puffed Snacks Production Machine Corn Puffs Making Machine
¥20,000.00 Select options This product has multiple variants. The options may be chosen on the product page