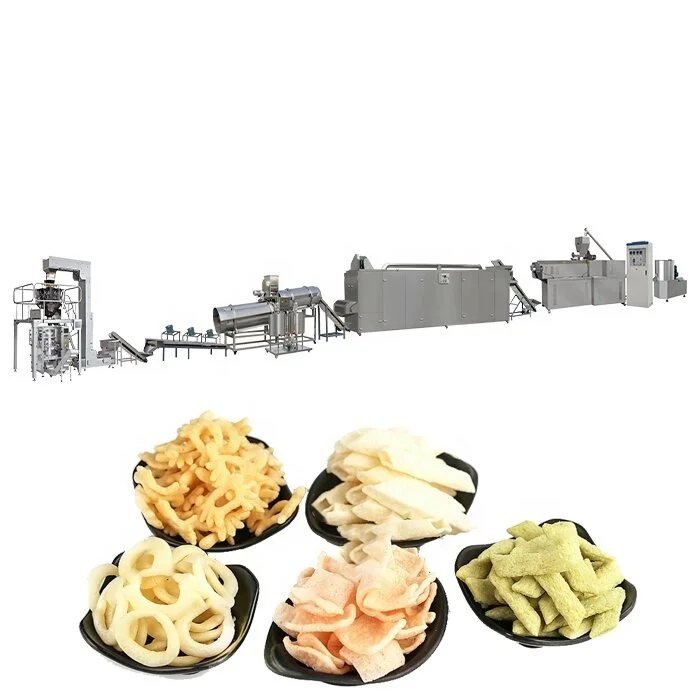
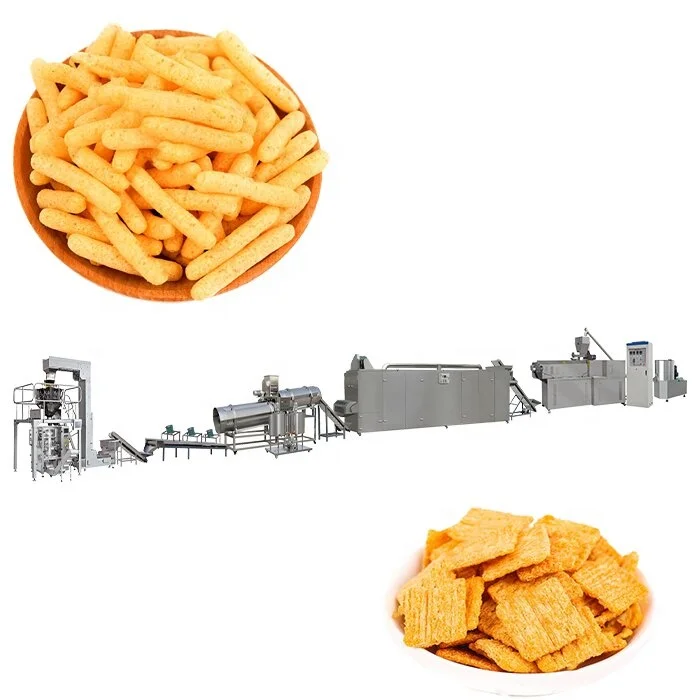
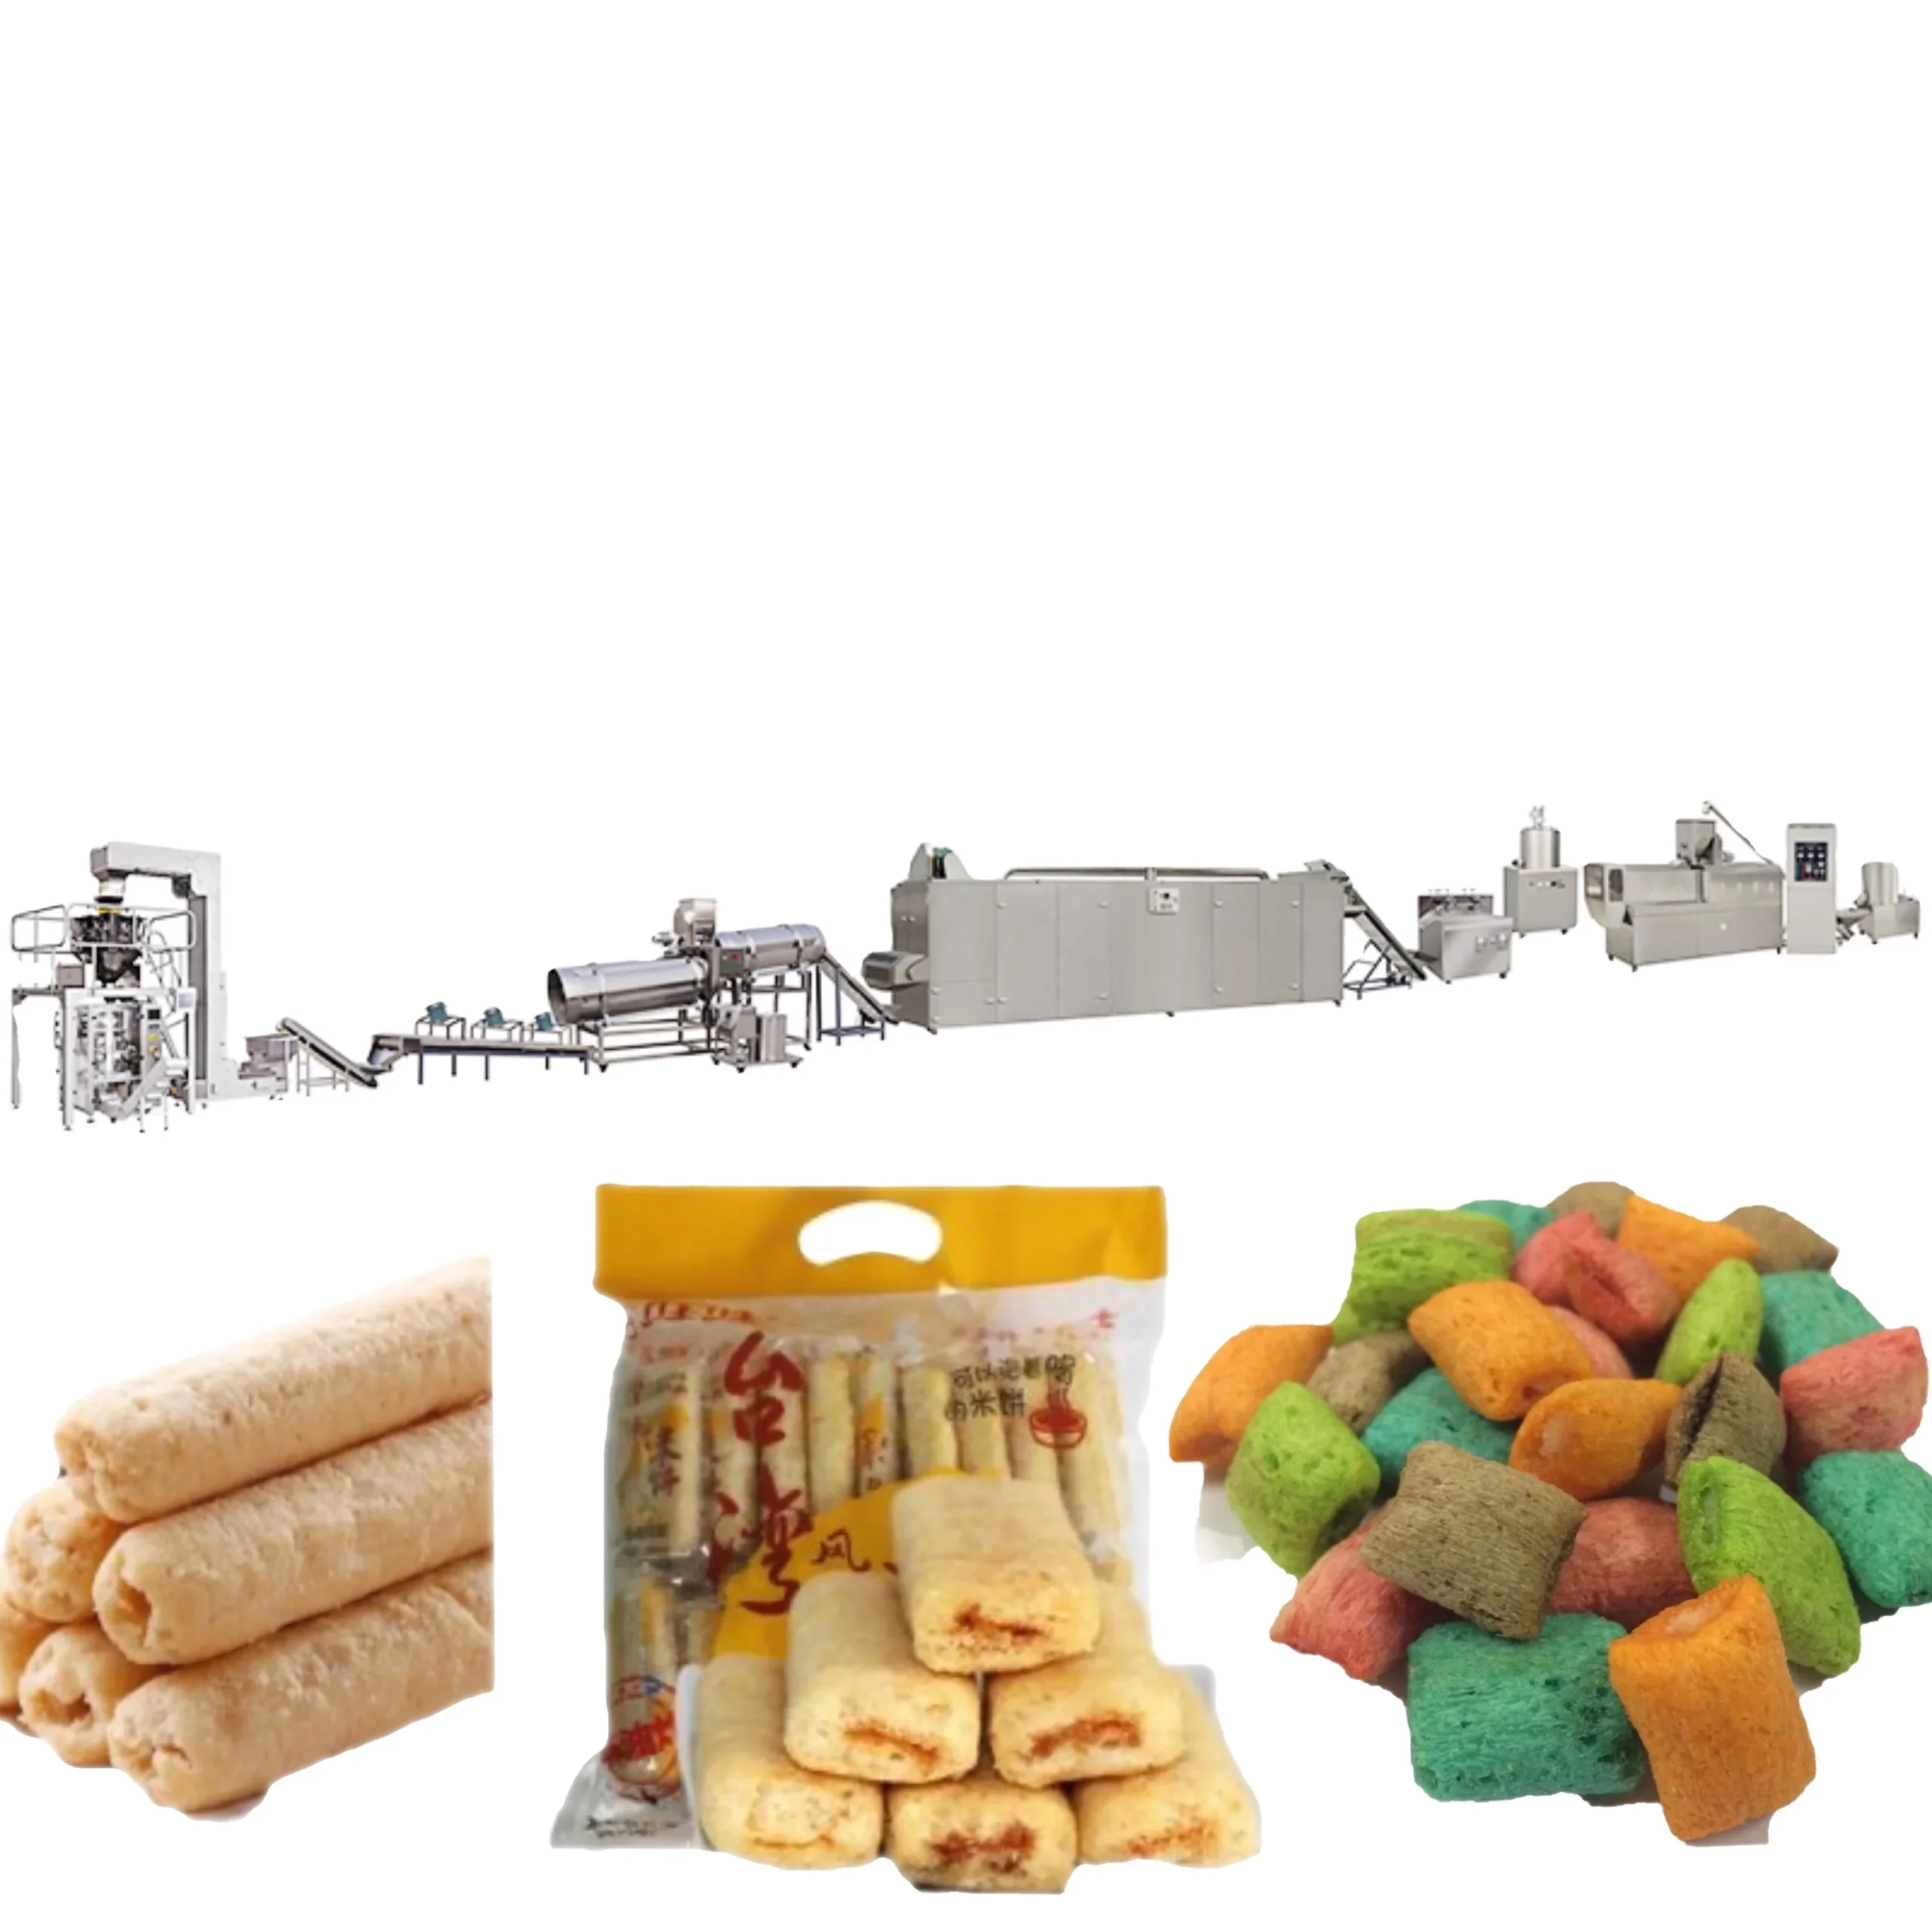
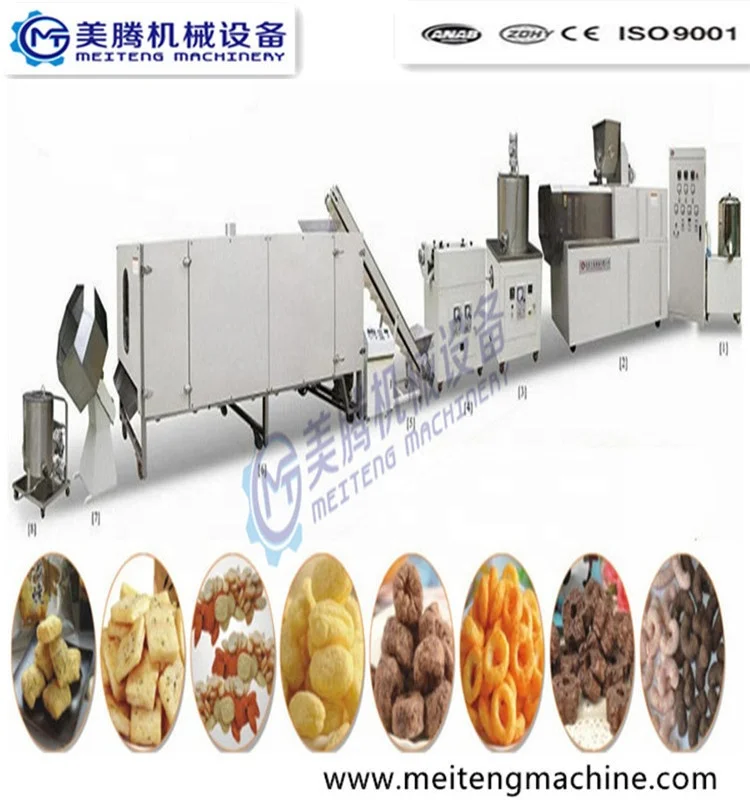
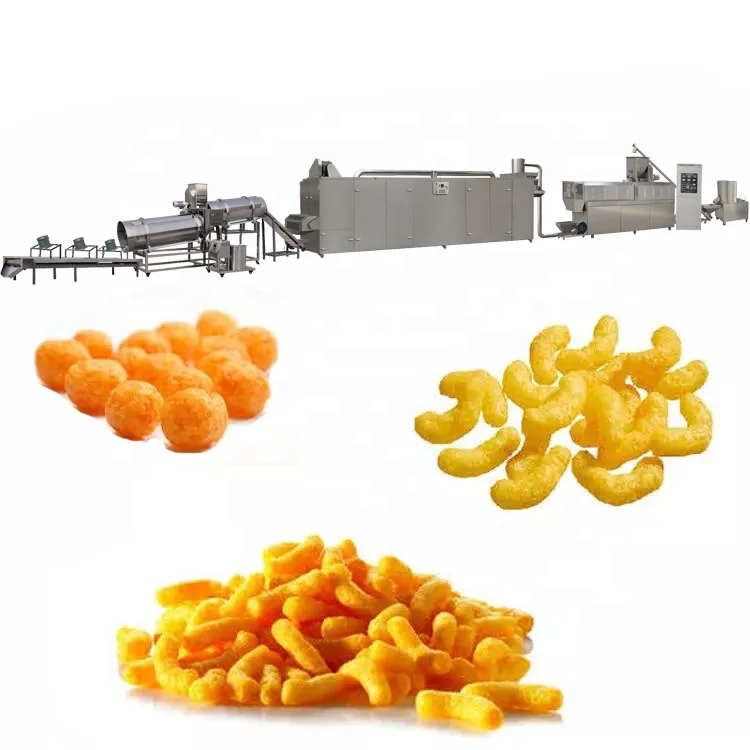
MT65 / MT70 / MT85 Twin Screw Snack Food Extrusion Line — turnkey configuration from mixer to packing with Siemens main motor, five-layer SUS mesh belt dryer, and interchangeable die system. Complete line throughput is calculated across every station to match your corn or rice formulation, with screw configuration and barrel temperature profile specified to target puff density and expansion. In-house trial runs on your raw material verify output before shipment.
- Nitriding-treated barrel and screw with self-cleaning design for fast changeover
- PLC and MCC control with speed-adjusted inverter on feeding, extrusion, and cutting
- CE and ISO certified, 24-month warranty with lifetime service support
Description
Turnkey Line Accountability — Every station on the MT65 / MT70 / MT85 snack food extrusion line is throughput-balanced by one supplier, so extruder output, dryer residence time, and flavoring drum capacity align to your actual recipe rather than to catalog assumptions.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 |
| Product Type | Twin Screw Snack Food Extrusion Line |
| Screw Type | Twin-screw |
| Installed Power | MT65 — 70 kW; MT70 — 100 kW; MT85 — 200 kW |
| Real Power Consumption | MT65 — 40 kW; MT70 — 70 kW; MT85 — 150 kW |
| Output Capacity | MT65 — 100–150 kg/h (basis not stated in source); MT70 — 200–240 kg/h (basis not stated in source); MT85 — 300–400 kg/h (basis not stated in source) |
| Overall Dimensions (L×W×H) | MT65 — 20,000 × 1,200 × 2,200 mm; MT70 — 25,000 × 1,500 × 2,200 mm; MT85 — 30,000 × 3,500 × 4,300 mm |
| Main Motor | Siemens brand |
| Control System | Speed-adjusted inverter on feeding, extrusion, and cutting systems |
| Gearbox | Automatic lubrication function |
| Barrel & Screw Treatment | Nitriding process, high strength, wear-resistant, self-cleaning |
| Cutting System | Rotary knife on die head seat, V-belt drive |
| Feeding System | Food-grade stainless steel twin-screw feeder |
| Dryer | Five-layer mesh belt, SUS construction, auto temp control up to 160°C, electric / gas / oil heating options |
| Cooler | Stainless steel belt, 450 mm width, fan-assisted, 6,000 × 600 × 800 mm |
| Screw Conveyor | 1.1 kW, 2,500 × 500 × 2,000 mm, stainless steel sealed roller |
| Flavoring System | Semi-automatic or automatic, compatible with sugar, oil, and powder seasoning |
| Die Configuration | Interchangeable molds — flowers, stars, wheels, squares, hearts, rings, strips, custom shapes |
| Certifications | CE, ISO |
| Warranty | 24 months, lifetime service |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn puff and Nik Naks production | Corn grits, corn meal with adjustable moisture conditioning |
| Rice puff and rice crisp snacks | Rice flour, rice grits, broken rice blends |
| Core-filled snack pillows | Grain-based shell with cream, chocolate, or fruit filling |
| Multi-grain extruded shapes | Blends of wheat, oat, sorghum, and maize |
| 2D and 3D pellet snacks | Starch-based formulations for secondary puffing |
What "300 kg/h" Means When Your Corn Grits Arrive Wet
Capacity figures on an extruder nameplate assume a reference moisture and granulation that your actual shipment may not match.
Last year I configured a corn puff line for a Southeast Asian buyer who ordered based on catalog output. When his corn grits arrived at the testing workshop, moisture content ran noticeably higher than the typical range. Extrusion expansion dropped, and throughput fell well short of the nameplate figure during the trial. We reconfigured the screw combination, adjusted the die bore, and re-ran the material before the line shipped. That snack food extrusion production line turnkey project left the factory with verified throughput on his specific formulation, not an assumption from a generic test [NEED_CITE: moisture variability in tropical grain supply chains].
When a line is assembled from separate vendors, nobody takes responsibility for the gap between quoted and actual capacity. The extruder supplier blames the dryer, the dryer supplier blames the upstream feeder, and the buyer absorbs the lost production hours during commissioning.
Throughput Matching Across Every Station
A snack food extrusion production line turnkey project fails the moment one station runs slower than the rest. The extruder pushes product into a dryer that cannot evaporate moisture fast enough, or the flavoring drum cannot coat at the rate the extruder delivers. On the MT65 / MT70 / MT85 configuration, each station is selected so its processing capacity aligns with the extruder output for your target product format. The five-layer mesh belt dryer provides sufficient residence time and surface area, while the cooling conveyor and flavoring system are sized to keep pace without product backlog or idle time.
Raw Material Behavior Before the Line Ships
Corn, rice, and multi-grain blends each respond differently to shear, temperature, and moisture inside the barrel. A screw combination that produces open-cell corn curls will compress rice puffs into dense pellets. The testing workshop allows trial runs on your actual raw material before the line leaves the factory. Screw elements are rearranged, die geometry is adjusted, and dryer temperature profiles are logged — so product development happens at the machine, not on your factory floor weeks after delivery [NEED_CITE: twin-screw extrusion screw configuration principles for snack applications].
Barrel Metallurgy and Process Stability
The nitriding treatment on the barrel and screw elements provides surface hardness that resists abrasive wear from corn and rice grits over extended production campaigns. Self-cleaning screw geometry reduces material carryover when switching between recipes or colors, cutting changeover time between runs. The Siemens main motor paired with inverter-driven feeding and cutting maintains consistent screw speed and knife rotation, which directly governs product length uniformity and density batch after batch. Interchangeable die plates allow format changes — rings, stars, strips, custom profiles — without mechanical modification to the extruder barrel or drive train.
When the Die and Dryer Are an Afterthought
A snack producer who selects an extruder on motor power alone often discovers that the downstream dryer cannot keep up with the moisture load. Product exits the die at high moisture and must be dried to a shelf-stable level; if the dryer is undersized, the line backs up and operators throttle the extruder down, losing the throughput they paid for [NEED_CITE: dryer capacity calculation for extruded snack moisture removal]. Flavoring drums that cannot tumble fast enough leave uneven seasoning coverage, generating off-spec product that must be reprocessed or discarded. These mismatches surface only during commissioning, when the line is already bolted to your floor and the vendor’s installation crew is counting days.
Why Source the Full Line Under One Supplier
The MT65 / MT70 / MT85 line arrives with every station — mixer, screw conveyor, extruder, vibrating cooler, dryer, flavoring system, cooling machine, packing interface — designed as a single throughput chain. One supplier means one warranty accountability point and one commissioning schedule. The screw configuration and die design are specified to your raw material, not copied from a generic build library. In-house testing on your actual formulation verifies expansion, texture, and output before the crate is sealed. Electrical schematics confirm voltage, frequency, and control language for your market before production begins, avoiding the delay of rewiring a control panel on-site. Documentation covers the full chain — layout drawings, capacity calculations, trial run reports, wear parts lists — so your maintenance team has references from day one.
Documentation & Verification
- Line layout showing station sequence and throughput calculation for your snack format
- Trial run report on your raw material with screw and die configuration record
- Electrical schematic confirming voltage, frequency, and HMI language before production
- Factory test record covering every station from mixer to packing interface
- CE declaration of conformity and ISO certificate for the complete line
- Wear parts list with part numbers for screws, dies, knives, and mesh belt sections
Installation, Commissioning & Support
- Foundation and utility plan reflecting the MT85 line footprint of up to 30,000 × 3,500 mm
- Dedicated power circuit sized for the model’s real consumption up to 150 kW
- Phased mechanical assembly with extruder, dryer, and cooler aligned on-site
- First-run parameter setting using trial-run data from the factory test
- Operator training covering die changes, screw cleaning, and inverter adjustment
- Spare wear parts inventory — screws, die plates, rotary knives — supplied with initial shipment
Preparing a Useful Inquiry
To configure a line that matches your production target, share your primary raw material and its typical moisture range, the snack format you intend to produce, and your target hourly output. Include your local voltage and frequency standard, preferred control language, and whether your facility uses electric, gas, or thermal oil heating for the dryer. If you have existing upstream or downstream equipment that must integrate, specify its capacity and interface dimensions.
Frequently Asked Questions
Q: How is line capacity verified on my specific raw material before shipment?
A: We run your actual raw material through the extruder in the testing workshop, adjusting screw configuration, die bore, and dryer temperature until the target expansion and throughput are achieved. A trial run report documenting these settings ships with the line, so commissioning starts from a known baseline rather than a generic parameter set.
Q: How do you match throughput between extruder, dryer, and flavoring stations?
A: Each station is selected based on the extruder output for your specific product format. The five-layer mesh belt dryer is sized for the moisture load your recipe generates, and the flavoring drum volume and rotation speed are calculated to coat at the extruder delivery rate without bottlenecks or idle gaps.
Q: What does phased installation and commissioning look like for a complete line?
A: Mechanical assembly begins with extruder and dryer alignment, followed by upstream mixing and downstream cooling stations. Electrical connections and inverter calibration come next, then trial runs using the factory-verified parameters. Operator training covers die changes, screw cleaning, and routine maintenance across all stations before handover.
Q: How are screw configuration and die design selected for my target snack format?
A: Screw element arrangement — conveying, kneading, and reverse-flight sections — is designed around your raw material’s starch gelatinization behavior and target expansion. Die geometry is matched to the product shape and density your market expects, then validated during the in-house trial run before the line ships.
Q: What spare wear parts are included, and how are replacements supplied?
A: The initial shipment includes spare screw elements, die plates, rotary knives, and mesh belt sections identified in the wear parts list. Replacement parts are manufactured to the same nitriding specification and can be ordered against the part numbers in your documentation package for direct shipment.
Related products
-

Automatic High Productivity Puffed Corn Snacks Extruder Production Equipment New Condition Puff Snack Food Making Machine
¥11,050.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Corn Crisps Extruder Production Machine for Maize Chips and Corn Sticks New Condition
¥8,000.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Puffed Food Snack Machine Electric Corn Puffs Snacks Making Machinery New Condition Flavorful Puff Snack Production
¥7,550.00 Select options This product has multiple variants. The options may be chosen on the product page -

Automatic Puff Corn Snack Stick Production Line Equipment New Condition Machines
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page