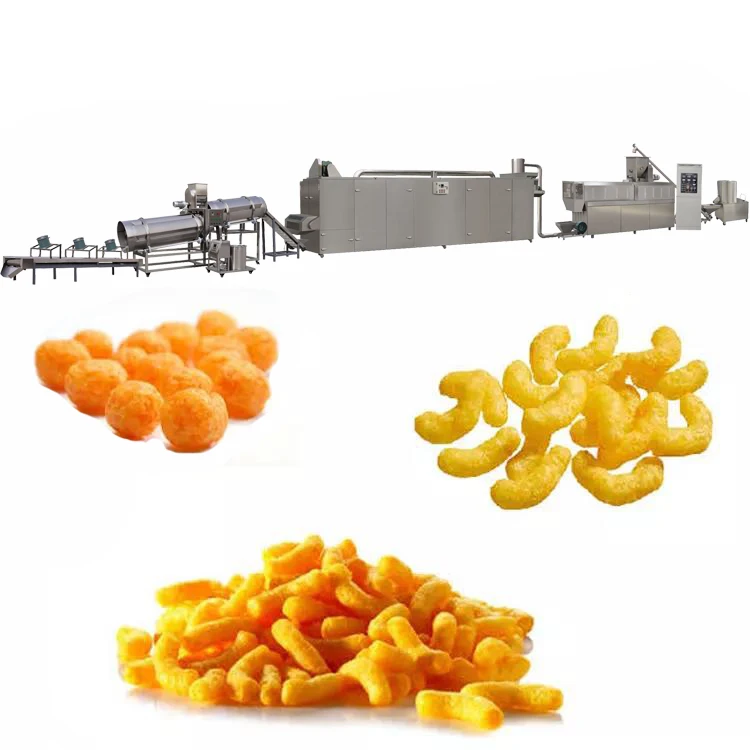
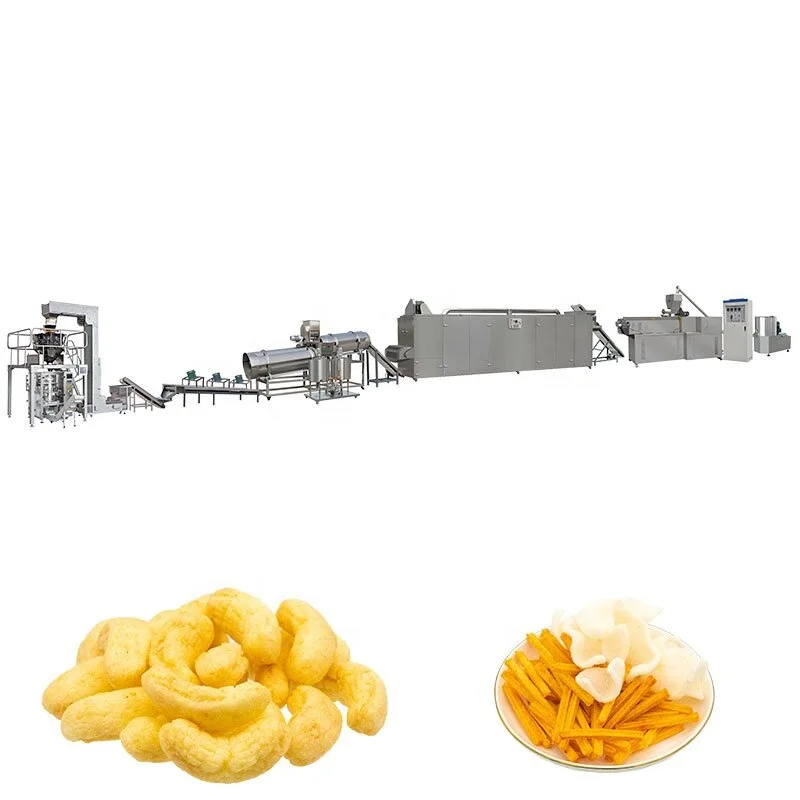
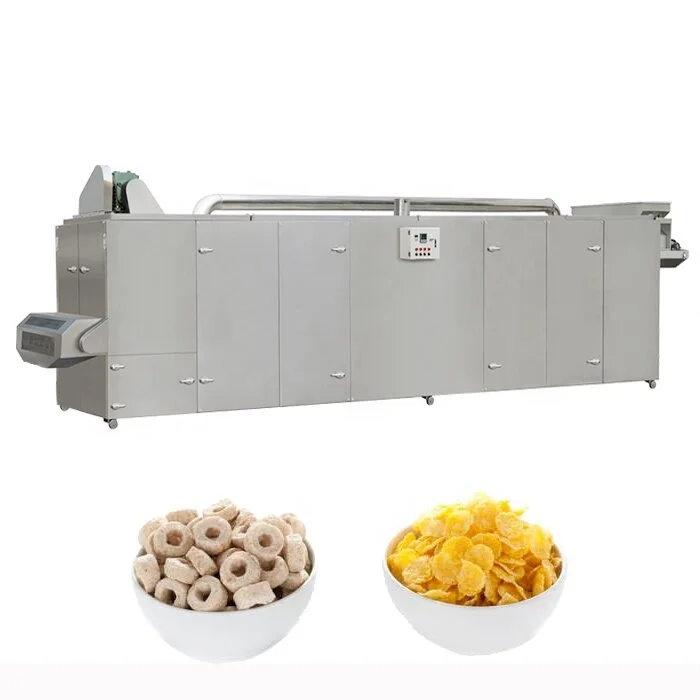
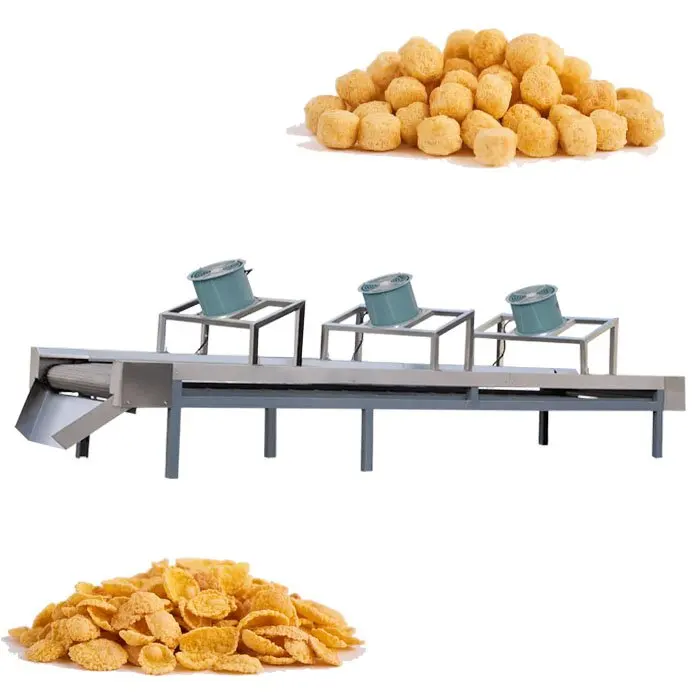
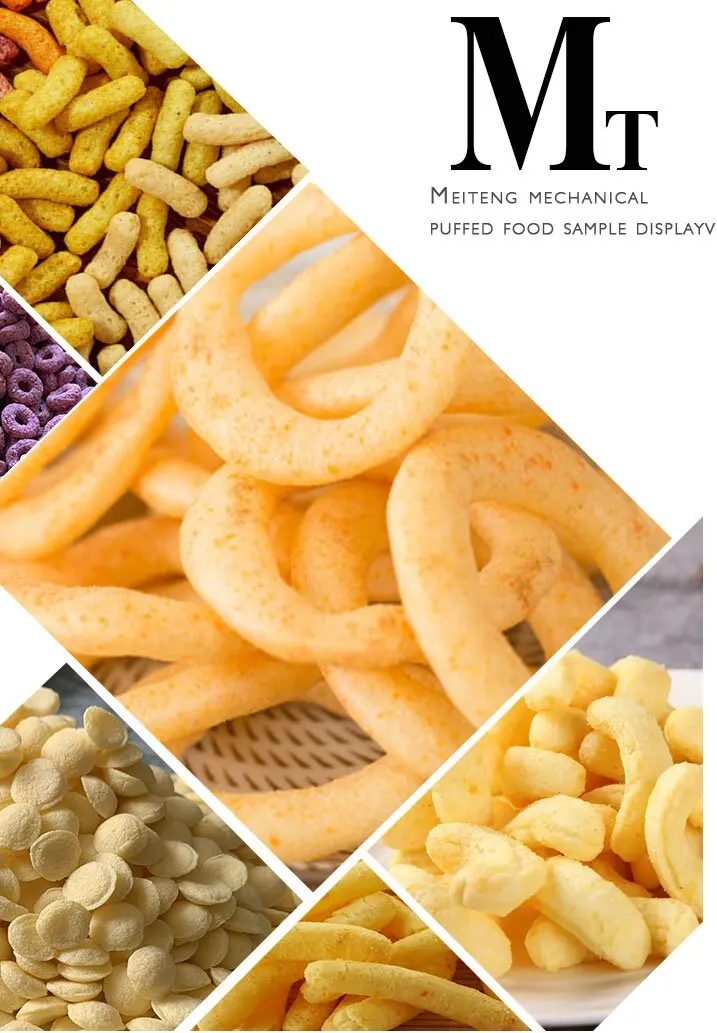
Twin Screw Puffed Snack Food Extrusion Line, Automatic PLC Control, Customizable Dryer & Flavoring — integrated from mixing through extruding, drying, and flavoring with throughput matched at every station.
- Screw configuration and die design specified to your raw material formulation and target product density
- Dryer length and layer count customized to moisture removal requirements for consistent puffing texture
- Semi-automatic or full-automatic flavoring system selected based on snack type and production scale
As a turnkey project, the complete line layout is engineered with matched station capacity, utility planning, and phased installation — verified through trial runs on your actual ingredients in our testing workshop before shipment.
Description
Integrated Throughput Matching — Every station from mixing through flavoring is calculated as one system so the extruder never starves a dryer or overfeeds a coating drum on your puffed corn snack production line turnkey project.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Puffed Snack Food Extrusion Line |
| Screw Type | Twin-screw (double screw extruder) |
| Line Stations | Mixing → Extruding → Shaping → Cutting → Drying → Flavoring |
| Control System | Automatic with PLC and MCC options (basis to be confirmed) |
| Flavoring System | Sugar, oil, and powder seasoning; semi-automatic or automatic |
| Dryer Configuration | Customizable length and layer count per product moisture target |
| Output Capacity | Rated capacity based on raw material formulation and moisture content (basis to be confirmed) |
| Voltage & Frequency | Configurable to target market (basis to be confirmed) |
| Screw & Die Setup | Matched to raw material and target product shape, size, and density |
| Product Shape & Size | Selectable via die and cutter configuration |
| Warranty | 24 months with lifetime service support |
| Language Options | English operation, service, and maintenance manuals |
| Installation | On-site overseas commissioning with 1–2 dispatched engineers |
| Certification | CE, ISO (electronic edition available for export documentation) |
Application Suitability
| Application | Material or Output |
|---|---|
| Puffed corn snacks and maize-based extruded formats | Corn grits, maize flour, grain blends |
| Core-filled snack products | Grain-based shell with cream, chocolate, or fruit filling |
| Puffed rice snacks | Rice flour, rice grits, blended rice formulations |
| Shaped puffed snack formats | Various grain formulations producing rings, balls, pillows, stars |
Why Nominal Capacity Numbers Mislead Snack Producers
A puffed corn snack production line turnkey project quoted on a single output figure often collapses when the buyer switches to their own grain blend, moisture level, or target density. Real throughput is verified only when the line runs your exact formulation through every station.
I once watched a corn extrusion line stall at the dryer because the upstream extruder pushed product faster than the three-layer oven could handle. The manufacturer had sized each station independently. The extruder hit its rated number, but the finished output fell short because the dryer became a bottleneck. Mismatched stations like this show up more often than buyers expect, especially when equipment is assembled from separate vendors rather than designed as one integrated project. [NEED_CITE: throughput matching principles in multi-station food processing lines]
Screw Configuration Dictates Your Snack Texture, Not the Brochure
The twin-screw extruder at the heart of this line accepts a configurable screw arrangement and die plate designed around your raw material behavior. Corn grits gelatinize differently than rice flour under shear and heat, and a screw profile copied from a generic build will produce the wrong expansion or leave dense, undercooked centers. The screw elements are selected and sequenced so that starch gelatinization completes before the material reaches the die face, giving you consistent puff structure across long production runs. This is where a puffed corn snack production line turnkey project either succeeds or fails before product ever leaves the barrel.
Drying and Flavoring Are Not Afterthoughts in Line Design
The dryer on this line is built with adjustable length and layer count because different puffed formats carry different moisture loads out of the die. A high-moisture core-filled pillow needs more residence time than a thin corn ring, and a dryer that is too short leaves product soggy or forces the line to slow down. Downstream, the flavoring station offers semi-automatic and automatic options depending on whether you are applying oil and powder in sequence or running a single-pass sugar glaze. Each station must accept the full output of the one before it without accumulation or starvation, which is why the entire puffed corn snack production line turnkey configuration is calculated as one continuous system rather than a collection of independent machines. [NEED_CITE: moisture removal requirements for extruded snack products by format]
Reading the Specs That Actually Shape Your Product
The twin-screw design matters here because single-screw extruders struggle with mixed-grain formulations that vary in particle size and fat content — the self-wiping action of intermeshing twin screws keeps material moving uniformly and prevents burn-on inside the barrel. The die and cutter configuration determines not just shape but also product density, since die orifice diameter combined with cutter speed controls the length and expansion ratio of each piece. Moisture content entering the extruder directly affects expansion behavior, and the PLC-based control system lets operators hold temperature profiles and feed rates steady across shifts so that batch-to-batch variation stays within specification. Voltage and frequency confirmation before build ensures the motor and heating elements match local supply without requiring field transformers that add failure points.
What Happens When the Line Is Assembled from Separate Vendors
Buyers who source an extruder from one supplier, a dryer from another, and a flavoring drum from a third often discover during commissioning that the stations do not communicate or pace each other correctly. The extruder runs at full output while the dryer falls behind, forcing operators to idle the upstream machine and lose effective capacity. Flavoring drums sized for a lower throughput leave product under-coated, and conveyors between mismatched stations drop product or create surges. These problems are expensive to fix after installation because they require mechanical modifications, additional buffer hoppers, or complete station replacements. [NEED_CITE: common commissioning failures in multi-vendor food processing lines]
Why Procuring This Line as One Project Changes the Outcome
Every station on this line is specified by the same engineering team that designs the layout, so throughput calculations flow from the mixer through the packing end as one document rather than several disconnected quotes. The screw and die configuration is set after reviewing your raw material data, not pulled from a standard catalog. An in-house testing workshop runs trial production on your actual formulation before the line ships, catching expansion or density issues before they become your problem on the factory floor. Electrical schematics are drawn to match your installation country’s voltage, frequency, and control language requirements so that commissioning starts with power-on rather than rewiring. The CE and ISO certification documentation travels with the shipment and satisfies customs and local regulatory review without delays.
Documentation & Verification
- Line layout drawing showing capacity calculation and throughput matching for every station
- Trial run report produced on your grain formulation in the testing workshop before shipment
- Screw and die configuration record matched to your target snack shape and density
- Electrical schematic with voltage and frequency confirmed for your installation country
- Operation and maintenance manual provided in English with wear parts list
Installation, Commissioning & Support
- Foundation and floor space plan drawn to the twin-screw extruder footprint and dryer length
- Dedicated power circuit sized to the confirmed motor rating and heating element load
- Line arrives in shipping segments with on-site assembly supervised by dispatched engineers
- First-run parameter setting on your raw material including barrel temperature profile and cutter speed
- Operator training covering screw changes, die swaps, and PLC screen navigation in English
- Wear parts inventory list for screws, dies, and cutter blades with reorder specifications
What to Prepare Before Requesting a Line Quotation
To configure a puffed corn snack production line turnkey project that matches your facility, share your target product format, the grain or blended formulation you plan to run, and your expected daily output volume. Confirm your workshop dimensions including ceiling height, the local voltage and frequency supply, and your preferred control language. If you have existing upstream batching or downstream packing equipment, note the interface points so the line layout connects without gaps.
Frequently Asked Questions
Q: How is line capacity verified against my specific raw material formulation and moisture content?
A: Before shipment, your grain formulation is run through the extruder and supporting stations in the in-house testing workshop. The trial documents actual throughput, expansion behavior, and product density on your material rather than relying on nominal figures calculated from a reference recipe.
Q: What is the process for screw and die configuration selection for different snack shapes and densities?
A: The screw element sequence and die plate are specified after reviewing your raw material composition, target expansion ratio, and finished product geometry. The configuration record is documented so you can replicate results or adjust for new formats later by swapping defined components.
Q: How is throughput matched between the extruder, dryer, and flavoring stations to avoid line bottlenecks?
A: Each station is calculated against the extruder output on your formulation, so the dryer length, layer count, and conveyor speed are sized to handle the full product flow without accumulation or idle time. The flavoring drum capacity is matched to the same rate.
Q: What does the turnkey project timeline look like from layout approval through phased installation and commissioning?
A: After line layout and specification approval, production and factory testing proceed over typical multi-week lead times. Engineers then travel to your site for assembly, first-run commissioning on your material, and operator training before handover.
Q: What utility planning is required for a complete puffed snack line?
A: You will need confirmed electrical supply at the agreed voltage and frequency, compressed air for pneumatic actuators, and floor space matching the approved layout drawing. Steam or hot air supply for the dryer is specified during the design phase based on your chosen dryer configuration.
Related products
-

Automatic Puff Corn Snack Stick Production Line Equipment New Condition Machines
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puffed Snacks Seasoning Flavor Machine Twin Screw Corn Puffing Food Making Extruder Equipment
¥8,355.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puff Corn Snacks Food Line Puffed Rice Ball Production Making Equipment Machines
¥10,565.00 Select options This product has multiple variants. The options may be chosen on the product page -

Twin Screw Corn Puffs Extruder Machine Small Corn Snack Food Extruder Machine
¥100.00 Select options This product has multiple variants. The options may be chosen on the product page