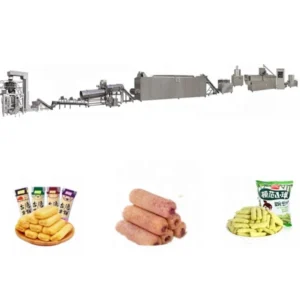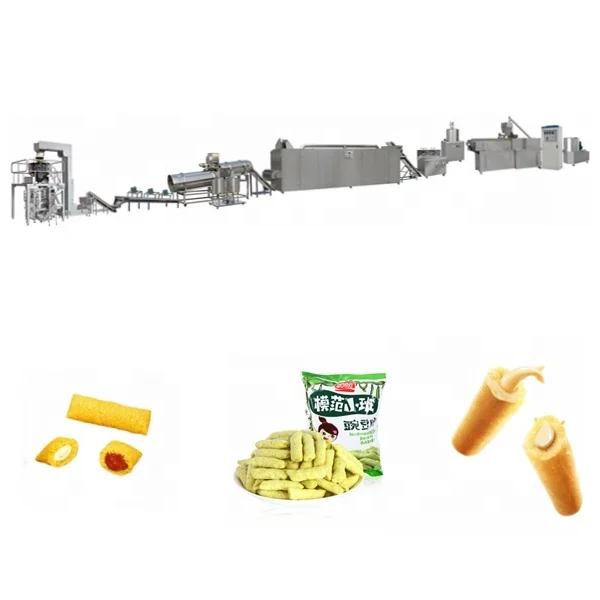
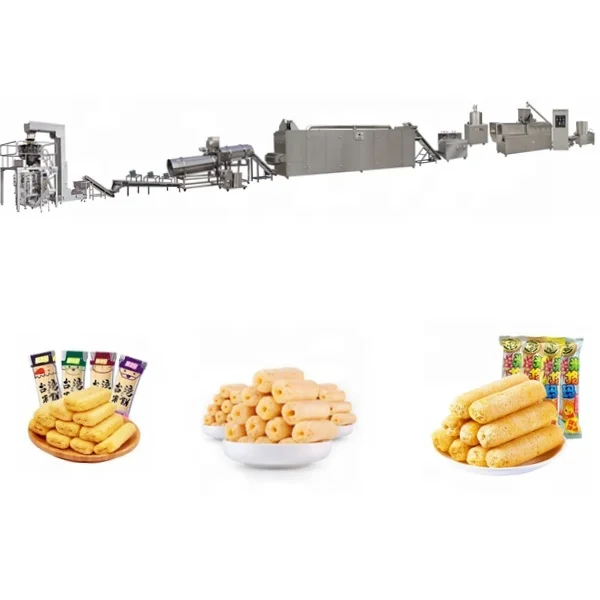
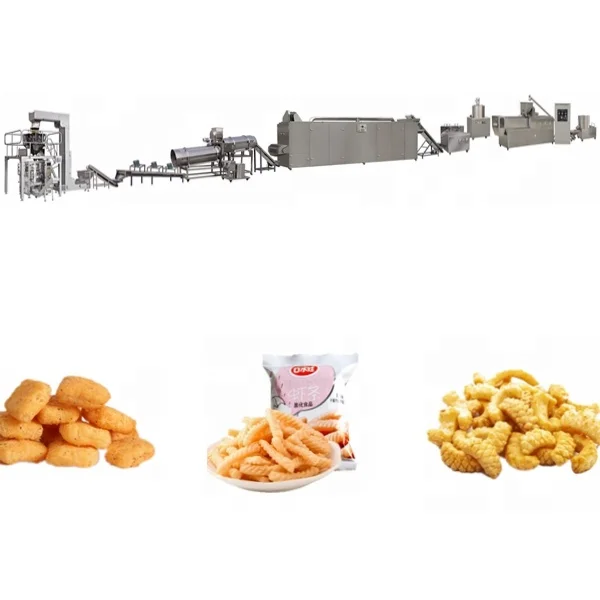
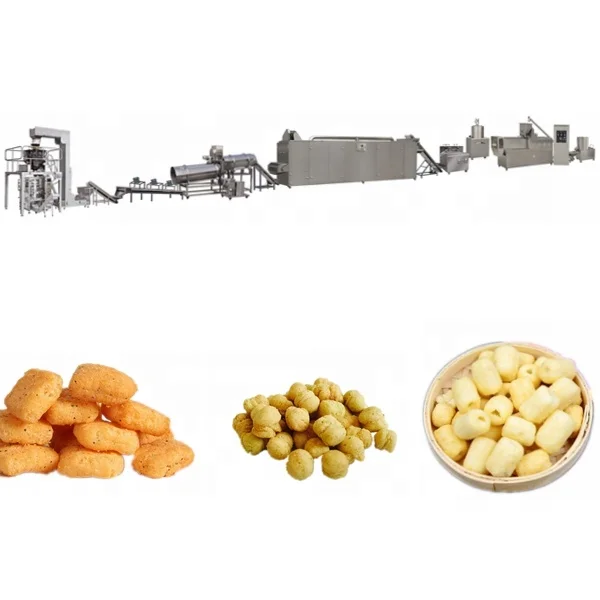
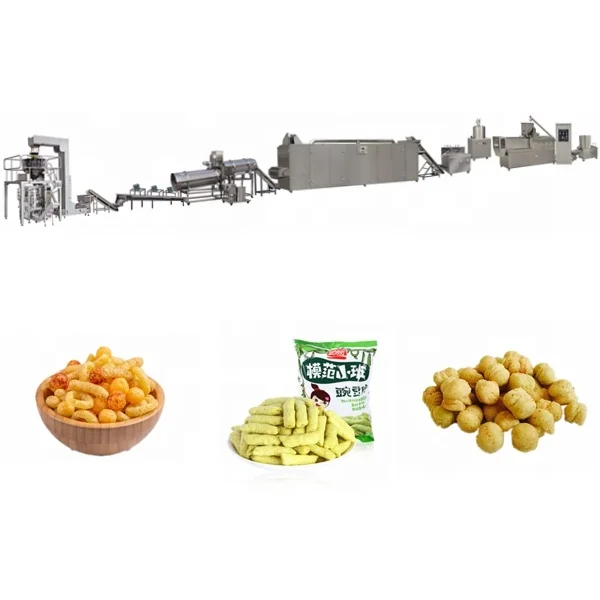
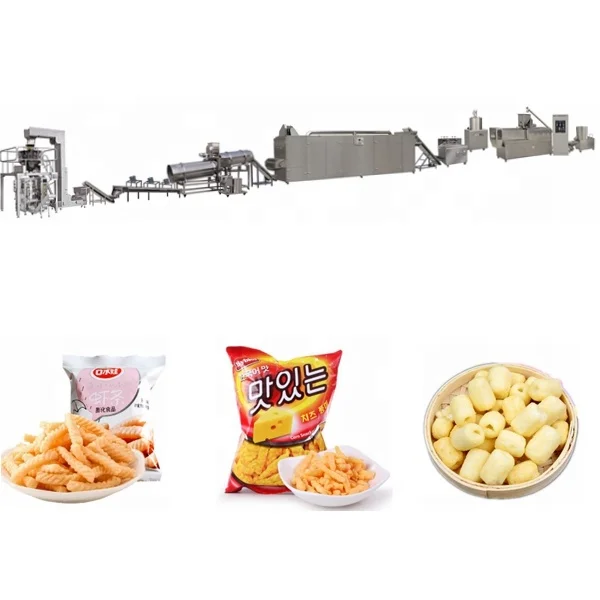
Twin Screw Puffed Snack Food Extrusion Line, Food-Grade SS304, 380V/50Hz, Siemens Motors — engineered for corn, wheat, rice and cereal-based puffed snacks, artificial rice and nutrition products.
This turnkey line matches throughput across mixing, extrusion, vibrate cooling, roasting and packing stations, with screw and die configuration specified to your raw material moisture, starch behaviour and target product density. Energy source selectable across electricity, gas, diesel or steam to fit your plant utilities.
- Layout and capacity calculation, trial run on your raw material, and screw configuration record delivered with the project.
Description
Line Throughput Alignment — every station from mixer through packing is capacity-matched to your cereal formulation, preventing the bottlenecks that occur when extruders are sourced separately from downstream equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Puffed Snack Food Extrusion Line |
| Screw Type | Twin screw (double screw) |
| Contact Material | Food grade stainless steel 201/304 |
| Voltage & Frequency | Three phase 380V/50Hz; Single phase 220V/50Hz (customizable to local voltage per country) |
| Electrical Components | Siemens (China-made) or top Chinese brand motors; Delixi or Delta inverters |
| Energy Source Options | Electricity / Gas / Diesel / Steam |
| Power (Electricity mode) | Approx. 100 kW (rated or peak not specified in source) |
| Power (Gas/Diesel mode) | Approx. 50–60 kW (rated or peak not specified in source) |
| Line Stations | Mixer → Extruder → Vibrate Cooler → Roasting Machine → Packing Machine |
| Assembly State | Complete line with supporting equipment |
| Output Capacity | (basis to be confirmed) |
| Control System | (to be confirmed) |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn and wheat puffed snack sticks | Corn grits, wheat flour, grain blends |
| Cheese balls and shaped extruded snacks | Cereal-based formulations with flavoring additions |
| Core-filled snacks | Twin-screw co-extrusion with cream or jam filling |
| Artificial and fortified rice | Rice flour, millet, buckwheat blended with vitamins, proteins and minerals |
| Multi-grain puffed cereal products | Brown rice, oat, sorghum and other cereal blends |
What Capacity Figures on Snack Extruders Actually Mean on Your Grain Blend
A rated throughput only holds when the screw profile, die geometry and barrel temperature match the starch composition of your specific raw material.
I learned this the hard way on a puff sticks line in Vietnam. The factory trial ran on corn flour and the numbers looked fine. The customer’s actual formula carried a heavy cassava starch load, and the moment we fed it on-site, expansion collapsed entirely. We had to rebuild the screw combination and temperature curve from scratch, losing two weeks before product met spec. That experience reshaped how I approach every turnkey puffed snack extrusion line project: trial runs must happen on the buyer’s own formula before the machines leave the workshop. Nominal capacity without a raw material basis is just a number on a nameplate [NEED_CITE: starch gelatinisation behaviour differences between corn, cassava and wheat under twin-screw extrusion].
Matching Station Throughput Across the Full Snack Line
The most common failure point in a puffed snack project is not the extruder itself but the station upstream or downstream that cannot keep pace. A turnkey puffed snack extrusion line must be engineered so that the mixer batch cycle, extruder throughput, cooler residence time and roasting capacity all align. When the cooler is undersized, product backs up and moisture migration destroys the texture you just engineered in the barrel.
Why Raw Material Dictates Screw and Die Design
Corn, wheat, rice and cassava all behave differently inside the barrel. Starch gelatinisation temperature, protein denaturation point and fibre content determine how much shear and heat the material can absorb before it either over-expands or collapses. The screw configuration and die orifice must be specified against the buyer’s actual formulation, not copied from a generic build intended for a different grain. This is the difference between consistent product density and a line that produces scrap [NEED_CITE: screw configuration selection criteria for multi-grain extrusion].
Reading the Specifications That Matter
The twin-screw design handles a broader range of cereal formulations than single-screw machines, which is essential when buyers blend wheat, corn and minor grains. Food-grade stainless steel contact surfaces (201 or 304) meet hygiene requirements and simplify washdown between product changeovers. The energy source options — electricity, gas, diesel or steam — mean the roasting and drying stages can be configured around whatever utility infrastructure the buyer’s factory already has. Electrical components from Siemens, Delixi or Delta are serviceable in most export markets, reducing the risk of extended downtime waiting for proprietary parts. Voltage and frequency are customizable per country, which matters because a 380V/50Hz machine dropped into a 440V/60Hz plant will not commission correctly without prior confirmation.
The Cost of Skipping Configuration Verification
When screw and die selections are carried over from a different grain application, the texture and density of the final puff will miss the target market expects. Undersized downstream stations create a bottleneck that forces the extruder to run below its capability. Voltage mismatches discovered at commissioning rather than at order stage delay production start by weeks [NEED_CITE: voltage and frequency standards by export market]. These are not theoretical risks — they are the most frequent complaints from buyers who sourced individual machines rather than a matched line.
Why Source This Line as a Single Project
Capacity matching across every station eliminates the finger-pointing that happens when separate vendors supply the extruder, cooler and roaster. Screw and die configuration is documented against your raw material and target product, so the build is specific rather than generic. An in-house testing workshop allows trial runs on your actual formula before shipment, catching formulation issues at the factory instead of on your floor. Pre-sales engineering covers line layout and utility planning, so the installation sequence is defined before the machines arrive. Ongoing maintenance support and wear parts supply are included, meaning screw and die replacements are available when the first changeover is due.
Documentation & Verification
- Line layout drawing with capacity calculation across all stations from mixer to packing
- Factory trial run report on your specific grain blend and moisture level before dispatch
- Screw combination and die orifice configuration record matched to your product format
- Electrical schematic with voltage, frequency and control language confirmed per destination country
- CE declaration of conformity and ISO certificate for customs and import compliance
- Operation and maintenance manual with wear parts list for local service teams
Installation, Commissioning & Support
- Floor plan review confirming utility connection points for the 100 kW electrical load or gas/diesel alternative
- Phased installation schedule aligning station assembly with local contractor availability
- First-run commissioning with screw speed, barrel temperature and feed rate set to your trial report parameters
- Operator training covering product changeover procedures and die swap sequences
- Wear parts inventory recommendation covering screws, dies and seals for the first operating cycle
- Maintenance schedule aligned with stainless steel contact surface inspection intervals
What We Need to Build Your Line Correctly
To configure a turnkey puffed snack extrusion line that holds capacity on your actual production floor, share your raw material formulation including grain types and moisture targets, the product shapes and densities your market requires, and your factory’s available voltage, frequency and energy source. If you are replacing an existing line or adding to one, let us know the upstream and downstream equipment already in place so station throughput can be matched accordingly.
Frequently Asked Questions
Q: How is the line capacity determined and validated before shipment?
A: Capacity depends on raw material type, moisture content and target product format. We run a trial in our testing workshop using your actual grain formulation and record the throughput, expansion rate and product density. This report ships with the line so the figures are tied to your specific conditions rather than a generic benchmark.
Q: How do you handle voltage and control language differences across markets?
A: Voltage and frequency are confirmed during the specification stage against your factory’s electrical supply. The control system language is set to your operator requirement before dispatch. Electrical schematics are provided so local electricians can verify connections during commissioning without guesswork.
Q: What happens if the extruder output does not match the cooler or roaster capacity?
A: Every station is capacity-calculated during the layout phase so throughput is balanced. The vibrate cooler, roasting machine and packing station are all sized against the extruder output on your specific formulation, preventing bottlenecks that occur when machines are sourced from separate vendors.
Q: How are screw and die configurations selected for different snack formats?
A: The screw combination and die design are specified based on your raw material and target product shape. The configuration record is documented and included in your delivery package, so replacements can be ordered with the exact same profile when wear parts are due.
Q: What does installation and operator training cover?
A: On-site commissioning includes station alignment, utility connection verification and first-run parameter setting based on the factory trial report. Operator training covers daily operation, product changeover, die replacement and basic maintenance. A wear parts list is provided so consumables can be planned for the first operating cycle.
Related products
-

Puff Corn Snacks Food Line Puffed Rice Ball Production Making Equipment Machines
¥10,565.00 Select options This product has multiple variants. The options may be chosen on the product page -

Corn Puff Processing Line with Mixer Fryer Baking Oven Automatic High Productivity Grain Products Snack Making Machine
¥8,300.00 Select options This product has multiple variants. The options may be chosen on the product page -

Puff Corn Extruder Machine Puffed Core Filled Snack Food Production Line Machine
¥8,500.00 Select options This product has multiple variants. The options may be chosen on the product page -

Full Automatic Crispy Maize Chocos Corn Flakes Breakfast Cereals Processing Production Line Industrial Equipment
¥1,000.00 Select options This product has multiple variants. The options may be chosen on the product page